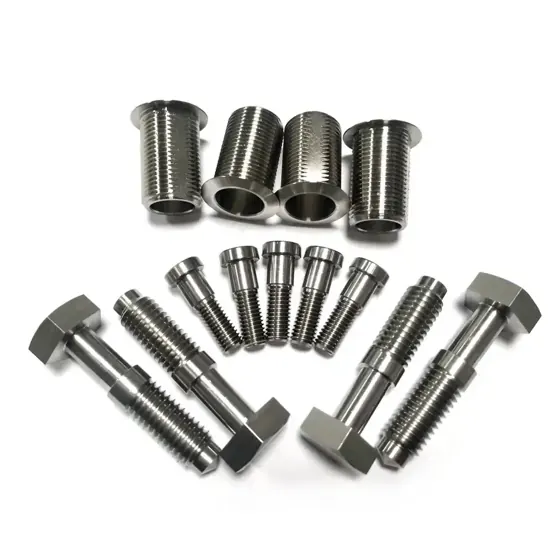
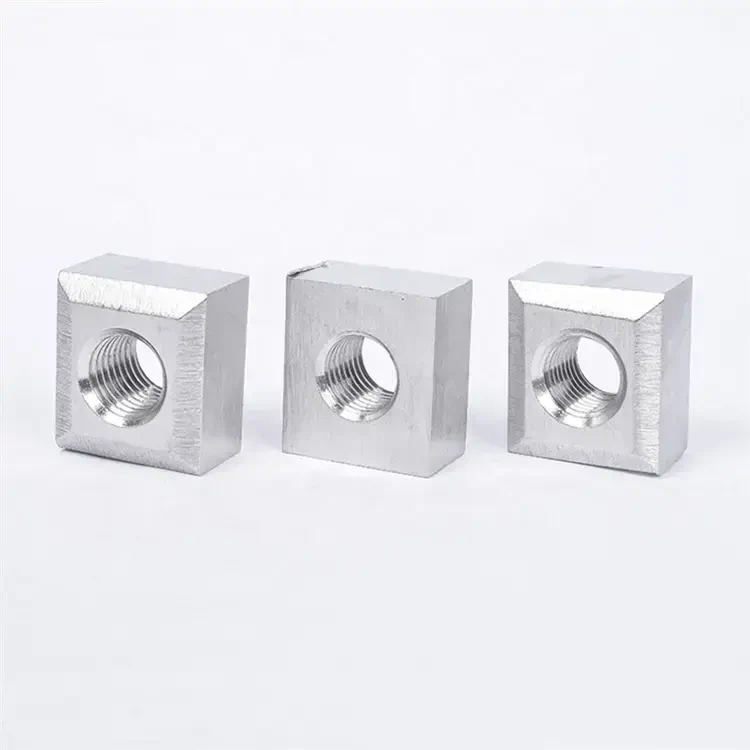
CNC Machining Parts
Wire EDM Parts
Custom wire electrical discharge machining for parts that cannot be milled or turned.
Product Overview
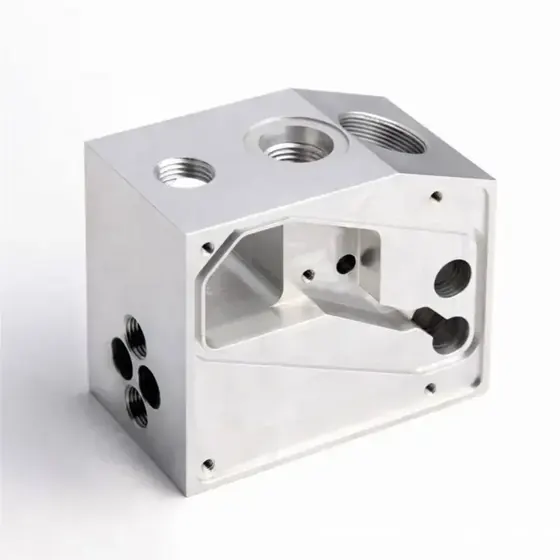
Custom wire electrical discharge machining for parts that cannot be milled or turned. A charged wire erodes the workpiece through controlled electrical discharges, so hardness does not limit the cut and there is no tool pressure to distort a thin section. Parts are made to client specification in materials including brass, copper and titanium, and the process is used for punches and dies, mould components and aerospace parts.
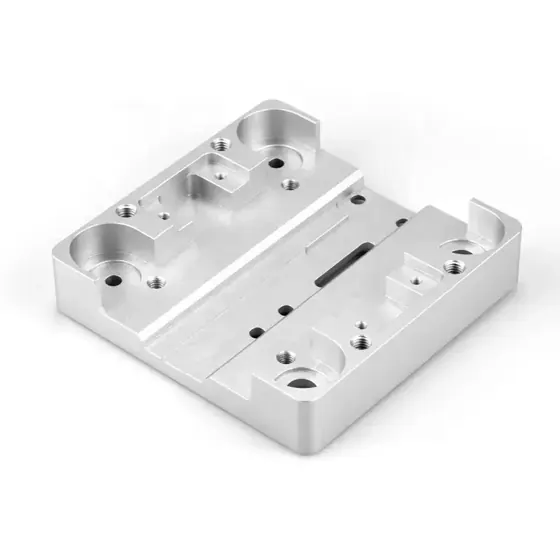
Key benefits
Why Buyers Choose This Specification
Hardness Stops Being a Constraint
Wire EDM removes material by electrical discharge rather than by cutting force, so a hardened tool steel part can be finished after heat treatment instead of being machined soft and then distorting in the furnace.
No Cutting Force on Thin Sections
Because nothing touches the part, delicate ribs and narrow webs that would deflect under a milling cutter can be produced to size.
Made to Your Specification
Parts are produced from client drawings rather than from a catalogue, which is what makes the process useful for punches, dies and mould inserts that exist only in your tooling.
Inspection Before Despatch
Parts are checked on measurement equipment by a dedicated quality control team before release, which matters most on tooling that has to fit an existing die set.
Application scenarios
Where It Is Used
- Punches and dies for press tooling
- Mould components for plastic injection moulding
- Aerospace components for aircraft and space vehicles
- Medical device parts requiring fine detail
- Extrusion dies with complex profiles
- Prototype parts in hardened material before a production tool is cut
Who it is for
The Buyers This Product Suits
Toolrooms and Die Makers
Punches, dies and mould components are the core wire EDM workload and the parts where profile accuracy decides whether the tool works.
Aerospace and Medical Suppliers
Both sectors need fine detail in difficult materials, which is where an unconventional cutting process earns its cost.
Engineers With Post-Hardening Features
If a feature has to be added after heat treatment, wire EDM is usually the only way to add it without distortion.
Problems it solves
What It Fixes
Distortion After Heat Treatment
Machining soft then hardening moves the part. Wire EDM cuts the hardened blank, so the finished geometry is the geometry that leaves the shop.
Features Too Fine for a Cutter
Narrow slots and sharp internal corners have a minimum radius set by the cutter diameter. A wire has no such minimum in the same way.
Tooling Nobody Will Quote
Custom punches and mould inserts are one-offs. They are quoted here from drawings rather than turned away as non-standard.
Specifications
Published Figures For This Product
Every value below comes from our own product specification. Where a figure is not published we leave it out rather than estimating it.
| Process | Wire electrical discharge machining |
|---|---|
| Material Removal | Controlled electrical discharges between wire and workpiece |
| Power Supply | Provides the electrical energy required for the discharges |
| Materials | Brass, copper, titanium and other conductive metals |
| Typical Parts | Punches and dies, mould components, aerospace components |
| Build Type | Custom to client specification |
| Inspection | Advanced testing equipment, dedicated quality control team |
| Grade | Custom to drawing |
Packing and documents
How It Ships And What Comes With It
Packing And Loading
Shipping volume for this item depends on the configuration and capacity you select, so no fixed container figure is published. Confirm the specification and the destination and a loading plan is issued with the quotation, rather than a figure we cannot support.
Documentation On File
- Precision Machining and Fabrication · CNC Machining Parts Specification Sheet12.6 KB
- Catalogue · Full Product Catalogue154.0 KB
Sourcing And Inspection
This product is supplied through TrueGlow Imaging, working with manufacturing partners whose facilities are visited and verified rather than taken on trust. In-process quality control and delivery supervision are available so goods are inspected before the container is sealed. Certifications quoted on this page are those stated on the product specification and belong to that product range rather than to our trading entity, so ask for the certificate covering your specific item.
Handling guide
Getting It Right First Time
Step 1
Send a 2D drawing or 3D model with the required tolerance clearly marked.
Step 2
State the material and its condition, since cutting a hardened blank changes the process plan.
Step 3
Indicate surface finish requirements on the cut faces, not just the dimensions.
Step 4
Say whether the part is a replacement for existing tooling so mating dimensions can be prioritised.
Step 5
Allow for wire EDM start holes on closed profiles when designing the blank.
Comparison
How It Compares In Our Range
When wire EDM is the right process and when milling is.
| Wire EDM | No cutting force, cuts hardened material, fine internal corners and thin sections. Slower and priced by cut length. |
|---|---|
| CNC Milling | Faster on open geometry and softer material, but limited by cutter radius, cutting force and material hardness. |
FAQ
Wire EDM Parts Questions
Can you cut hardened steel?
Yes. Wire EDM removes material by electrical discharge, so hardness does not limit the cut the way it limits a milling cutter.
Which materials do you work in?
Conductive metals including brass, copper and titanium, along with tool steels.
Do you work from our drawings?
Yes, parts are produced to client specification. Send a 2D drawing or 3D model with tolerances marked.
How is quality checked?
Parts are inspected on measurement equipment by a dedicated quality control team before despatch.
What industries do you supply?
Applications run from aerospace to medical devices, along with press tooling and injection mould components.
Can you make a single part?
Yes. Wire EDM work is usually tooling, which is ordered in ones and twos rather than in production quantities.
Related products
Other Products Buyers Look At
Industries
Sectors That Use This Product
Metal Fabrication and Machine Shops
Custom parts, tooling and the cranes that move them around the shop.
Warehousing and Heavy Industry
Lifting from 250 kg to 360 tons, indoors on a runway or outdoors on legs.
Food Packaging Lines
Depalletizing to palletizing, balanced against the filler in the middle.
Quote Wire EDM Parts
Send the capacity or size you need, the quantity and the destination, and we will confirm the configuration, the lead time and a loading plan.