Field Tested Crusher Wear Parts With Proven Performance
Manganese steel and high chromium wear parts for cone, jaw, HSI, VSI and roller crushers — bowl liners, mantles, jaw plates, blow bars, rotor tips and roller shells — plus fully customised castings poured to your drawing or sample.
Six Wear Part Families For Crushing Grinding And Shredding
Crusher dealers, quarry and aggregate operators, mining and recycling contractors, demolition fleets and OEM equipment builders who need OEM-equivalent wear parts without OEM lead times.
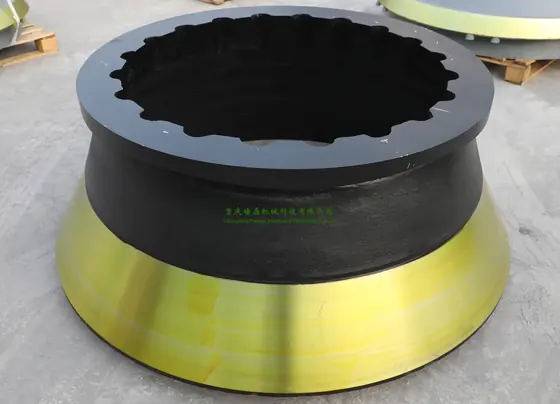
Cone Crusher Parts
High manganese bowl liners, concaves and mantles cast to suit the cone crushers already running in your pit.
Explore Range →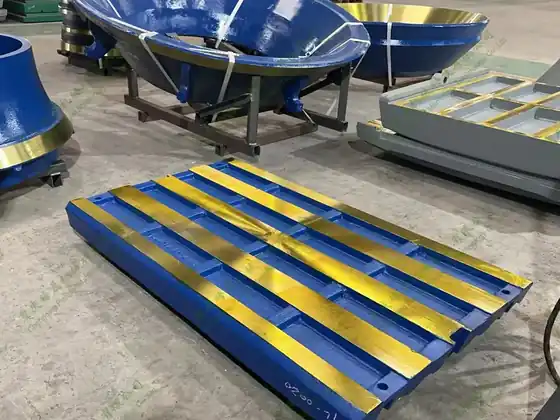
Jaw Crusher Parts
Fixed and movable jaw plates in high manganese, cast to the tooth profile your crusher was designed around.
Explore Range →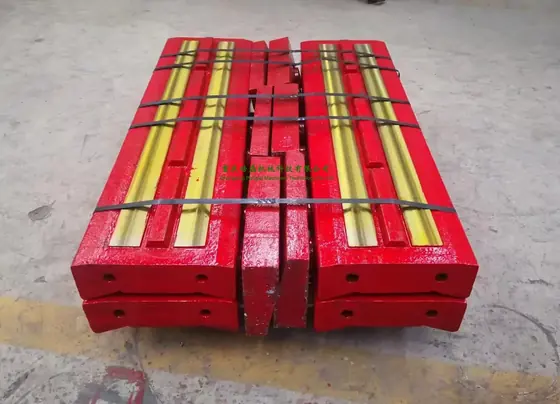
HSI Crusher Parts
Blow bars in manganese, chrome, ceramic-insert and TIC-insert configurations for horizontal shaft impactors.
Explore Range →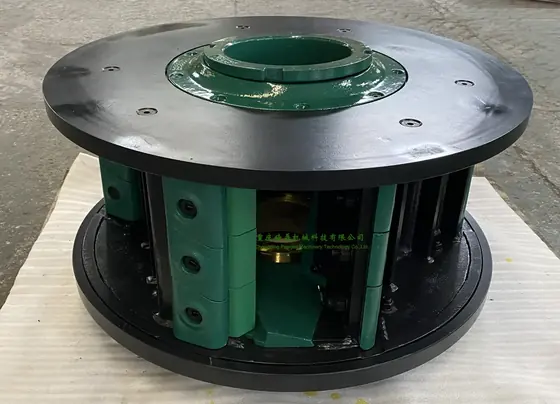
VSI Crusher Parts
The complete rotor wear package for vertical shaft impactors, held finished in stock to cut downtime.
Explore Range →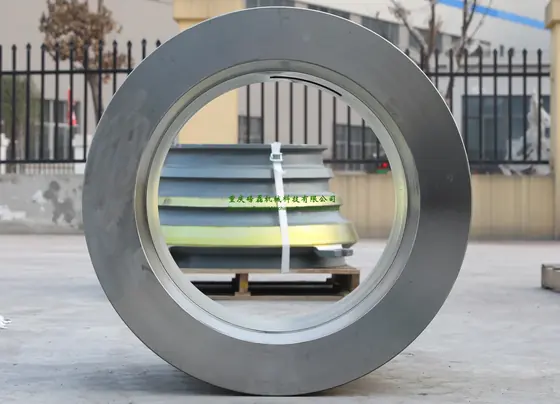
Roller Crusher Parts
Roller shells in smooth and corrugated surface, cast by a foundry that has been an OEM supplier to a roller crusher builder for years.
Explore Range →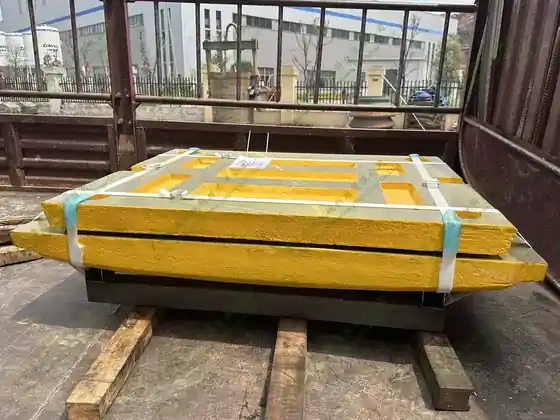
Customized Casting Parts
Wear castings made to your drawing or your sample, including parts nobody supplies any more.
Explore Range →Every Part We Cast Listed In One Place
Twenty-nine wear parts across cone, jaw, impact, VSI, roller and customised castings. Each one links to its materials, the models it suits and the inspection supplied with it.
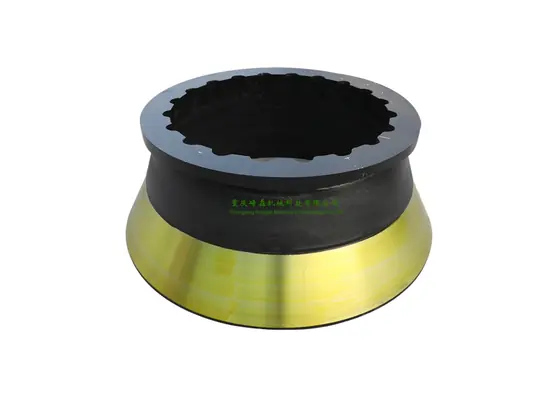
Bowl Liner And Concave
The fixed half of the cone crushing chamber, cast in seven manganese grades
View Part →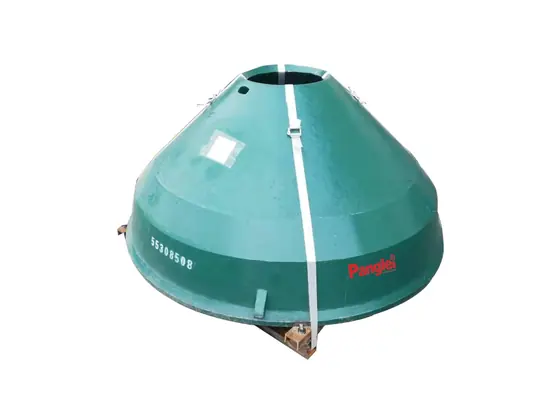
Cone Crusher Mantle
The moving cone face, cast to gyrate against your existing bowl liner
View Part →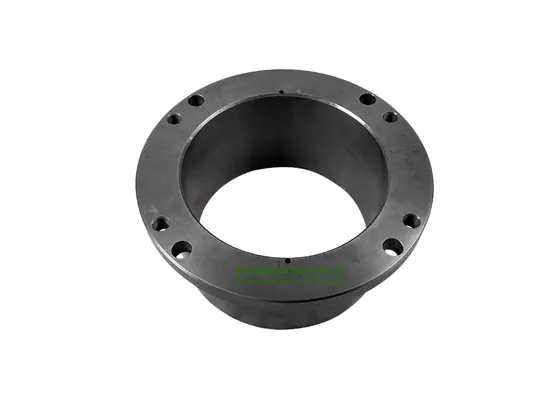
Cone Crusher Burning Ring
The sacrificial ring that protects the head above the mantle
View Part →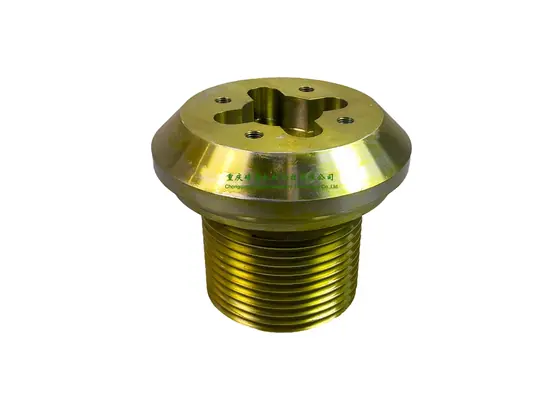
Cone Crusher Feed Plate
Distributes feed evenly into the crushing chamber and takes the impact instead of the head
View Part →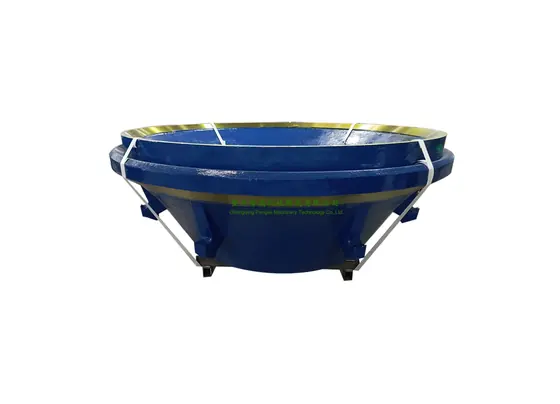
Cone Crusher Rim Liner
Protects the bowl rim above the concave from feed washing
View Part →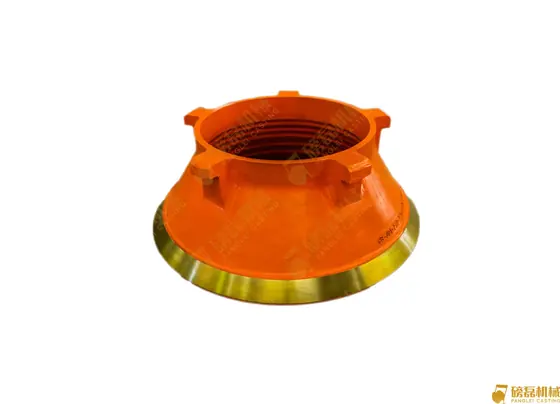
Spider Cap And Spider Arm Shield
Shields the spider bearing and arms from the feed passing over them
View Part →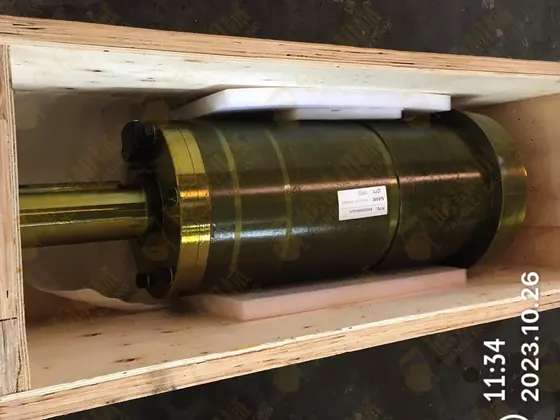
Main Shaft Assembly
Complete main shaft assemblies supplied to European customers
View Part →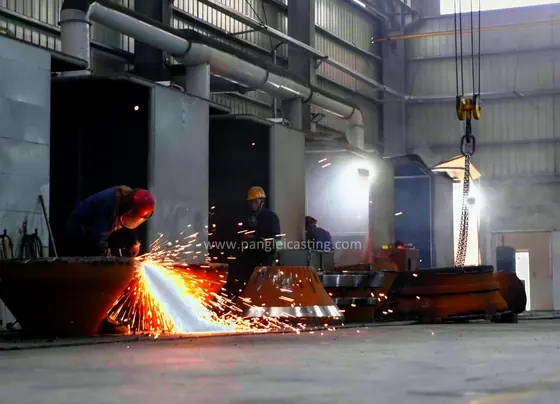
Shaft Sleeves And Bushings
Bearing surfaces machined to the fit the crusher was designed around
View Part →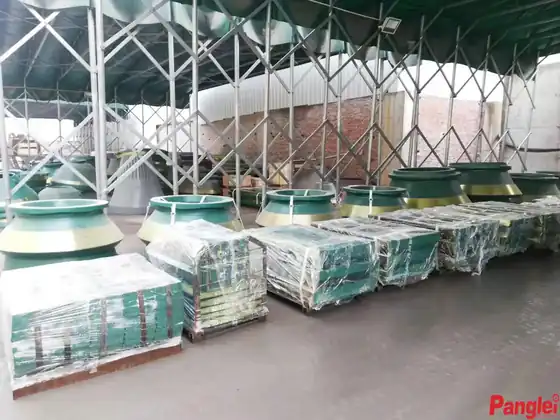
Cone Crusher Mounting Plate
The seating plate between the crusher frame and the wear components above it
View Part →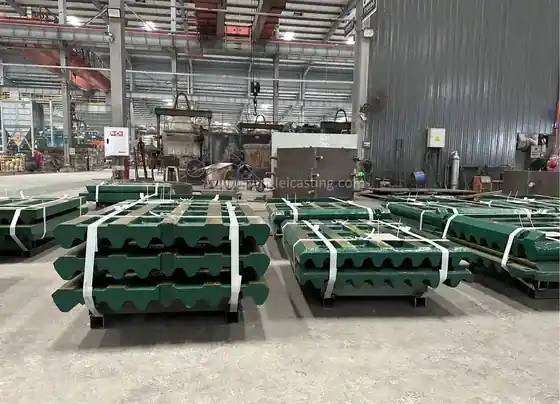
Fixed Jaw Plate
Stationary jaw dies in high manganese, from 600 × 400 machines up to a C200
View Part →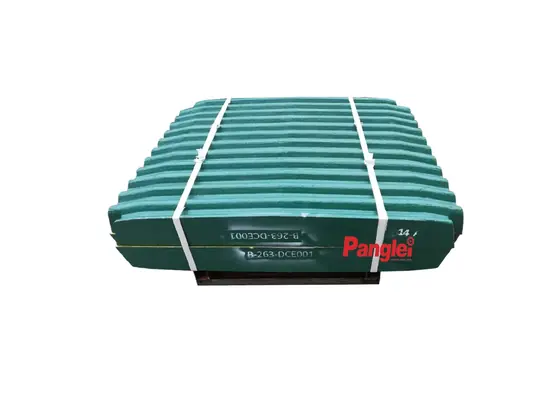
Swing Jaw Plate
Movable jaw dies cast to the same profile and heat as the fixed half
View Part →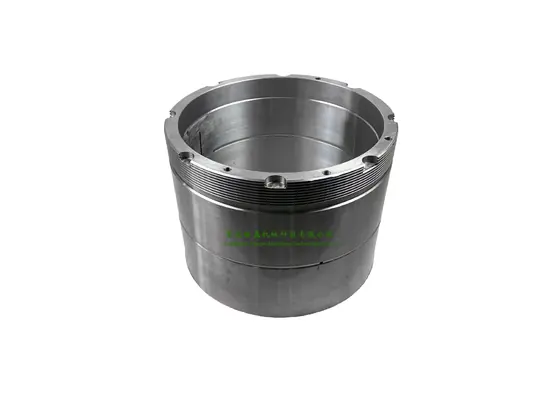
Jaw Crusher Cheek Plate
Side liners that keep the crushing chamber square and protect the frame
View Part →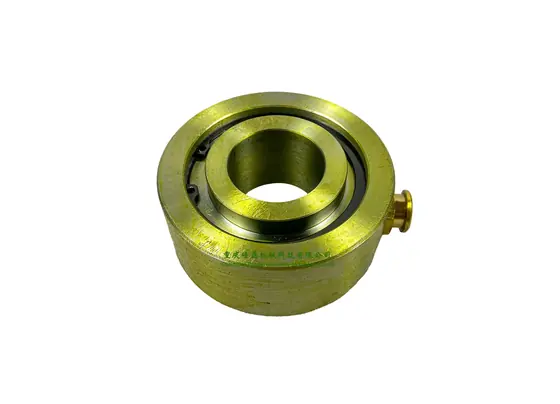
Jaw Crusher Toggle Plate
The designed weak point that protects the whole crusher from uncrushable feed
View Part →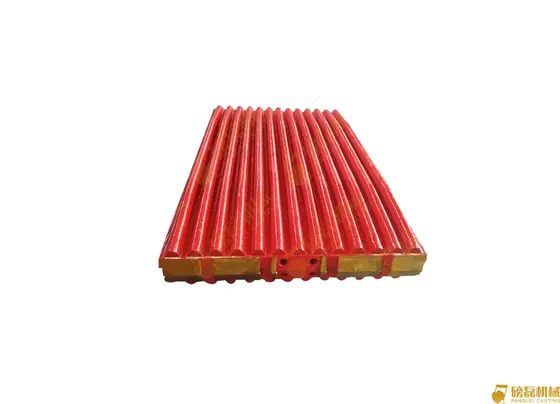
Jaw Wedges And Fixing Bolts
The clamping parts that decide whether a new die stays bedded
View Part →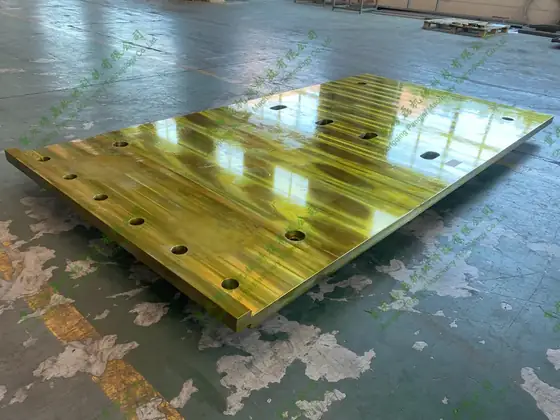
Jaw Crusher Shim Plate
Machined plate for setting the closed side setting, supplied in defined thicknesses
View Part →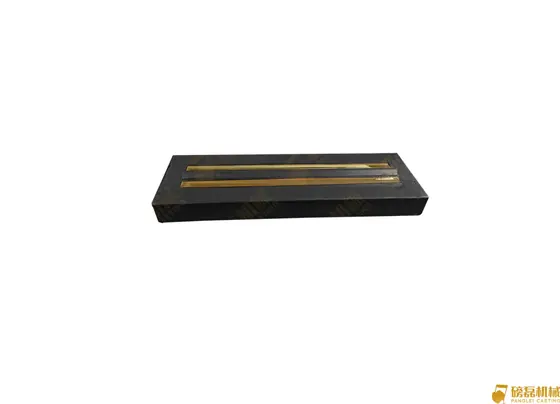
Impact Crusher Blow Bar
Manganese, chrome, ceramic-insert and TIC-insert bars for horizontal shaft impactors
View Part →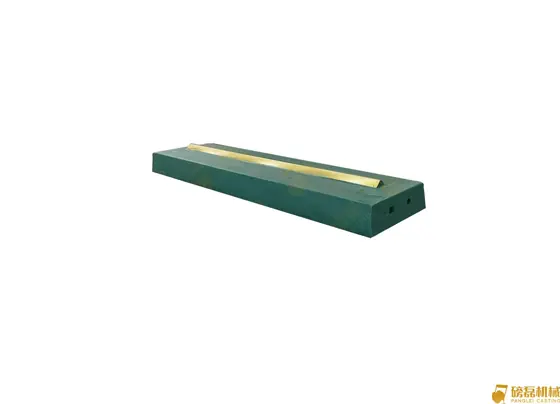
Impact Crusher Break Plate
The impact aprons that turn rotor energy into product size
View Part →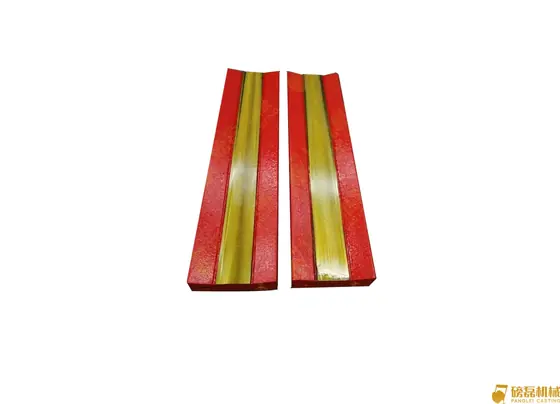
Impact Crusher Side Liner
Chamber side protection that keeps the impactor housing out of the wear path
View Part →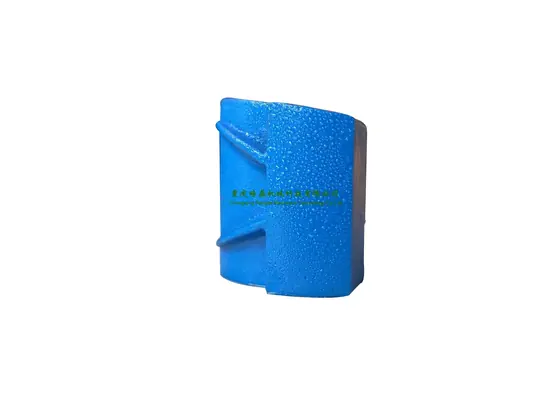
VSI Rotor Tip
High chromium tips held finished in stock so the rotor is never the reason you stop
View Part →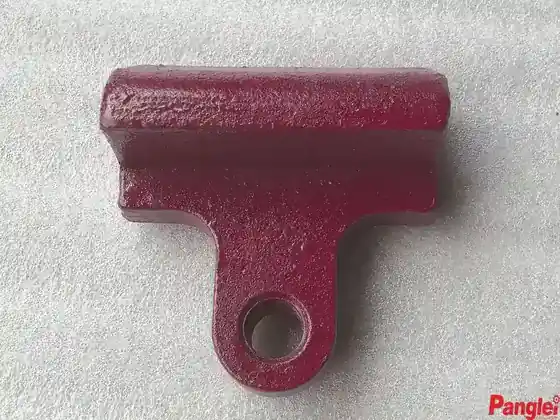
VSI Distributor Plate
Splits the feed evenly to the rotor ports so tips wear at the same rate
View Part →
VSI Feed Tube
Guides feed down onto the distributor without wearing into the rotor housing
View Part →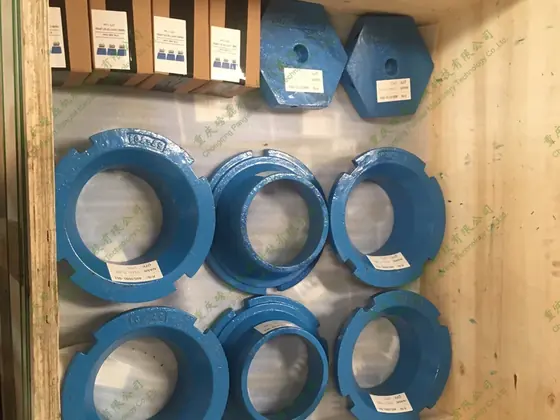
VSI Cavity Wear Plate
Lines the crushing cavity where material leaving the rotor lands
View Part →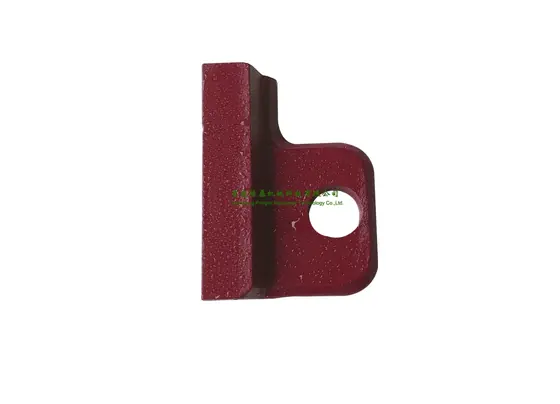
VSI Upper And Lower Wear Plates
Rotor top and bottom protection supplied as a matched set with the tips
View Part →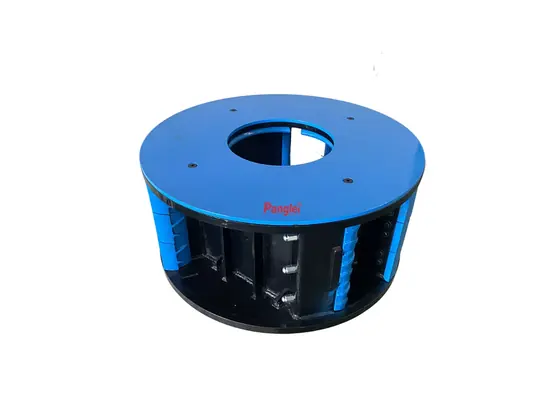
VSI Rotor Body And Frame
Complete rotor bodies for Barmac type and CV series machines
View Part →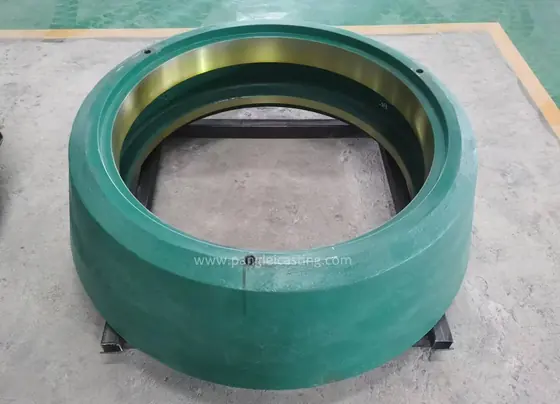
Smooth Surface Roller Shell
Smooth-faced shells for controlled reduction, cast by an OEM roller supplier
View Part →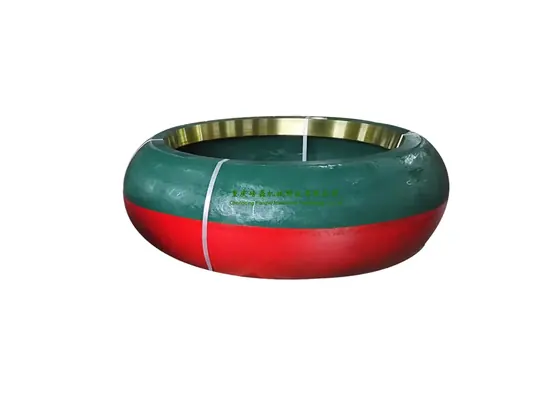
Corrugated Surface Roller Shell
Corrugated faces cast to your existing profile, not substituted with a standard pattern
View Part →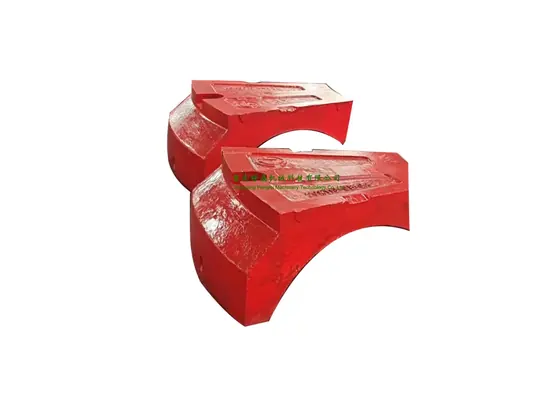
Reverse Engineered Wear Castings
From a worn part with no drawing to a repeatable casting
View Part →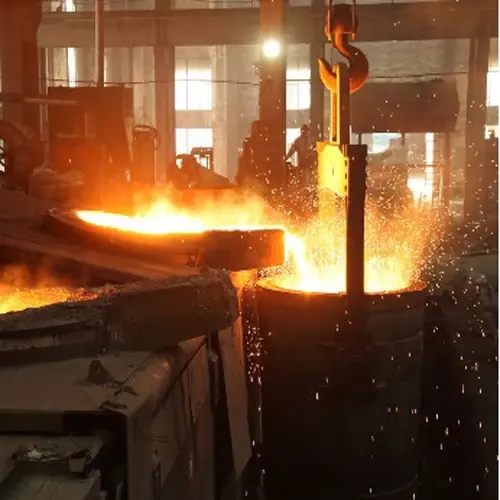
Grinding Roller
Mill grinding rollers supplied to the Chinese electric power industry
View Part →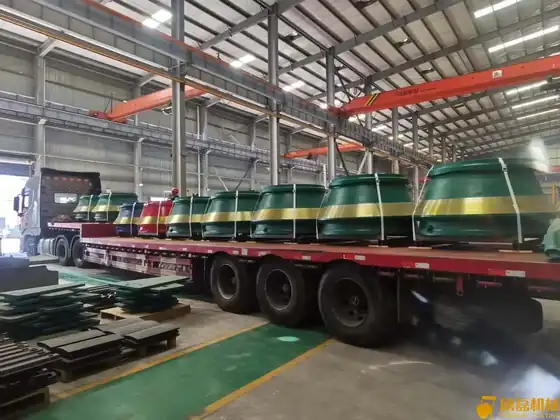
Mill Liner
Mill liners in manganese and high chromium for grinding circuits
View Part →Four Reasons A Wear Part Order Goes Wrong
Wear parts that arrive late, do not seat correctly, or wear out before the next planned shutdown. We hold thousands of finished patterns, so proven parts go straight into production instead of waiting weeks for tooling.
Parts That Arrive After The Shutdown
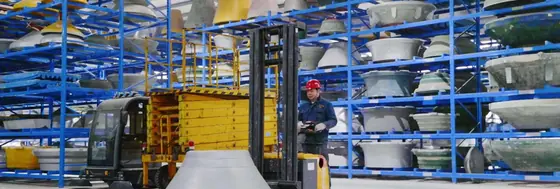
Thousands of finished patterns are already on the shelf. A part we have cast before goes straight into moulding, with no pattern cost and no pattern lead time.
Liners That Will Not Seat
Castings are machined strictly to drawing on vertical lathes up to Ø3.4 m, and a dimensional inspection report is issued before anything is packed.
The Wrong Alloy For Your Feed
Seven manganese grades from Mn13 to Mn22Cr3, three high chromium white irons and alloy steels — so the recommendation follows your rock, not our ladle.
No Record Of What You Bought
Chemical analysis on every heat, verified from a sample taken during melting and retained for at least three years.
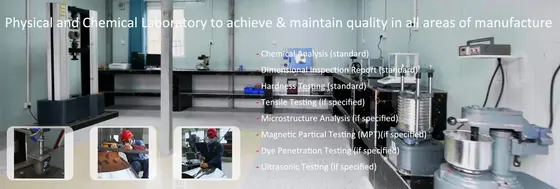
A Foundry Built New In 2022 With Its Own Laboratory
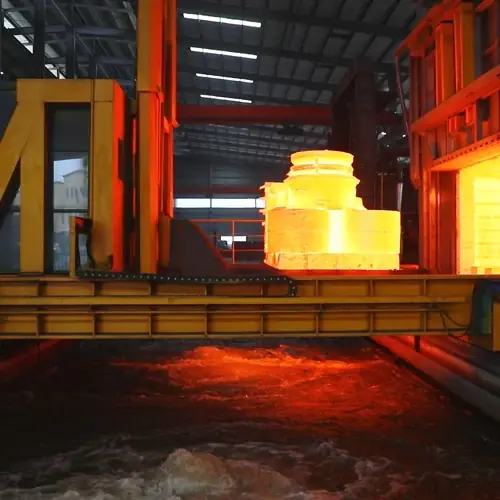
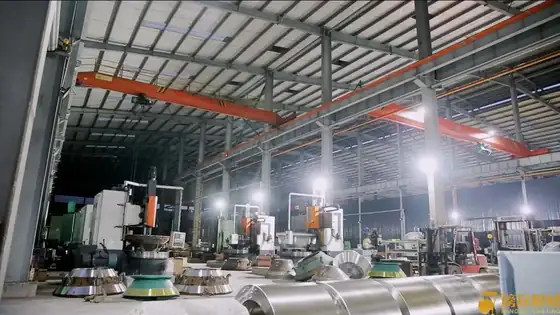
A foundry built new in 2022 with its own physical and chemical laboratory, 5-tonne induction melting, a 2,000 m³ quench pool and twelve vertical lathes — melting, heat treatment, machining and inspection all under one roof and one QC department.
Eight Controlled Steps From Drawing To Steel Pallet
Melting, heat treatment, machining and inspection all happen inside one works and under one QC department, which is why an out-of-specification analysis is corrected in the ladle rather than discovered in a finished part.
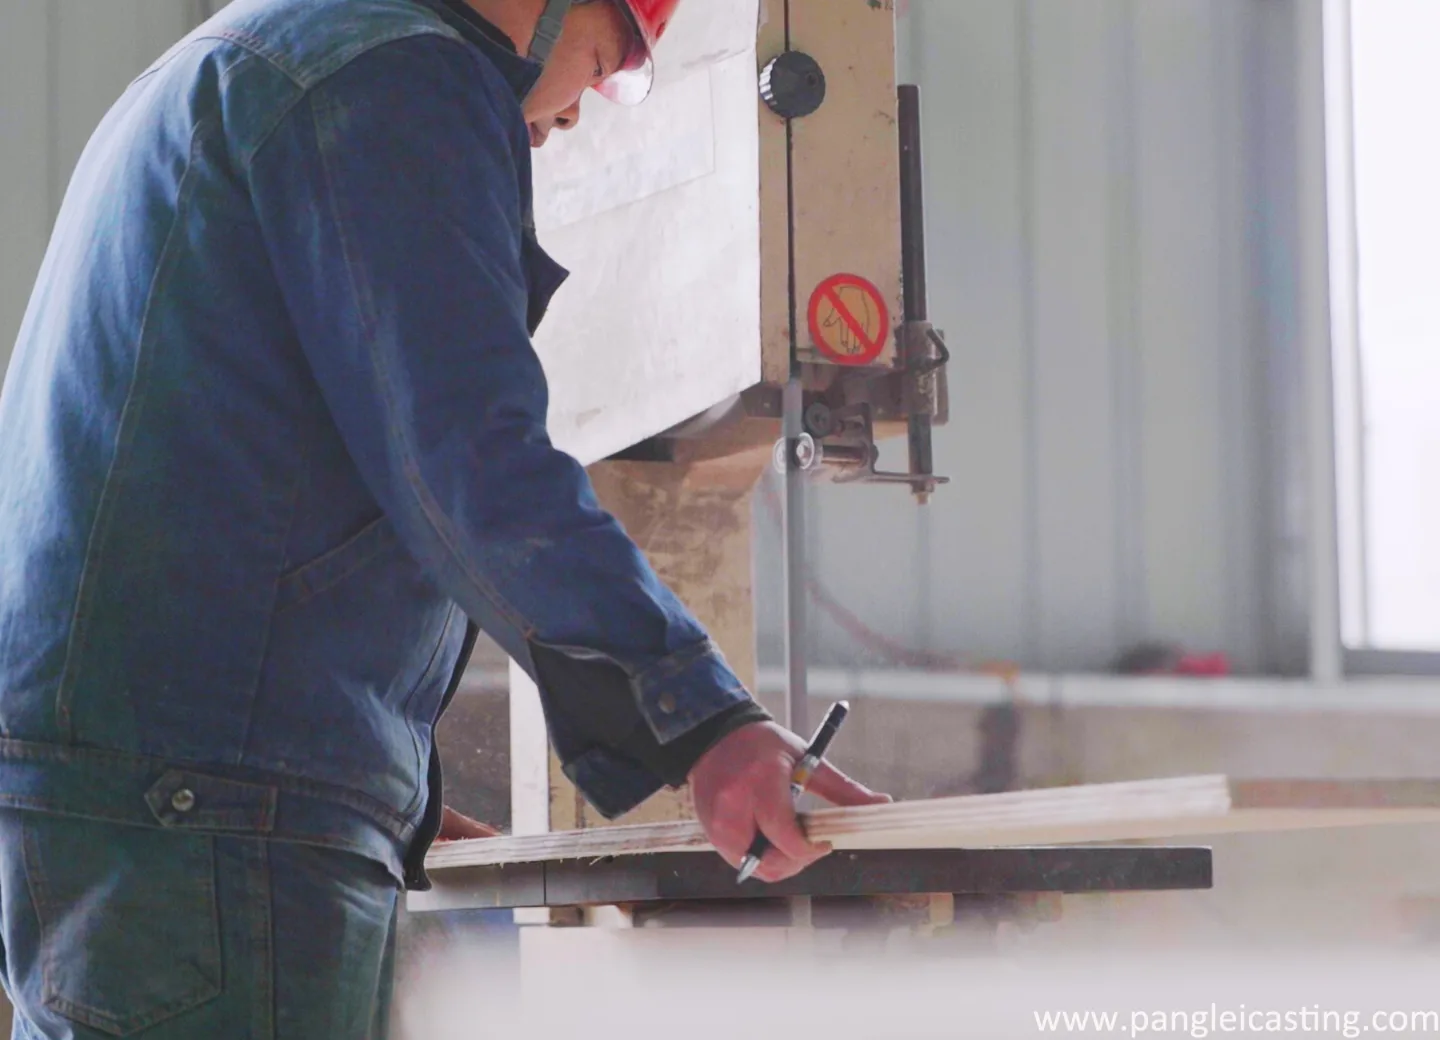
Pattern Making
Once drawings are confirmed, pattern making starts immediately in our own pattern shop. Thousands of finished patterns are already on the shelf, so repeat parts skip this step entirely.
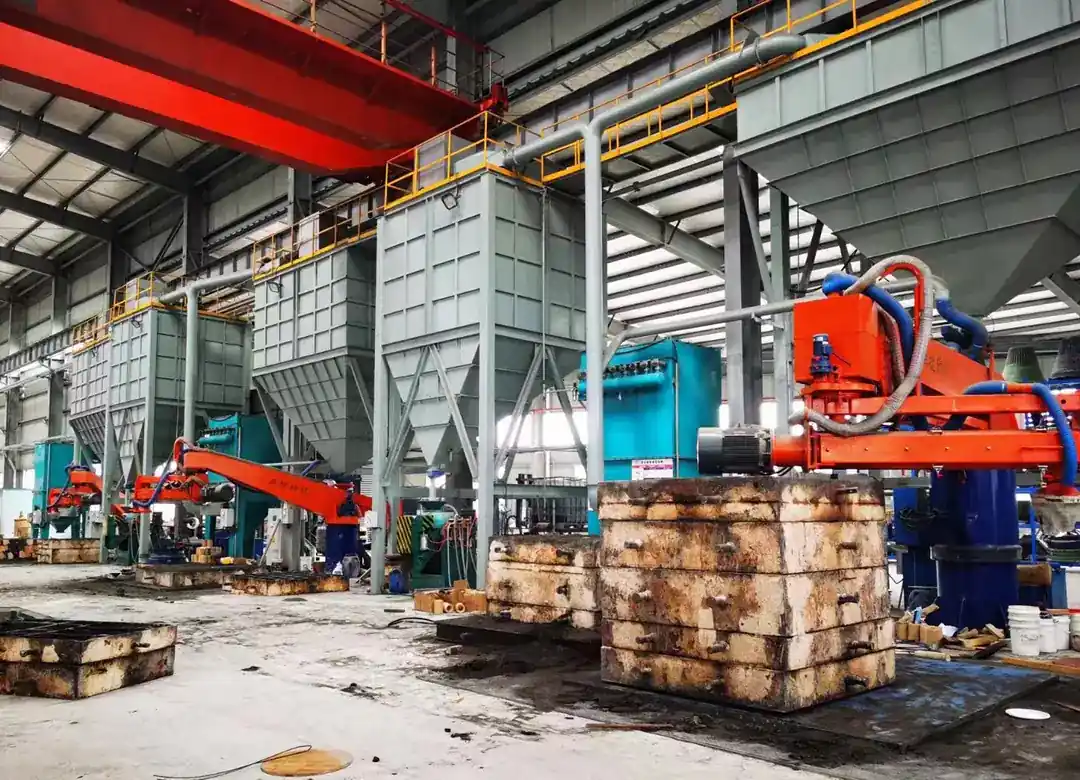
Sandbox Making
Casting Process Simulation System (CPSS) is run before the moulds are made. The cavity is kept as solid and as clean as possible so that inclusions have nowhere to start.
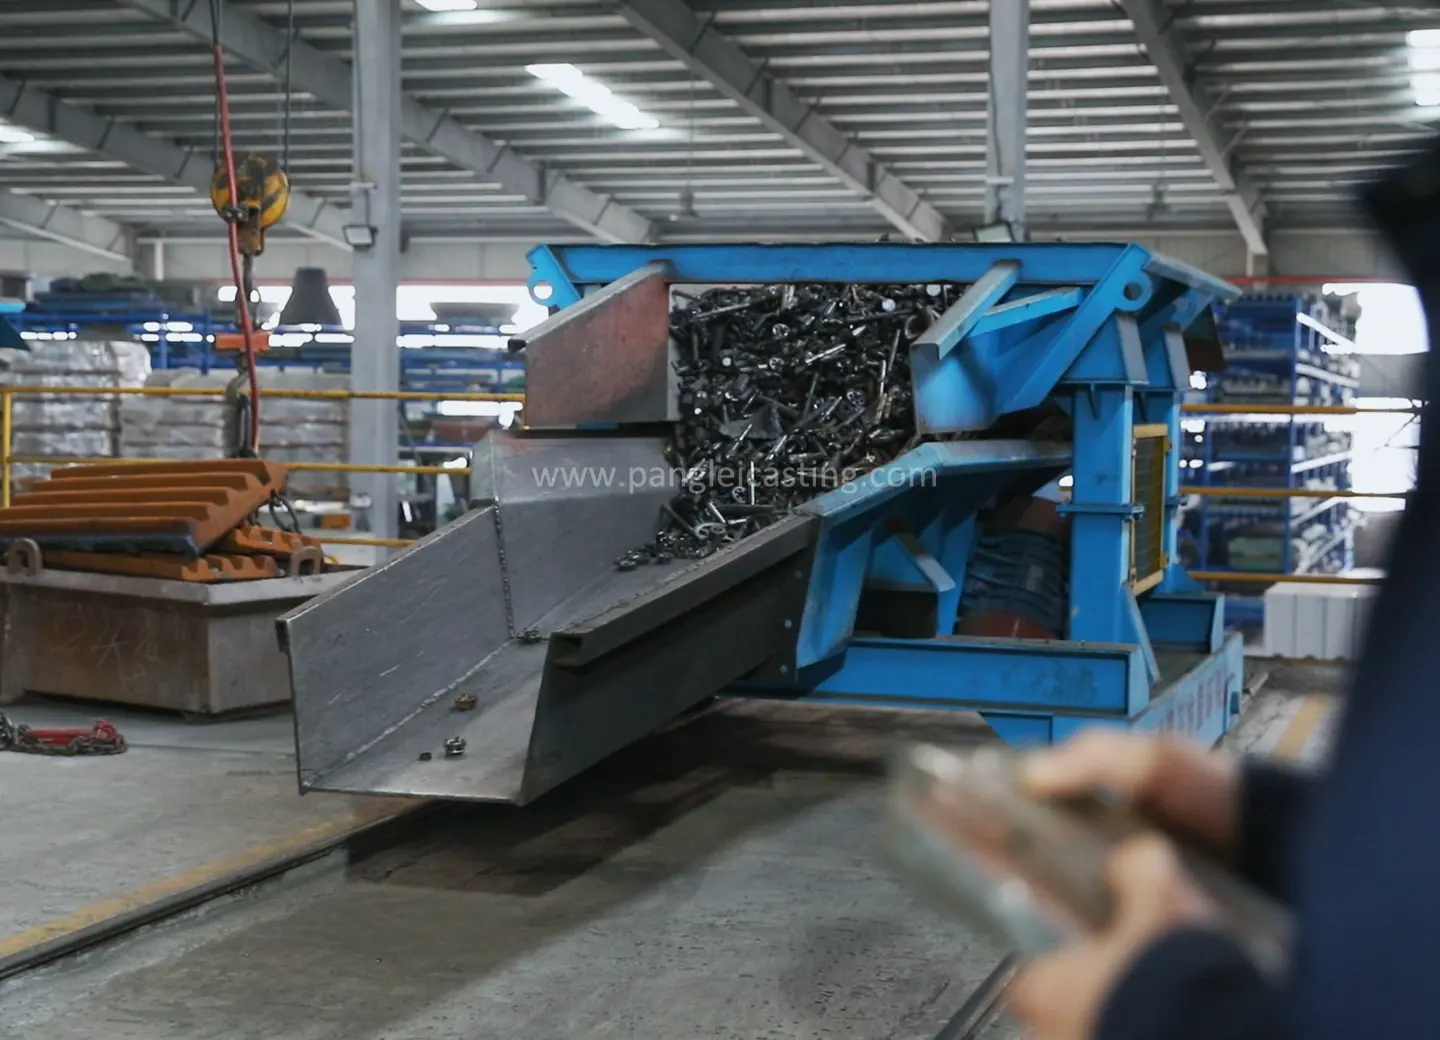
Melting And Pouring
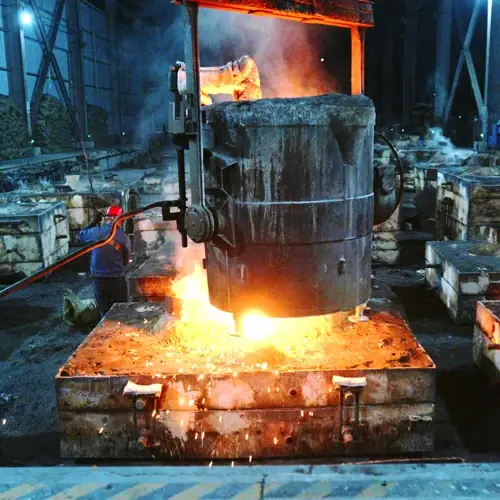
Charge materials are bought to a high standard and temperature is controlled through the whole pour to achieve a fine grain structure. Samples are taken to verify the analysis and adjusted if needed, then kept for at least three years for traceability.
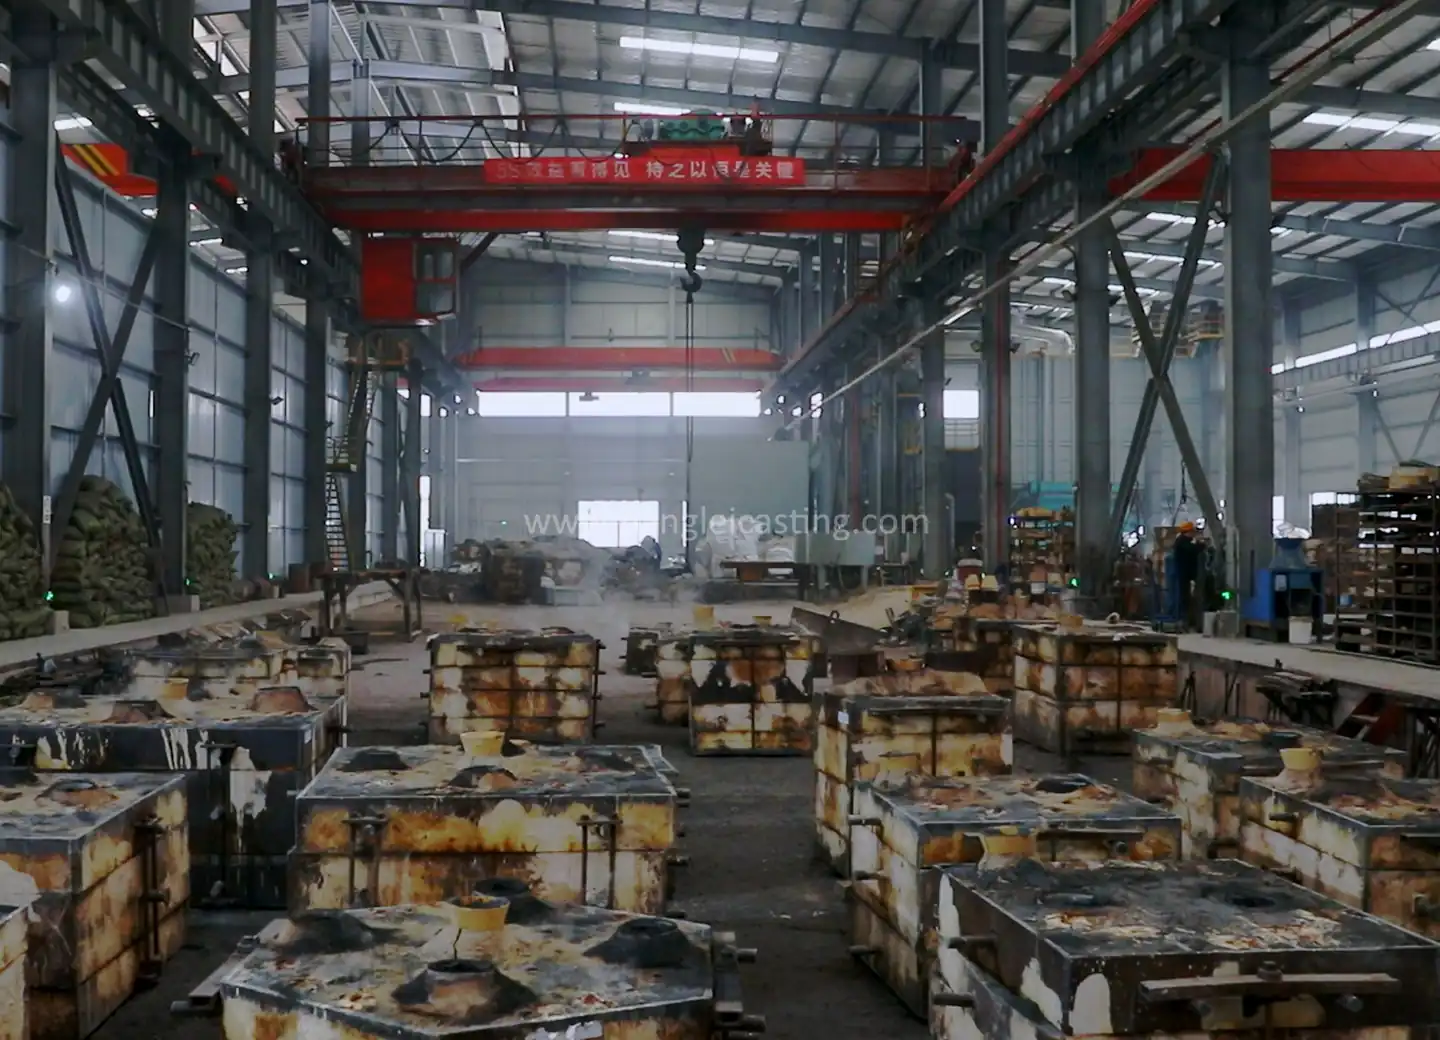
Sandbox Opening
Also called casting cleaning. After initial cooling the box is opened, risers and runners are removed and the casting is cleaned. Cooling time is set by casting size, not by the clock.
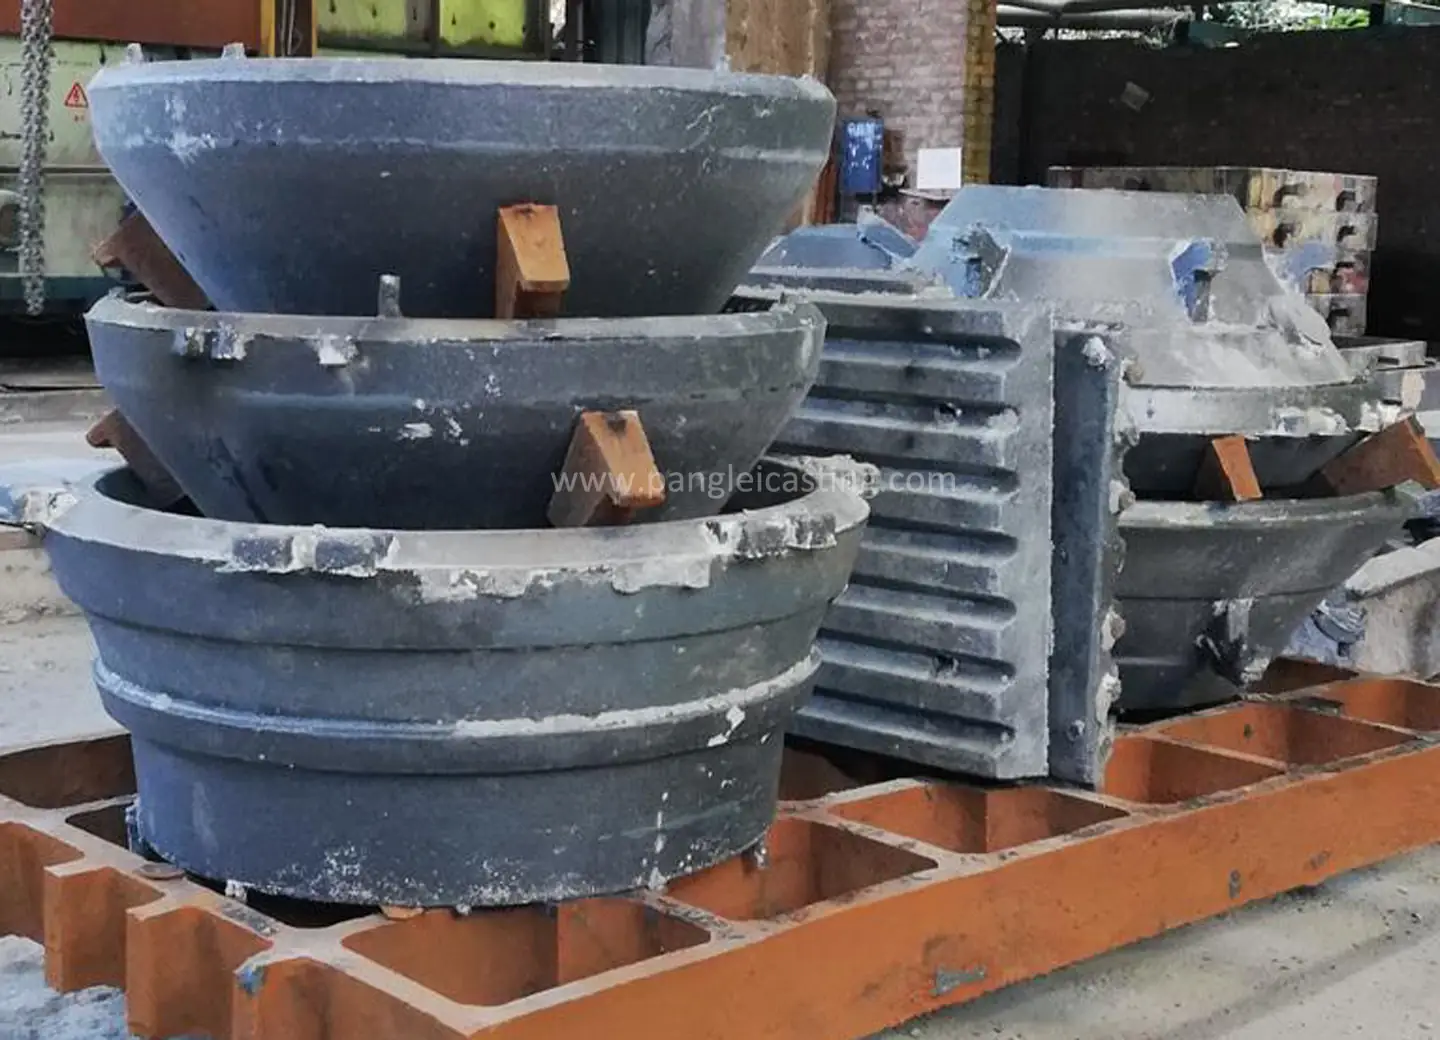
Heat Treatment
Heating temperature is strictly controlled and castings are spaced in the furnace so they heat uniformly and meet the water fully. Quenching begins within 30 seconds of withdrawal from the oven.
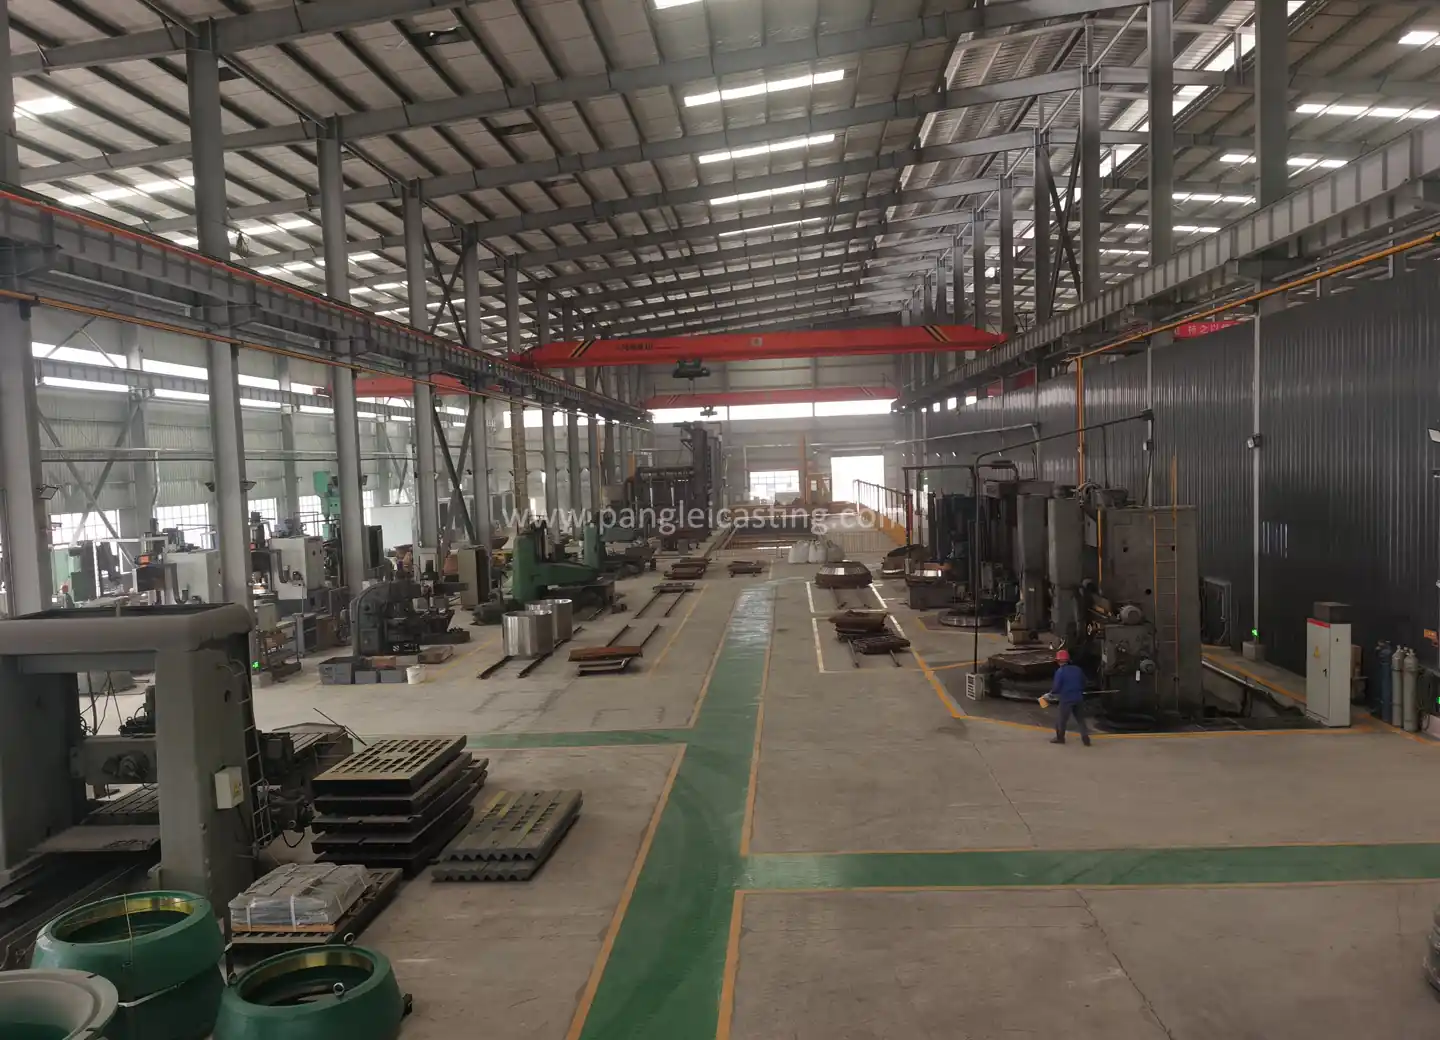
Machining
After rectifying and polishing, castings are machined strictly to drawing for correct fitment. QC then carries out dimensional inspection and issues the dimensional inspection report.
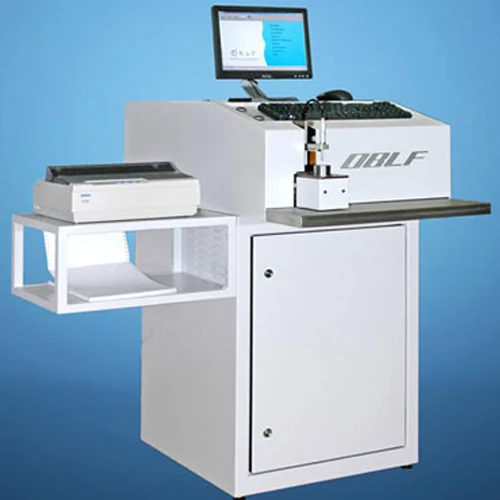
Inspection
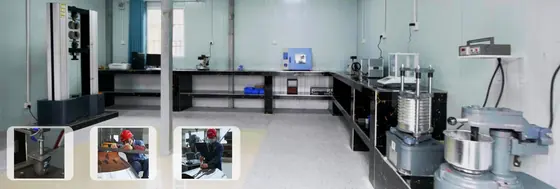
Our own physical and chemical laboratory covers spectrometry, hardness, microstructure, dye penetrant and dimensional inspection on site rather than at a third party.
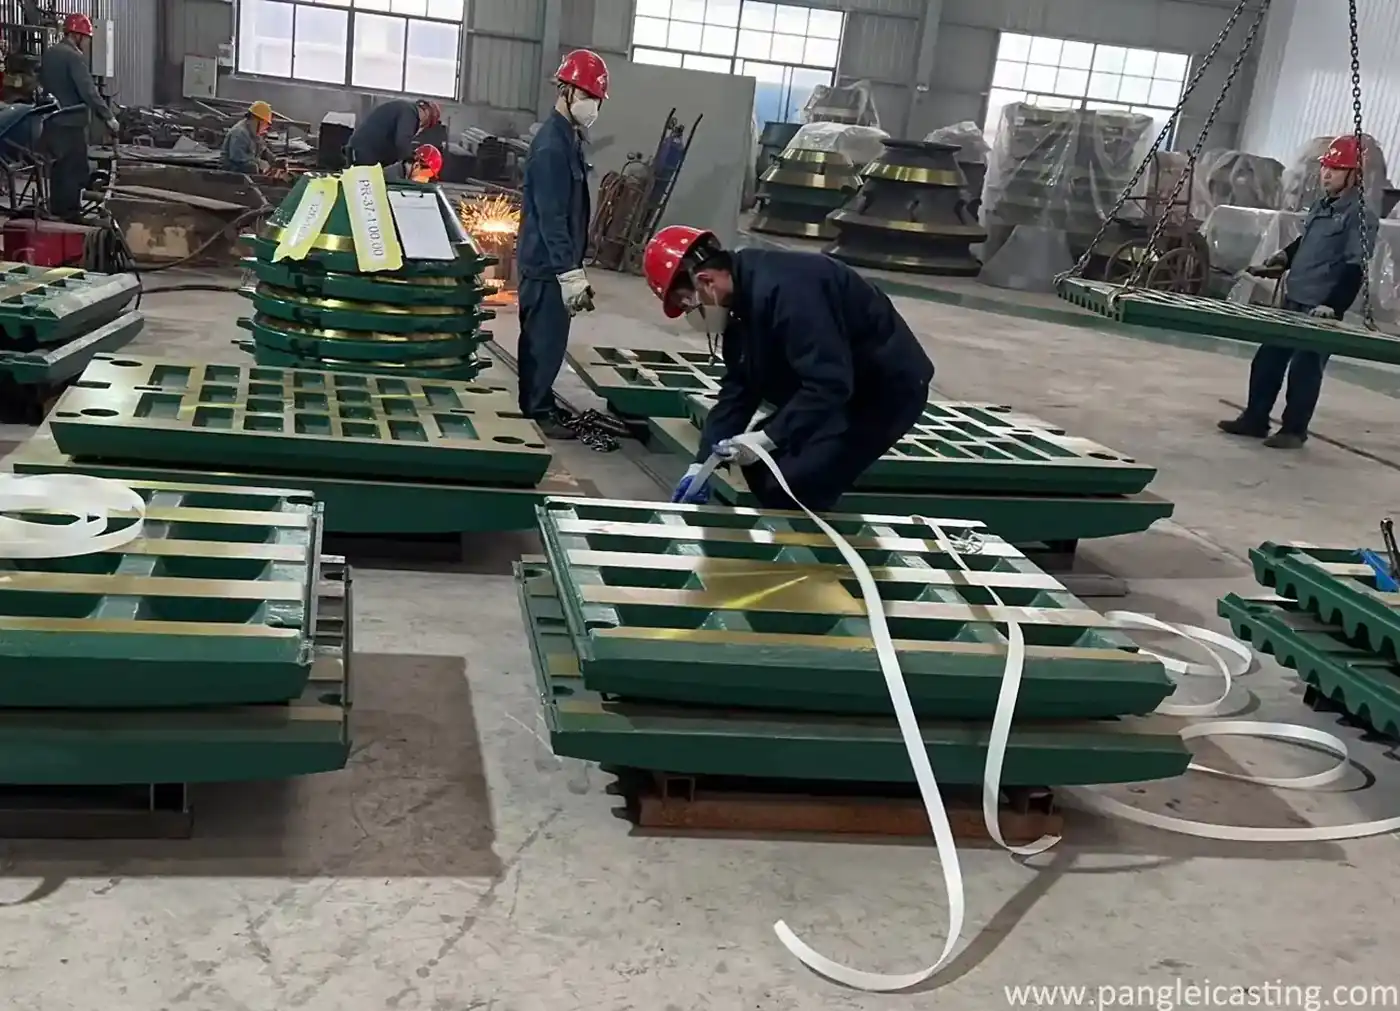
Packing And Delivery
Finished parts are packed on steel pallets for forklift handling, to international standards for road, rail, sea and air transport.
Industries Running Our Castings Today
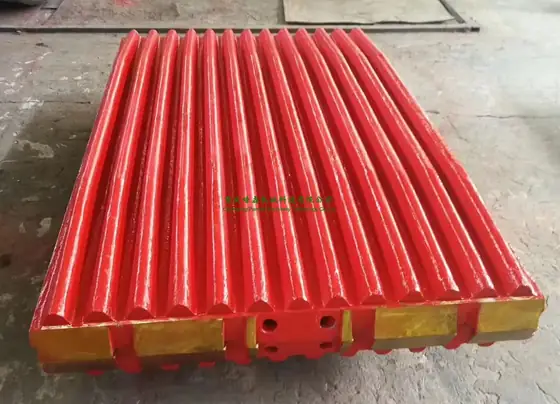
Quarrying And Aggregates
Wear parts for the crushing circuits behind every aggregate plant
See Applications →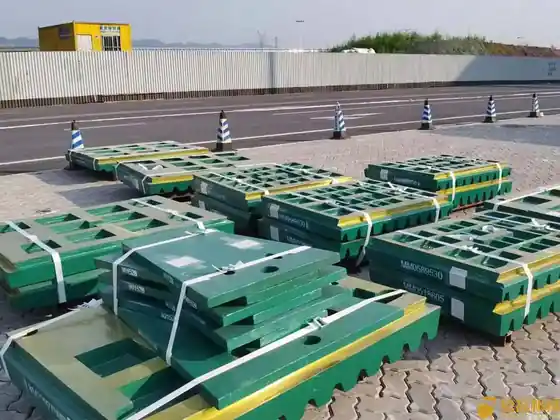
Mining And Ore Processing
Crusher and mill wear parts for copper, iron ore and hard rock operations
See Applications →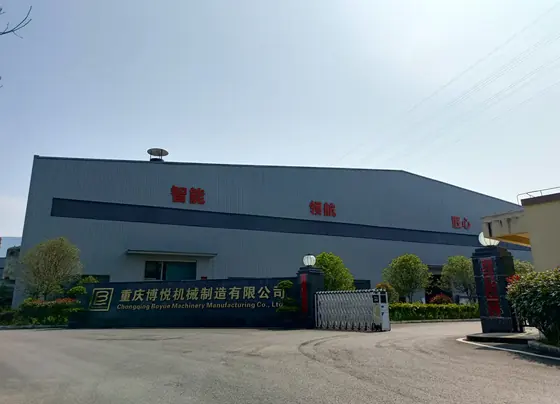
Recycling And Demolition
Wear parts built for feed that contains steel as well as stone
See Applications →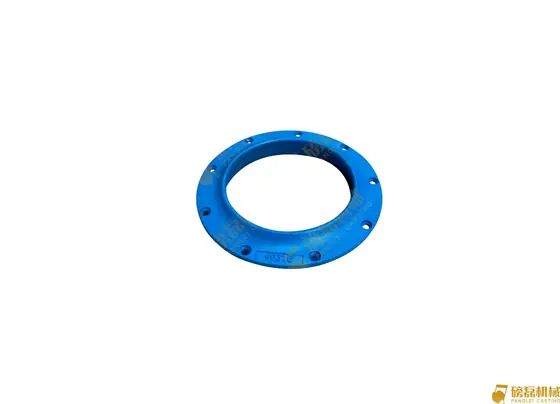
Power Generation
Grinding rollers and mill liners for coal-fired generation
See Applications →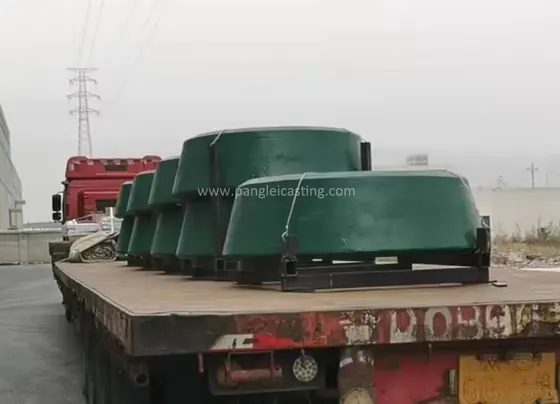
OEM Equipment Manufacturers
Contract casting for crusher and roller machine builders
See Applications →How We Work When There Is No Catalogue Number
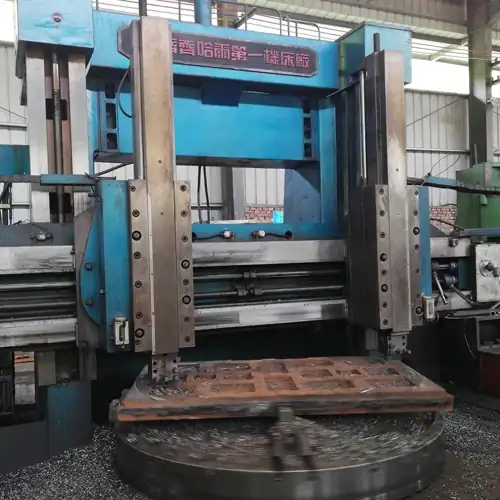
Reverse Engineering And 3D Scanning
From a worn part with no drawing to a repeatable casting
How It Works →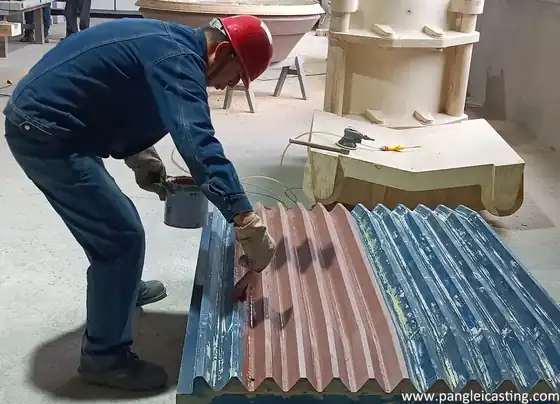
Ready Made Pattern Inventory
Thousands of finished patterns already on the shelf
How It Works →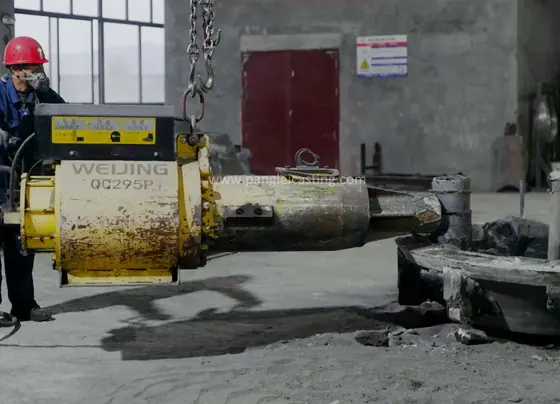
Wear Material Selection
Matching the alloy to the feed rather than to the catalogue
How It Works →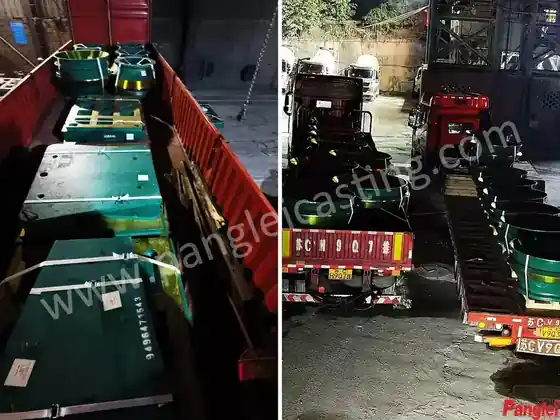
OEM Contract Casting
Wear part programmes for equipment manufacturers
How It Works →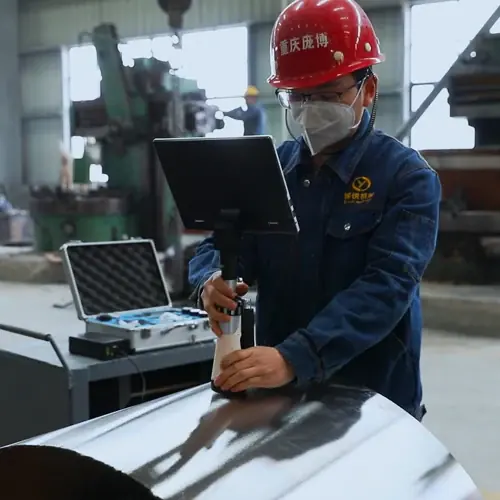
Export Packing And Delivery
Steel-palletised packing and door-to-door delivery from Chongqing
How It Works →The Works At Beidu Aluminium Industrial Park
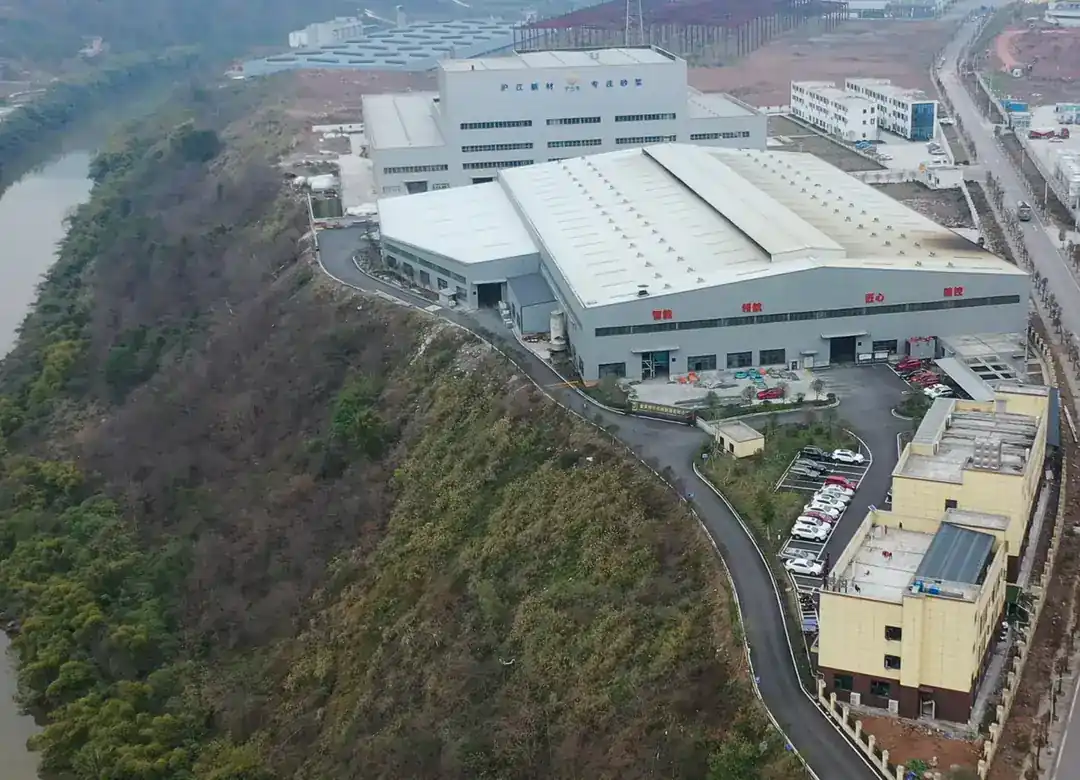
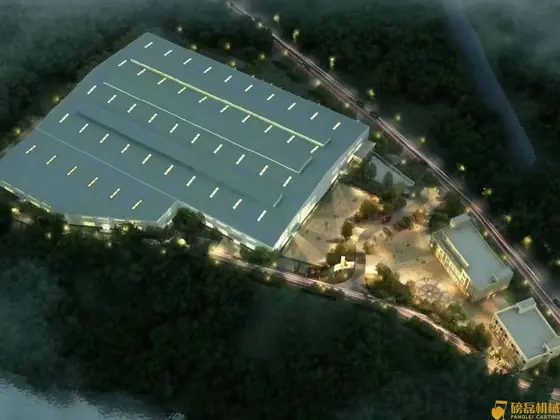
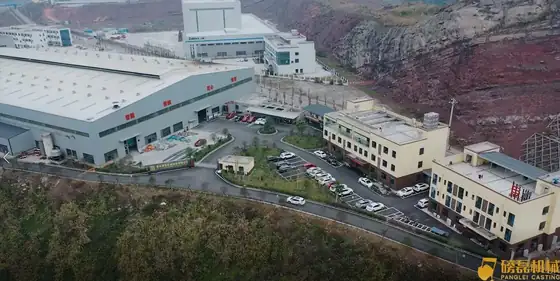
We moved into the new foundry at the end of 2022 after two years of building. The site covers about 26,680 m² and on-site visits are warmly welcomed.
Parts We Have Supplied Under Real Part Numbers
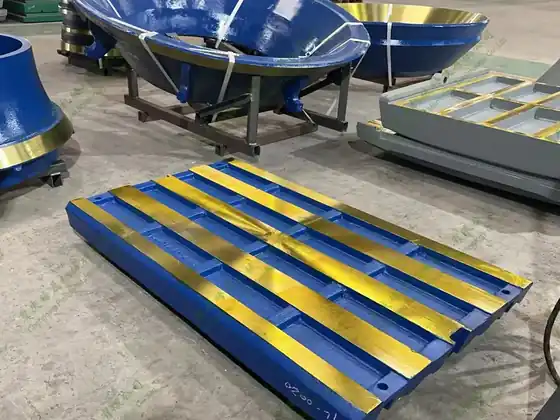
Swing Jaw Plate 600/3012 For A Pegson 1100 × 800 In Liberia
600/3012 swing jaw plate in Mn22Cr2
Read The Case →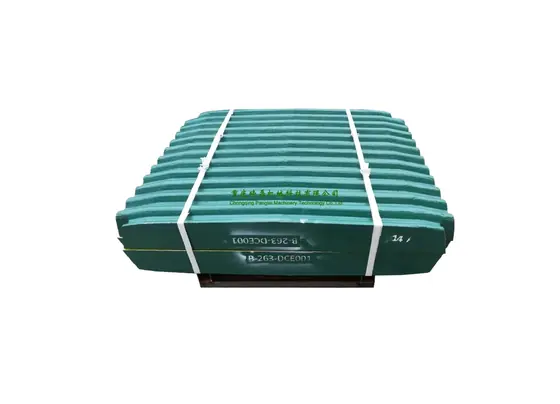
Extec C10 Jaw Dies J6920000 And J6930000 In Mn18Cr2
J6920000 fixed jaw die and J6930000 swing jaw die in Mn18Cr2
Read The Case →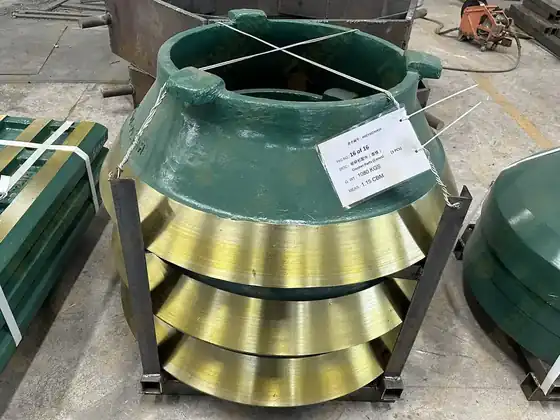
Repeat Cone Sets 603/9052 And 603/9106 For A Pegson 1000 Maxtrak
603/9052 bowl liner and 603/9106 mantle in Mn22Cr2
Read The Case →Material And Process Guides For Buyers Of Wear Parts
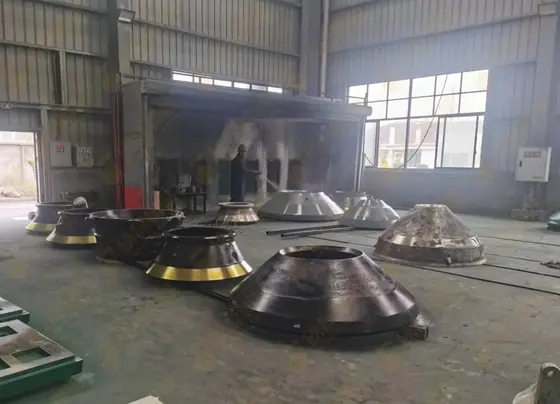
Manganese Steel Grades For Crusher Wear Parts Explained
Mn13 through Mn22Cr3 — what the manganese and chromium content actually changes, and how to pick a grade from your feed rather than from a catalogue.
Read Guide →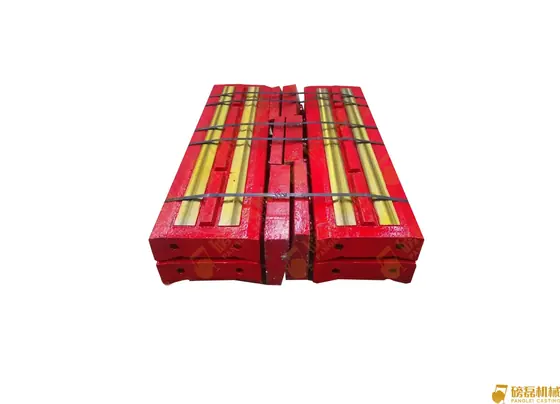
How To Choose Blow Bar Material For An Impact Crusher
Manganese, 20% chrome, 26% chrome, ceramic inserts or TIC — a decision that comes down to one question about your feed.
Read Guide →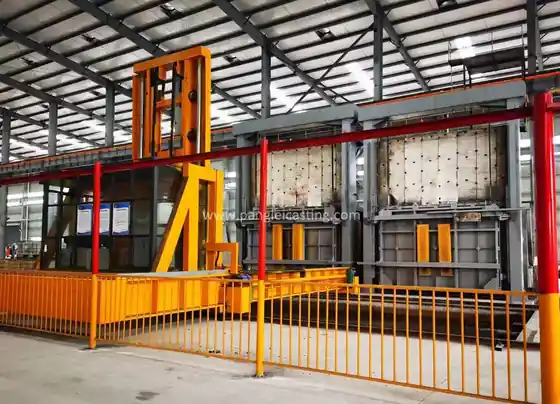
Heat Treatment Of Crusher Wear Castings And Why 30 Seconds Matters
Solution treatment and quenching decide whether a manganese casting is tough or brittle. The controls that make the difference are simple and unforgiving.
Read Guide →Questions Buyers Ask Before The First Order
What exactly does PangLei Casting manufacture?
Wear-resistant castings for crushing equipment: bowl liners, concaves and mantles for cone crushers, fixed and swing jaw plates, blow bars for impactors, rotor tips and wear plates for VSI machines, roller shells, and fully customised castings to drawing or sample.
Are these OEM parts?
No. They are OEM-equivalent parts manufactured and warranted by PangLei. Manufacturer names, part numbers and model numbers are used for identification only, and we have no association with the OEM.
Which materials do you pour?
Austenitic manganese steels Mn13, Mn18, Mn13Cr2, Mn18Cr2, Mn22Cr2 and Mn13-22CrMo; high chromium white cast irons Cr15, Cr25 and Cr30; and alloy steels of various grades.
How large a casting can you produce?
Up to 10 tonnes as a single casting, melted in two 5 t intermediate frequency furnaces and machined on vertical lathes up to Ø3.4 m.
Can I visit the foundry?
Yes. On-site visits are warmly welcomed. Since the new foundry began running at the end of 2022, a number of clients have chosen to work with us after visiting.
How do you ship to Europe?
Three routes. Air from Chongqing Jiangbei International Airport, rail on the Chongqing–Xinjiang–Europe line through Kazakhstan, Russia, Belarus and Poland to Duisburg, or sea freight via Shanghai Port, about three days inland from us. Door-to-door delivery is available.
Send Us A Part Number Or A Photograph Of The Worn Part
Tell us the machine model and the part number, or send a photograph and the main dimensions. We will confirm whether the pattern is already held and quote from there.