Jaw Crusher Toggle Plate
The designed weak point that protects the whole crusher from uncrushable feed
What This Casting Does And Why It Matters
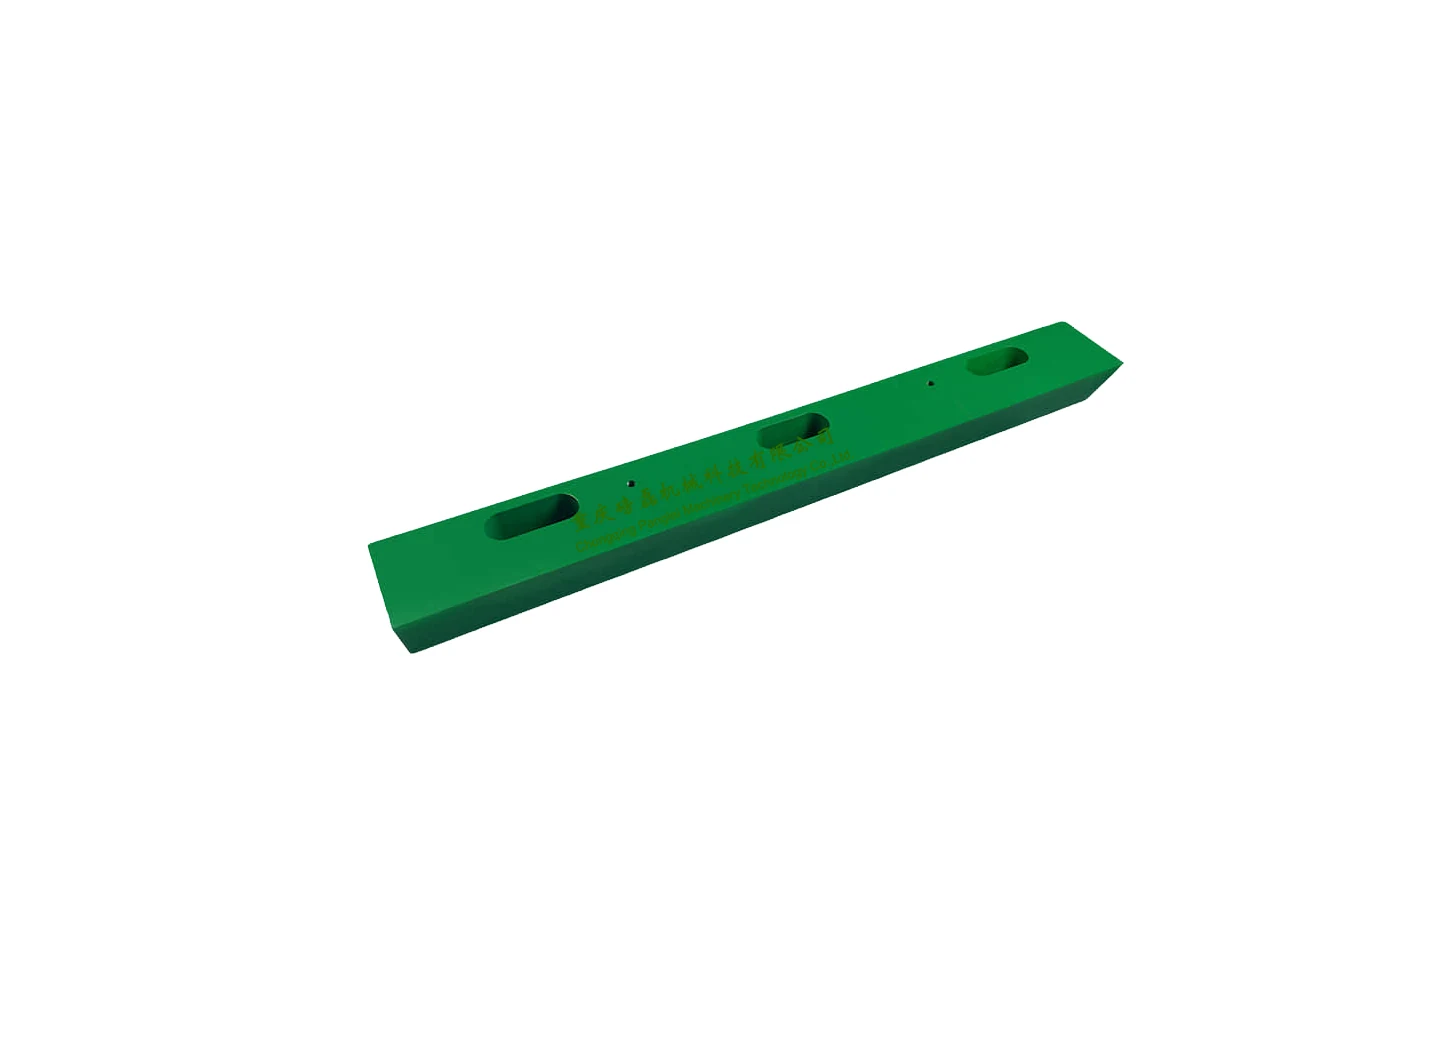
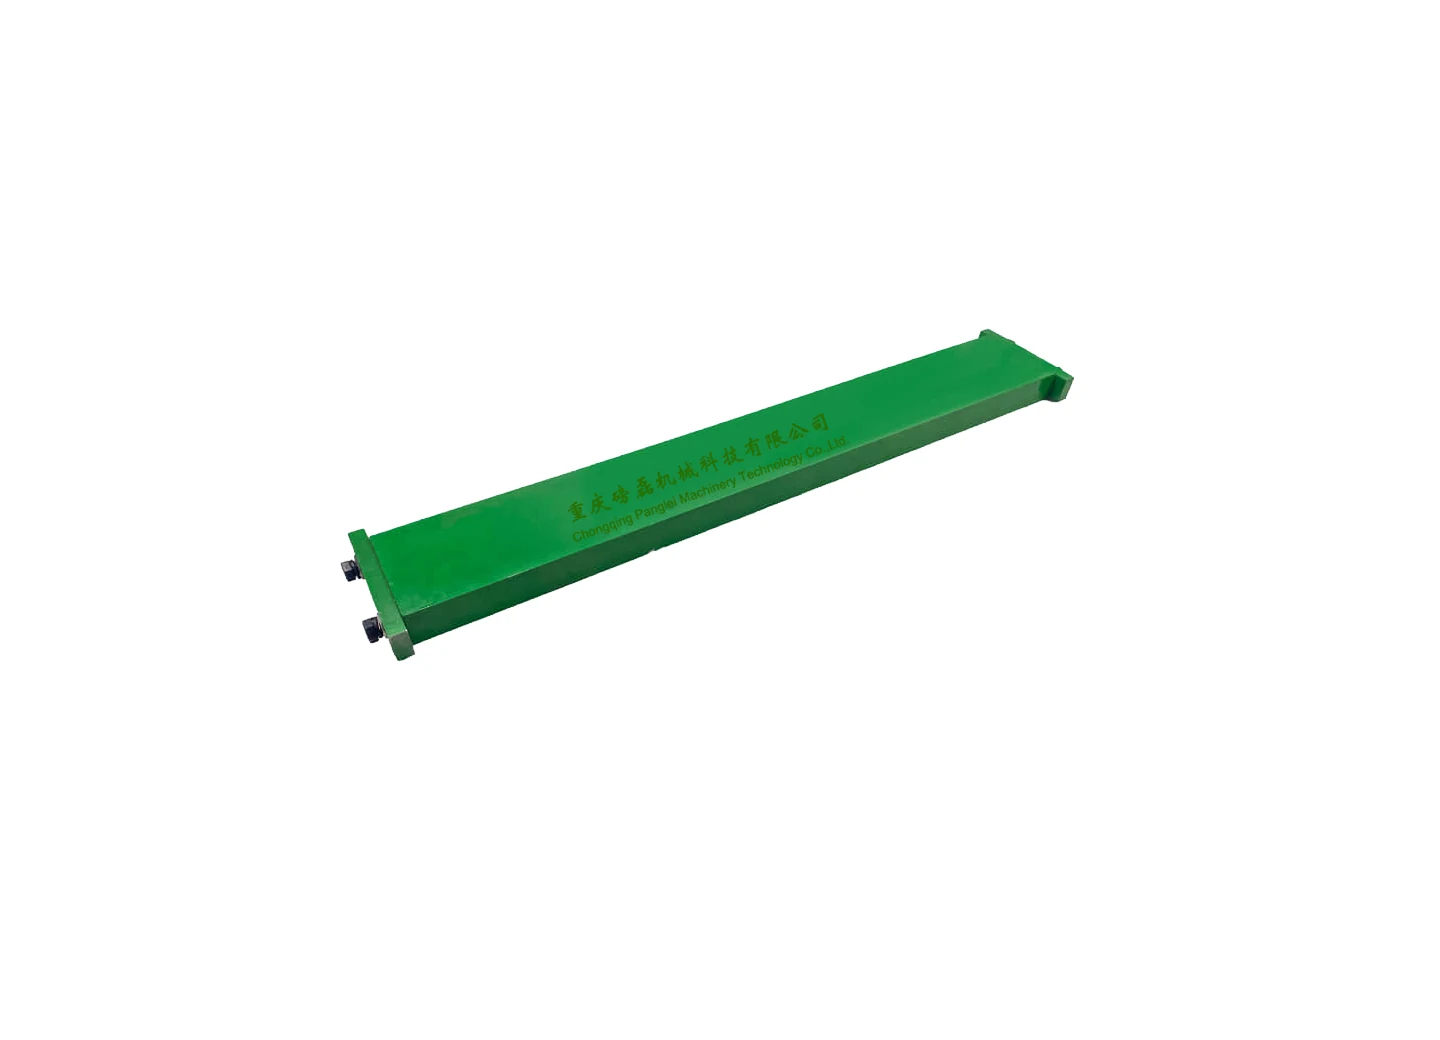
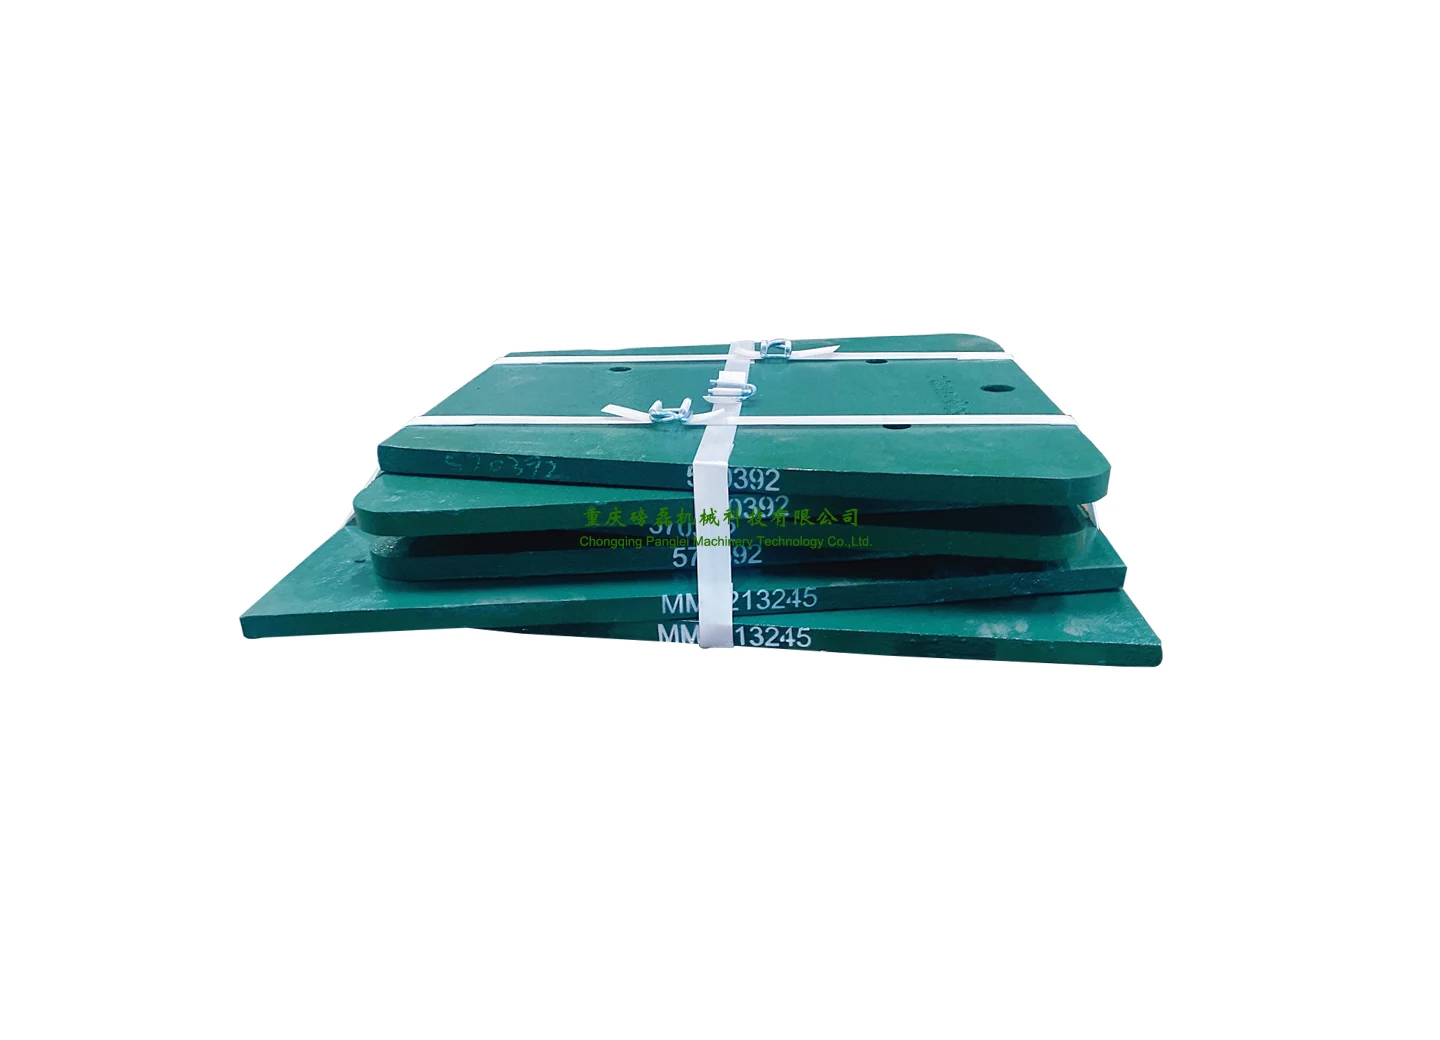
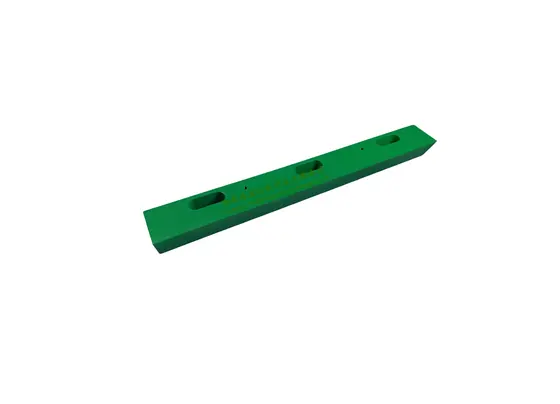
A toggle plate is meant to fail. When a piece of uncrushable steel enters the chamber, the toggle breaks and the pitman stops before the frame, the bearings or the shaft take the load. That only works if the toggle is cast to the right dimensions and the right material — a toggle that is too strong protects nothing. PangLei casts toggle plates to suit most makes and models of jaw crusher, to the original geometry.
Technical Features
- Cast to the original dimensions from pattern or sample
- Material selected to reproduce the designed failure behaviour
- Bearing faces machined where the original is machined
- Dimensional inspection report issued
What You Get That You Would Not Get Elsewhere
Cast to the original geometry so the intended break load is preserved
Protects the frame, pitman and bearings from tramp metal events
Supplied with the die and cheek plate package
Available for machines no longer supported by their builder
The Failures This Part Is Cast To Prevent
- Over-strong replacement toggles that transfer tramp loads into the frame
- Toggles unavailable for older machines, leaving the crusher unprotected
- Spare toggles not held, so a cheap break becomes a long shutdown
- Toggle seat wear going unnoticed until the plate jumps
Who It Is For
- Every jaw crusher operator
- Recycling contractors with tramp metal in the feed
- Mobile plant fleets far from a parts counter
- Rebuild workshops
Application Scenarios
- Primary crushing where tramp steel can enter
- Concrete recycling with rebar
- Demolition waste processing
- Spares holding for mobile fleets
Technical Data For Jaw Crusher Toggle Plate
Every figure here comes from our published foundry capability. Where a value depends on your machine it is confirmed at quotation rather than guessed.
| Specification | Detail |
|---|---|
| Part type | Toggle plate |
| Function | Designed failure point on tramp metal entry |
| Source geometry | Original pattern, customer sample or 3D scan |
| Machining | Bearing faces machined as original |
| Inspection | Dimensional inspection report |
| Models | Most makes and models of jaw crusher |
| Supplied with | Jaw die and cheek plate packages |
| Packing | Steel pallet |
Manganese Grades Available For This Part
| Material | Mn % | C % | Si % | P % | S % | Cr % |
|---|---|---|---|---|---|---|
| Mn13 | 11-14 | 1.00-1.45 | 0.3-1.0 | < 0.06 | < 0.04 | — |
| Mn13Cr2 | 11-14 | 1.15-1.25 | 0.3-0.8 | < 0.06 | < 0.04 | 1.5-2.5 |
| Mn18 | 17-19 | 1.2-1.3 | 0.3-0.8 | < 0.06 | < 0.04 | — |
| Mn18Cr2 | 17-19 | 1.2-1.3 | 0.4-0.9 | < 0.06 | < 0.04 | 1.5-2.5 |
| Mn20Cr3 | 19-21 | 1.2-1.3 | 0.3-0.8 | < 0.06 | < 0.04 | 2.5-3 |
| Mn22Cr2 | 21-23 | 1.1-1.4 | 0.3-0.8 | < 0.06 | < 0.04 | 1.5-2.5 |
| Mn22Cr3 | 21-23 | 1.1-1.4 | 0.3-0.8 | < 0.06 | < 0.04 | 2.5-3 |
How This Casting Is Made
Pattern Making
Once drawings are confirmed, pattern making starts immediately in our own pattern shop. Thousands of finished patterns are already on the shelf, so repeat parts skip this step entirely.
Sandbox Making
Casting Process Simulation System (CPSS) is run before the moulds are made. The cavity is kept as solid and as clean as possible so that inclusions have nowhere to start.
Melting And Pouring
Charge materials are bought to a high standard and temperature is controlled through the whole pour to achieve a fine grain structure. Samples are taken to verify the analysis and adjusted if needed, then kept for at least three years for traceability.
Sandbox Opening
Also called casting cleaning. After initial cooling the box is opened, risers and runners are removed and the casting is cleaned. Cooling time is set by casting size, not by the clock.
Heat Treatment
Heating temperature is strictly controlled and castings are spaced in the furnace so they heat uniformly and meet the water fully. Quenching begins within 30 seconds of withdrawal from the oven.
Machining
After rectifying and polishing, castings are machined strictly to drawing for correct fitment. QC then carries out dimensional inspection and issues the dimensional inspection report.
Inspection
Our own physical and chemical laboratory covers spectrometry, hardness, microstructure, dye penetrant and dimensional inspection on site rather than at a third party.
Packing And Delivery
Finished parts are packed on steel pallets for forklift handling, to international standards for road, rail, sea and air transport.
Inspection Supplied With This Part
Chemical analysis and a dimensional inspection report are standard on every order. The remaining procedures are carried out in our own physical and chemical laboratory when specified at order stage.
| Procedure | When |
|---|---|
| Chemical Analysis | standard on every heat |
| Dimensional Inspection Report | standard on every order |
| Hardness Testing | if specified |
| Tensile Testing | if specified |
| Microstructure Analysis | if specified |
| Magnetic Particle Testing | if specified |
| Dye Penetrant Testing | if specified |
| Ultrasonic Testing | if specified |
Laboratory Equipment
- German-made OBLF direct-reading spectrometer
- Hardness testing equipment
- Metallurgical microscope
- Dye penetrant inspection equipment
- Dimensional inspection equipment
How This Part Compares With The Alternatives
| Compared With | What Changes |
|---|---|
| A heavier aftermarket toggle | A toggle that does not break at the designed load shifts the damage to the frame and the bearings. We cast to the original geometry deliberately. |
| Welding a broken toggle | A repaired toggle has an unknown break load, which defeats its only purpose. |
| Not holding a spare | The toggle is the cheapest part of the crusher and the one most likely to stop it. Hold at least one. |
If Your Part Is Not Standard
With our own pattern shop, a 3D scanner and Casting Process Simulation System, we work from your drawing, your worn sample, or a scan taken on your site. Material grade, profile and machining are all specified against your machine rather than against a catalogue.
- Reverse engineering from a worn part, with no drawing required
- On-site 3D scanning where the component cannot be removed
- Material grade selected against your feed rather than a default
- Pattern retained afterwards, so repeat orders skip pattern making
Fitting And Getting The Life Out Of It
- Always hold at least one spare toggle on site
- Inspect the toggle seats when replacing the plate
- Check the tension spring and rod condition at the same time
- Never substitute a heavier toggle to stop repeat breakages — find the tramp metal source
- Re-set the closed side setting after fitting
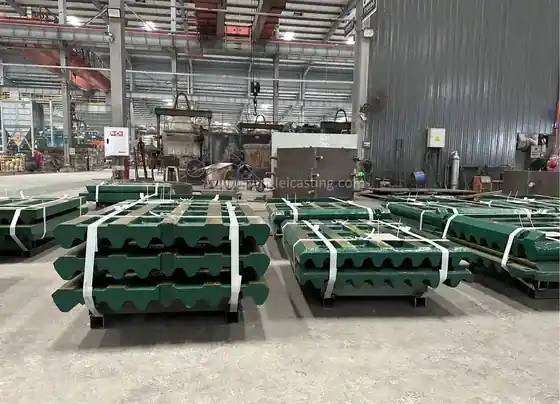
Jaw Crusher Toggle Plate At The Foundry
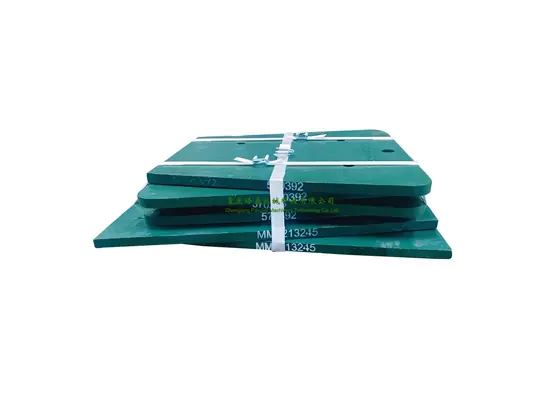
Parts Usually Ordered Alongside This One
Fixed Jaw Plate
Stationary jaw dies in high manganese, from 600 × 400 machines up to a C200
View Part →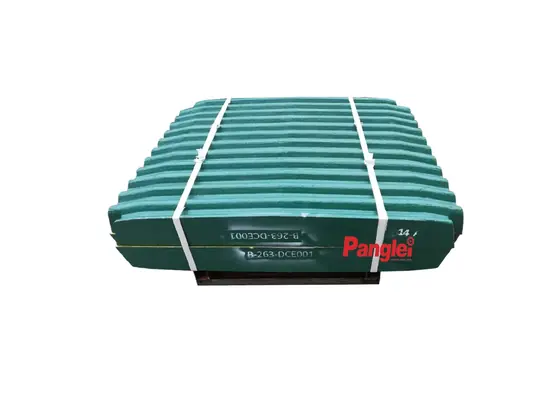
Swing Jaw Plate
Movable jaw dies cast to the same profile and heat as the fixed half
View Part →
Jaw Crusher Cheek Plate
Side liners that keep the crushing chamber square and protect the frame
View Part →
Jaw Crusher Shim Plate
Machined plate for setting the closed side setting, supplied in defined thicknesses
View Part →Jaw Crusher Toggle Plate Questions
Why not supply a stronger toggle?
Because the toggle is the machine's mechanical fuse. Making it stronger moves the next failure into the frame or the bearings, which cost far more than a toggle.
Do you supply toggle seats as well?
Tell us what you need with the enquiry — we cast a wide range of jaw spares to suit most makes and models.
Can you cast a toggle for a discontinued machine?
Yes, from the broken part or a drawing, through our pattern shop.
How many spares should I hold?
At least one per machine, and more where tramp metal is common in the feed.
Get A Price For Jaw Crusher Toggle Plate
Send the machine model, the part number if you have one, and the quantity. If you have neither, a photograph with the main dimensions is enough to start.