Stress Control and Insulation Tubes
C102-10 Stress Control Heat Shrink Tube up to 24 kV
High permittivity black tubing that redistributes the electrical field at the screen cut back on 6 to 24 kV cable
- Operating temperature: -55 to 105°C
- Minimum fully recovery temperature: 125°C
- Single or Dual wall(adhesive-lined) optional
- Shrink ratio: 2.5:1
- Standard Color: Black
- Equivalent to TE JSCR
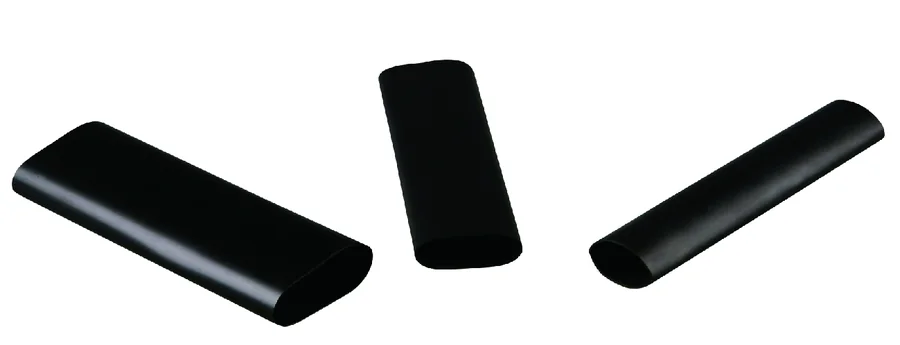
C102-10 · Stress Control and Insulation Tubes
Product Overview
What C102-10 Does
Stress control heat shrink tube.Electrical stress control protection of power cable termination and joint Products in 10kV(C102-10) and 35kV(C102-35) ratings are offered
High permittivity black tubing that redistributes the electrical field at the screen cut back on 6 to 24 kV cable It is manufactured by Dalian United Polymer Material Co., Ltd. in Dalian China where radiation cross linking extrusion and molding are all performed in house under one quality system.
Key Benefits
- Consistent field control that does not depend on jointer skill
- A short compact termination that fits inside crowded cable boxes and RMU compartments
- Volume resistivity of 1.0×10¹¹ Ω·cm or higher so the layer controls the field without becoming a leakage path
- Loss factor at 50 Hz held to 1.0 or below at 1000 V so heating stays low in service
- Available single wall or adhesive lined for sealed applications
Who It Is For
Who Benefits Most from C102-10
The buyers and site teams this product was designed around
MV Accessory Kit Manufacturers
The stress control layer is the single most critical component in any MV termination and is bought in bulk by kit assemblers.
Utility Jointing Teams
Crews building non standard terminations where a kit is unavailable and the stress control tube must be sourced separately.
Switchgear OEMs
Manufacturers terminating MV cable inside factory built assemblies who need a controlled and repeatable stress relief method.
Test Laboratories and Training Centres
Facilities preparing sample terminations for type testing or jointer certification.
Problems It Solves
Problems This Product Removes
Every one of these is a failure mode we have seen on real networks
The Screen Cut Back Is Where Terminations Fail
Cutting the metallic screen concentrates the electric field at a single sharp edge. Without stress control that concentration starts partial discharge and slowly erodes the insulation until breakdown.
Stress Cones Are Bulky and Position Sensitive
A geometric stress cone needs space and precise placement. A high permittivity tube achieves the same field redistribution in a fraction of the length.
Mastic Based Stress Control Is Messy and Inconsistent
Hand applied stress control mastic depends on the jointer building an even profile. An extruded tube gives the same result every time.
Partial Discharge Limits Are Tightening
Utilities now specify 10 pC. A stress control layer with a dielectric constant of 10 to 25 keeps discharge inside that limit at both ambient and operating temperature.
Application Scenarios
Where It Is Used
Termination Screen Cut Back
Overlapping the metallic screen and the core insulation to smooth the field discontinuity.
Joint Screen Interruption
Restoring field control either side of a joint where the screen has been cut.
Elbow and Connector Interfaces
Where a separable connector meets a cable and the field must be graded.
Rebuilt and Repaired Terminations
Restoring stress control on a termination that has been cut back and remade.
Type Test Sample Preparation
Building repeatable samples for laboratory qualification.
Technical Data
Specifications and Dimensions
Test methods and requirements taken directly from the manufacturing specification
Technical Data
| Property | Test Method | Requirement |
|---|---|---|
| Tensile Strength | ASTM D2671 | ≥12 MPa |
| Ultimate Elongation | ASTM D2671 | ≥300% |
| Heat Aging (136°C/168h) Tensile Strength Ultimate Elongation | ASTM D2671 | ≥10 MPa ≥250% |
| Water absorption (23°C/24h) | ASTM D2671 | ≤1.0% |
| Low-temperature flexibility (-40°C/4h) | ASTM D2671 | No cracking |
| Heat shock (200°C/4h) | ASTM D2671 | No splitting |
| Volume resistivity | ASTM D2671 | ≥1.0×10¹¹ Ω·cm |
| Dielectric constant | IEC 62631-2-1 | 10 to 25 |
| Loss factor(50Hz) | IEC 62631-2-1 | ≤ 1.0 (1000V) |
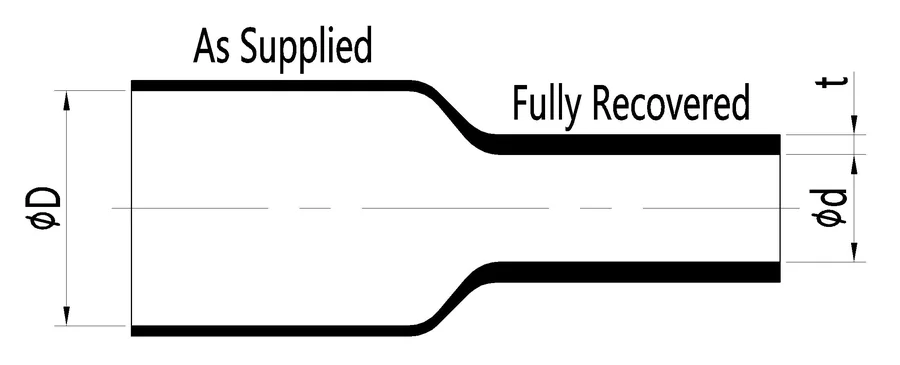
Dimensions
| Size C102-10 | As supplied(mm) Inner diameter D (min.) | After recovered (mm) Inner diameter d (max.) | Wall thickness t (nom.) | Standard length (m/pcs) |
|---|---|---|---|---|
| 26/10 | 26 | 10 | 2.6 | Spool or ≤1.5 |
| 30/12 | 30 | 12 | 2.7 | Spool or ≤1.5 |
| 35/14 | 35 | 14 | 2.8 | Spool or ≤1.5 |
| 40/16 | 40 | 16 | 3 | Spool or ≤1.5 |
| 47/18 | 47 | 18 | 3 | Spool or ≤1.5 |
| 55/21 | 55 | 21 | 3 | ≤1.5 |
| 65/24 | 65 | 24 | 3 | ≤1.5 |
| 85/30 | 85 | 30 | 3.2 | ≤1.5 |
| 95/45 | 95 | 45 | 3 | ≤1.5 |
CROSS REFERENCE · Tyco-Raychem: JSCR
Manufacturing and Quality
How It Is Made and Checked
Compounding extrusion radiation cross linking expansion and test all under one roof in Dalian
-
01
Compounding
Base polyolefin antioxidants flame retardants and functional fillers are mixed to a recipe held under our own formulation control rather than bought as a masterbatch.
-
02
Extrusion
The compound is extruded to the required wall and diameter. Co extruded products form two or three layers in a single pass so no interface can trap air.
-
03
Radiation Cross Linking
Electron beam irradiation creates the cross linked network that gives the material its shape memory. This step is what makes the product heat shrinkable.
-
04
Expansion
The cross linked part is heated expanded to its supplied diameter and cooled under tension so the expanded shape is locked in until heat is applied again.
-
05
Test and Inspection
More than 90 percent of product performance tests are carried out in our own laboratory including tensile elongation heat aging dielectric strength and tracking resistance.
-
06
Packing and Traceability
Each batch carries a production record so a delivered part can be traced back to its compound lot and process parameters.
Certification
ISO 9001:2015
Quality management system
IATF 16949:2016
Automotive quality management
ISO 14001:2015
Environmental management
ISO 45001:2018
Occupational health and safety
GJB 9001C-2017
Defence quality management
UL 224 E341796
Extruded insulating tubing
CE / RoHS
European conformity and restricted substances
CCS / ABS / DNV
Marine classification society approvals
Comparison
How C102-10 Compares
An honest comparison so you can rule this product in or out quickly
| Stress Control Method | Consistency | Space Needed | Skill Dependence |
|---|---|---|---|
| C102-10 stress control tube | High and repeatable | Short | Low |
| Geometric stress cone | High | Long | Medium |
| Stress control mastic | Variable | Short | High |
| No stress control | Fails early | None | Not acceptable |
Use Guide
How to Select and Install C102-10
The sequence our engineers walk customers through on every first installation
-
01
Cut the Screen Cleanly
The screen edge must be square and free of burrs. A ragged edge defeats the purpose of the stress control layer.
-
02
Set the Overlap
The tube must overlap the metallic screen and the core insulation by the distance in the kit drawing typically 20 to 30 mm on each side.
-
03
Clean the Insulation Surface
Remove all semiconductive residue. Wipe in one direction away from the screen so contamination is not dragged back.
-
04
Position Before Heating
Slide the tube into position and check the overlap on both sides before any heat is applied.
-
05
Shrink from the Screen Outward
Start over the metallic screen and work toward the conductor so trapped air is driven away from the critical interface.
-
06
Apply Insulation over It
The stress control layer is never the outer surface. Cover it with C101 non tracking tube or the insulating layers supplied in the kit.
FAQ
C102-10 Frequently Asked Questions
The questions buyers ask before they place an order
Why is the tube black
What is the difference between C102-10 and C102-35
Can I use stress control tube on its own
How much overlap onto the screen is needed
Is it a direct substitute for Raychem JSCR
Do you supply it on spools
Still need an answer ask our engineers on WhatsApp
Related
Related Products
C102-35 Stress Control
The 36 kV stress control layer with a dielectric constant of 25 to 50 for 26/35 kV terminations and joints
VIEW DETAILS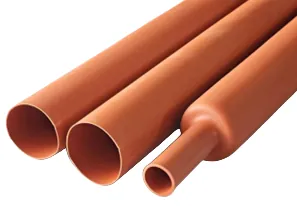
C101 Non Tracking Tube
Red anti tracking outer insulation for indoor and outdoor terminations and joints from 6 kV to 36 kV
VIEW DETAILS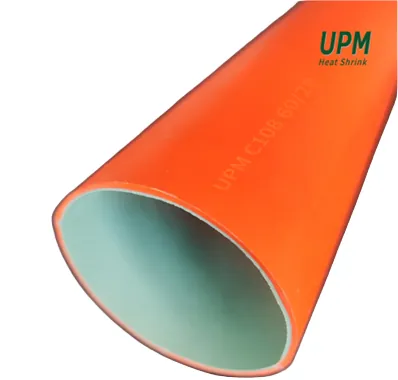
C108 Composite Tube
A single tube that carries both anti tracking insulation and a zinc oxide stress control sealant for terminations up to 24 kV
VIEW DETAILS
MV Kits 8.7/15 kV
Indoor outdoor and joint kits for 8.7/15 (17.5) kV single core and three core cable tested to IEC 60502-4
VIEW DETAILSGet a Quotation for C102-10
Send us the voltage class conductor size and quantity and we will return a part number a price and a lead time. No form to fill in.