- Home
- Products
- Device Assembly Systems
- Combination Device Assembly
DK-04 · Device Assembly Systems
Combination Device Assembly
Multi station systems that bring several assembly processes into one controlled cycle
Overview
What This Machine Does
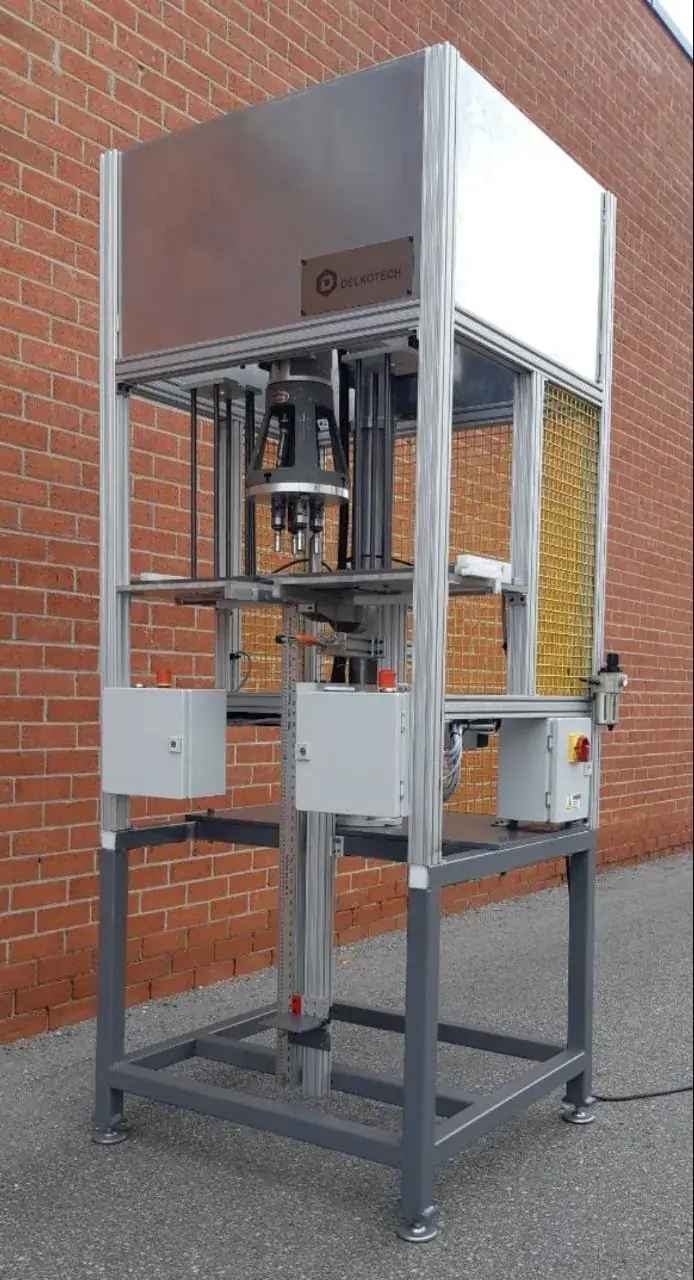
Some products need several unrelated processes before they are finished: a component pressed in, a seal applied, a fastener driven, a function checked. Run as separate operations they create queues, handling and four chances to mislocate the same part.
A combination assembly system brings those processes into one machine with one part location. The part is placed once, and each station works from the same datum while the controller keeps track of what has been done to it.
Delkotech builds these systems around the actual process sequence, with the station order, the cycle and the buffering sized to the rate you need rather than to a standard platform.
From the original specification: Combination device assembly is listed among Delkotech's services.
Key Benefits
What It Changes on Your Floor
One location, several processes
Locating once and processing several times removes the error that each re-fixture introduces.
No queues between operations
Work in progress between stations disappears, and with it the floor space and handling it consumed.
Cycle balanced as a whole
Station times are balanced against each other, rather than each operation optimising in isolation.
Single record per part
The part accumulates one record across all processes instead of four disconnected ones.
Smaller footprint
One machine replaces a line of benches and the space between them.
Application Scenarios
Where It Is Used
Press, seal and fasten sequences
Combining mechanical assembly steps that are normally done at separate benches.
Assembly with in line checking
Adding verification between processes so a fault is caught before more value is added.
Mixed process sub-assembly
Bringing together operations that use different technologies in one cycle.
Sub-assembly feeding a main line
Producing a completed sub-assembly at the rate the main line consumes it.
Who It Is For
Plants That Ask for This Machine
- Manufacturers with a sub-assembly spread across several benches
- Plants losing accuracy to repeated re-fixturing
- Producers who need one record covering several processes
- Operations short of floor space for a line of separate stations
Problems It Solves
Re-fixturing error
Every transfer between operations re-establishes the datum, and every re-establishment adds error.
Work in progress
Queues between benches hide problems and occupy floor space.
Disconnected records
Four operations producing four records makes a later question hard to answer.
Unbalanced operations
Separately optimised benches rarely balance, so one of them is always the constraint.
Technical Features
How It Is Built
Multi station layout
Stations arranged in process order with buffering sized to the cycle.
Single part location
The part is located once and every station references that datum.
In line verification
Checks between processes so value is not added to a part that has already failed.
Unified part record
One record per part covering every process in the machine.
Balanced cycle
Station times balanced so the machine rate is not set by one slow operation.
Written sequence of operation
Behaviour documented before coding, including what happens when a station fails.
Specifications
Specification Sheet
Delkotech builds to order, so dimensional and performance values are set against your part at design review, then measured and recorded before shipment. Values not yet fixed for your project are marked TBC rather than guessed.
| System type | Multi station combination assembly system |
|---|---|
| Station count | Set to the process sequence, specified per order |
| Part location | Single datum carried through all stations |
| Verification | In line checking between processes as specified |
| Cycle time | TBC - confirmed at design review |
| Throughput | TBC - confirmed at design review |
| Footprint | TBC - confirmed at design review |
| Part size range | TBC - confirmed at design review |
| Transfer | Indexing or continuous, selected at concept stage |
| Control platform | PLC with HMI, structured by station |
| Data output | One record per part, available to plant systems |
| Guarding | Fixed and interlocked guarding designed at layout |
| Electrical supply | TBC - confirmed at design review |
| Compressed air | TBC - confirmed at design review |
| Built at | Delkotech facility, Vaughan, Ontario, Canada |
| Structure | Welded steel base frame with machined station mounting surfaces |
|---|---|
| Pallets and nests | Machined pallets carrying part specific locating elements |
| Handles | Sub-assemblies and their components as specified |
| Contact surfaces | Non marking materials where the part carries a finish |
Manufacturing Process
From Enquiry to Commissioned Machine
Process sequence study
Every current operation is walked through, timed and questioned before it is designed into a machine.
Layout and balance
Station order and cycle balance agreed with a target rate.
Design
Stations, transfer, controls and safety designed together.
Build and integration
Manufactured and integrated at the Vaughan facility.
Rate and capability proving
Run to rate with your parts, with each station's result measured.
Installation and training
Installed and handed over with training and documentation.
Quality Control
What Is Checked Before It Ships
- Each station verified individually before the machine is run as a whole
- Pallet and nest locations measured against the part drawing
- Station to station datum consistency confirmed
- Full cycle run to rate with customer parts
- Safety functions and fault recovery verified and recorded
Certifications
Compliance Position
Built to be validated to current regulatory standards with documentation supporting validation. Project specific certificates are TBC until contract stage.
Customization Options
- Station count and process mix set to your sequence
- Indexing or continuous transfer
- Manual, semi-automatic or fully automatic loading
- Spare station position for a process you expect to add
- Data output to your plant systems
- Pallet design covering a part family
Comparison
Compared With the Alternatives
| Separate benches | Flexible and cheap to change, but slower, larger and less accurate once the sequence is settled. |
|---|---|
| A line of standalone machines | Each machine is simpler, but you carry the transfers, the queues and the integration between them. |
| A single robot cell serving several processes | Flexible for varied geometry. A combination machine is usually faster when the sequence is fixed and the rate matters. |
Use Guide
Running It Well
Load onto the pallet correctly
The whole machine references the pallet datum. A part seated incorrectly affects every station after it.
Do not run with a station disabled
Disabling a station produces parts missing an operation with no record saying so.
Check pallets on a schedule
Pallets take the wear. A pallet inspection routine catches location drift before it becomes scrap.
Use the fault recovery procedure
The documented recovery sequence exists so a part part-way through the process is handled consistently.
Questions
Combination Device Assembly Questions
How many processes can one machine combine?
There is no fixed limit. The practical constraint is cycle balance and access for maintenance, which we work through at layout stage against your target rate.
What happens if one station fails mid cycle?
The fault handling is defined in the sequence of operation, including what happens to the part in process. That behaviour is agreed with you rather than left to the code.
Can we add a process later?
Yes, if we plan for it. Ask for a spare station position at concept stage. Adding one to a fully packed machine later is significantly more expensive.
Does it produce one record per part?
Yes. The part accumulates a single record across all stations, which is far more useful than separate records per operation.
How is the rate confirmed?
The machine is run to rate with your parts before shipment, with station times measured individually so you can see where the cycle actually sits.
What do you need to quote?
The current operation sequence, part drawings, samples, your target rate and the floor space available.
Related
Related Equipment
Device Assembly Systems
Safety Device Assembly Systems
Assembly and test systems for devices where every unit must be proved before it ships
View equipment
Device Assembly Systems
Diagnostic Device Automation
Automated assembly and inspection for diagnostic devices with a record for every unit
View equipmentSheet Metal Automation
Place Processing Automation Machines
Stations that position the part and perform the operation in one controlled cycle
View equipmentRelated
Related Articles
Talk to an engineer
Get a Quotation for This Machine
Send the part drawing, the operation and the rate you need. You will get a concept and a defined scope, not a brochure.