- Home
- Products
- CNC Assembly Machines
- CNC Guard Rail Assembly Machines
DK-02 · CNC Assembly Machines
CNC Guard Rail Assembly Machines
Index and fasten long rail assemblies to a programmed pattern instead of by hand marking
Overview
What This Machine Does
Guard rail, railing and balustrade assemblies are long, repetitive and unforgiving. Every post, bracket and fastener has a position, and hand marking a long rail means clamping, measuring, re-clamping and accepting whatever drift comes with it.
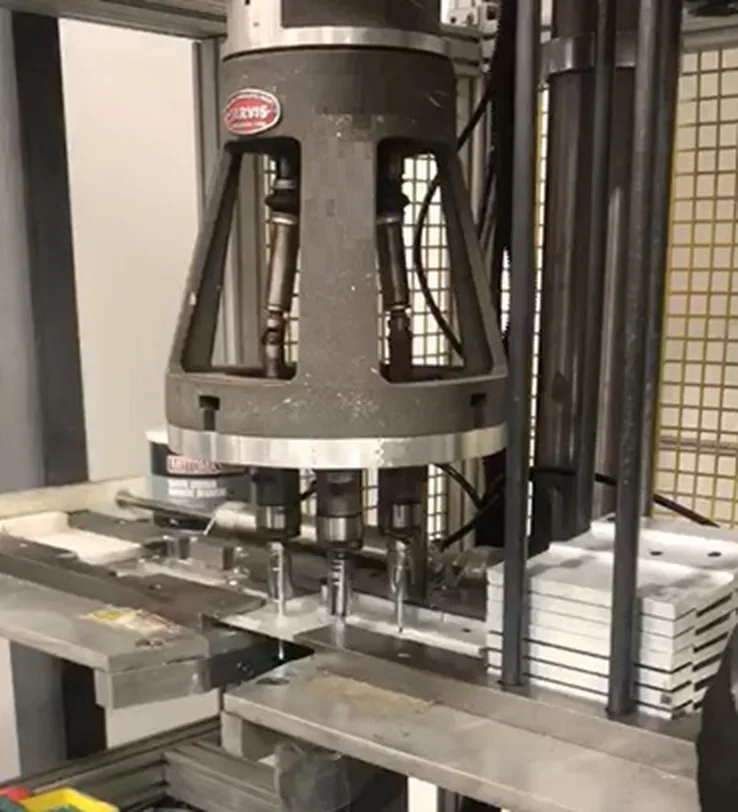
A CNC guard rail assembly machine holds the profile on a single datum, indexes it under the head, and performs the drilling, fastening or insertion at each programmed position. The pattern comes from a program, so the hundredth rail matches the first.
Delkotech builds these machines for the rail sections the customer actually produces, including the awkward end conditions that a general purpose machine would need a manual operation to cover.
From the original specification: CNC guard rail assembly machines are listed among Delkotech's services and appear as a delivered project.
Key Benefits
What It Changes on Your Floor
One datum for the whole rail
The profile is located once. Every subsequent position references that datum instead of the previous mark.
Pattern from a program
Changing the post spacing is a program selection, not a new marking jig.
Consistent hole and fastener positions
Field assembly stops being a fitting exercise, because the parts actually line up.
Faster through the batch
The indexing and fastening happen at machine speed while the operator prepares the next rail.
Inspection that means something
Because the pattern is programmed, a check on the first and last of the batch tells you about the whole batch.
Application Scenarios
Where It Is Used
Guard rail and barrier assembly
Fastening posts, brackets and rails to a repeating pattern.
Architectural railing and balustrade
Producing matched rail sets where visible alignment matters.
Structural rail sub-assembly
Preparing long profiles with a fastener pattern before they go to site.
Extruded profile fabrication
Drilling, tapping and fastening aluminium extrusions in repeating positions.
Who It Is For
Plants That Ask for This Machine
- Railing and guard rail fabricators producing repeat sections
- Aluminium extrusion fabricators adding assembly operations in house
- Manufacturers whose field crews are losing time to holes that do not line up
- Producers moving from job shop marking to programmed batch production
Problems It Solves
Accumulated marking error
Measuring from the last mark instead of from a datum stacks error along a long rail. The machine indexes from the datum every time.
Re-clamping a long profile
Each re-clamp is a chance to shift the reference. One clamping and a programmed index removes them.
Field rework
Holes that do not line up on site are the most expensive way to discover a fabrication problem.
Setup time between patterns
A physical jig per pattern is storage, handling and setup. A program is a selection at the HMI.
Technical Features
How It Is Built
Long profile support and indexing
Support and drive arrangement sized to the rail length so the profile is controlled along its whole span.
Programmed fastener positions
Positions stored as part programs and selected at the HMI.
Multi operation head
Drilling, tapping, fastening or insertion as the assembly requires.
Datum clamping
Clamping designed so the reference face is held without distorting the profile.
Part program management
Recipes stored per product so changeover is an operator selection.
Guarded working zone
Access and guarding laid out for loading long profiles safely.
Specifications
Specification Sheet
Delkotech builds to order, so dimensional and performance values are set against your part at design review, then measured and recorded before shipment. Values not yet fixed for your project are marked TBC rather than guessed.
| Machine type | CNC controlled rail and profile assembly machine |
|---|---|
| Workpiece | Long profiles, rails and extrusions |
| Positioning | Programmed indexing from a single datum |
| Maximum profile length | TBC - confirmed at design review |
| Profile section range | TBC - confirmed at design review |
| Positional accuracy | TBC - confirmed at design review |
| Cycle time per position | TBC - confirmed at design review |
| Operations | Drilling, tapping, fastening or insertion, specified per application |
| Control platform | PLC and CNC control with HMI recipe selection |
| Recipe storage | Part programs stored and selected by the operator |
| Guarding | Fixed and interlocked guarding around the working zone |
| Electrical supply | TBC - confirmed at design review |
| Compressed air | TBC - confirmed at design review |
| Built at | Delkotech facility, Vaughan, Ontario, Canada |
| Handles | Steel and aluminium rail sections, extrusions and formed profiles |
|---|---|
| Structure | Welded steel bed with machined mounting and support surfaces |
| Contact surfaces | Non marking supports where the profile carries a finish |
| Tooling | Hardened tool steel drilling and fastening tooling |
Manufacturing Process
From Enquiry to Commissioned Machine
Product range review
The rail sections, lengths and fastener patterns you actually produce are recorded, including the end conditions.
Datum and clamping concept
The locating scheme is agreed before detail design.
Design
Mechanical, control and safety design carried out together.
Build
Manufactured and assembled at the Vaughan facility.
Programming and try out
Part programs created for your patterns and proved on your profiles.
Installation and training
Installed and handed over with operator training on recipe selection.
Quality Control
What Is Checked Before It Ships
- Indexing accuracy measured over the full profile length and recorded
- Sample rails produced and fastener positions measured against the program
- Repeatability confirmed across a continuous batch
- Recipe recall verified for every stored pattern
- Safety functions verified before shipment
Certifications
Compliance Position
Equipment is designed to be validated to current regulatory standards. Project specific certificates are TBC until contract stage. Delkotech does not certify the finished rail assembly against a barrier standard - that remains the responsibility of the product manufacturer.
Customization Options
- Maximum profile length set to your production
- Tooling for your fastener type and size
- Single or multi head arrangement
- Automatic or assisted profile loading
- Recipe structure matched to your product coding
- Integration with upstream cutting equipment
Comparison
Compared With the Alternatives
| Marking jig and hand drill | Cheap and flexible, but the error accumulates along the rail and setup time returns with every pattern change. |
|---|---|
| General purpose CNC machining centre | Accurate, but the table rarely suits a long profile and the machine is over specified for drilling a hole pattern. |
| Outsourcing the drilling | Removes the capital cost and adds a transport loop, a queue and a supplier to chase when the pattern changes. |
Use Guide
Running It Well
Load against the datum stop
The whole program references the datum. A profile pushed short is the most common cause of a shifted pattern.
Check the first rail of each batch
One measured rail at the start confirms the right recipe is loaded before you make fifty.
Support long sections
Unsupported overhang bends under its own weight and moves the working position.
Keep recipes named by product
A recipe list that matches your product codes prevents the wrong pattern being selected.
Photographs
The Machine in the Shop
Photographs of Delkotech built equipment. No stock imagery is used on this site.
Questions
CNC Guard Rail Assembly Machines Questions
What is the longest rail the machine can handle?
Maximum length is set by the bed and support arrangement, which we size to your production. Tell us the longest section you make and we design to it rather than asking you to work within a standard.
Can it handle more than one fastener pattern?
Yes. Patterns are stored as part programs and selected by the operator at the HMI, so a pattern change is a selection rather than a jig change.
What accuracy can we expect?
Positional accuracy is agreed during design review against your assembly tolerance and then measured and recorded before shipment. We do not publish a figure that is not tied to a specific build.
Does it work with aluminium extrusion?
Yes. Clamping and support are chosen so an extrusion is held without distorting the section, and contact surfaces can be specified non marking for finished profiles.
Can it load rails automatically?
Assisted or automatic loading can be included. Whether it is worth the cost depends on your batch sizes, which we go through at concept stage.
How long does a pattern change take?
For a stored recipe it is an HMI selection and a datum check. If the section itself changes, changeover also includes any tooling or support adjustment, which is quantified at design review.
Related
Related Equipment
CNC Assembly Machines
Multi Spindle Screw Machines
Drive every fastener in a pattern in one stroke with torque controlled at each spindle
View equipment
CNC Assembly Machines
CNC Custom Automation Equipment
Purpose built CNC machines designed around your part when no catalogue machine fits
View equipment
CNC Assembly Machines
CNC Silicon Window Machines
Programmed sealant and glazing machines for window and glass panel production
View equipmentRelated
Related Projects
Project
CNC Guard Rail Assembly Machine
Programmed fastener patterns on long rail sections from a single datum
Read the projectProject
CNC Riveting Railing Machine
Programmed riveting positions on railing assemblies with consistent set force
Read the projectProject
Multi Spindle Post Screws Railing Machine
Driving the full fastener pattern on railing posts in one controlled stroke
Read the projectRelated
Related Articles
Buying Guide
Why a Sequence of Operation Comes Before the Code
The single document that determines whether a custom machine project goes well
Read the articleProcess Guide
Clinching Riveting and Spot Welding Compared
Choosing a sheet metal joining method when the panel is already finished
Read the articleTalk to an engineer
Get a Quotation for This Machine
Send the part drawing, the operation and the rate you need. You will get a concept and a defined scope, not a brochure.