- Home
- Products
- Sheet Metal Automation
- Automatic Sheet Metal Pick and Place Machine
DK-01 · Sheet Metal Automation
Automatic Sheet Metal Pick and Place Machine
Vacuum gantry de-stacker that feeds blanks to a laser or press without manual lifting
Overview
What This Machine Does
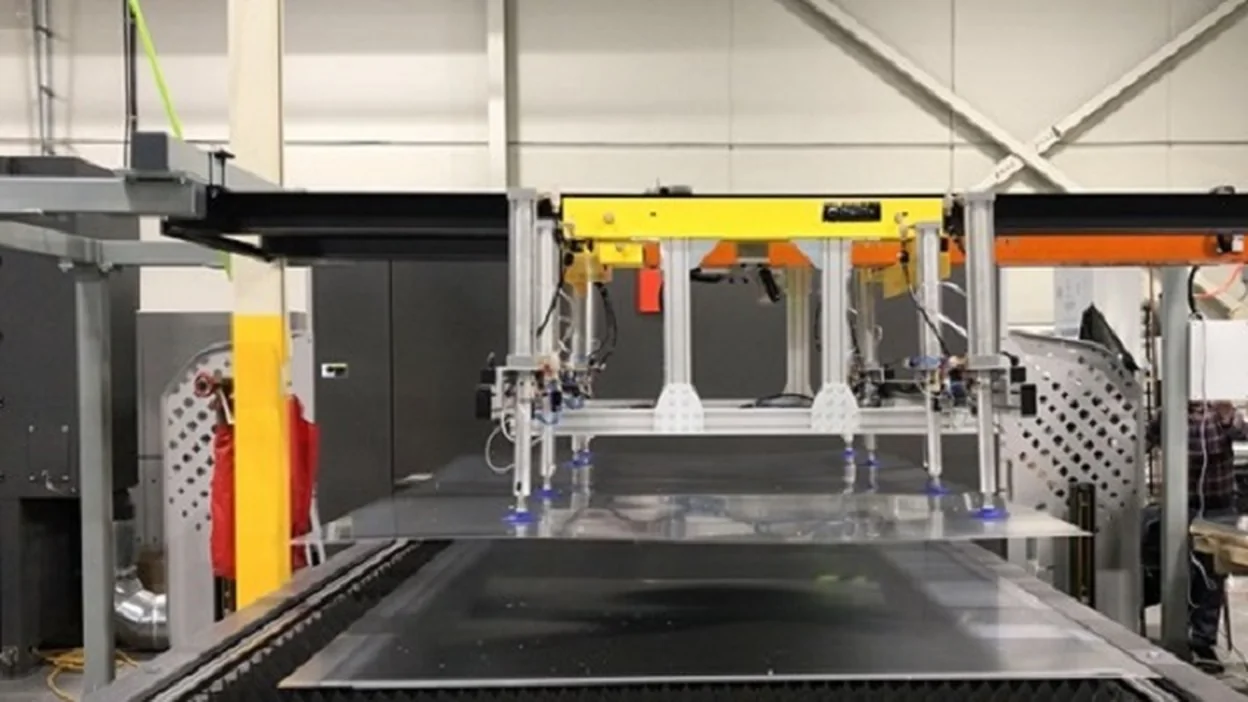
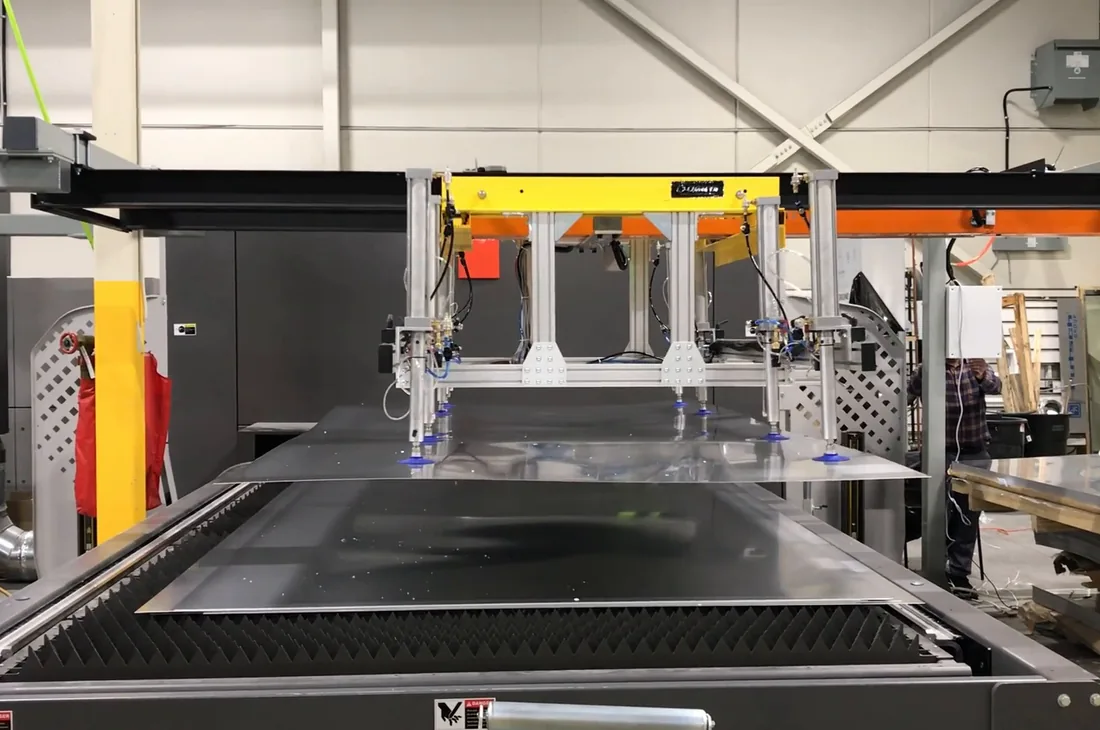
The Delkotech pick and place system is a vacuum gantry that lifts sheet metal blanks one at a time from a pallet and places them on the infeed of the next process, most often a laser cutting machine or a press.
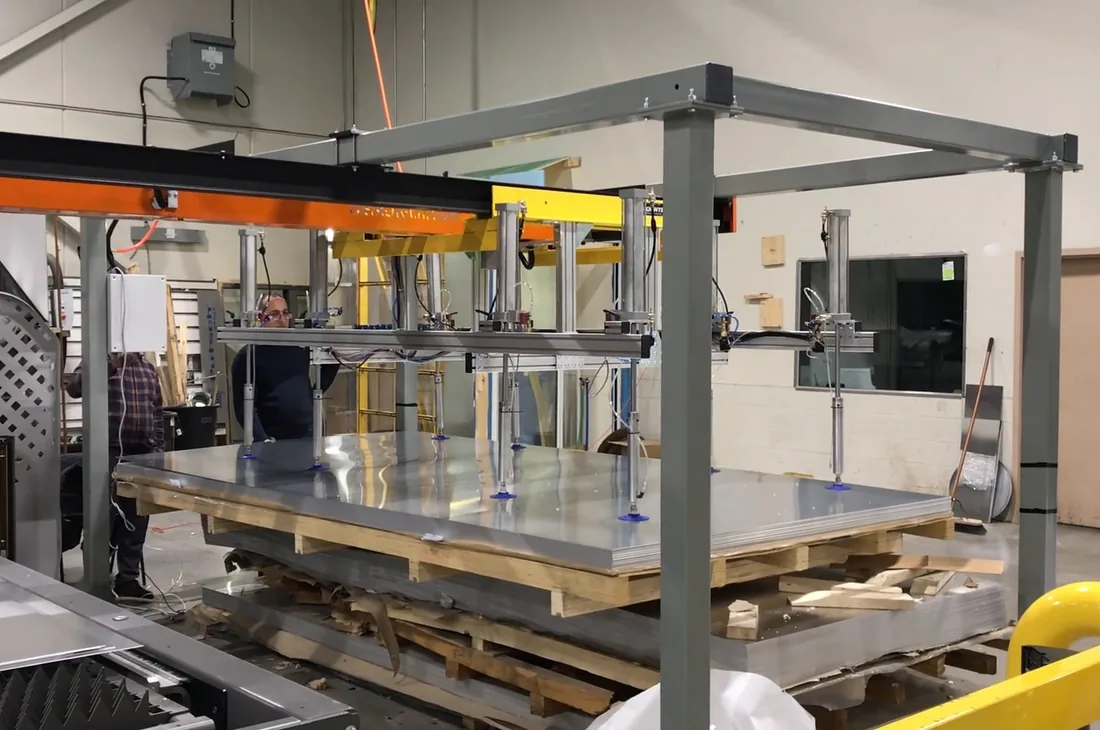
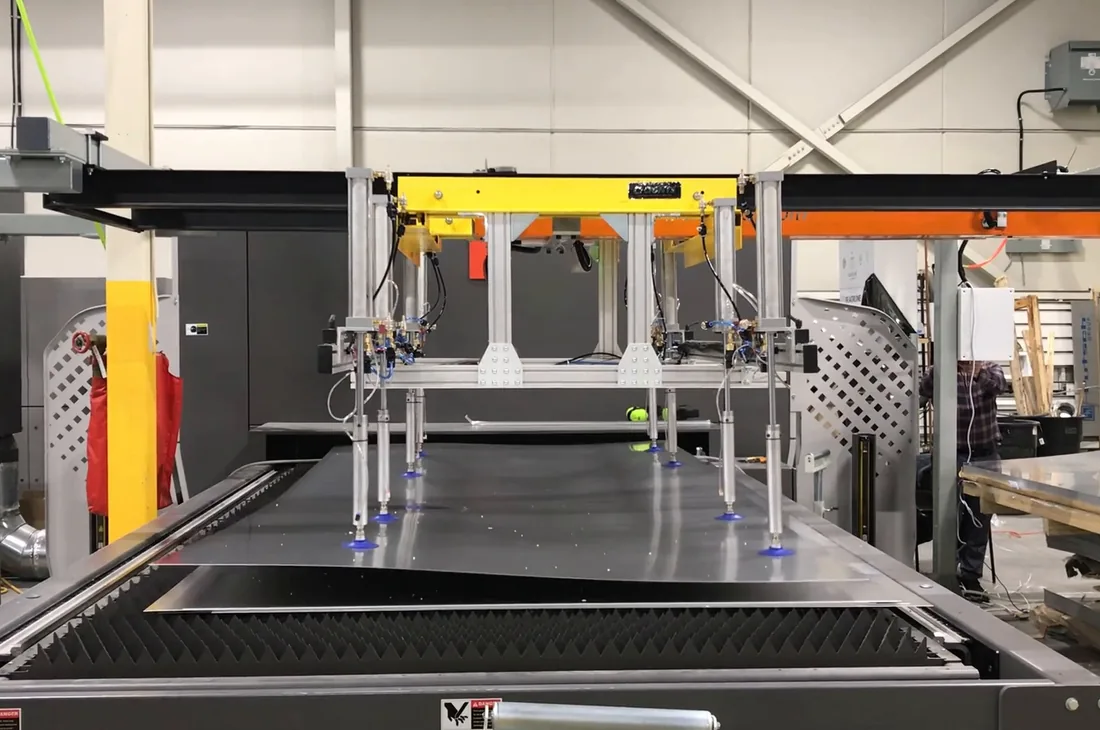
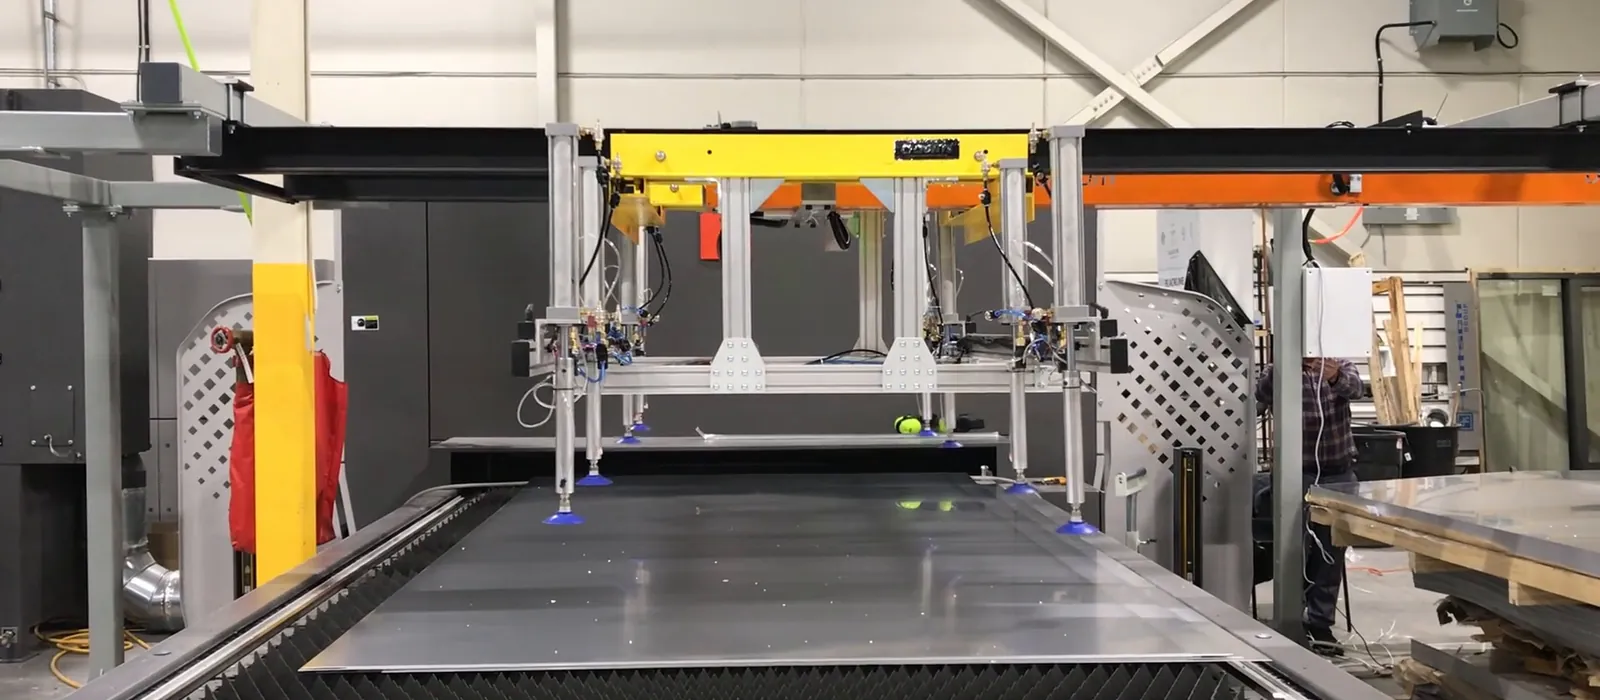
The gantry spans the loading station and the machine table. Suction cups mounted on a cross beam lower onto the top blank, lift it clear of the stack, traverse and release it in a repeatable position. The loading weight is specified for each order, so the frame, drives and cup layout are sized around the sheet you actually run rather than a catalogue maximum.
The photographs and video on this page are of a system built at the Delkotech facility in Vaughan, feeding aluminium blanks into a laser cutting machine.
From the original specification: Automatic Sheet Pick and Place System / De-Stacker is designed and developed. The loading weight is different according to order.
Key Benefits
What It Changes on Your Floor
Takes the lift out of the job
A large blank is awkward and heavy for two people and trivial for a vacuum gantry. The manual handling risk at the front of the line disappears.
One blank at a time
Separation at the stack is the point of a de-stacker. Double blanks that would crash a laser head are addressed at the pick, not discovered afterwards.
Repeatable placement
The blank lands in the same position every cycle, so the downstream program does not need a margin for how a person set it down.
Runs the shift
The cell keeps feeding through breaks and shift changes, which is usually where the manual line loses its rate.
Surface stays clean
Vacuum lifting from the face avoids the dragging and edge scuffing that comes with sliding a sheet across a table.
Application Scenarios
Where It Is Used
Laser cutting infeed
Blank loading onto a flat bed laser, with the gantry clearing the working envelope between cycles.
Press and brake feeding
Presenting blanks to a press line where the operator would otherwise be reaching into the die area.
Sheet to conveyor transfer
Moving sheets from a pallet onto a powered conveyor that feeds the next station.
Pallet to pallet re-stacking
Transferring sheets between pallets or between a pallet and a buffer table during a changeover.
Who It Is For
Plants That Ask for This Machine
- Sheet metal fabricators running flat bed lasers where the machine waits on loading
- Aluminium fabricators handling large format blanks that require two operators
- Automotive parts manufacturers with repetitive blank feeding between operations
- Plants that have a manual handling finding they need to close on the shop floor
Problems It Solves
The laser is faster than the loader
A fast cutting head that idles between sheets is expensive idle time. Automating the load recovers cycle the machine can already deliver.
Double blanks
Two sheets picked as one damages tooling or scraps the cut. A de-stacker addresses separation at the stack.
Manual handling injuries
Large blanks are the classic sheet metal back injury. Removing the lift removes the exposure.
Placement variation
Hand loading puts the blank down differently each time, which forces a tolerance margin into every downstream program.
Technical Features
How It Is Built
Vacuum cup cross beam
Cup count and spacing set for the blank size and mass specified on the order.
Gantry frame
Welded steel structure spanning the loading station and the target machine, with the working height set to the existing equipment.
Servo or pneumatic vertical axis
Vertical stroke sized to the stack height so the head clears a full pallet and an almost empty one.
Stack height tracking
The pick height follows the stack down so the approach stays consistent as the pallet empties.
Guarded working envelope
Fixed guarding and interlocked access around the traverse path, laid out so pallet changes do not require defeating a guard.
Interface to the downstream machine
Handshake signals so the gantry and the cutting or pressing machine agree on when it is safe to enter.
Specifications
Specification Sheet
Delkotech builds to order, so dimensional and performance values are set against your part at design review, then measured and recorded before shipment. Values not yet fixed for your project are marked TBC rather than guessed.
| Machine type | Vacuum gantry pick and place system with de-stacking function |
|---|---|
| Handling method | Vacuum cup array, top face pick |
| Loading weight | Specified per order - the source specification states loading weight differs according to order |
| Blank size range | TBC - confirmed at design review |
| Stack height | TBC - confirmed at design review |
| Cycle time | TBC - confirmed at design review |
| Traverse stroke | TBC - confirmed at design review |
| Vertical stroke | TBC - confirmed at design review |
| Drive type | Servo or pneumatic, selected against required cycle |
| Control platform | PLC with operator HMI, specified with the customer |
| Compressed air supply | TBC - confirmed at design review |
| Electrical supply | TBC - confirmed at design review |
| Guarding | Fixed guarding with interlocked access, designed at layout stage |
| Built at | Delkotech facility, Vaughan, Ontario, Canada |
| Frame | Welded and machined steel structure |
|---|---|
| Linear motion | Guided linear axes with covered rails on the traverse |
| Vacuum tooling | Bellows or flat vacuum cups selected for the sheet finish |
| Handles | Steel, aluminium and coated sheet, with cup type chosen so the finish is not marked |
Manufacturing Process
From Enquiry to Commissioned Machine
Application review
Blank size, mass, surface finish, stack height and target rate are recorded from your actual production, not from a nominal case.
Layout
The gantry is laid out against the real footprint of the loading station and the downstream machine, including pallet truck access.
Mechanical and control design
Frame, axes, tooling and control architecture are designed together, with the sequence of operation written before code.
Build and assembly
The system is built and assembled at the Vaughan facility.
Dry cycle and part proving
The cell is cycled empty, then with your blanks, then at rate.
Installation and commissioning
Installed against the existing machine, interfaced, and run with your operators.
Quality Control
What Is Checked Before It Ships
- Axis travel and repeatability checked before tooling is fitted
- Vacuum circuit leak checked and hold time measured with the heaviest specified blank
- Pick and place cycle run continuously to confirm placement repeats
- Safety functions and interlocks verified and recorded
- Rate run with customer supplied blanks before shipment
Certifications
Compliance Position
Delkotech builds equipment designed to operate in mass production and able to be validated to current regulatory standards. Specific third party marks and certificates for a given build are confirmed at contract stage and are listed as TBC until then.
Customization Options
- Loading weight and blank format sized to your order
- Cup layout adapted to perforated, formed or coated blanks
- Single or double station loading
- Integration to an existing laser, press or conveyor
- Stack separation arrangement for material that tends to stick
- Buffer table or scrap position added to the traverse
Comparison
Compared With the Alternatives
| Manual two person loading | No capital cost, but it sets the rate of the whole line, carries the handling risk and places the blank differently every time. |
|---|---|
| Articulated robot with vacuum tooling | Flexible for mixed geometry and orientation changes. A gantry is usually the better answer when the move is a straight transfer of large flat blanks, because the span and stiffness come cheaper. |
| Roll fed or coil line | Right when the part is cut from coil in one continuous process. A de-stacker is for plants that buy and store blanks. |
Use Guide
Running It Well
Present the stack squarely
The pick position assumes the pallet is placed against its locating stops. A skewed pallet is the most common cause of a missed pick.
Keep the cups clean
Oil and swarf on the cup face is the usual reason hold time falls off. Wipe the cups at shift start.
Watch the separation
If the material is oily and blanks begin to lift in pairs, the separation setting is the first adjustment, not the vacuum level.
Respect the guarding
The interlocked access is positioned for pallet changes. If a task requires a guard to be opened, the cycle should be stopped, not bypassed.
Photographs
The Machine in the Shop
Photographs of Delkotech built equipment. No stock imagery is used on this site.
Questions
Automatic Sheet Metal Pick and Place Machine Questions
How heavy a blank can the system lift?
Loading weight is specified per order. The original specification for this system states that the loading weight is different according to order, so the frame, drives and vacuum tooling are sized to the sheet you tell us you run. Send the blank size, thickness, material and finish and we will confirm the configuration.
Can it feed my existing laser cutting machine?
That is the usual application. The gantry is laid out against the existing machine and interfaced to it with a handshake, so the two agree on when it is safe to enter the working area. Tell us the machine make and table format when you enquire.
How does it avoid picking two sheets at once?
Separation is handled at the stack rather than detected afterwards. The arrangement depends on the material, because oily aluminium behaves differently from dry steel, so the method is chosen during application review.
What happens as the pallet empties?
The pick height follows the stack down, so the approach remains consistent from a full pallet to the last blank.
Do we need a compressed air supply?
Yes, for the vacuum generation and any pneumatic axes. The required flow and pressure are confirmed at design review and listed in the handover documentation.
What is the lead time?
Lead time depends on the configuration and the current build schedule at the Vaughan facility. Email [email protected] with your blank specification and target date and we will give you a schedule.
Related
Related Equipment
Sheet Metal Automation
Place Processing Automation Machines
Stations that position the part and perform the operation in one controlled cycle
View equipment
Sheet Metal Automation
Clinching Machine
Cold forming press that joins sheet metal without heat consumables or surface damage
View equipmentRobotics and Motion
Robotic Motion Assembly
Robot assembly cells delivered complete with tooling presentation guarding and controls
View equipmentRelated
Related Articles
Comparison Guide
Gantry or Robot for Pick and Place
How to choose between a gantry and an articulated robot for a handling application
Read the articleDesign Guide
Selecting Vacuum Cups for Sheet Metal Handling
Why hold time and cup layout matter more than raw vacuum level
Read the articleTroubleshooting Guide
Preventing Double Blanks in a De-Stacker
Why two sheets lift as one and what actually fixes it
Read the articleTalk to an engineer
Get a Quotation for This Machine
Send the part drawing, the operation and the rate you need. You will get a concept and a defined scope, not a brochure.