Client Background
Sheet metal fabrication operation running a flat bed laser
Project Challenge
Blanks were being lifted onto the laser table by hand. The sheets were large enough to need two people, the laser waited between cuts, and the placement varied with whoever was loading.
Customer Pain Points
- Two operators tied to the front of one machine
- Cutting capacity lost to loading time
- Manual handling exposure on every sheet
- Placement varying enough to force a margin into the cutting program
- Risk of two blanks being lifted as one
Our Solution
What We Built
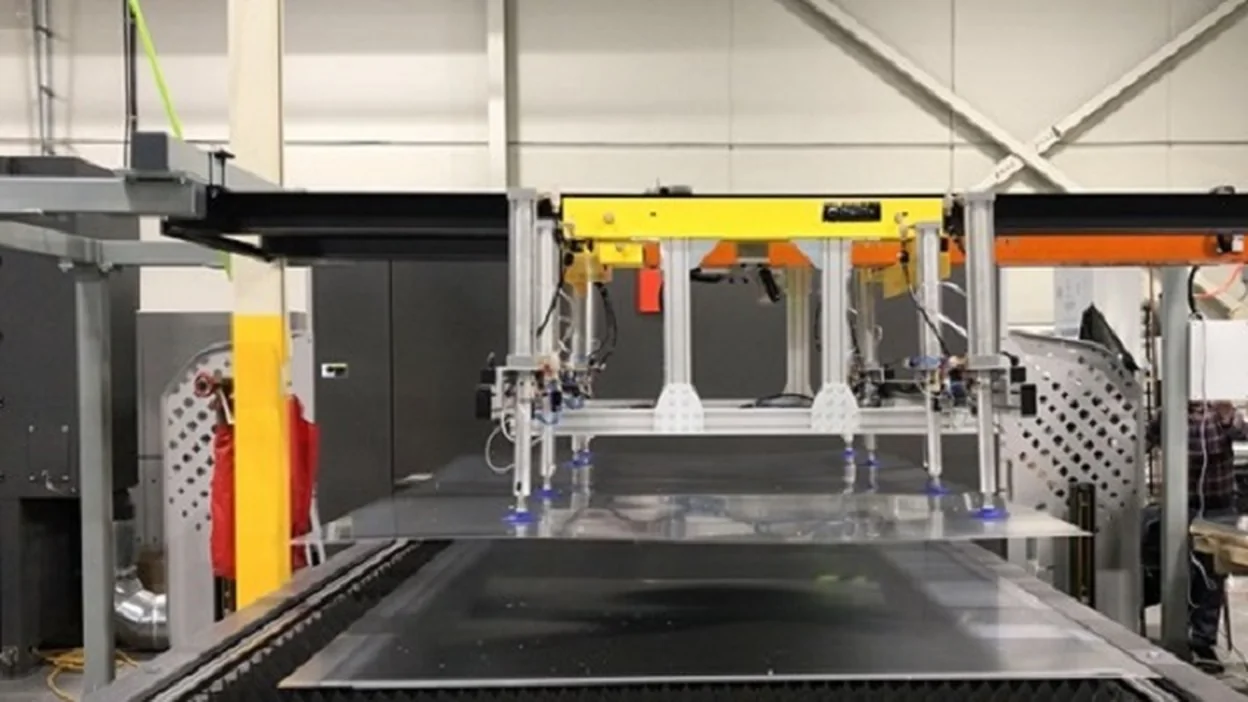
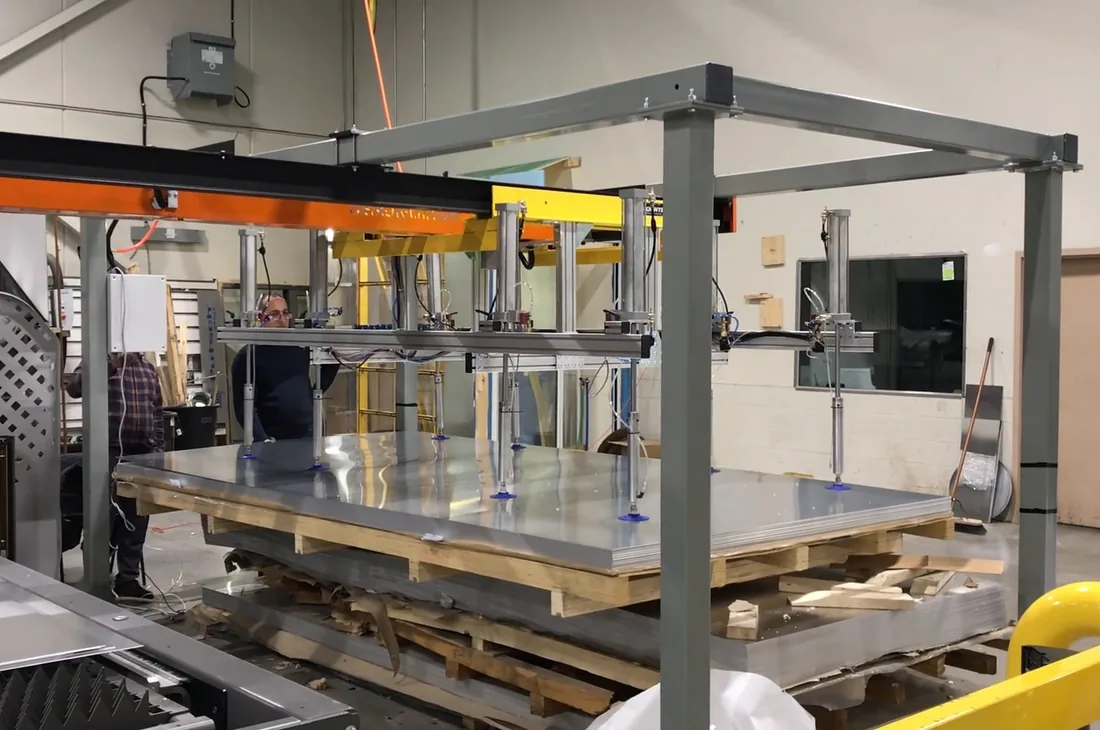
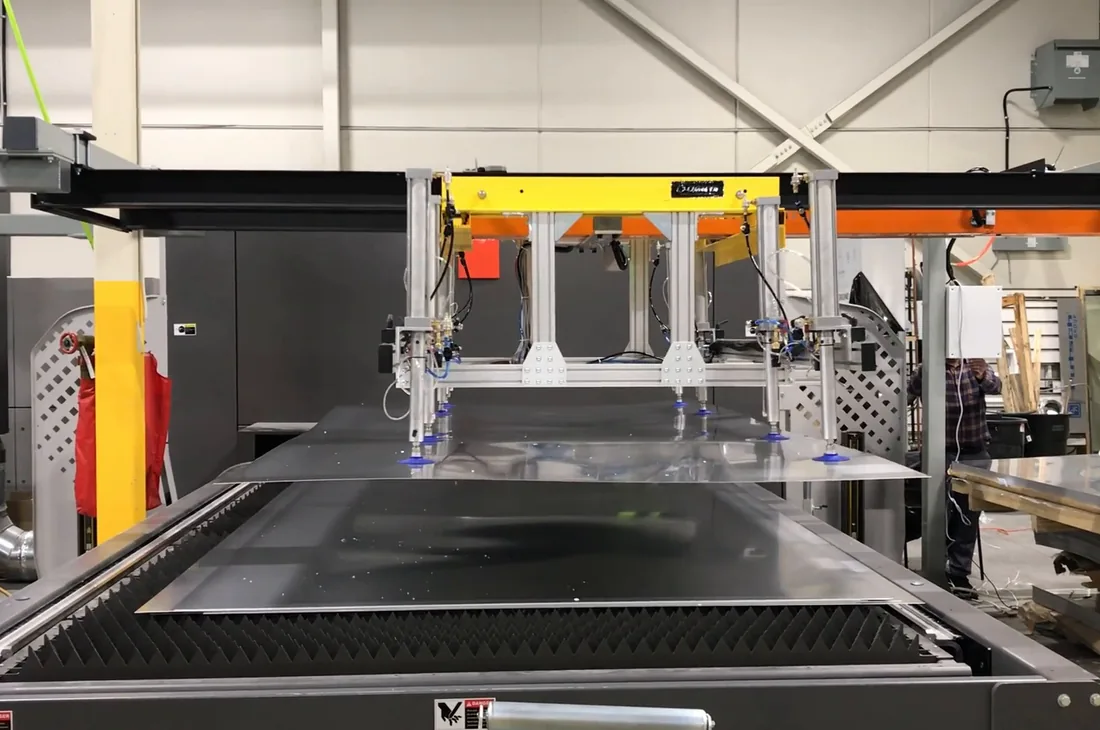
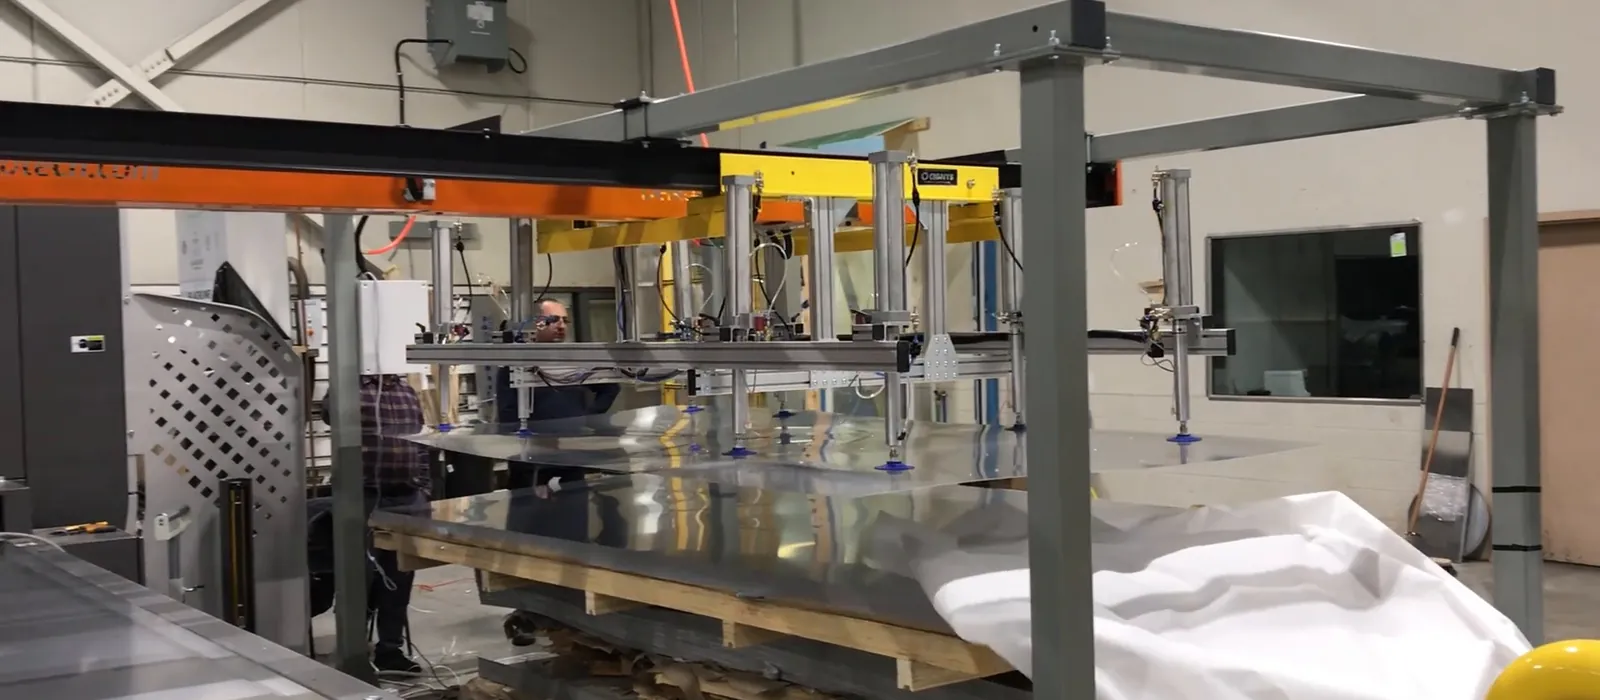
A vacuum gantry spanning the loading station and the laser table. Suction cups on a cross beam lower onto the top blank, lift it clear of the stack, traverse and release it in a repeatable position on the machine table. The pick height follows the stack down as the pallet empties, and the gantry clears the working envelope before the cutting cycle is allowed to start.
Manufacturing Process
How the Machine Was Built
Application review
Blank size, mass, surface and stack height recorded from the customer's actual production, with loading weight specified per the order.
Layout
Gantry laid out against the real footprint of the loading station and the laser, including pallet truck access.
Design
Frame, axes, vacuum tooling and control architecture designed together, with the sequence of operation written before code.
Build and assembly
Manufactured and assembled at the Delkotech facility in Vaughan.
Try out
Dry cycled, then run with blanks, then run at rate before installation.
Installation
Installed against the existing laser, interfaced with a handshake and commissioned with the customer's operators.
Supply Chain Coordination
Sourcing and Build
Structural steel, linear motion components, vacuum tooling and control hardware are sourced against the design, with the control platform chosen to match what the customer's maintenance team already supports. Build and assembly take place at the Vaughan facility so mechanical and controls work happen under one roof.
Quality Control
Checked Before Shipment
- Axis travel and repeatability checked before tooling was fitted
- Vacuum hold time measured with the heaviest specified blank
- Placement repeatability confirmed over a continuous cycle
- Safety functions and interlocks verified and recorded
- Rate run with customer blanks before shipment
Final Result
What the Machine Does Now
The cell loads the laser without an operator lifting a sheet. Blanks arrive on the table in a repeatable position, the machine is fed through breaks and shift changes, and the manual handling exposure at the front of the line has been removed.
Customer Benefit
Why It Mattered
The customer recovered cutting capacity that the machine could always deliver but the loading method could not support, and closed a manual handling risk at the same time.
Delkotech does not publish customer names, contract values or measured production figures for this project. Technical details and a reference discussion can be arranged on request.
Photographs
The Machine on the Floor
Related
Equipment Used
Sheet Metal Automation
Automatic Sheet Metal Pick and Place Machine
Vacuum gantry de-stacker that feeds blanks to a laser or press without manual lifting
View equipment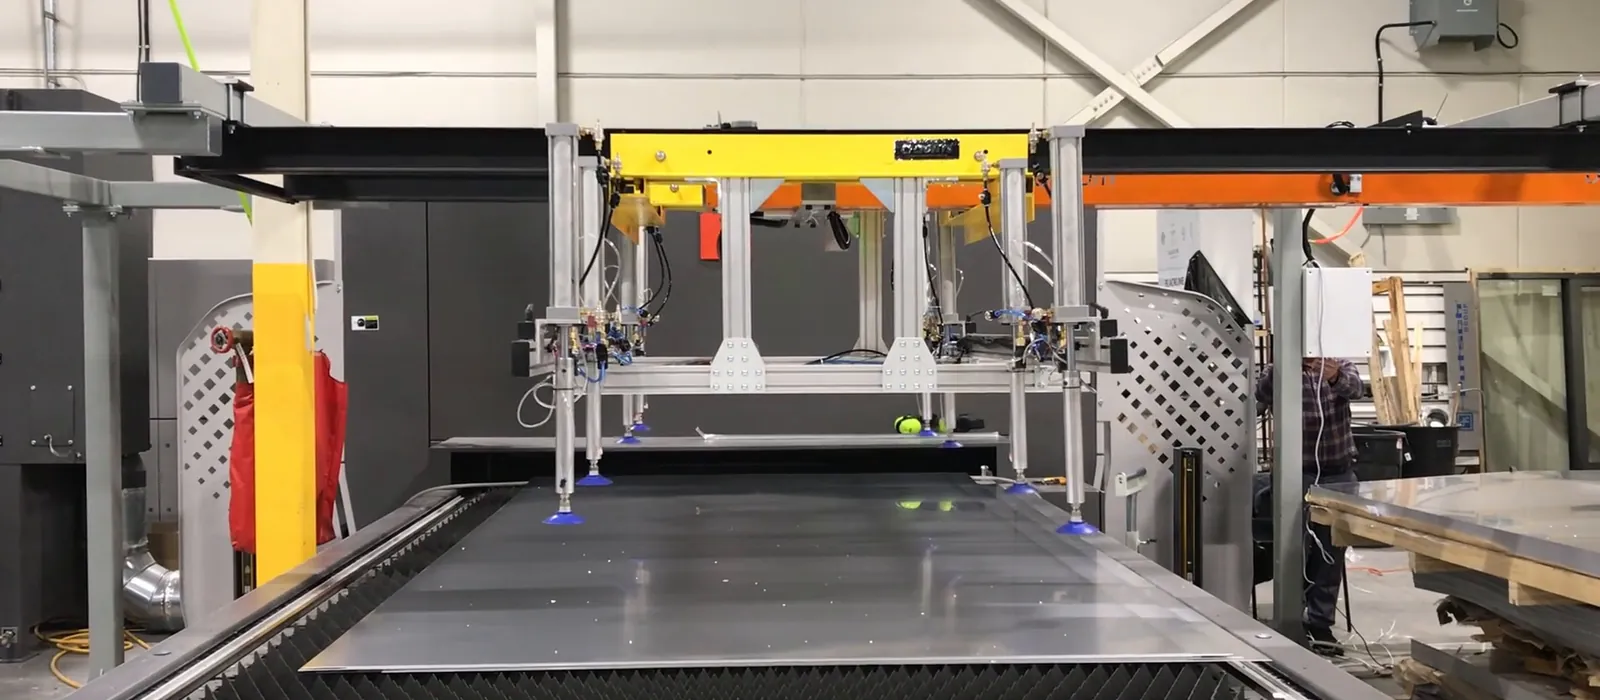
Sheet Metal Automation
Place Processing Automation Machines
Stations that position the part and perform the operation in one controlled cycle
View equipmentRobotics and Motion
Robotic Motion Assembly
Robot assembly cells delivered complete with tooling presentation guarding and controls
View equipmentRelated
Related Reading
Comparison Guide
Gantry or Robot for Pick and Place
How to choose between a gantry and an articulated robot for a handling application
Read the articleDesign Guide
Selecting Vacuum Cups for Sheet Metal Handling
Why hold time and cup layout matter more than raw vacuum level
Read the articleTroubleshooting Guide
Preventing Double Blanks in a De-Stacker
Why two sheets lift as one and what actually fixes it
Read the articleQuestions
About This Project
Can you tell us who the customer was?
Delkotech does not publish customer names, contract values or measured production figures for this project. Technical details and a reference discussion can be arranged on request.
Could you build the same machine for us?
Not identically, and that is the point. The machine was designed around one customer's part, rate and floor space. The same approach applied to your part produces a different machine.
How long did the project take?
Project duration depends on scope and the build schedule at the time. We are happy to give you a realistic schedule for your own requirement once the scope is defined.
What was proved before the machine shipped?
The checks listed in the quality control section of this page, run at the Vaughan facility. Customer witnessed try out before shipment can be arranged.
How do we start a similar project?
Email [email protected] with the part drawing, the operation and the rate. That is enough for a concept and a defined scope.
Talk to an engineer
Have a Similar Operation
Send the part and describe the step. We will tell you what the same approach would look like applied to your line.