Client Background
Panel and enclosure fabrication operation working in pre-finished sheet
Project Challenge
Back panels had to be joined without marking or burning the finish. Welding damaged the coating and created a touch up step, and fasteners added a piece price and a stores line to every assembly.
Customer Pain Points
- Coating damage at every welded joint
- A touch up operation that existed only to repair the joining process
- Fastener cost, feeding and stores handling
- Welding fume and extraction in an assembly area
- Joint verification that required destructive sampling
Our Solution
What We Built
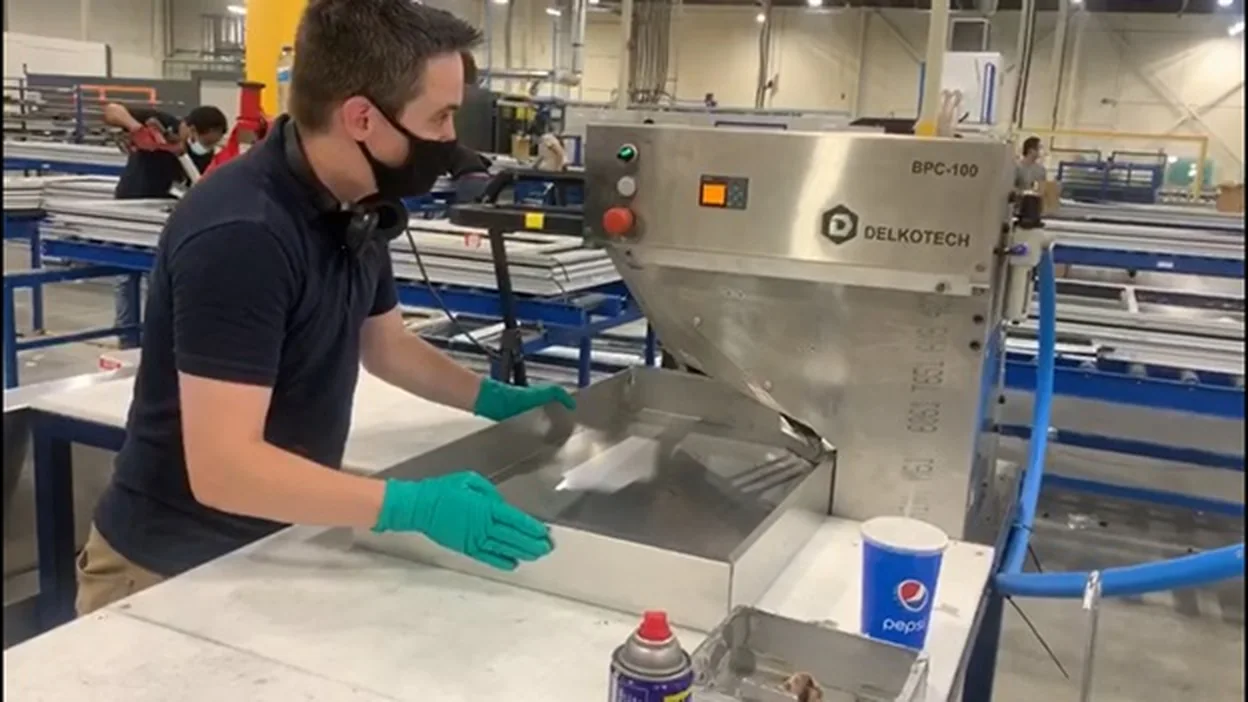
A Delkotech built clinching press that joins the panels by localised cold forming. The clinching process joins sheet metal without heat and without a consumable, and coated and painted sheet can be joined without damage to the surface finish. Frame throat and tooling were set so every joint position on the panel is reachable, and the stroke is controlled so each joint sees the same setting depth.
Manufacturing Process
How the Machine Was Built
Joint study
Material combination, total thickness, coating and required joint strength reviewed against the customer's own panels.
Tooling selection
Punch and die geometry selected for the stack and trialled on the customer's material.
Frame sizing
Throat and stroke sized so every joint position on the panel is reachable.
Build
Press, tooling and controls built and assembled at the Vaughan facility.
Sample joints
Buttons formed on customer material and checked against the agreed reference before shipment.
Installation
Set up on the customer floor with operator and maintenance training.
Supply Chain Coordination
Sourcing and Build
Frame steel, tool steel for the punch and die sets, drive and control components are sourced against the design. Tooling is treated as a wear item from the start, with the change interval based on joint counts rather than on a quality incident.
Quality Control
Checked Before Shipment
- Setting depth measured across the stroke range and recorded
- Sample joints formed on customer supplied material
- Button geometry checked against the agreed reference
- Repeatability run to confirm consistent joints over a continuous cycle
- Guarding and initiation circuit verified before shipment
Final Result
What the Machine Does Now
Panels are joined with the coating intact. The touch up operation that existed to repair weld damage is no longer needed, and joint quality can be checked visually and dimensionally on the line instead of by destructive sampling.
Customer Benefit
Why It Mattered
The joining step stopped creating work for the finishing department, and the consumable cost per joint went to zero.
Customer name, volumes and commercial terms are not published. Joint specifications and sample work can be discussed on request.
Related
Equipment Used
Sheet Metal Automation
Clinching Machine
Cold forming press that joins sheet metal without heat consumables or surface damage
View equipment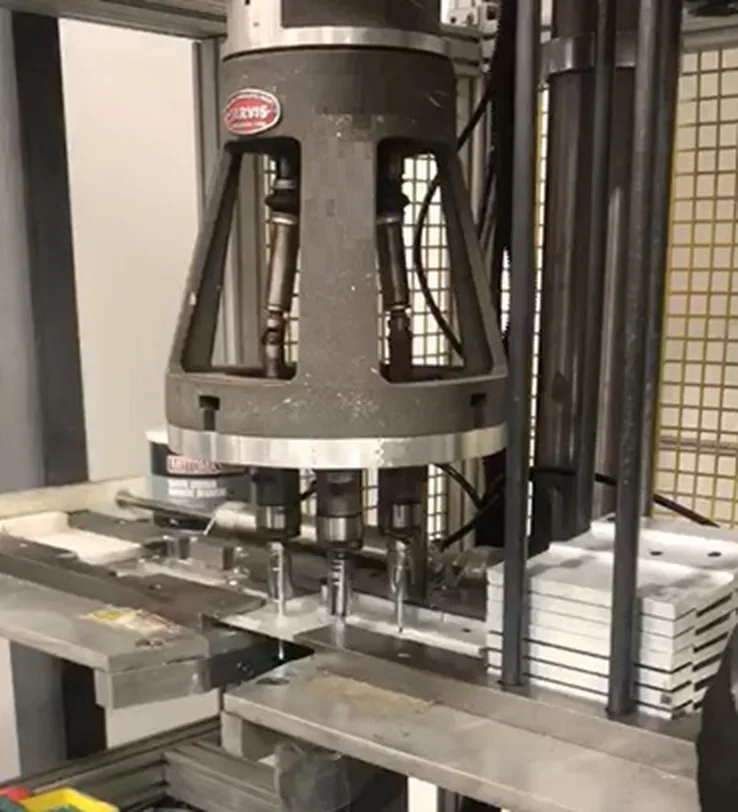
CNC Assembly Machines
Multi Spindle Screw Machines
Drive every fastener in a pattern in one stroke with torque controlled at each spindle
View equipment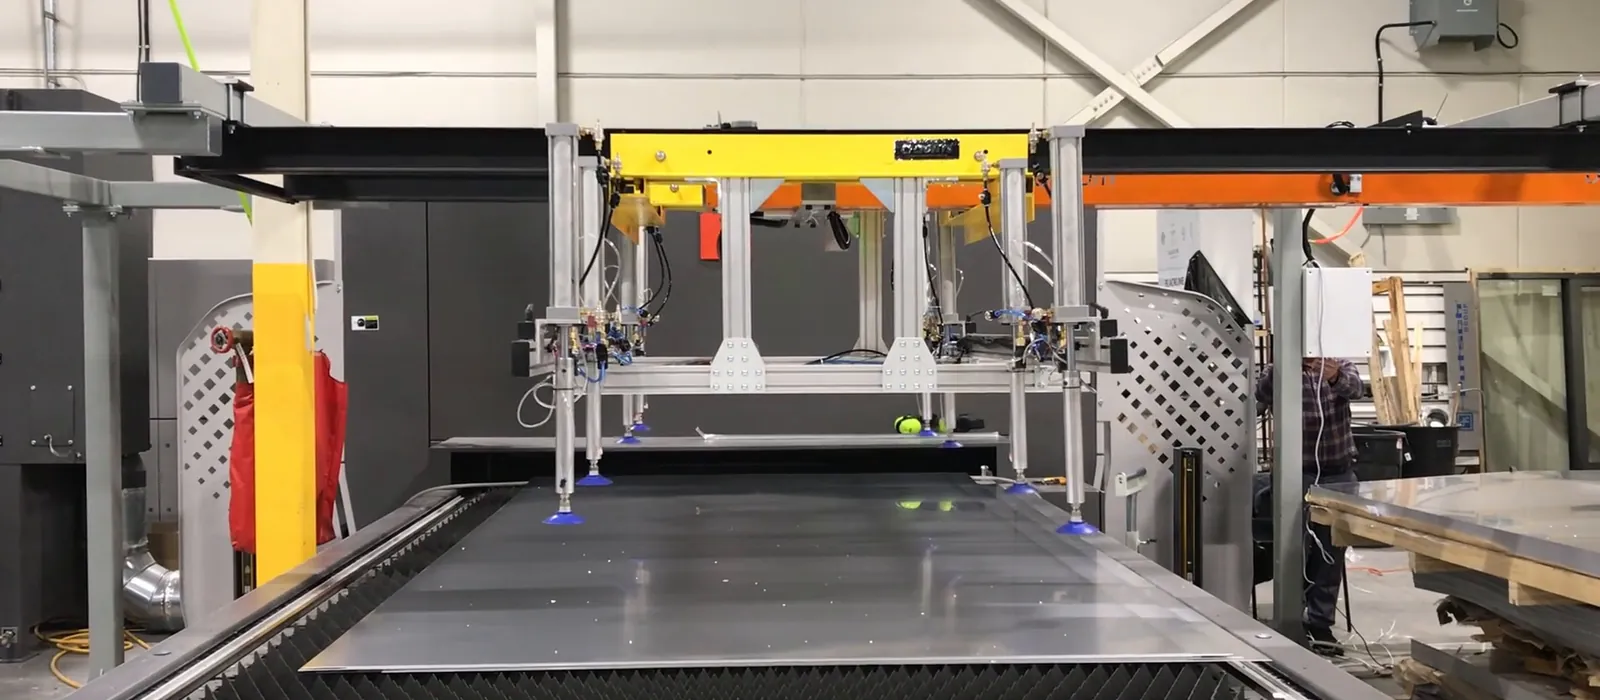
Sheet Metal Automation
Place Processing Automation Machines
Stations that position the part and perform the operation in one controlled cycle
View equipmentQuestions
About This Project
Can you tell us who the customer was?
Customer name, volumes and commercial terms are not published. Joint specifications and sample work can be discussed on request.
Could you build the same machine for us?
Not identically, and that is the point. The machine was designed around one customer's part, rate and floor space. The same approach applied to your part produces a different machine.
How long did the project take?
Project duration depends on scope and the build schedule at the time. We are happy to give you a realistic schedule for your own requirement once the scope is defined.
What was proved before the machine shipped?
The checks listed in the quality control section of this page, run at the Vaughan facility. Customer witnessed try out before shipment can be arranged.
How do we start a similar project?
Email [email protected] with the part drawing, the operation and the rate. That is enough for a concept and a defined scope.
Talk to an engineer
Have a Similar Operation
Send the part and describe the step. We will tell you what the same approach would look like applied to your line.