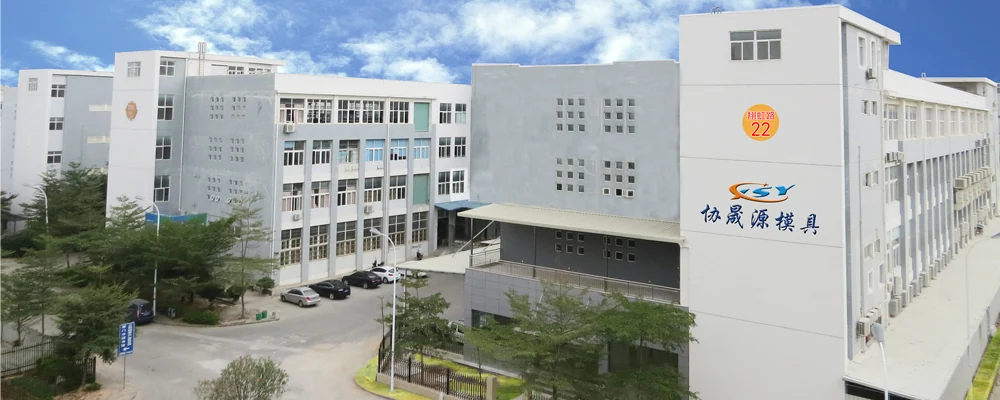
Injection Moulds Built And Proved In Our Own Tool Room
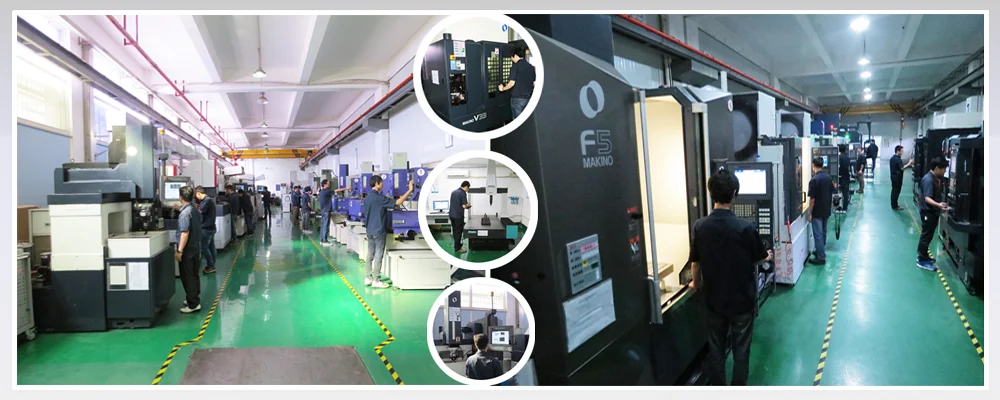
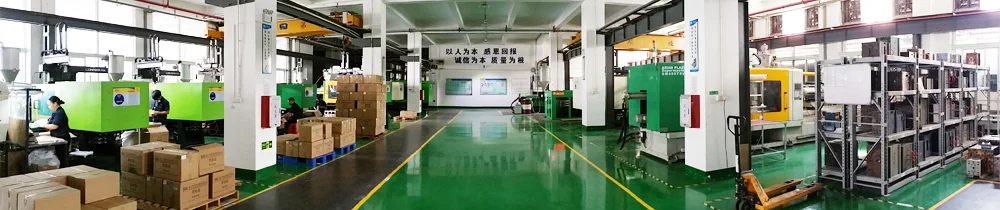
Five CNC machining centres, seven precision EDM machines and our own presses in Xiamen. Every mould is trialled here before it ships, and the measured cycle time goes with it.
- 2000Established
- 5000 m2Workshop Area
- 5CNC Machining Centres
- 7Precision EDM Machines
- 500K to 600KMould Shot Life
- 4 countriesExport Markets
What We Make And Who It Is For
Most of what goes wrong on a moulded part is decided before any steel is cut. We settle the gate, the slides, the cooling and the cavity steel against your material and your volume, then prove the tool on our own press before it leaves.
What We Make
Injection moulds for sanitary ware, automotive interior, home appliance and electronic parts, the mould components that keep them running, and the moulded parts themselves.
Who We Serve
Bathroom brands, tier two automotive suppliers, appliance makers, display and electronics assemblers, medical instrument companies and IT hardware manufacturers.
What Problem We Solve
Most of what goes wrong on a moulded part is decided before any steel is cut. We settle the gate, the slides, the cooling and the cavity steel against your material and your volume, then prove the tool on our own press before it leaves.
Why Customers Stay
A tool room and a moulding floor on the same site since 2000, so the people who cut the cavity are the people who watch it run.
Moulds And Moulded Parts
Every product here comes from the company catalogue. Where the record gives a cavity steel, a cavity count and a cycle time, the page shows them.
Moulds For Sanitary Ware Parts
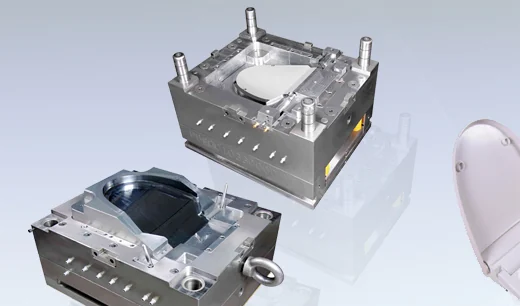
ABS Sanitary Part Mould With S136 Cavity Steel
Stainless quenched cavity for a plated bathroom part
Product materials ABSMould material S136 quenching
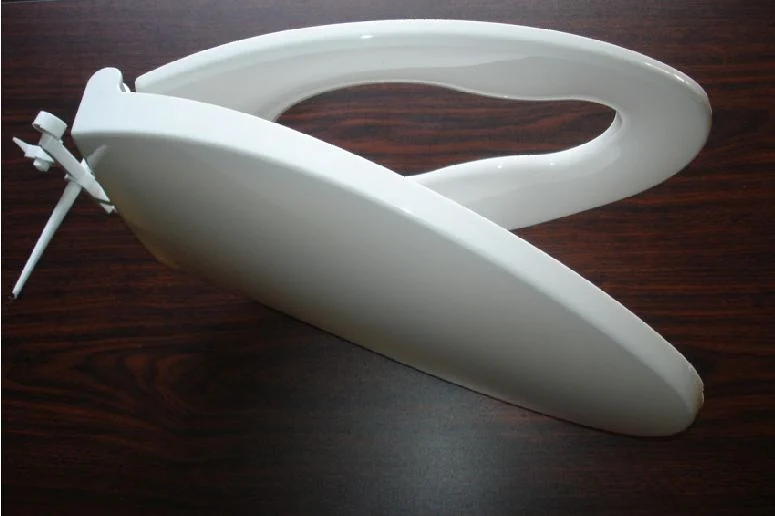
Moulds For Sanitary Ware Parts
PP Cover Plate Mould With NAK80 Cavity Steel
Pre-hardened NAK80 on a large flat polypropylene part
Product materials PPMould material DAIDO NAK80
Moulds For Sanitary Ware Parts
ABS Sanitary Part Mould With Three Slides
Three independent pull directions on one impression
Product materials ABSMould material DAIDO S-Star quenching
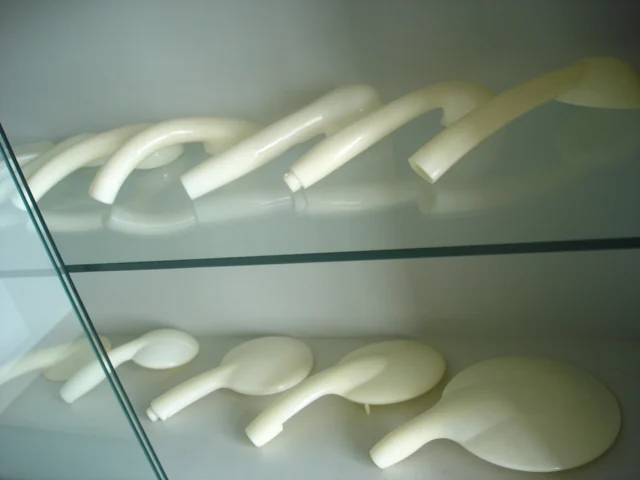
Moulds For Sanitary Ware Parts
ABS Shower Head Mould With Two Cavities And Six Slides
The most complex tool in the archived catalogue
Product materials ABSMould material DAIDO NAK80
Moulds For Sanitary Ware Parts
PP Cover Plate Family Mould
Two different parts out of the same shot
Product materials PPMould material DAIDO NAK80
Moulds For Sanitary Ware Parts
ABS Sanitary Part Mould With Two Cavities And Four Slides
The highest output sanitary tool in the archive
Product materials ABSMould material S136 quenching
Moulds For Sanitary Ware Parts
ABS Sanitary Part Mould With Submarine Gate
The simplest tool here, and the cheapest to keep running
Product materials ABSCavity 1 x 1
Moulds For Sanitary Ware Parts
ABS Shower Body Mould With S136 Cavity Steel
A heavy section part cooled for what it actually is
Product materials ABSMould material S136 quenching
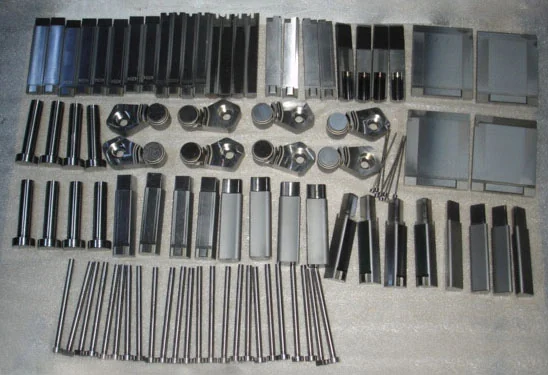
Moulds For Sanitary Ware Parts
Bush Mould
A small round part moulded on a replaceable core
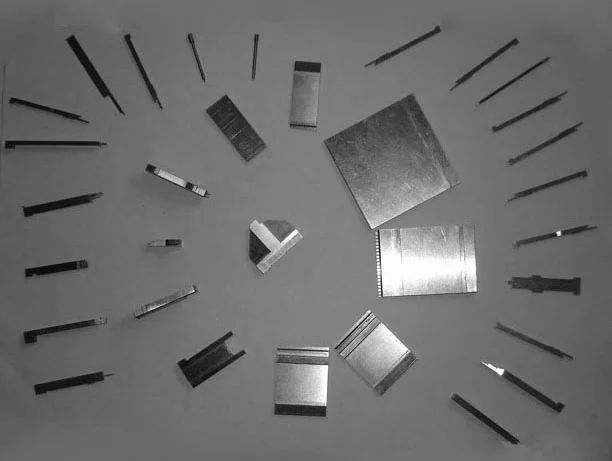
Moulds For Sanitary Ware Parts
Rotor Mould
Vane geometry cut by EDM rather than milled
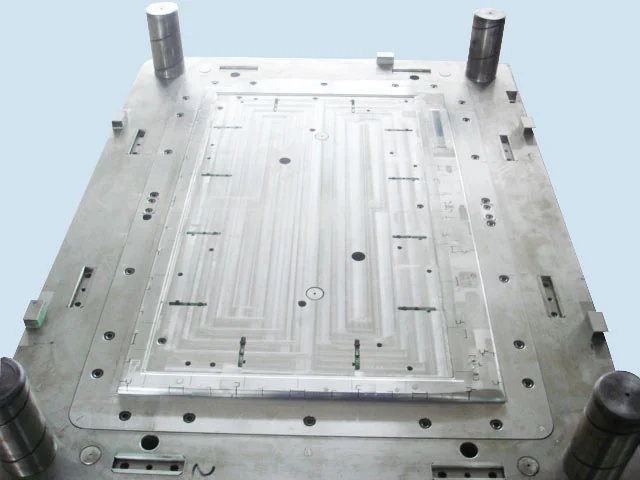
Moulds For Automotive Interior Parts
PC ABS Automotive Part Mould With SKD61 Cavity Steel
SKD61 for the melt temperature and abrasion of PC ABS
Product materials PC/ABSMould material SKD61
Moulds For Automotive Interior Parts
Support Bracket Mould
A load carrying part where the weld line position matters
Browse By Category
Category
Moulds For Sanitary Ware Parts
Injection moulds for shower heads, shower bodies, cisterns, seats and cover plates in ABS and PP
10 products
Category
Moulds For Automotive Interior Parts
Injection moulds for support brackets, door panel parts and tray tables in PC ABS and engineering blends
4 products
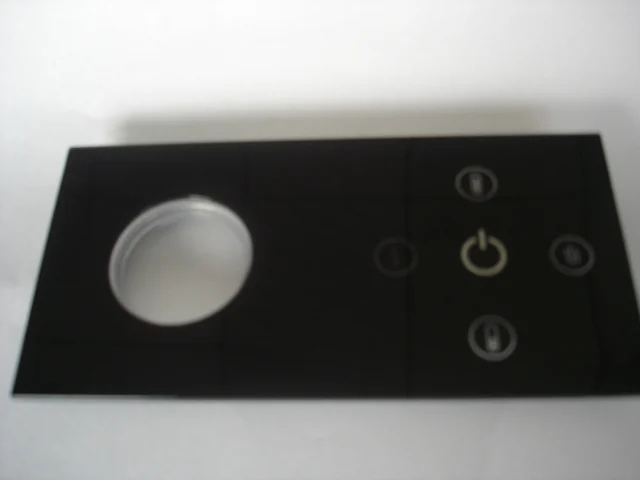
Category
Moulds For Home Appliance Parts
Injection moulds for appliance housings, control panels and trim parts in PC and PC blends
2 products
Category
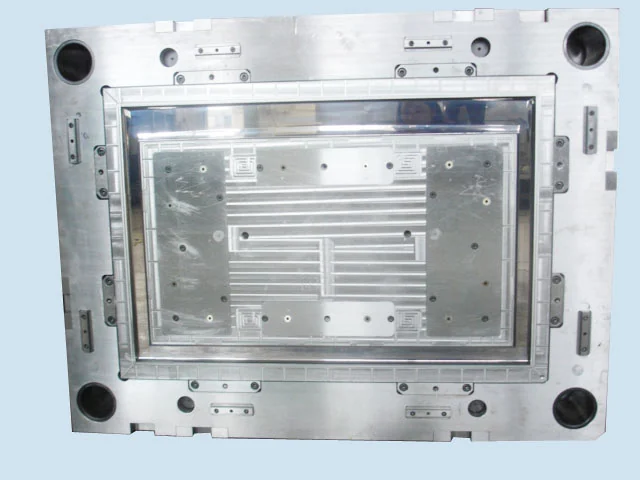
Moulds For Electronic And Audiovisual Parts
Injection moulds for television front shells, enclosures and electronic housings in PC and PC ABS
4 products
Category
Moulds For Other Product Series
Injection moulds that sit outside the sanitary, automotive, appliance and electronics groups
3 products
Category
Mould Components And Inserts
Machined cavity inserts, core pins, slides and mould base components made in the same tool room
2 products
Category
Plastic Injection Moulded Parts
Finished moulded parts produced on our own presses, from shower fittings to television front shells
13 products
Who We Serve
Bathroom brands, tier two automotive suppliers, appliance makers, display and electronics assemblers, medical instrument companies and IT hardware manufacturers.
Industry
Sanitary Ware
Shower heads, hand showers, cisterns, toilet seats and cover plates moulded in ABS and PP
Industry
Home Appliance
Housings, control panels and trim parts for white goods and small domestic appliances
Industry
Automotive Interior
Support brackets, door panel parts and tray tables moulded in PC ABS and engineering blends
Industry
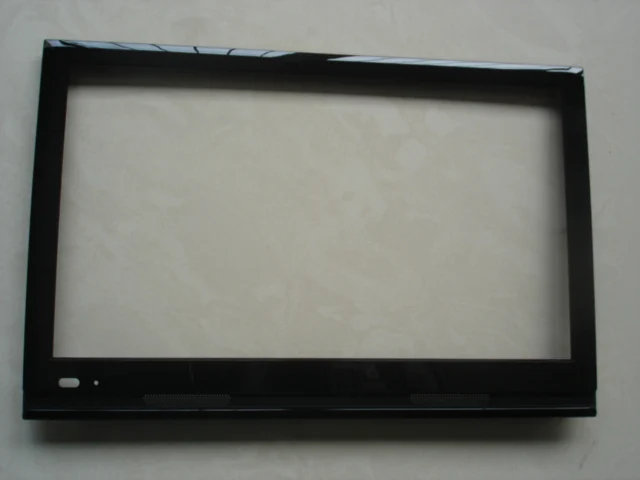
Electronics And Audiovisual
Television front shells, enclosures and electronic housings in PC and PC ABS
Industry
Medical Instrument
Instrument housings and moulded components for medical equipment makers
Industry
IT And Communications
Enclosures, covers and moulded detail parts for IT and communications hardware
What Goes Wrong On A Moulded Part
The gate is in the wrong place and it is now in steel
Gate position decides where weld lines land, how evenly the part packs and whether anyone has to trim it. Moving it later means welding and recutting a cavity. We agree it in writing at design review instead.
The cavity steel was chosen for the quotation, not the part
A pre-hardened cavity on a plated ABS part looks like a saving until the polish goes at two hundred thousand shots. Every mould in this catalogue names its steel, and the reason it was chosen.
Nobody knows whether the cycle time is real
An estimated cycle time becomes your piece price. Ours are measured on a trial here, on our own machines, and the figure travels with the tool.
The tool arrives untried and becomes your problem
A mould shipped without a trial moves the risk to whoever opens the crate. Ours run on an injection machine in this building first, and the correction list goes with them.
The tool was corrected at the bench and nobody wrote it down
Three years later a repair starts from a drawing that no longer matches the tool. Corrections here are recorded against the mould number with the date and the reason.
Mould and moulding sit with different suppliers
When the part is wrong, the tool maker blames the process and the moulder blames the tool. Both happen here, which removes the argument.
Why Buyers Choose XSY Mould
What the plant holds
- 5 cnc machining centres - high-precision cavity and core milling, run from cad cam programmes
- 7 precision edm machines - spark erosion for ribs, text and corners a cutter cannot reach
- 4 wire cutting machines - fast wire and slow wire cutting for inserts, slides and ejector holes
- 4 precision grinding machines - flatness and parallelism on plates, inserts and slide faces
- 9 milling machines - plate preparation, pockets and general tool room work
How We Work
Solution
Mould Design And DFM Review
The stage where most of the tool cost and nearly all of the part risk is decided
Solution
Mould Making And First Article Trial
Cutting, fitting and proving the tool in our own press before it ships
Solution
Injection Moulding Production
Running the tool for finished parts instead of shipping it away
Solution
Export Packing And Delivery
Getting the mould or the parts out of Xiamen without damage or customs delay
Every Mould Goes Through The Same Route
Design review
Part geometry, wall sections, draft and gate position are reviewed against the moulding material before any steel is cut.
Steel inspection
Cavity and core blocks are checked on arrival so that the hardness and grade match what the mould was quoted with.
In-process measurement
Machined inserts, slides and plates are measured between operations rather than only at the end of the tool room route.
Fitting and spotting
Parting line, slide movement and ejection are fitted by hand before the mould goes to the press.
Mould trial
The mould is run on an injection machine and short shots, full parts and a cycle time reading are taken from the trial.
First article measurement
Trial parts are measured on the image projector against the drawing and the report goes out with the samples.
Pre-shipment check
Mould surfaces are cleaned and oiled, water and hydraulic circuits are plugged, and the spare component set is packed with the tool.
From The Knowledge Centre
Material Guide
How To Choose Cavity Steel For An Injection Mould
S136, NAK80, S-Star, SKD61 and 718 all appear in this catalogue. What each one is actually for, and what it costs you to pick the wrong one.
Process Guide
Pinpoint Side Submarine And Valve Gates Compared
All four gate types appear in this catalogue. Where each one belongs, what it leaves on the part, and what it costs in mould construction.
Comparison Article
Hot Runner Or Cold Runner For Your Injection Mould
When the extra tool cost of a hot runner pays for itself, and when it is money spent on a manifold you then have to maintain.
Buying Guide
Single Cavity Multi Cavity Or Family Mould
Impression count is most of the tool price and most of the piece price. How to decide it before you ask for a quotation.
Design Guide
Slides And Lifters And What Undercuts Really Cost
Every undercut adds a moving part to the mould. From one slide to six, what each one adds to cost, cycle and maintenance.
Material Guide
ABS PP PC And ASA For Moulded Industrial Parts
The four materials in this catalogue, what each is chosen for, and what changing between them does to the mould.
Download Centre
Company Profile
XSY Mould Capability Overview
Plant, equipment list, quality route and export terms on two pages.
Download PDF
Technical Reference
Mould Steel And Material Reference
S136, NAK80, S-Star, SKD61 and 718 compared against ABS, PP, PC, PC ABS and ASA.
Download PDF
Checklist
Injection Mould Enquiry Checklist
The nine things a mould maker needs from you before a quotation means anything.
Download PDF
Specification Sheet
Archived Mould Specification Table
Every specified mould in this catalogue with its material, cavity steel, cavity count, slides, gate, cycle and shot life.
Download PDF
Questions Buyers Ask First
Six things worth knowing before you send a drawing.
Do you build moulds only, or do you also mould the parts?
Both, on the same site. The tool room builds and proves the mould, and injection machines below 600 tons run production. Buyers who only want parts stop at the moulding stage and never take delivery of a tool.
What information do you need before you can quote a mould?
A 3D model in STEP or IGES, a drawing marking the dimensions that matter, the exact moulding grade and colour, whether the part is plated or painted, and the annual volume. Volume decides impression count, and impression count is most of the tool price.
Which materials do you mould?
The archived catalogue records ABS, PP, PC, PC ABS and ASA. Those cover the sanitary, appliance, automotive and electronics parts shown here. Name your exact grade at enquiry, because fillers and flame retardant packages change the cavity steel choice.
How long does a mould take?
It depends on impression count and slide complexity, so a date is given with the quotation rather than as a general figure. What the date includes is the first trial and the corrections that come out of it, not just the moment the tool is finished.
Where do you ship from and on what terms?
Xiamen. The archived catalogue quotes FOB Xiamen or CIF, with payment by T/T or L/C and a minimum order of one set. Mould work from this plant has gone to the Netherlands, Croatia, Japan and Taiwan.
Can you work on a tool that was built somewhere else?
Yes, provided it arrives with its drawings and a spare component set. We check it in the press first and report what we find before committing to a cycle time.
Send Us A Part And We Will Quote It Properly
A model, the moulding grade and your annual volume are enough to get a real number with the cavity steel and impression count named.