Slides And Lifters And What Undercuts Really Cost
Every undercut adds a moving part to the mould. From one slide to six, what each one adds to cost, cycle and maintenance.
An undercut is a feature the mould cannot simply open away from
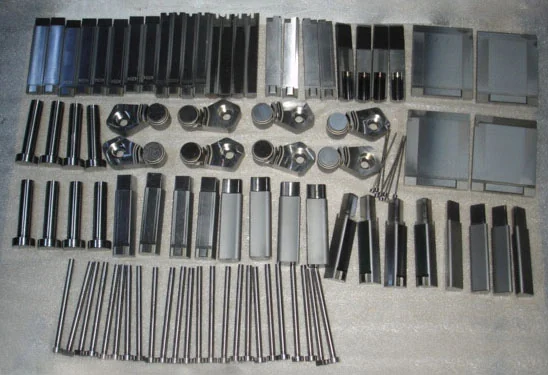
If a feature sits sideways to the direction the mould opens, something has to move sideways to release it. That something is a slide or a lifter, and it is a mechanism: it wears, it needs grease, and it is where flash starts when it stops fitting. The tools in this catalogue range from zero slides to six, and the difference in ownership cost between the two ends is larger than the difference in purchase price.
What each slide adds
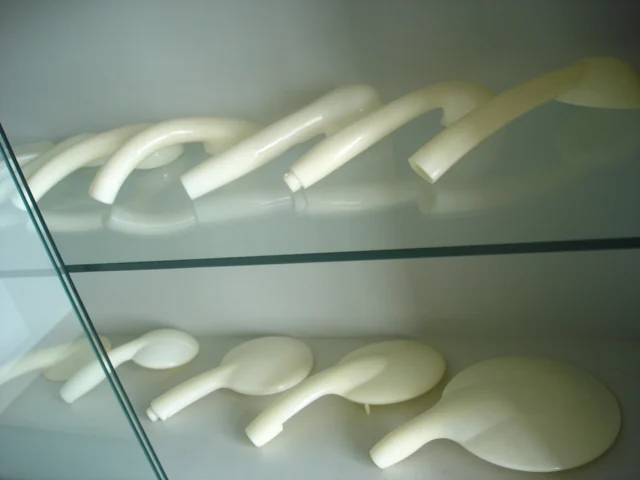
The first slide adds the most, because the mould base has to grow to accommodate the mechanism and the ejection has to be sequenced around it. After that each additional slide is cheaper to build but keeps adding cycle time, since every slide has to clear before ejection and close before the next shot. The six slide shower head tool in this catalogue cycles in 100 seconds; the no slide electronic tool cycles in 50.
The six slide shower head tool
Lifters for internal undercuts
A lifter moves at an angle as the ejector plate pushes, so it releases an internal undercut without the separate mechanism a slide needs. It suits small internal features such as a snap hook or a latch window. It cannot handle a large external feature, and it travels inside the ejection stroke, so the part has to have somewhere for it to go.
The cheapest undercut is the one designed out
Before accepting a slide, check whether the feature can be reoriented, shut off against the opposite face, or moved to a separate part. A design review that removes two slides from a tool pays for itself several times over the life of the programme. The straight pull PC tools in this catalogue, with no side actions at all, are the cheapest moulds here to own.
In This Guide
Products Referenced In This Guide
Moulds For Sanitary Ware Parts
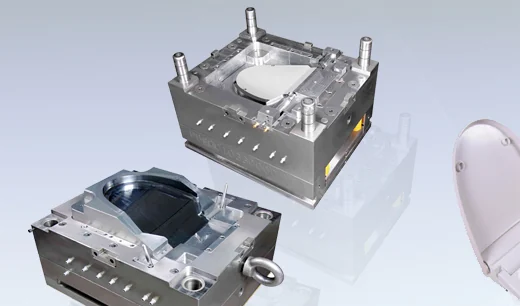
ABS Shower Head Mould With Two Cavities And Six Slides
The most complex tool in the archived catalogue
Product materials ABSMould material DAIDO NAK80
Moulds For Sanitary Ware Parts
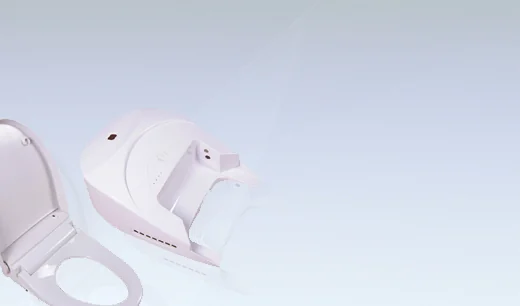
ABS Sanitary Part Mould With Three Slides
Three independent pull directions on one impression
Product materials ABSMould material DAIDO S-Star quenching
Moulds For Electronic And Audiovisual Parts
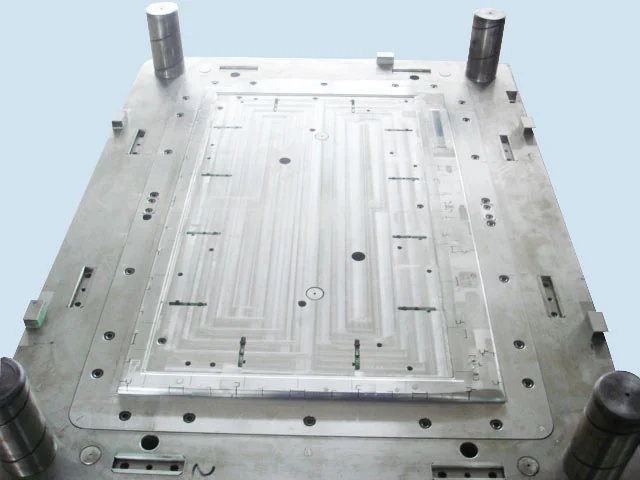
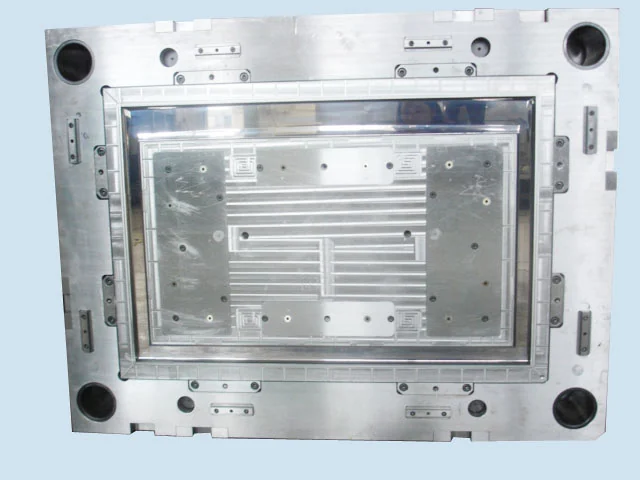
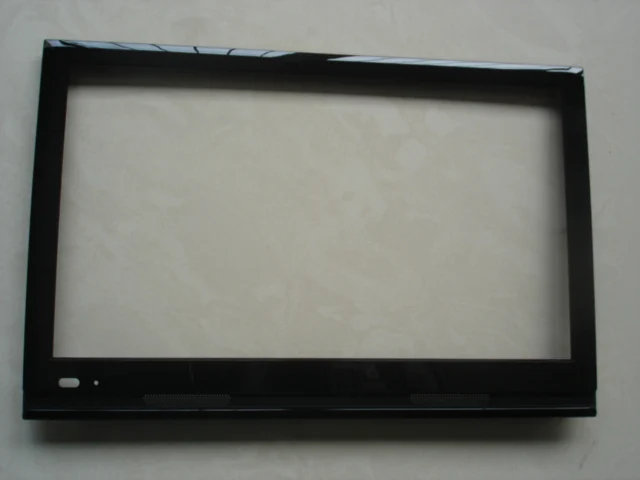
PC Electronic Part Mould With S136 Cavity Steel
No slides at all, which keeps flash risk near zero
Product materials PCMould material S136
Mould Components And Inserts
Mould Base Components
Guide pillars, bushings and slide hardware as a matched set
Related Reading
Buying Guide
How Cycle Time Decides The Price Of A Moulded Part
The cycles in this catalogue run from 40 to 100 seconds. What drives that spread, and why it matters more than the tool price.
Buying Guide
How To Brief A Chinese Mould Maker And Get A Real Quotation
What to send, what to ask for, and which missing piece of information causes most of the surprises later.
Industry
Sanitary Ware
Shower heads, hand showers, cisterns, toilet seats and cover plates moulded in ABS and PP
Industry
IT And Communications
Enclosures, covers and moulded detail parts for IT and communications hardware
Questions On This Topic
Follow up questions this guide raises.
How many slides is too many?
There is no fixed number. Six is normal on a shower head. Six on a flat cover would suggest the part should be redesigned. What matters is whether each slide is earning a feature that the product genuinely needs.
Do slides always add cycle time?
Yes, because the sequence is longer. How much depends on travel and whether slides can move simultaneously. It is usually a few seconds each, which over a production life is a real number.
What maintenance do slides need?
Greasing on a defined interval, wear plate inspection, and a check that every slide returns fully after any press change. A slide that does not return will damage the cavity on the next close, which is the most expensive avoidable failure on a mould.
Apply This To Your Own Part
General guidance only goes so far. Send the model and the moulding grade and we will tell you what it means for your tool.