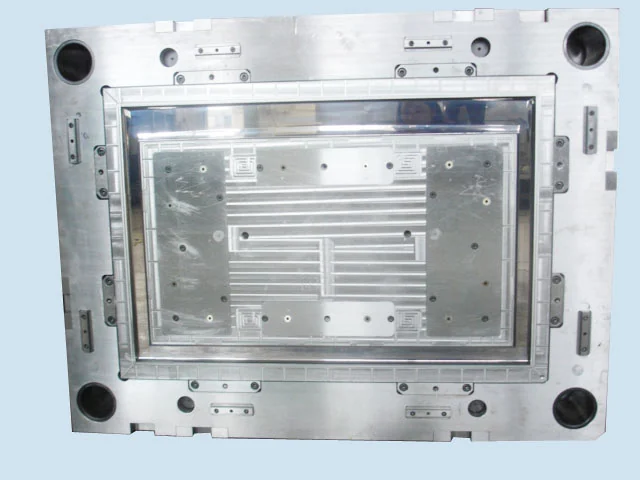
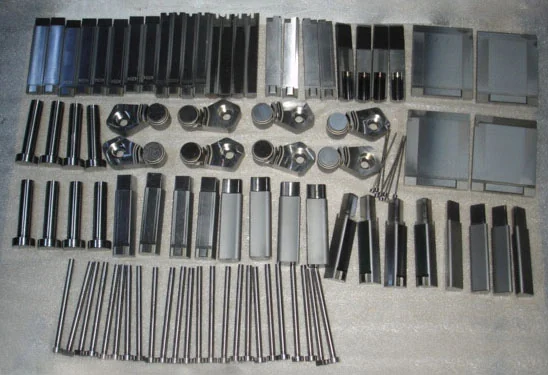
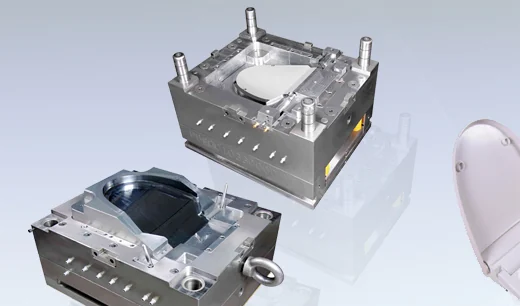
PP Cover Plate Family Mould
Family mould PP tool, DAIDO NAK80 cavity, two slides, side gate, 100 sec cycle, 500,000 shots.
What This Tool Is
A 1+1 family tool: two different cover plate components come out of every shot instead of two copies of one part, so the pair always matches in colour and batch. The tool runs two slides and a side gate. The archived record puts the cycle at 100 sec and the tool life at 500,000 shots.
Polypropylene shrinks considerably more than the styrenics, so the cavity has to be cut oversize by the right amount and the cooling has to be laid out for the part rather than carried over.
Company catalogue record 175.
Specification And Trade Terms
Mould specification
| Product materials | PP |
|---|---|
| Mould material | DAIDO NAK80 |
| Cavity | 1 + 1 family |
| Slider | 2 |
| Gate | Side gate |
| Cycle time | 100 sec |
| Warranty | 500,000 shots |
Commercial terms
| Product origin | China |
|---|---|
| Price terms | FOB Xiamen or CIF |
| Payment terms | T/T or L/C |
| Minimum order | 1 set |
| Mould standard | HASCO or DME standard components |
Key Benefits
NAK80 arrives pre-hardened and pre-polished, so the cavity goes straight to finishing without a heat treatment step that can move a large block, which is why it is the cavity steel on this a matched pair of PP cover plate components tool
A side gate feeds the part from the edge on a simple two plate tool
A family layout gives one tool, one press and one setting instead of two of each, and the matched parts always leave the press in the same colour and batch
Two slides is a low count for this kind of part, and every slide left out is cycle time and maintenance removed
Polypropylene shrinks considerably more than the styrenics, so the cavity has to be cut oversize by the right amount and the cooling has to be laid out for the part rather than carried over
Problems It Solves
Polypropylene parts come out of a cavity cut for the wrong shrinkage at the wrong size, and no process setting fixes that
A cold gate on a visible face leaves a witness that somebody then has to trim, colour match or hide
Who It Is For And Where It Is Used
Who it is for
- Bathroom and sanitary ware brands
- Sanitary component assemblers
- Trading companies holding a bathroom brand
Application scenarios
- Moving a European shower tool to an Asian source without changing the part
- Replacing a cover plate tool that has started to bow parts
- Adding a second impression once a launch programme reaches volume
Technical Features And Materials
Technical features
- DAIDO NAK80 cavity and core
- 1 + 1 family impression layout
- Side gate feed
- Two mechanical slides with hardened wear plates
- Cavity and core rated at 500,000 shots
- HASCO or DME standard mould base components
Customisation options
- Impression count revised up or down once you give us the real annual volume
- Cavity steel changed from DAIDO NAK80 where your moulding grade or your expected shot count calls for something different
- Gate type moved away from the side gate if the cosmetic face or the degating requirement changes
- Cosmetic features such as texture, logos and part numbers cut as replaceable inserts so a later change does not mean a new cavity
- Mould base built to HASCO or DME dimensions, or to a standard your own tool room already stocks spares for
Materials
- PP
How This Mould Is Made
- Cavity and core blocks are inspected against the specified grade before they enter the machining route
- Cavity geometry is cut on the CNC machining centres from programmes generated off the released part model
- Rib roots, text and internal corners are burned in with EDM electrodes, which is detail no rotating cutter can reach
- The two slide pockets are wire cut so the slide fit repeats rather than being filed in
- The moulding face is polished to the finish the part needs, which for a plated part is a different grade from a textured one
- Parting line, shut offs and ejection are fitted and spotted by hand at the bench
- The tool is trialled on one of our injection machines and the 100 sec cycle is measured rather than assumed
Quality Control On This Tool
- Incoming cavity and core steel is checked against the grade on the order, not against the delivery note
- Machined inserts and plates are measured between operations rather than only at the end of the route
- Slide travel and shut off contact are checked at the bench before the tool goes anywhere near a press
- Trial parts are measured on the 2D image measuring projector against the dimensions nominated on your drawing
- Each impression is reported separately, because matched cavities drift apart over life and an averaged figure hides that
- Corrections found at trial are recorded against the mould number with the date and the reason, so a repair years later starts from what the tool actually is
- Before shipment the water and hydraulic circuits are blown out and plugged and the moulding faces are oiled
Compared With The Alternatives
Separate single cavity tools for each part
More flexible if the parts are ever needed in different quantities, but twice the tool cost and twice the press time.
A quenched stainless cavity such as S136
Longer polish life and corrosion resistance for a plated or damp environment part, at a higher steel and heat treatment cost than this tool needed.
A hot runner version
Removes the runner weight and allows a gate in the middle of the part, at a higher tool cost and with a heated manifold to maintain.
Use And Maintenance Guide
- Run the tool in the PP grade it was trialled with; changing grade changes shrinkage and cavity wear at the same time
- Inspect the side gate at every service, because gate condition is what decides whether parts come off the tool clean
- Grease the slide gibs on the interval in the tool documentation rather than waiting for flash to appear
- Check that every slide returns fully after a press change; a slide that does not return will damage the cavity on the next close
- Oil the moulding faces and plug the circuits for any storage longer than a week
Related Products
Moulds For Sanitary Ware Parts
ABS Sanitary Part Mould With S136 Cavity Steel
Stainless quenched cavity for a plated bathroom part
Product materials ABSMould material S136 quenching
Moulds For Sanitary Ware Parts
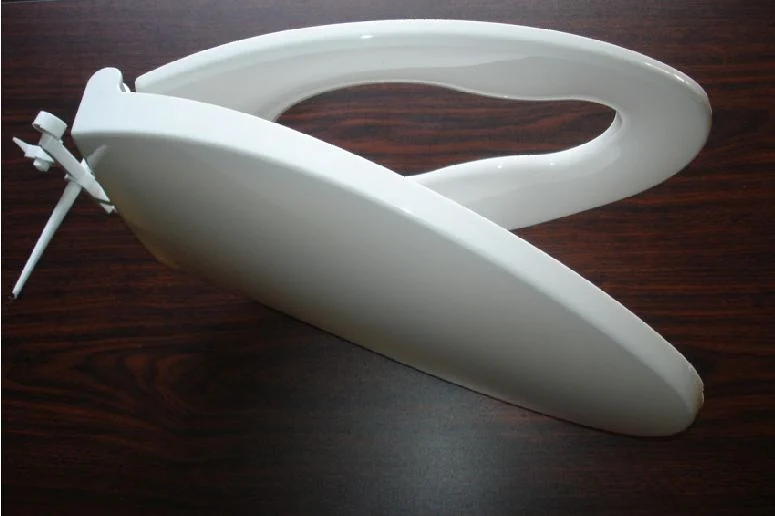
PP Cover Plate Mould With NAK80 Cavity Steel
Pre-hardened NAK80 on a large flat polypropylene part
Product materials PPMould material DAIDO NAK80
Moulds For Sanitary Ware Parts
ABS Sanitary Part Mould With Three Slides
Three independent pull directions on one impression
Product materials ABSMould material DAIDO S-Star quenching
Moulds For Automotive Interior Parts
PC ABS Automotive Part Mould With SKD61 Cavity Steel
SKD61 for the melt temperature and abrasion of PC ABS
Product materials PC/ABSMould material SKD61
Industries And Guides
Industry
Sanitary Ware
Shower heads, hand showers, cisterns, toilet seats and cover plates moulded in ABS and PP
Industry
Medical Instrument
Instrument housings and moulded components for medical equipment makers
Buying Guide
Single Cavity Multi Cavity Or Family Mould
Impression count is most of the tool price and most of the piece price. How to decide it before you ask for a quotation.
PP Cover Plate Family Mould Questions
What buyers ask about this tool before ordering.
Why DAIDO NAK80 for this tool?
NAK80 arrives pre-hardened and pre-polished, so the cavity goes straight to finishing without a heat treatment step that can move a large block. It polishes well, which is why it turns up on cosmetic parts that are not plated.
What does the side gate mean for the finished part?
A side gate feeds the part from the edge on a simple two plate tool. The witness sits on the edge, so the gate position has to land somewhere the assembly or the finish covers.
What does the 500,000 shots figure actually cover?
It is the cavity and core life the tool was built for, running the nominated PP grade under normal maintenance. It is not a guarantee against damage from a mispositioned part, a press fault or a missed service interval.
Is the 100 sec cycle achievable in our press?
It was measured on a trial here with the mould running PP. Cycle time follows the heaviest section of the part far more than it follows the press, so it should transfer, but confirm your clamp tonnage and cooling capacity with us first.
What happens if I need more of one part than the other?
A family tool makes that awkward. You either overproduce one part or block an impression, which unbalances the fill. If the ratio is not close to what the tool was built for, separate tools usually work out better.
Get A Quotation For This Tool
Tell us your moulding grade, annual volume and target date and we will come back with a specification you can compare against any other offer.