Injection Moulds For Electronics And Audiovisual
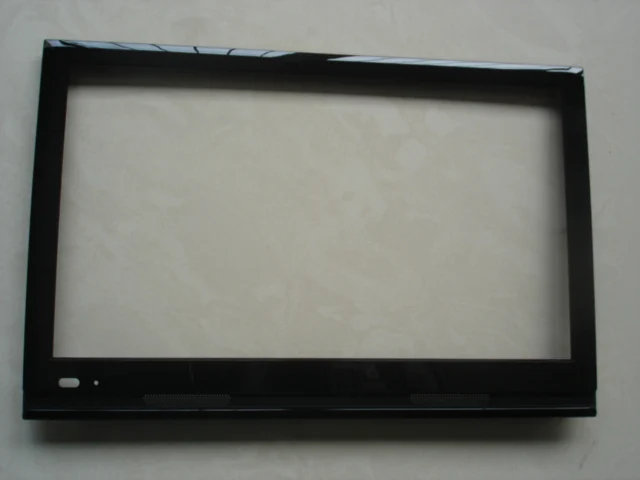
Television front shells, enclosures and electronic housings in PC and PC ABS
What Makes Electronics And Audiovisual Parts Difficult
A television bezel is a large thin wall part where the smallest sink mark reads as a defect across the whole front face
Cold runner gating on a wide part leaves a long flow path and an uneven pack, which shows up as a bow in the frame
Electronic housings often need six or more slides for connector and vent openings, and each one is a potential flash line
What Buyers In This Sector Need
- Hot runner or valve gate feeding when the part is too wide to fill evenly from one cold gate
- Cavity steel that stays stable at PC processing temperature
- Slide design that can be serviced in the press rather than needing the tool pulled every time
Recommended Products
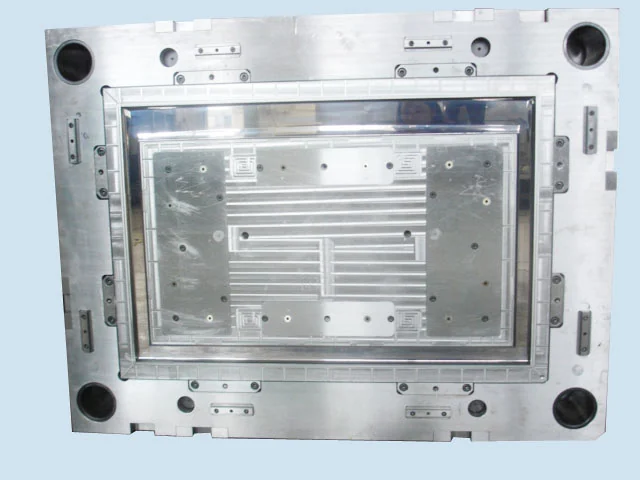
Moulds For Electronic And Audiovisual Parts
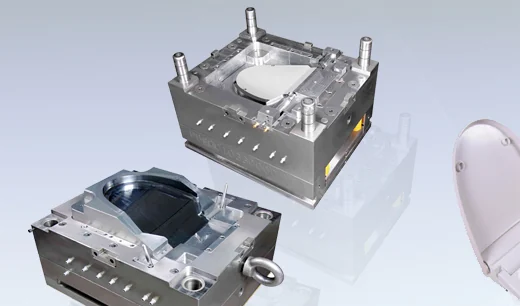
Hot Runner Mould With Valve Gate
The only hot runner tool in the archived catalogue
Product materials PC/ABSMould material SKD61
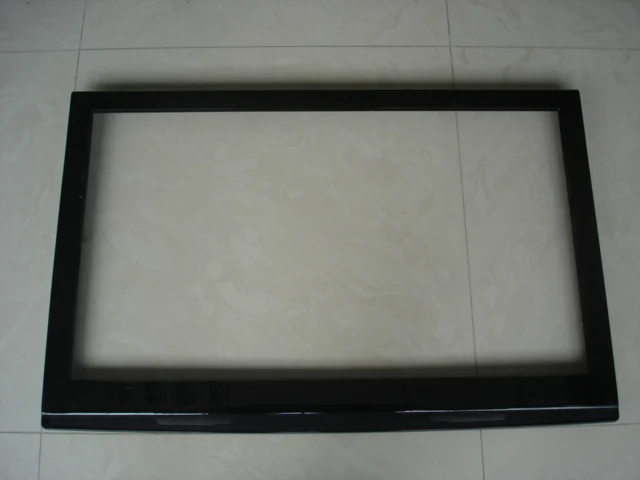
Moulds For Electronic And Audiovisual Parts
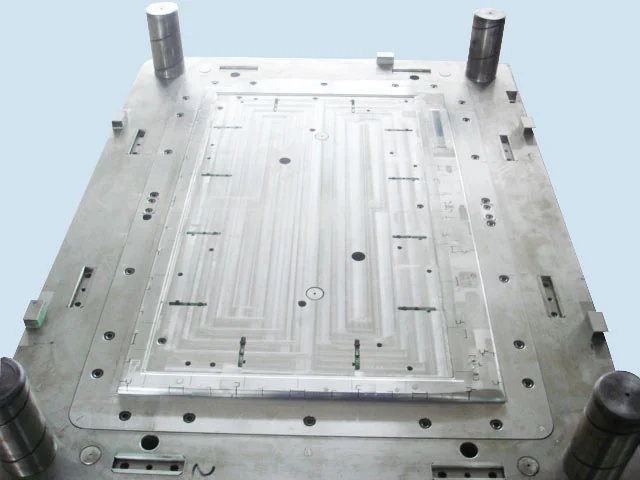
PC Electronic Series Mould With SKD61 Cavity Steel
SKD61 with a pinpoint gate for a cosmetic PC part
Product materials PCMould material SKD61
Moulds For Electronic And Audiovisual Parts
PC Electronic Part Mould With S136 Cavity Steel
No slides at all, which keeps flash risk near zero
Product materials PCMould material S136
Moulds For Electronic And Audiovisual Parts
ABS Electronic Part Mould With Two Cavities And Six Slides
Six slides across two impressions on a 60 second cycle
Product materials ABSMould material NAK80
Plastic Injection Moulded Parts
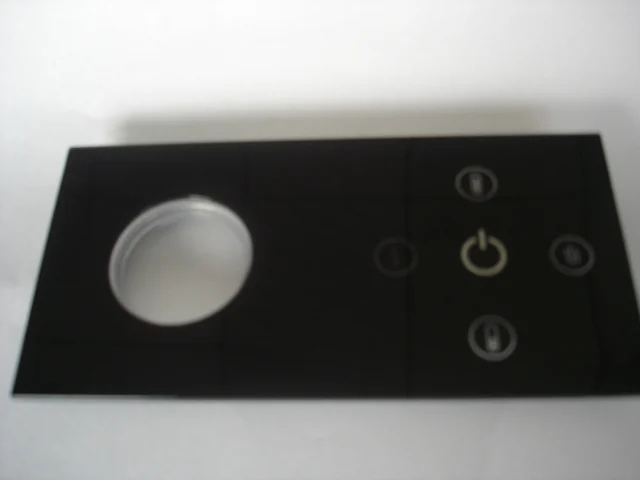
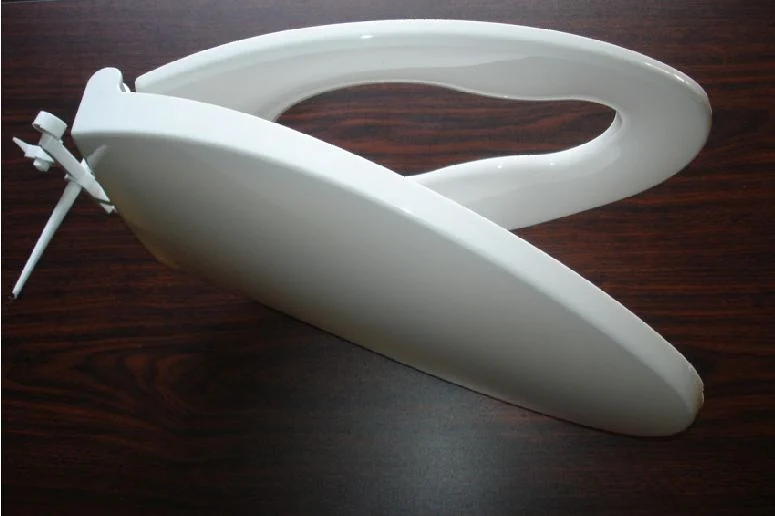
Moulded Television Front Shells
A wide gloss black part where every defect is visible
Typical Application Scenarios
A display assembler sourcing a front shell tool and wanting the trial parts checked on a flatness fixture before shipment
An electronics brand consolidating several small enclosure tools with one supplier
How A Project Runs
Design review
Part geometry, wall sections, draft and gate position are reviewed against the moulding material before any steel is cut.
Steel inspection
Cavity and core blocks are checked on arrival so that the hardness and grade match what the mould was quoted with.
In-process measurement
Machined inserts, slides and plates are measured between operations rather than only at the end of the tool room route.
Fitting and spotting
Parting line, slide movement and ejection are fitted by hand before the mould goes to the press.
Related Guides
Comparison Article
Hot Runner Or Cold Runner For Your Injection Mould
When the extra tool cost of a hot runner pays for itself, and when it is money spent on a manifold you then have to maintain.
Buying Guide
How Cycle Time Decides The Price Of A Moulded Part
The cycles in this catalogue run from 40 to 100 seconds. What drives that spread, and why it matters more than the tool price.
Material Guide
ABS PP PC And ASA For Moulded Industrial Parts
The four materials in this catalogue, what each is chosen for, and what changing between them does to the mould.
Electronics And Audiovisual Questions
What buyers in this sector ask before placing tooling work.
When is a hot runner worth the extra tool cost?
When the runner weight is a large share of the shot, when the flow path is too long to pack evenly, or when the gate has to sit in the middle of a cosmetic face. The archived hot runner mould runs a valve gate in PC ABS on a single cavity for exactly that reason.
How do you avoid sink marks on a large front shell?
Mostly by fixing the part rather than the tool: ribs are coredout to about half the wall, bosses are relieved, and the gate is put where the thick section is. What is left is handled by pack pressure and cooling layout, which is settled at the design review stage.
Tooling For Electronics And Audiovisual
Send the part, the moulding grade and the volume. We will name the cavity steel and the impression count in the quotation rather than after the order.