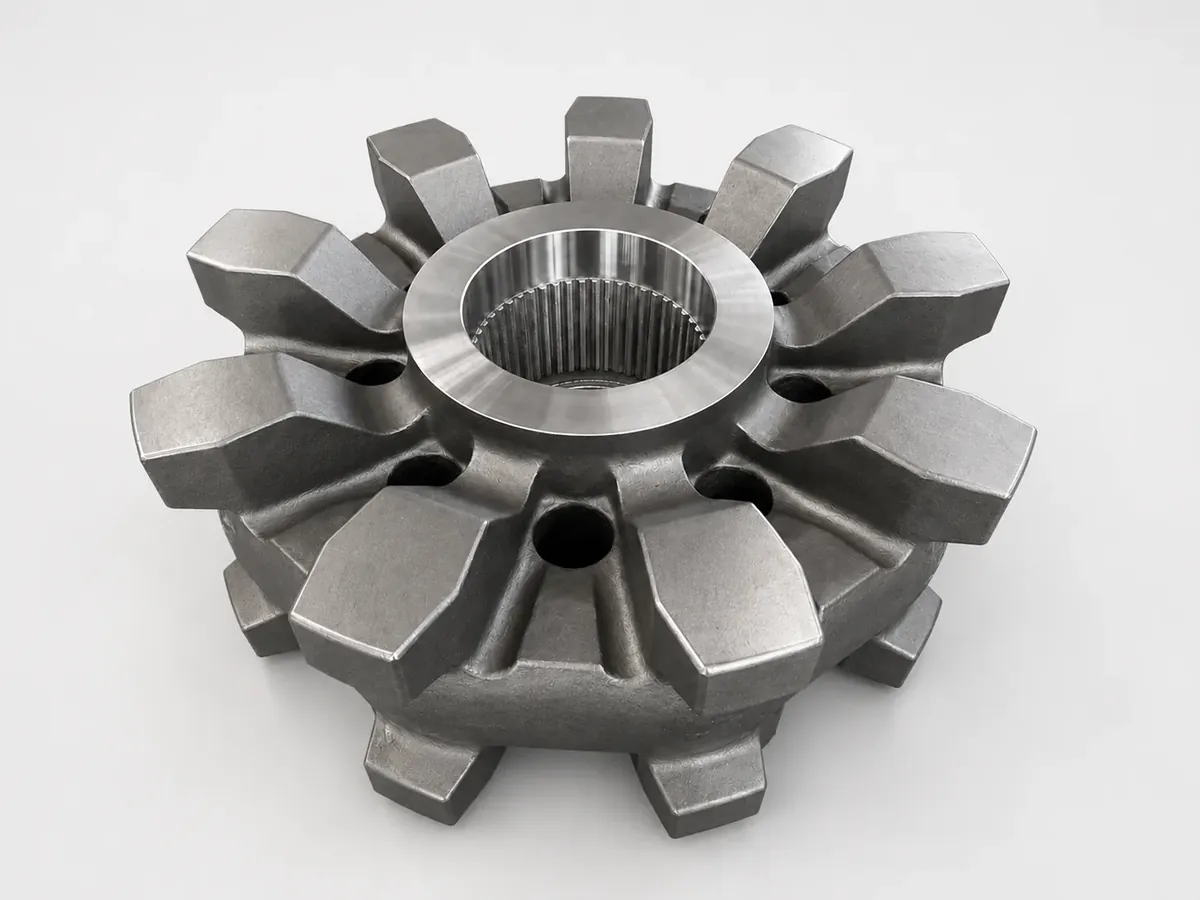
What This Part Is And Why It Is Made This Way
Wheel discs and impellers spin, so unbalanced mass and uneven wall thickness show up immediately as vibration. The casting has to reproduce the vane geometry consistently, batch after batch.
Parts are cast in steel grades and machined on the bore, the hub and the mounting faces, with dimensional inspection on the features that affect balance.
What You Get From This Route
Consistent vane geometry between batches keeps balance predictable.
Bore and hub machined on one setup to hold running accuracy.
Steel grade selected for the medium and the working temperature.
Application Scenarios
- Fan and blower impellers
- Pump impellers in abrasive service
- Mining and cement material handling wheels
- Drive wheel discs on heavy equipment
Who It Is For
- Fan, blower and pump manufacturers
- Plants replacing worn impellers in abrasive duty
- Equipment builders standardising rotating parts
Technical Features
- Steel casting with vaned geometry
- Machined bore, hub and mounting face
- Shell moulding or sand casting by batch size
- Dimensional inspection on balance critical features
What Buyers Run Into Without This Specification
- Wall thickness varies around the vanes and the wheel will not balance.
- The bore is machined off the casting datum and runs out on assembly.
- A replacement impeller does not match the original hub dimensions.
Published Material Weight And Process Data
Figures below are the published capability for steel castings and forgings. Part specific values — tolerance on individual features, finish, packing — are confirmed at drawing review and marked TBC until then.
| Material | 42CrMo4, G20Mn5, G26CrMo4, G18NiMoCr3-6, G22CrNi2Mo5-6, AISI 4340, AISI 4140, AISI 4325 and similar grades |
|---|---|
| Weight Range | Steel casting 50 kg - 20 T; forging 50 kg - 50 T |
| Process | Sand casting; shell moulding; open-die and closed-die forging; roll forging |
| Melting | High automation production lines with EAF + LF + VD / AOD melting routes |
| Tolerance | Zero draft sand casting to CT9 on automated heat treatment lines |
| Inspection | NDT with certified operators, single part certificates and quality document traceability |
| Part Specific Tolerance | TBC — confirmed against the customer drawing |
| Minimum Order Quantity | TBC — depends on the process route selected |
| Lead Time | TBC — confirmed with the production base at quotation |
How The Part Is Made And Checked
- Production — Highly automated production lines with EAF + LF + VD / AOD melting equipment.
- Quality — Certified NDT capability, supporting per-part certificates and traceable quality documents.
- Process Control — Automated heat treatment lines; zero draft sand casting reaches CT9.
Quality management is based on ISO 9001 and covers supplier management, raw material inspection, production process control and final inspection. Inspection results are archived and traceable.
Options And Alternatives
Parts are produced to the customer drawing rather than to a fixed catalogue item, so material grade, machining scope, surface treatment and packing are all specified per order. Machining, dimensional control, surface treatment and necessary pre-assembly can be added to the same supply route.
Where another process family would suit the part better — for example a forging in place of a casting for a shock loaded connector — that comparison is raised during drawing review rather than after tooling is committed.
How To Specify This Part
Say whether the wheel will be dynamically balanced and to which grade. That single requirement decides how tightly the wall thickness has to be controlled in the mould, and therefore whether shell moulding or sand casting is the right route.
- Send the drawing with material, quantity, quality standard and target delivery date.
- State the inspection class and the zones it applies to, rather than a general note.
- Confirm the packing requirement and the lifting equipment available at the destination.
Related Guides
Other Parts In This Range
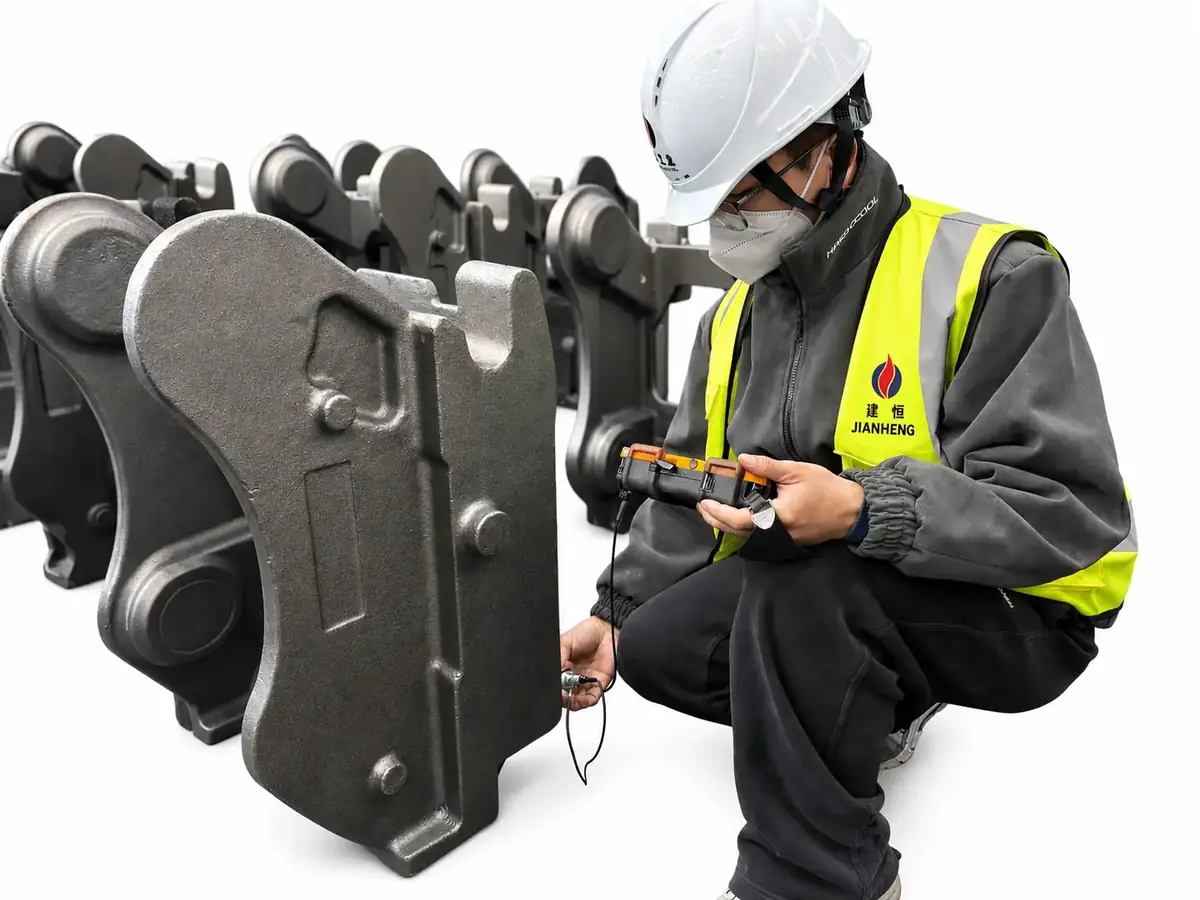
Large Steel Structural Castings
Load bearing steel castings up to 20 tonnes
View specifications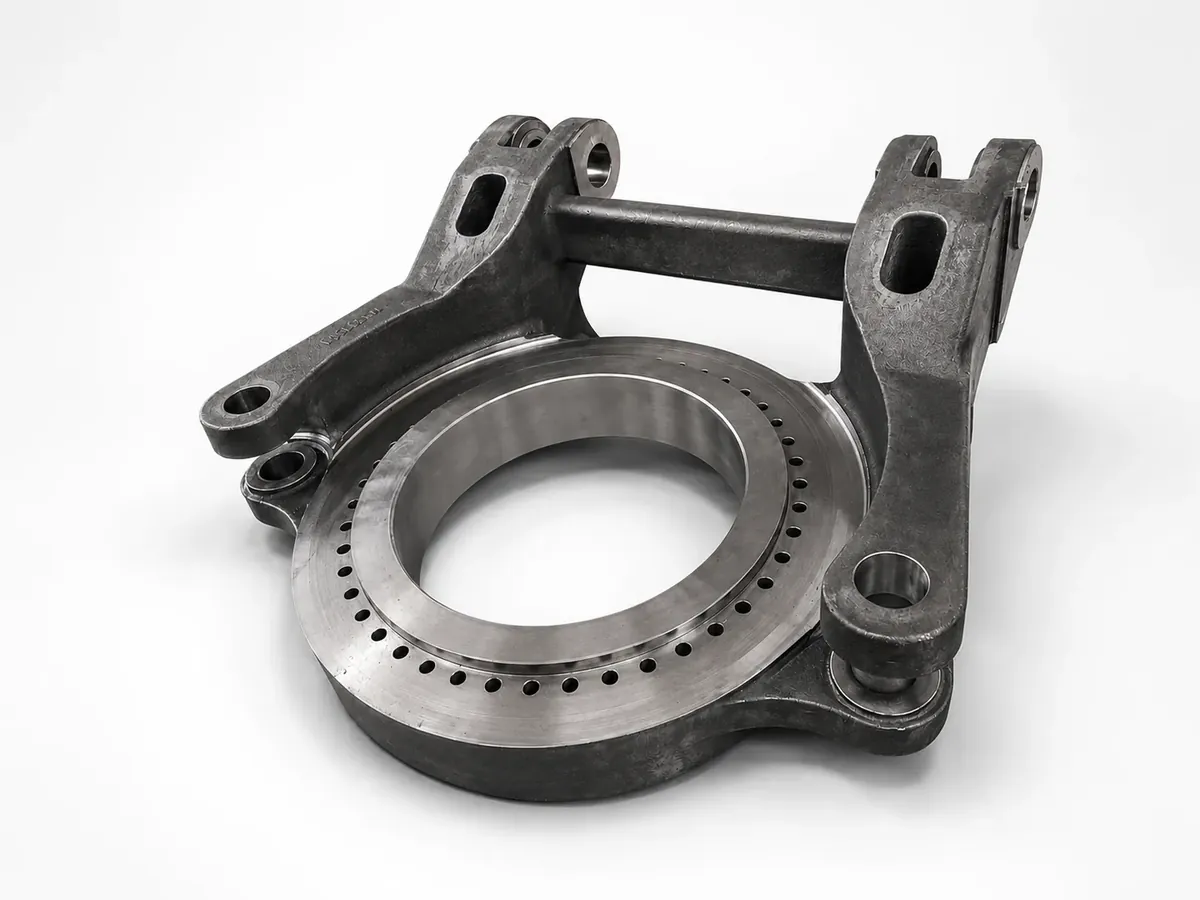
Slewing Support Structural Castings
Rotating support bodies with machined bearing seats
View specifications
Forged Shafts
Stepped shafts with continuous grain flow
View specifications
Flanges and Sleeve Components
Connection flanges and sleeve bodies
View specificationsWheel Discs and Impeller Components — Frequently Asked Questions
Can you reverse engineer a worn impeller?
A drawing is needed for production. If only a sample exists, 3D scanning is available in the group of inspection services to support dimensional verification during development.
Is dynamic balancing included?
Balancing is treated as a specified requirement. Please state the balance grade on the enquiry so it can be quoted as part of the process route.
What do you need to prepare a quotation?
Drawings, material, quantity, quality standard and target delivery date.
Which inspection is included?
The inspection scope is agreed during drawing review. Automated heat treatment lines; zero draft sand casting reaches CT9.
Get A Quotation For Wheel Discs and Impeller Components
Send the drawing and the application. We will confirm the process route, the production base and the inspection scope before quoting.