What This Part Is And Why It Is Made This Way
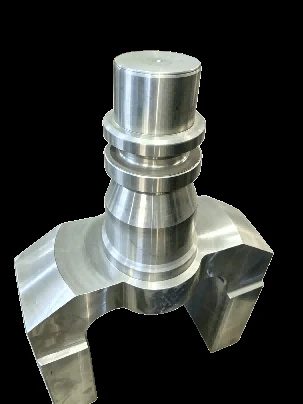
A die forged shaft comes out close to its finished shape with the grain flow following the contour, which is why it outlasts a shaft turned from bar in the same grade. The trade is tooling cost against fatigue life.
Shafts are forged on 300 T to 8000 T presses in weights from 0.2 kg to 100 kg, in carbon, alloy and stainless grades.
What You Get From This Route
Continuous metal flow line raises strength, reliability and service life.
Near net shape reduces machining stock and cycle time.
CMM and mechanical testing including -60 °C impact available.
Application Scenarios
- Transmission and drive shafts
- High volume shaft families
- Agricultural and construction machinery shafts
- Pump and compressor shafts
Who It Is For
- OEMs with repeating shaft volumes
- Designers upgrading a machined bar shaft that fails in fatigue
- Buyers needing certified mechanical properties
Technical Features
- Closed die forging on 300 T - 8000 T equipment
- Product weight 0.2 kg - 100 kg
- Grades C45E, 42CrMo4, 34CrNiMo6, 18CrNiMo7-6 and stainless options
- Suited to high batch, high precision, complex shape, high strength parts
What Buyers Run Into Without This Specification
- A bar turned shaft fails in fatigue at the shoulder radius.
- Machining stock is excessive and material cost dominates the part price.
- Low temperature impact requirements cannot be met by the current source.
Published Material Weight And Process Data
Figures below are the published capability for precision forging. Part specific values — tolerance on individual features, finish, packing — are confirmed at drawing review and marked TBC until then.
| Closed Die Forging | Equipment 300 T - 8000 T; product weight 0.2 kg - 100 kg |
|---|---|
| Rolled Ring Forging | Maximum diameter 9000 mm; ring, cone and cylinder shapes |
| Open Die Forging | No die cost, short development cycle, flexible size selection for large forgings |
| Carbon Steel | C22E / 20, C35E / 35, C45E / 45, C55E / 55 |
| Alloy Steel | 16MnCr5, 20MnCr5, 42CrMo4 / 42CrMo, 34CrNiMo6, 25CrMo4 / 25CrMo, 41Cr4 / 40Cr, 18CrNiMo7-6 |
| Stainless Steel | 1.4301 / 304, 1.4401 / 316, 1.4542 / 17-4PH, 1.4021 / 20Cr13, 1.4057 / 30Cr13 |
| Certificates | Production partners can support IATF 16949:2016 and ISO 9001:2015 |
| Part Specific Tolerance | TBC — confirmed against the customer drawing |
| Minimum Order Quantity | TBC — depends on the process route selected |
| Lead Time | TBC — confirmed with the production base at quotation |
How The Part Is Made And Checked
- CMM — Zeiss and Hexagon three coordinate measurement of critical dimensions and assembly positions.
- 3D Scan — Complex surfaces, contours and sample development stage dimensional verification.
- Mechanical — Tensile, hardness, -60 °C impact, metallographic and chemical composition testing.
- NDT — UT, MT, PT and RT non destructive testing.
- Ring Check — Leak testing, roughness, inner diameter and roundness related checks.
Quality management is based on ISO 9001 and covers supplier management, raw material inspection, production process control and final inspection. Inspection results are archived and traceable.
Options And Alternatives
Parts are produced to the customer drawing rather than to a fixed catalogue item, so material grade, machining scope, surface treatment and packing are all specified per order. Machining, dimensional control, surface treatment and necessary pre-assembly can be added to the same supply route.
Where another process family would suit the part better — for example a forging in place of a casting for a shock loaded connector — that comparison is raised during drawing review rather than after tooling is committed.
How To Specify This Part
Bring the annual quantity to the first conversation. Closed die forging pays back through tooling amortisation, so the volume — not the drawing — decides whether it beats machining from bar.
- Send the drawing with material, quantity, quality standard and target delivery date.
- State the inspection class and the zones it applies to, rather than a general note.
- Confirm the packing requirement and the lifting equipment available at the destination.
Related Guides
Other Parts In This Range
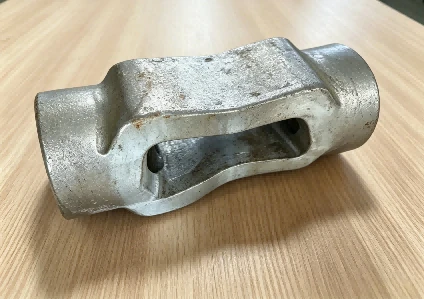
Closed Die Forged Connectors
High volume forged connection parts
View specifications
High Strength Connection and Lifting Components
Rated lifting and connection hardware
View specifications
Agricultural Machinery Forgings
Seasonal volume forgings for farm equipment
View specifications
Rolled Ring Forgings
Seamless rings to 9000 mm diameter
View specificationsPrecision Die Forged Shafts — Frequently Asked Questions
What press capacity is available?
Closed die forging equipment ranges from 300 T to 8000 T, covering product weights from 0.2 kg to 100 kg.
Can low temperature impact properties be certified?
Mechanical testing covers tensile, hardness, -60 °C impact, metallographic and chemical composition testing.
What do you need to prepare a quotation?
Drawings, material, quantity, quality standard and target delivery date.
Which inspection is included?
The inspection scope is agreed during drawing review. Leak testing, roughness, inner diameter and roundness related checks.
Get A Quotation For Precision Die Forged Shafts
Send the drawing and the application. We will confirm the process route, the production base and the inspection scope before quoting.