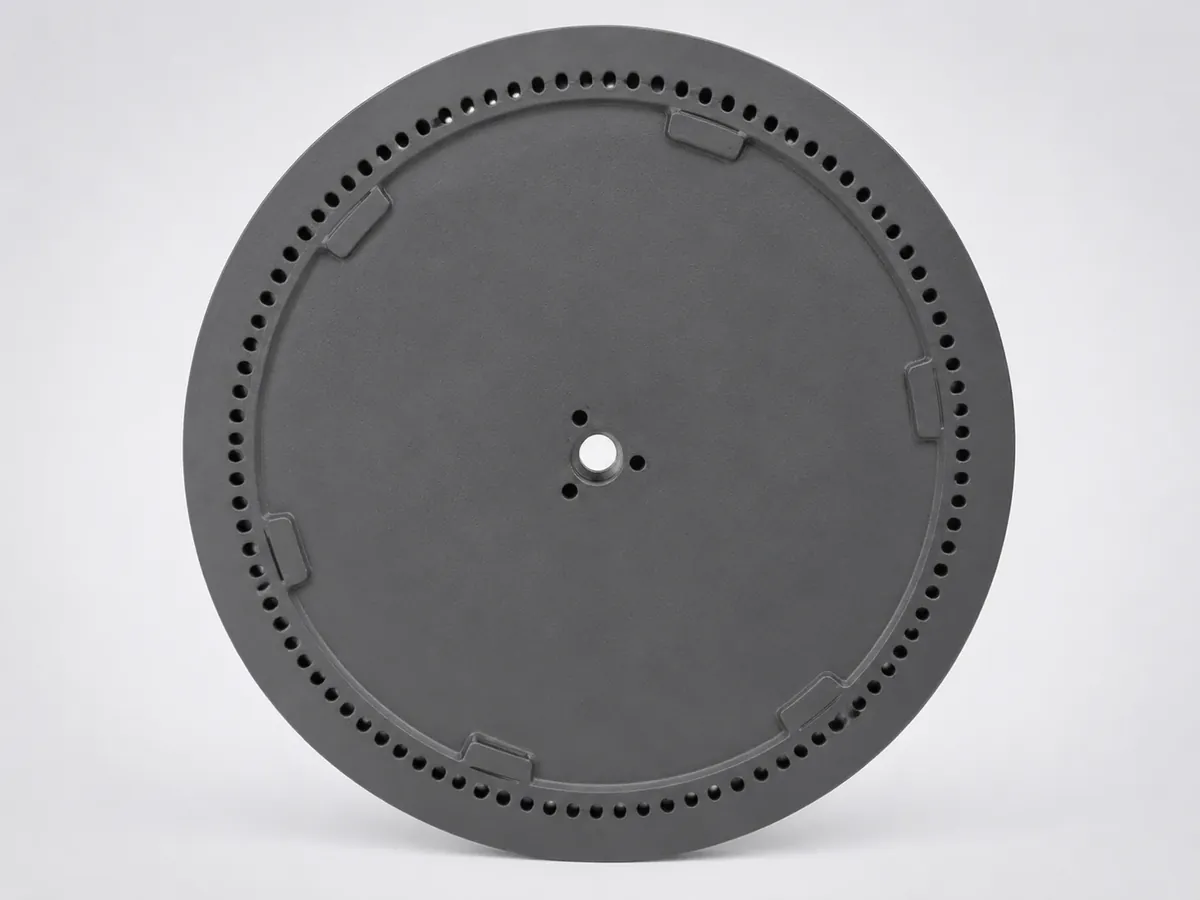
What This Part Is And Why It Is Made This Way
Flat iron castings look simple and are not: a large flat section cools unevenly and warps, and flatness is usually the acceptance criterion. Moulding route and cooling control matter more than the grade.
Disc type castings are produced in grey and ductile iron, with the moulding route chosen for dimensional stability on flat sections.
What You Get From This Route
Resin sand route available where dimensional stability beats cycle time.
Grey iron damping suits discs in vibration exposed positions.
Machining allowance planned so flat faces clean up without distortion.
Application Scenarios
- Cover and end plates
- Brake and friction discs in industrial equipment
- Machine base plates
- Flat sealing and mounting discs
Who It Is For
- Equipment builders with large flat components
- Buyers rejecting parts on flatness
- Designers converting plate fabrications to castings
Technical Features
- Grey iron EN-GJL-150 to 300 and ductile iron grades
- Green sand, resin sand and shell processes
- Weight 0.2 kg - 2000 kg
- Route selected for dimensional stability on flat sections
What Buyers Run Into Without This Specification
- Large flat castings warp and cannot be machined flat within allowance.
- Green sand tooling is chosen for a part that needs resin sand stability.
- Flatness is not specified and every batch is argued over.
Published Material Weight And Process Data
Figures below are the published capability for cast iron. Part specific values — tolerance on individual features, finish, packing — are confirmed at drawing review and marked TBC until then.
| Grey Iron | EN-GJL-150 / 200 / 250 / 300 |
|---|---|
| Ductile Iron | EN-GJS-400 / 450 / 500 / 600 / 700 / 800 |
| ADI | ADI800-10 / ADI1200-3 |
| Weight Range | 0.2 kg - 2000 kg |
| Process | Green sand process; resin sand process; shell process |
| Selection Basis | Grade and moulding route matched to customer drawing and application scenario |
| Part Specific Tolerance | TBC — confirmed against the customer drawing |
| Minimum Order Quantity | TBC — depends on the process route selected |
| Lead Time | TBC — confirmed with the production base at quotation |
How The Part Is Made And Checked
- Green Sand — High volume production of repeat parts at the lowest tooling cost.
- Resin Sand — Larger parts and complex cavities where dimensional stability matters more than cycle time.
- Shell Process — Better surface and dimensional accuracy for mid size batches.
Quality management is based on ISO 9001 and covers supplier management, raw material inspection, production process control and final inspection. Inspection results are archived and traceable.
Options And Alternatives
Parts are produced to the customer drawing rather than to a fixed catalogue item, so material grade, machining scope, surface treatment and packing are all specified per order. Machining, dimensional control, surface treatment and necessary pre-assembly can be added to the same supply route.
Where another process family would suit the part better — for example a forging in place of a casting for a shock loaded connector — that comparison is raised during drawing review rather than after tooling is committed.
How To Specify This Part
Put a flatness tolerance on the drawing and say whether it applies as cast or after machining. For flat iron castings that distinction changes the moulding route, the allowance and the price.
- Send the drawing with material, quantity, quality standard and target delivery date.
- State the inspection class and the zones it applies to, rather than a general note.
- Confirm the packing requirement and the lifting equipment available at the destination.
Related Guides
Other Parts In This Range
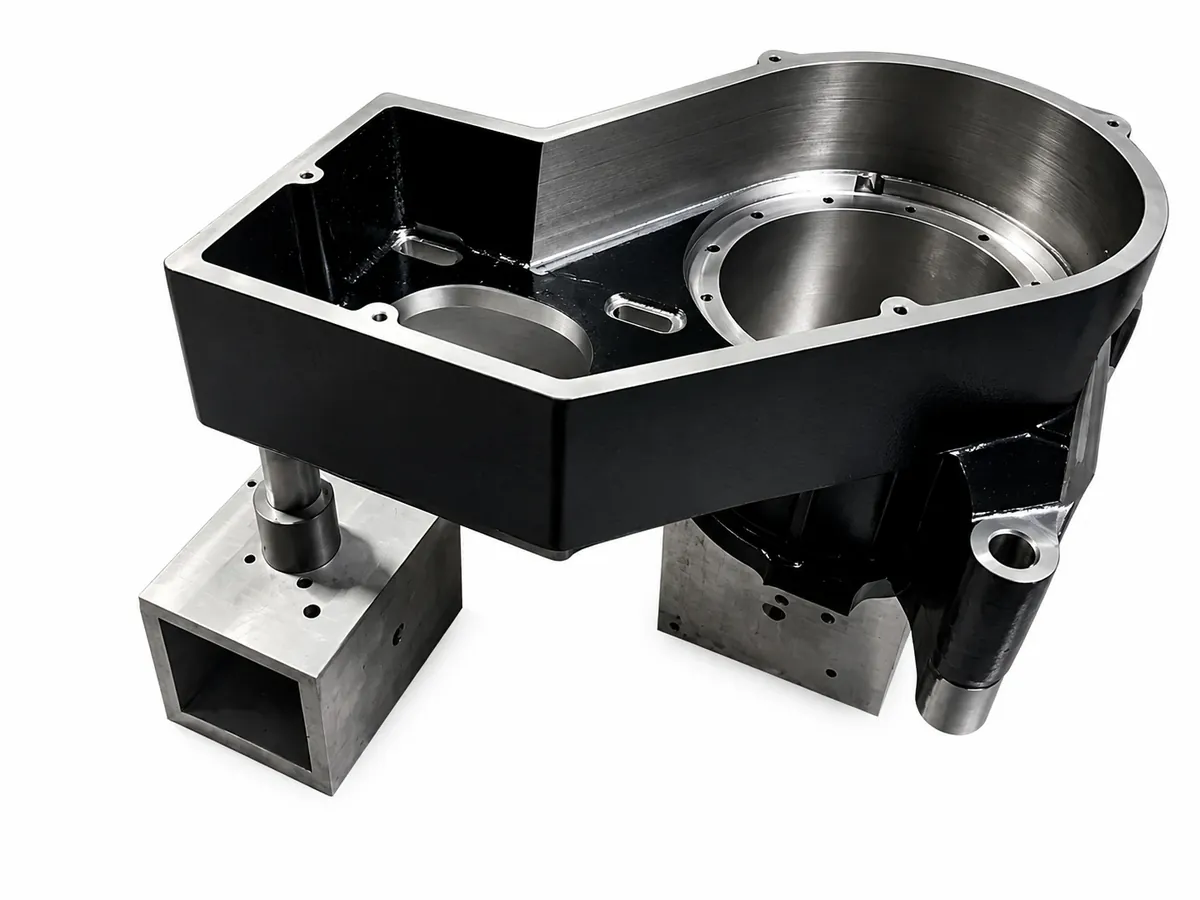
Mechanical Wear and Conveying Components
Screws, flights and wear surfaces
View specifications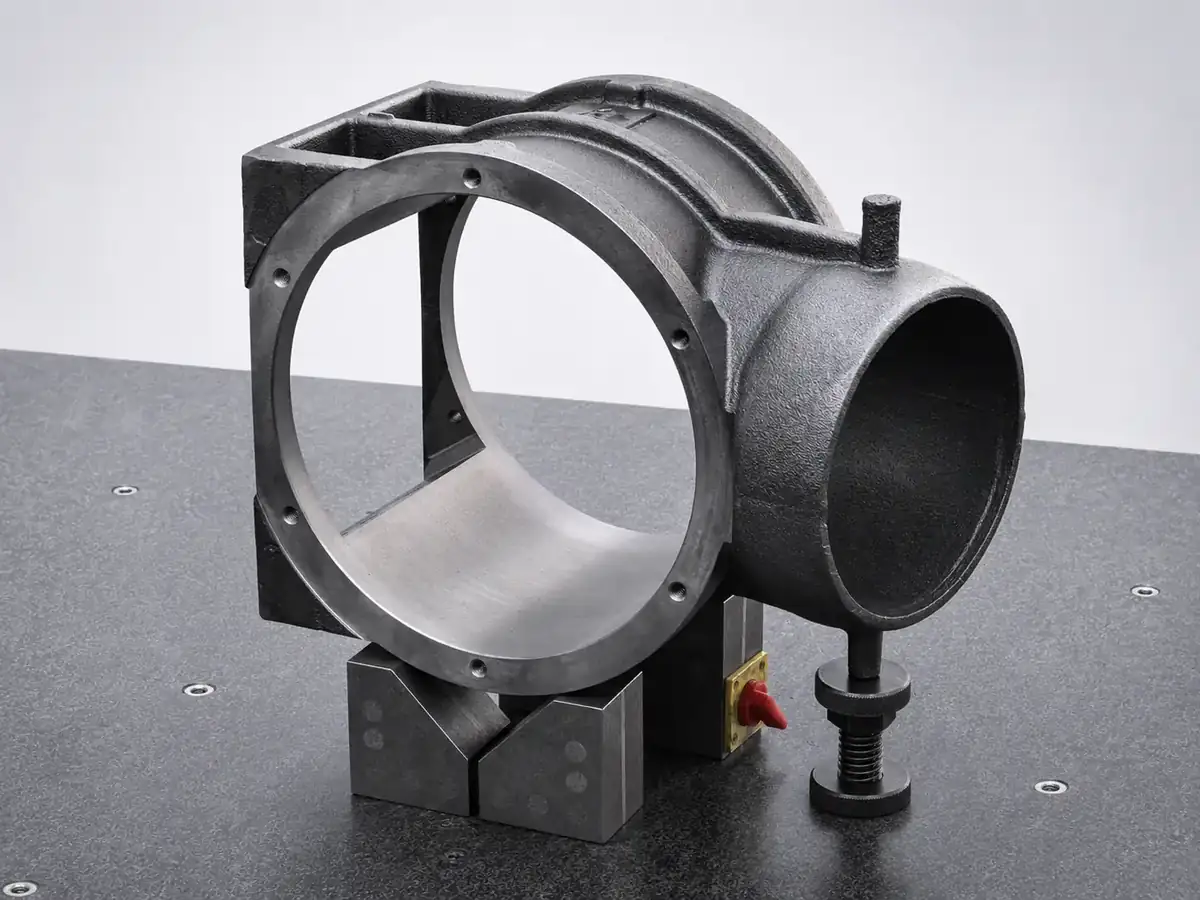
Ductile Iron Structural Brackets
Ductile iron support structures
View specifications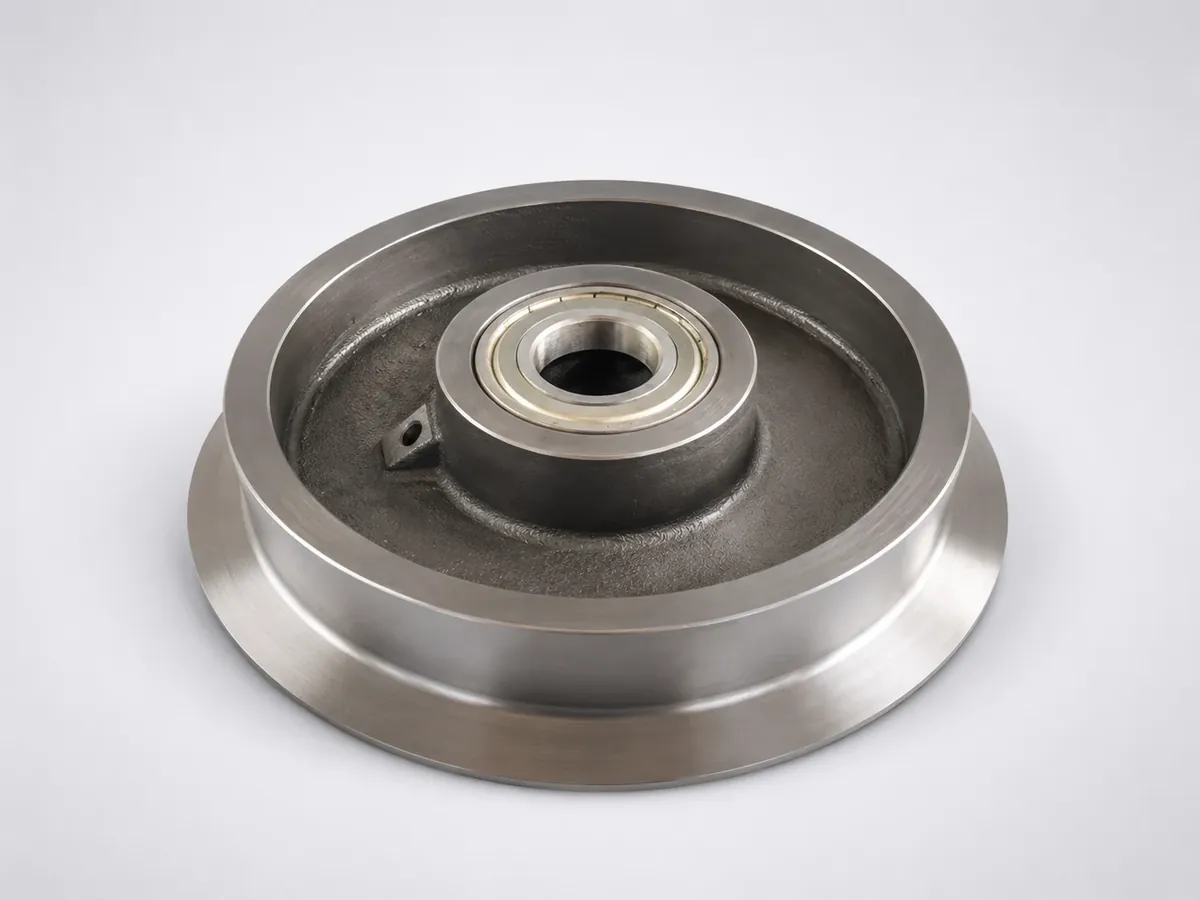
Wheel and Transmission Components
Pulleys, wheels and drive iron parts
View specifications
Disc Base Iron Castings
Base plates with integral bosses
View specificationsDisc Type Iron Castings — Frequently Asked Questions
Which process suits large flat castings?
Resin sand is normally proposed for larger parts and complex cavities where dimensional stability matters more than cycle time.
Can you machine the faces flat?
Machining is coordinated in the same supply chain, so parts can be supplied raw or machined to the drawing.
What do you need to prepare a quotation?
Drawings, material, quantity, quality standard and target delivery date.
Which inspection is included?
The inspection scope is agreed during drawing review. Better surface and dimensional accuracy for mid size batches.
Get A Quotation For Disc Type Iron Castings
Send the drawing and the application. We will confirm the process route, the production base and the inspection scope before quoting.