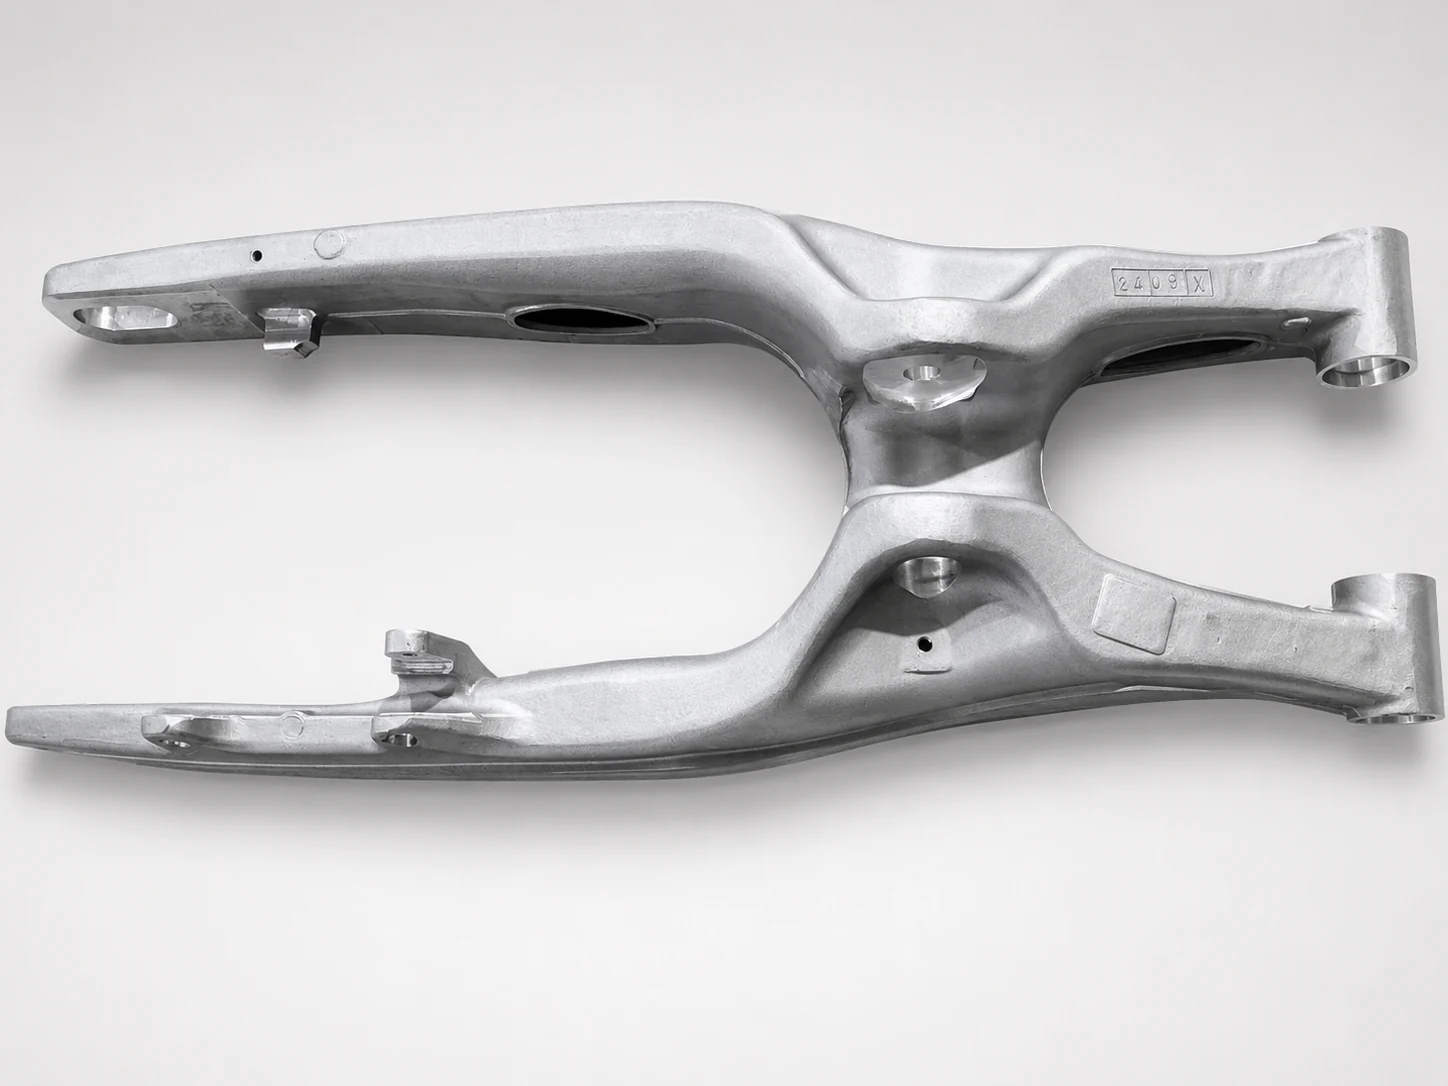
Lightweight Structural Components
Weight reduction without losing section strength
What This Part Is And Why It Is Made This Way
Switching a structural part from steel to aluminium only pays off if the section is redesigned at the same time — a direct material swap usually ends up heavier than necessary and weaker than intended. The casting route has to match the new section.
Lightweight structures are cast in grades such as EN AC-42100 (A356) and AlSi10Mg, with F, T4 or T6 heat treatment.
What You Get From This Route
T6 heat treatment raises strength so sections can stay thin.
Four casting routes available, so the process follows the design instead of limiting it.
Machining, welding and surface treatment coordinated in the same supply chain.
Application Scenarios
- Machine arms and swing components
- Portable equipment structures
- Transport equipment structural parts
- Robotic and automation structures
Who It Is For
- Designers converting steel parts to aluminium
- Equipment builders with weight or inertia targets
- OEMs reducing shipping weight on exported machines
Technical Features
- Materials EN AC-42100 (A356), EN AC-43000 (AlSi10Mg), A380, ADC12
- Heat treatment F, T4, T6
- Gravity die casting CT7-CT8 with 3 mm minimum wall
- Low pressure die casting CT7-CT8 with 2.5 mm minimum wall
What Buyers Run Into Without This Specification
- A direct steel to aluminium swap ends up heavy and still fails.
- The chosen casting route cannot fill the thin sections the design needs.
- Heat treatment is skipped and mechanical properties fall short.
Published Material Weight And Process Data
Figures below are the published capability for aluminum alloy casting. Part specific values — tolerance on individual features, finish, packing — are confirmed at drawing review and marked TBC until then.
| Material | ADC12, A380, EN AC-42100 (A356), EN AC-43000 (AlSi10Mg), EN AC-46000, EN AC-46100 |
|---|---|
| Heat Treatment | F, T4, T6 |
| Process | Sand casting; gravity die casting; high pressure die casting; low pressure metal and sand die casting |
| Gravity Die Casting | 5-15 min per part; min wall 3 mm; CT7-CT8; Ra 6.3-12.5 μm; batch 500-20k pcs |
| High Pressure Die Casting | 15-60 sec per part; min wall 0.8 mm; CT4-CT6; Ra 3.2-6.3 μm; batch 1k-100k pcs |
| Low Pressure Die Casting | 3-8 min per part; min wall 2.5 mm; CT7-CT8; Ra 6.3-12.5 μm; batch 100-10k pcs |
| Sand and Low Pressure Sand | 2-48 hours per part; min wall 3-6 mm; CT10-CT11; Ra 12.5-25 μm; batch 1-1000 pcs |
| Part Specific Tolerance | TBC — confirmed against the customer drawing |
| Minimum Order Quantity | TBC — depends on the process route selected |
| Lead Time | TBC — confirmed with the production base at quotation |
How The Part Is Made And Checked
- Secondary Process — Machining and forming, welding, extrusion, forging and CNC machining.
- Surface Treatment — Painting, coating and anodising.
- Quality Inspection — X-ray for internal defects, 3D scanning for complex surfaces, spectrum analysis for composition, pressure testing for housings, CMM for critical dimensions and film thickness for coatings.
Quality management is based on ISO 9001 and covers supplier management, raw material inspection, production process control and final inspection. Inspection results are archived and traceable.
Options And Alternatives
Parts are produced to the customer drawing rather than to a fixed catalogue item, so material grade, machining scope, surface treatment and packing are all specified per order. Machining, dimensional control, surface treatment and necessary pre-assembly can be added to the same supply route.
Where another process family would suit the part better — for example a forging in place of a casting for a shock loaded connector — that comparison is raised during drawing review rather than after tooling is committed.
How To Specify This Part
Bring the load case to the drawing review, not just the existing steel drawing. Redesigning the section for aluminium and then choosing the casting route is what delivers the weight saving; doing it the other way round rarely works.
- Send the drawing with material, quantity, quality standard and target delivery date.
- State the inspection class and the zones it applies to, rather than a general note.
- Confirm the packing requirement and the lifting equipment available at the destination.
Related Guides
Other Parts In This Range
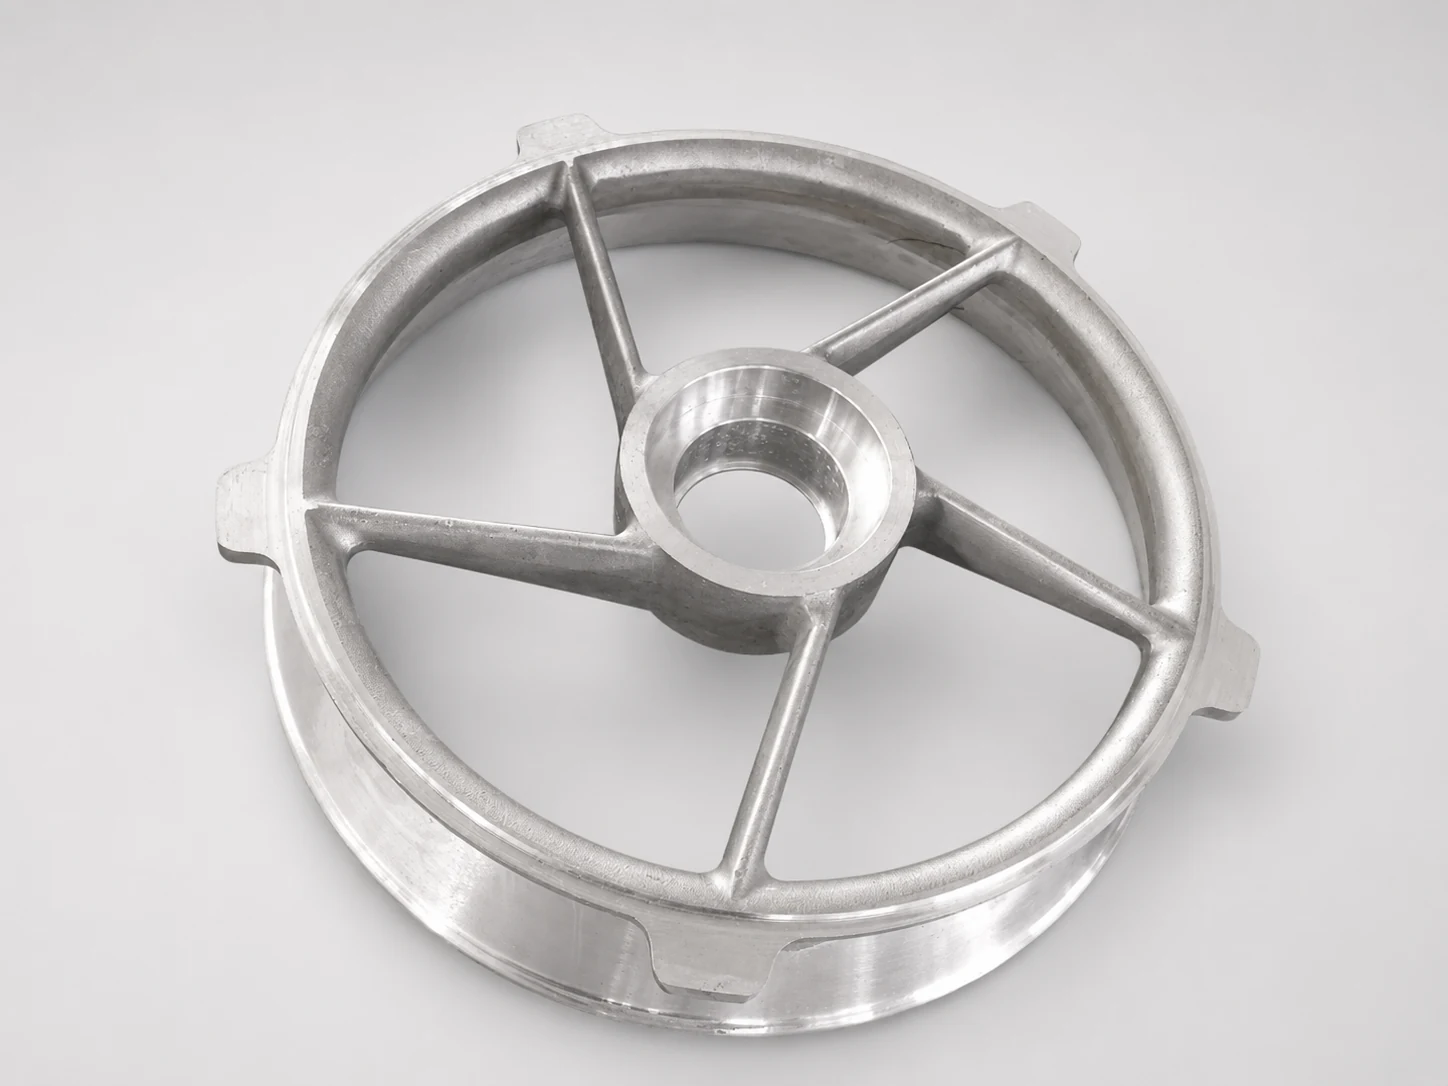
Wheel Discs and Rotating Components
Spoked discs and rotating aluminium parts
View specifications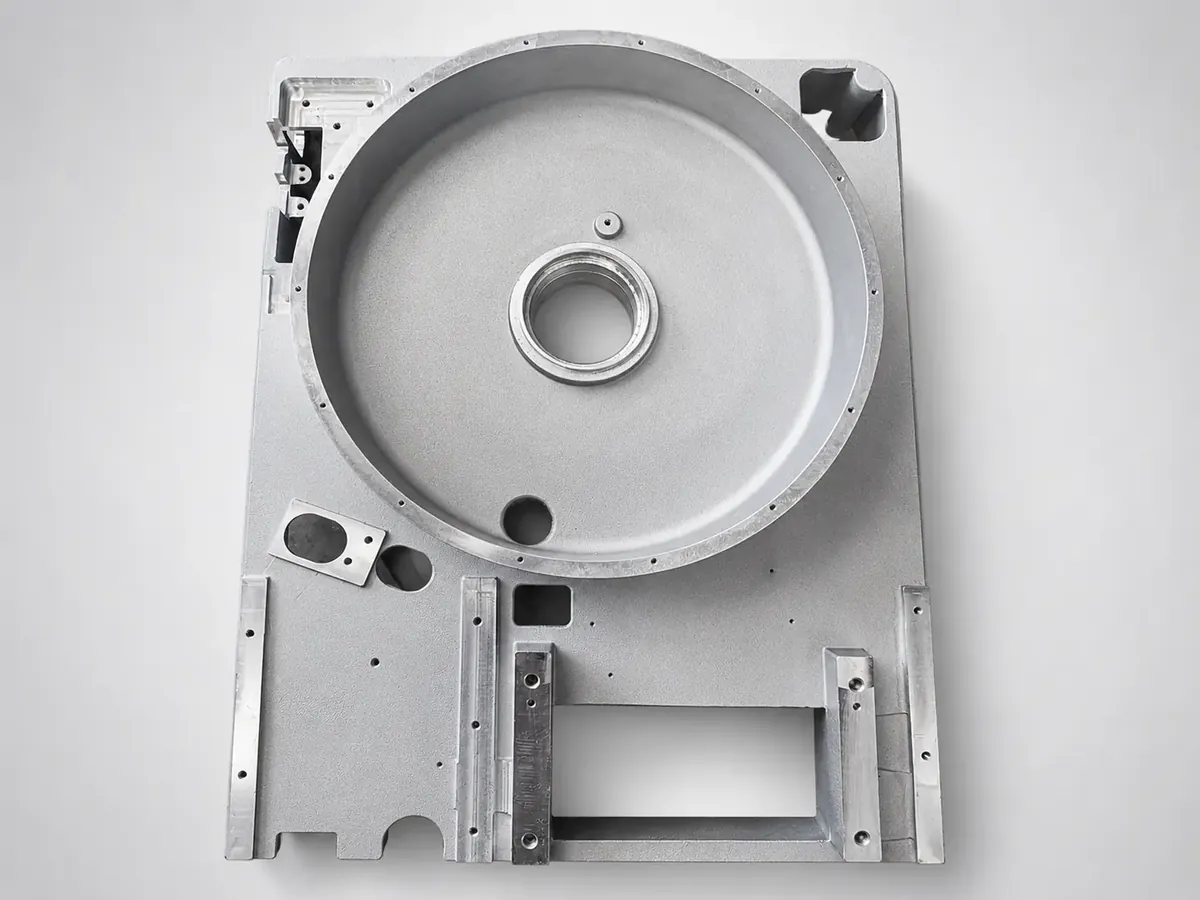
Aluminum Housing Components
Enclosures, covers and pressure tight housings
View specifications
Frames and Appearance Components
Visible frames and finished surfaces
View specifications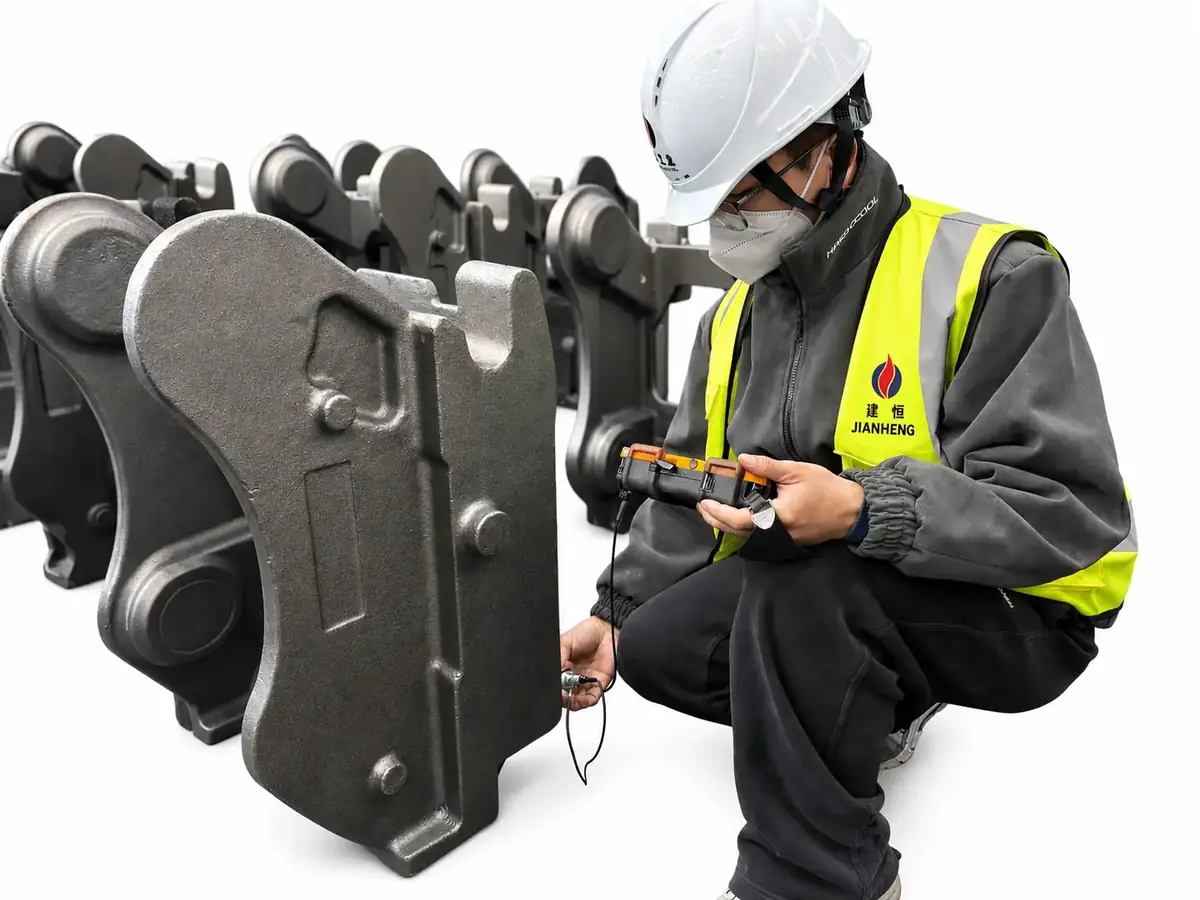
Large Steel Structural Castings
Load bearing steel castings up to 20 tonnes
View specificationsLightweight Structural Components — Frequently Asked Questions
Which aluminium casting route suits structural parts?
Gravity die casting and low pressure die casting are generally proposed for structural parts, because both give CT7-CT8 tolerance with good integrity. Low pressure suits parts needing higher strength and pressure tightness.
Is heat treatment available?
Yes. F, T4 and T6 conditions are available across the aluminium alloy business.
What do you need to prepare a quotation?
Drawings, material, quantity, quality standard and target delivery date.
Which inspection is included?
The inspection scope is agreed during drawing review. X-ray for internal defects, 3D scanning for complex surfaces, spectrum analysis for composition, pressure testing for housings, CMM for critical dimensions and film thickness for coatings.
Get A Quotation For Lightweight Structural Components
Send the drawing and the application. We will confirm the process route, the production base and the inspection scope before quoting.