What This Part Is And Why It Is Made This Way
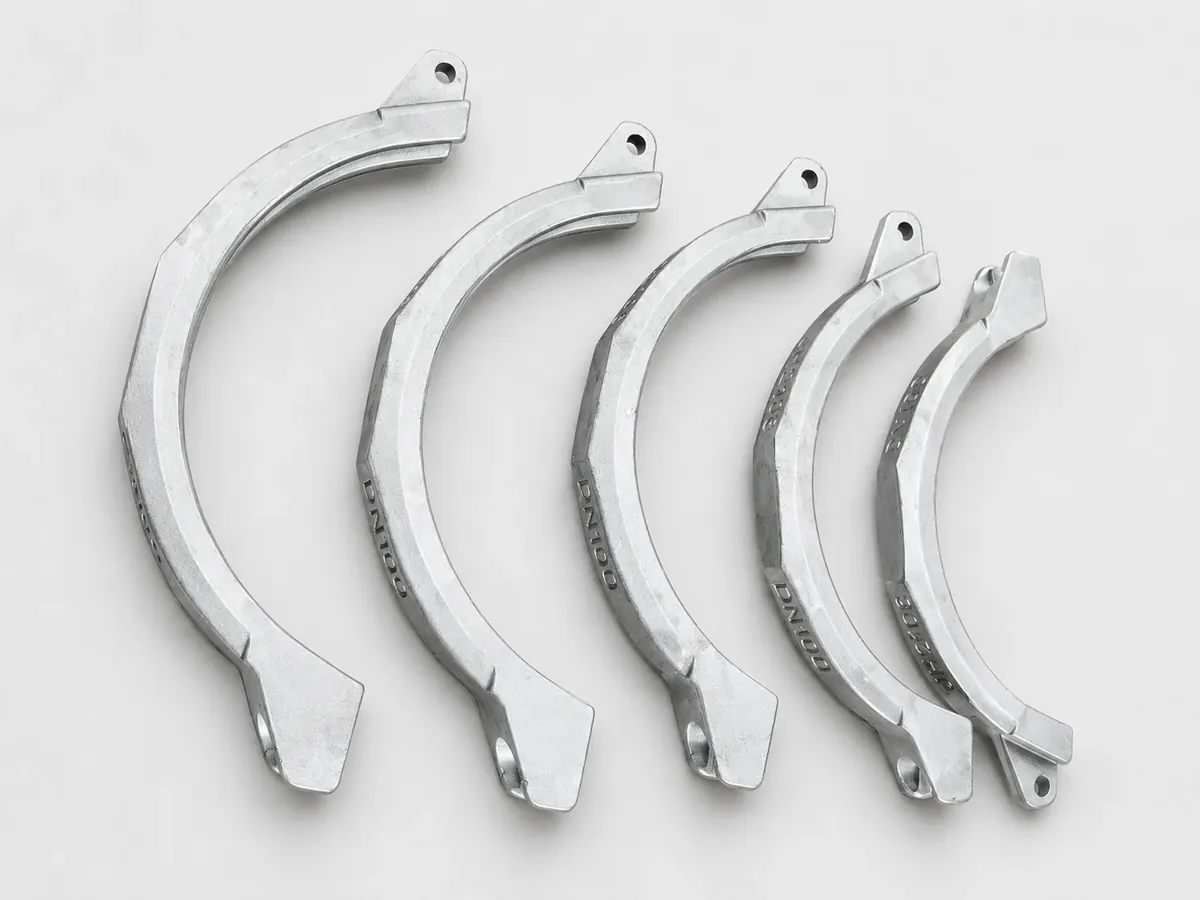
Thin walls are the hardest thing to cast well: metal freezes before it fills, and what survives the mould often distorts on cooling. The silica sol lost wax process exists precisely to make thin, curved sections repeatable.
These components are produced from 0.01 kg upwards at CT5 - CT9 tolerance and Ra 3.2 - Ra 6.3 surface, in grades including 1.4304, 1.4308 and 2Cr13.
What You Get From This Route
Silica sol shell reproduces thin sections that sand casting cannot fill reliably.
CT5 - CT9 tolerance means most features need no machining at all.
Ra 3.2 - Ra 6.3 as cast surface removes a polishing operation.
Application Scenarios
- Equipment covers and swept guards
- Curved handling and guiding components
- Instrument and valve internals
- Light structural brackets with formed profiles
Who It Is For
- Designers replacing fabricated sheet assemblies with a single casting
- Buyers paying too much for machining on curved surfaces
- OEMs needing consistent appearance parts
Technical Features
- Silica sol lost wax process
- Tolerance CT5 - CT9
- Surface Ra 3.2 - Ra 6.3
- Size range 2 mm - 2000 mm
What Buyers Run Into Without This Specification
- A fabricated assembly of bent parts is slow to build and never quite consistent.
- Machining a curved profile from solid wastes most of the material.
- Thin sections from a sand foundry come out incomplete or distorted.
Published Material Weight And Process Data
Figures below are the published capability for precision casting. Part specific values — tolerance on individual features, finish, packing — are confirmed at drawing review and marked TBC until then.
| Material | 1.4304 / 1.4308 / ASTM 8620 / 2Cr13 / 20Mn5 / 42CrMo4 / S355 |
|---|---|
| Weight Range | 0.01 kg - 300 kg |
| Process | Silica sol lost wax process |
| Tolerance Grade | CT5 - CT9 |
| Surface Roughness | Ra 3.2 - Ra 6.3 |
| Size Range | 2 mm - 2000 mm |
| Quick-Drying Route | 1 kg - 80 kg in G20Mn5+N / S355 / 42CrMo4 / G26CrMo4+QT1 / S690QL / GE300 |
| Part Specific Tolerance | TBC — confirmed against the customer drawing |
| Minimum Order Quantity | TBC — depends on the process route selected |
| Lead Time | TBC — confirmed with the production base at quotation |
How The Part Is Made And Checked
- Merged Scope — The precision casting scope now includes the former investment casting business, so one route covers both silica sol lost wax and quick-drying investment casting.
- Application Fit — Parts where appearance, assembly and dimensional consistency are demanding.
- Materials Covered — Carbon steel, low alloy steel, stainless steel and quenched and tempered grades.
Quality management is based on ISO 9001 and covers supplier management, raw material inspection, production process control and final inspection. Inspection results are archived and traceable.
Options And Alternatives
Parts are produced to the customer drawing rather than to a fixed catalogue item, so material grade, machining scope, surface treatment and packing are all specified per order. Machining, dimensional control, surface treatment and necessary pre-assembly can be added to the same supply route.
Where another process family would suit the part better — for example a forging in place of a casting for a shock loaded connector — that comparison is raised during drawing review rather than after tooling is committed.
How To Specify This Part
Mark the minimum wall thickness and the surfaces that must stay as cast. On thin curved parts the wall thickness decides feasibility, and stating which surfaces will not be machined lets the pattern be designed to leave them clean.
- Send the drawing with material, quantity, quality standard and target delivery date.
- State the inspection class and the zones it applies to, rather than a general note.
- Confirm the packing requirement and the lifting equipment available at the destination.
Related Guides
Other Parts In This Range
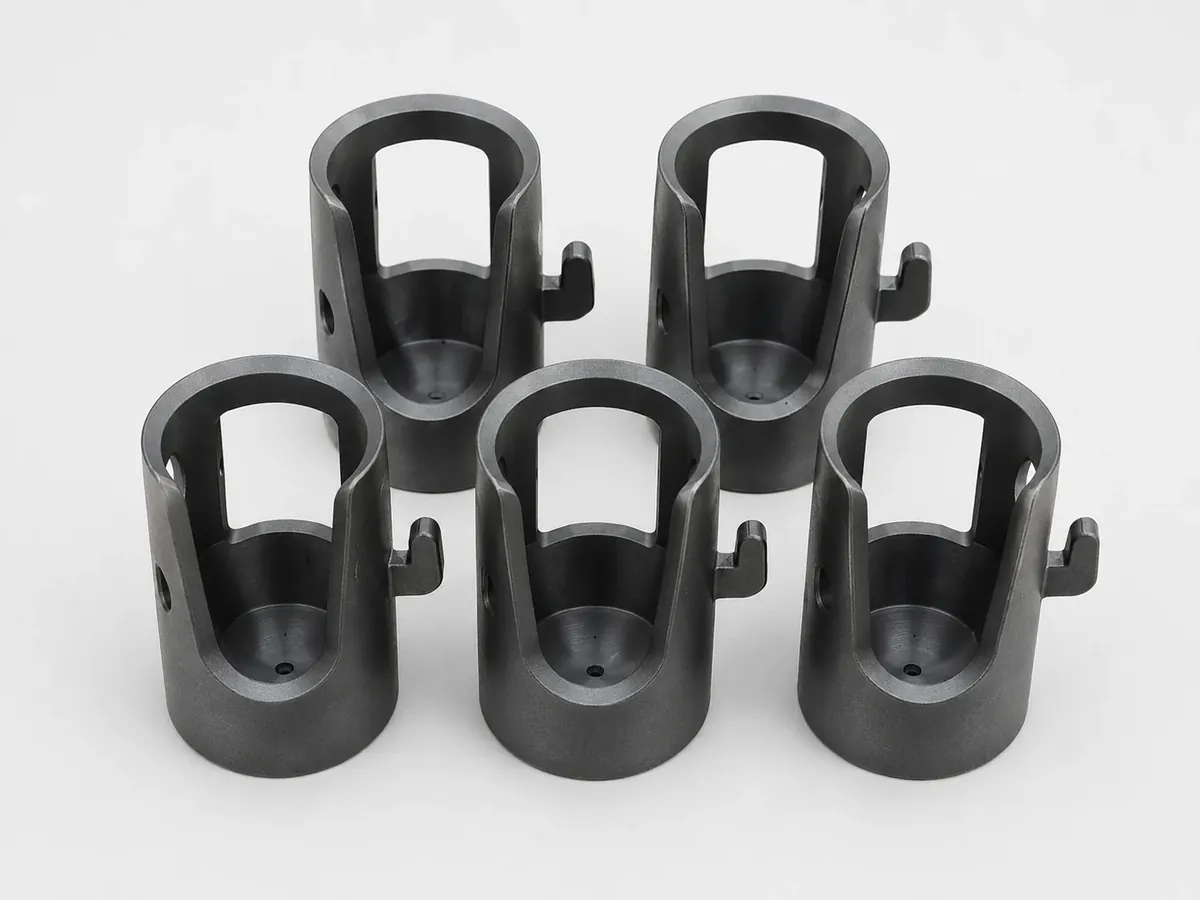
Lifting and Connection Components
Eyes, links and load carrying connectors
View specifications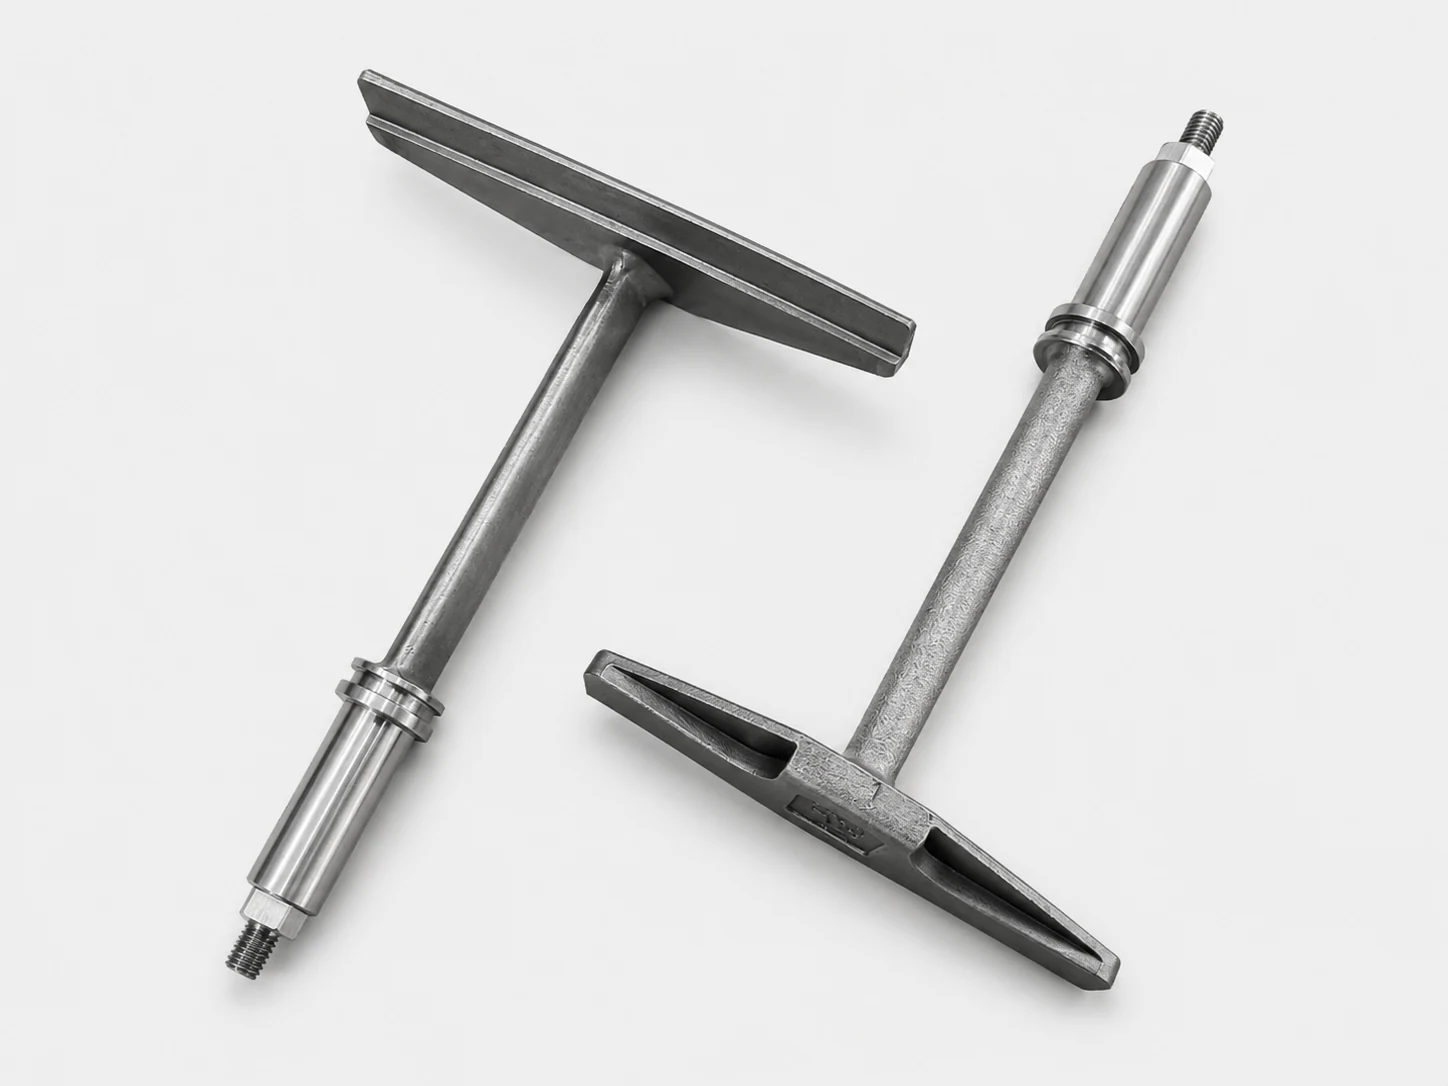
Shaft and Operating Components
Levers, spindles and actuating parts
View specifications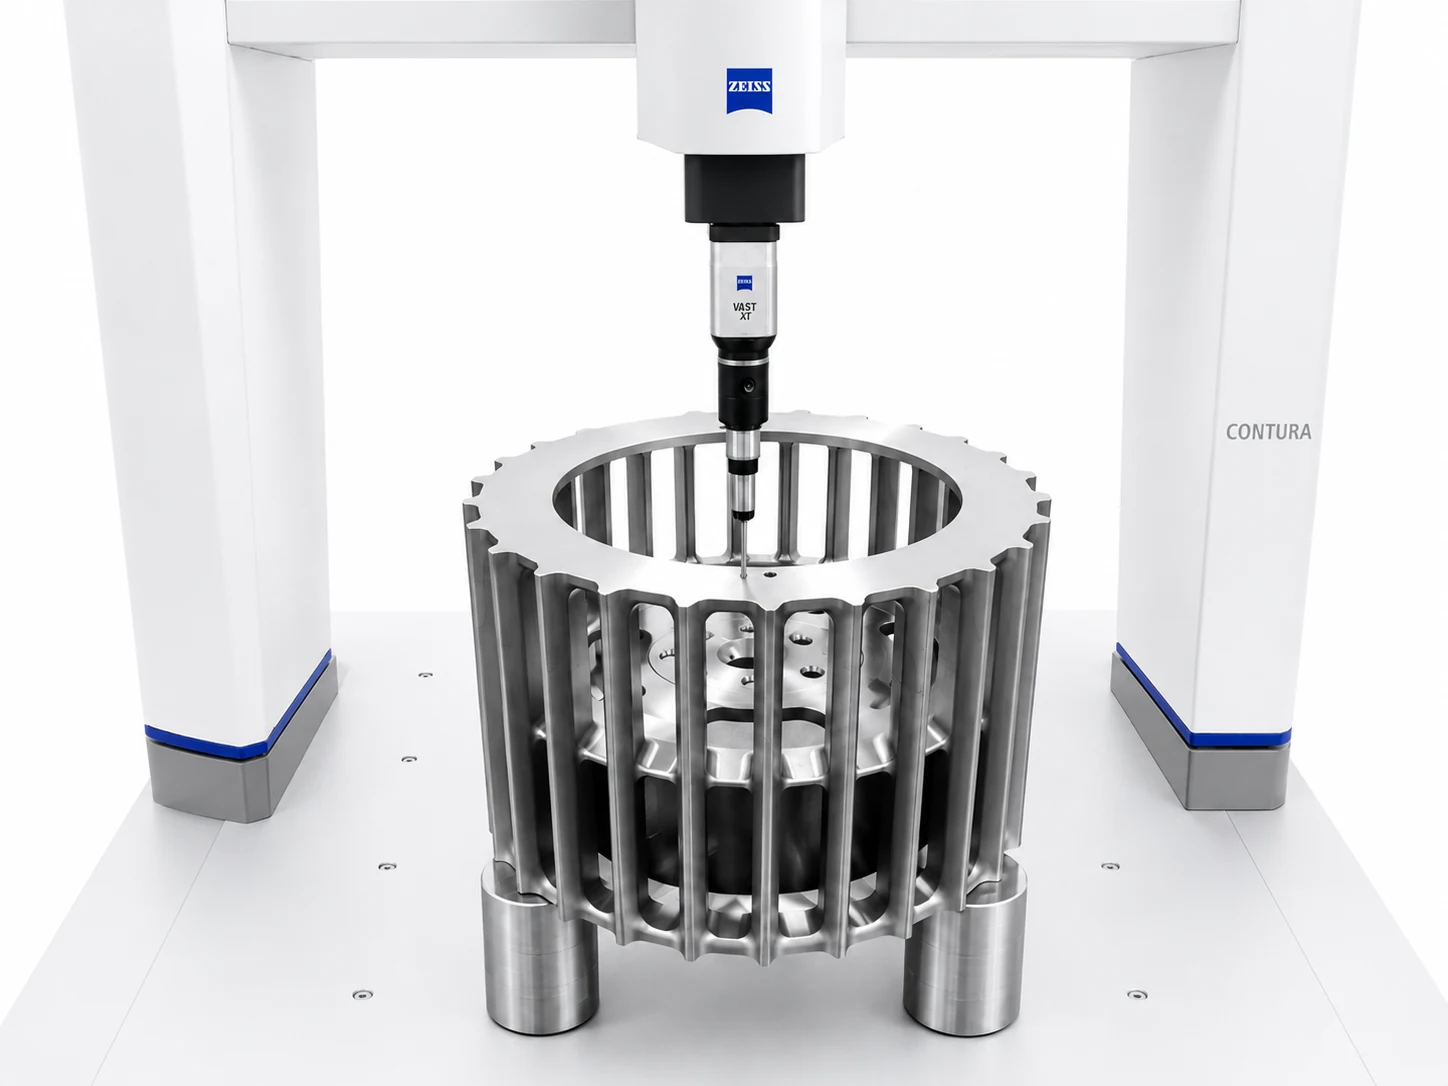
Inspection and Assembly Components
Parts qualified on the measuring machine
View specifications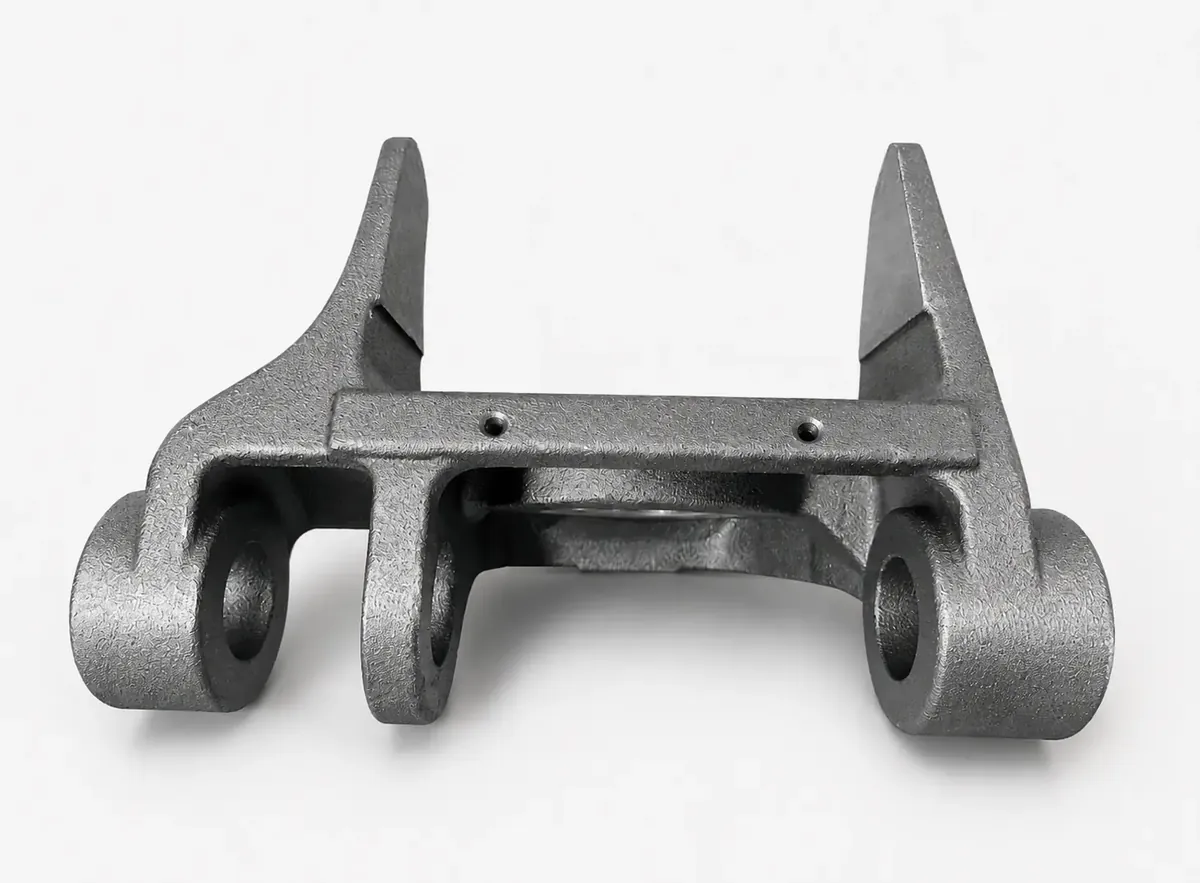
Connection and Support Structures
Bracket and support structures
View specificationsThin Wall and Curved Components — Frequently Asked Questions
How thin a wall can be cast?
Thin wall parts are covered by the silica sol lost wax process across a size range of 2 mm to 2000 mm. The achievable minimum wall is confirmed against the specific part geometry.
What surface finish can be expected as cast?
Ra 3.2 to Ra 6.3 is the normal as cast range for the silica sol lost wax process.
What do you need to prepare a quotation?
Drawings, material, quantity, quality standard and target delivery date.
Which inspection is included?
The inspection scope is agreed during drawing review. Carbon steel, low alloy steel, stainless steel and quenched and tempered grades.
Get A Quotation For Thin Wall and Curved Components
Send the drawing and the application. We will confirm the process route, the production base and the inspection scope before quoting.