What This Part Is And Why It Is Made This Way
Transmission parts fail at the tooth root and at the keyway, not in the middle of the body. That is why grade, heat treatment depth and root radius matter more than the nominal strength of the steel.
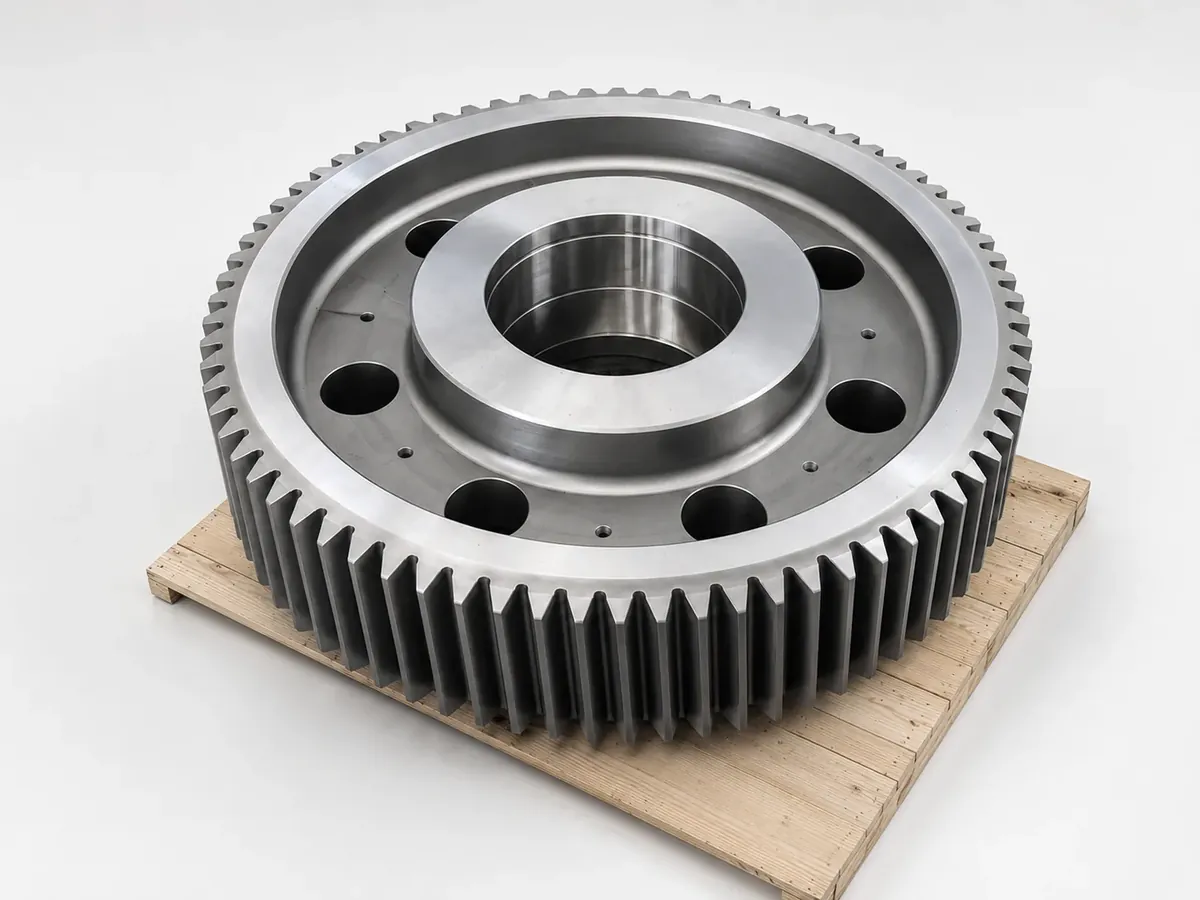
Gears and drive components are produced in alloy steel such as 42CrMo4 or case hardening grades, heat treated and then cut to the tooth data on the drawing.
What You Get From This Route
Case hardening grades available where surface hardness and a tough core are both required.
Heat treatment on automated lines keeps distortion repeatable across a batch.
Tooth data and hardness requirements confirmed before cutting starts.
Application Scenarios
- Industrial gearbox gears
- Mining and cement drive trains
- Construction machinery final drives
- Agricultural machinery transmissions
Who It Is For
- Gearbox manufacturers
- Equipment builders with in house assembly
- Service companies supplying drive line spares
Technical Features
- Alloy and case hardening steel grades
- Automated heat treatment lines
- Tooth cutting to drawing data
- Hardness and dimensional verification
What Buyers Run Into Without This Specification
- Teeth pit early because the case depth was never verified.
- The keyway is positioned from the wrong datum and the hub will not fit.
- Different batches have different hardness and wear rates diverge in the field.
Published Material Weight And Process Data
Figures below are the published capability for steel castings and forgings. Part specific values — tolerance on individual features, finish, packing — are confirmed at drawing review and marked TBC until then.
| Material | 42CrMo4, G20Mn5, G26CrMo4, G18NiMoCr3-6, G22CrNi2Mo5-6, AISI 4340, AISI 4140, AISI 4325 and similar grades |
|---|---|
| Weight Range | Steel casting 50 kg - 20 T; forging 50 kg - 50 T |
| Process | Sand casting; shell moulding; open-die and closed-die forging; roll forging |
| Melting | High automation production lines with EAF + LF + VD / AOD melting routes |
| Tolerance | Zero draft sand casting to CT9 on automated heat treatment lines |
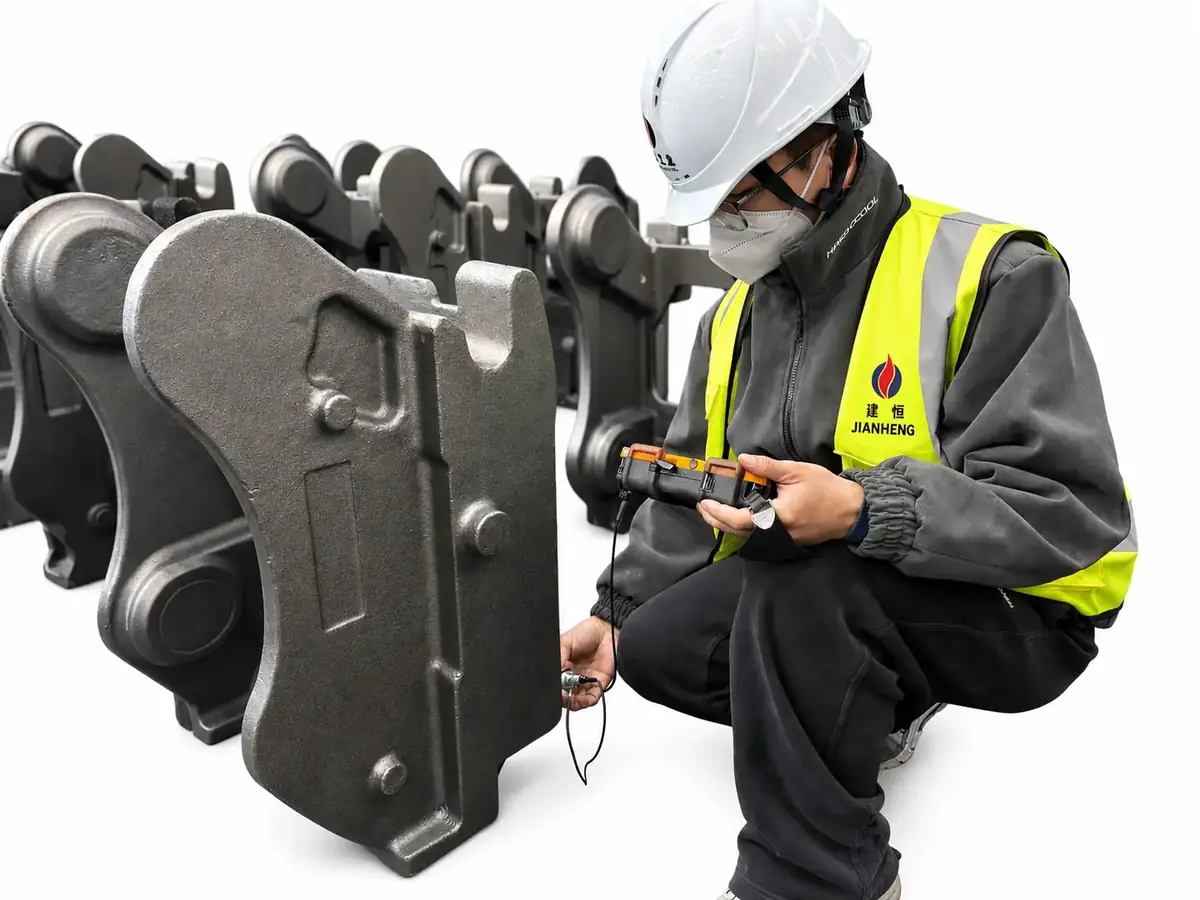
| Inspection | NDT with certified operators, single part certificates and quality document traceability |
| Part Specific Tolerance | TBC — confirmed against the customer drawing |
| Minimum Order Quantity | TBC — depends on the process route selected |
| Lead Time | TBC — confirmed with the production base at quotation |
How The Part Is Made And Checked
- Production — Highly automated production lines with EAF + LF + VD / AOD melting equipment.
- Quality — Certified NDT capability, supporting per-part certificates and traceable quality documents.
- Process Control — Automated heat treatment lines; zero draft sand casting reaches CT9.
Quality management is based on ISO 9001 and covers supplier management, raw material inspection, production process control and final inspection. Inspection results are archived and traceable.
Options And Alternatives
Parts are produced to the customer drawing rather than to a fixed catalogue item, so material grade, machining scope, surface treatment and packing are all specified per order. Machining, dimensional control, surface treatment and necessary pre-assembly can be added to the same supply route.
Where another process family would suit the part better — for example a forging in place of a casting for a shock loaded connector — that comparison is raised during drawing review rather than after tooling is committed.
How To Specify This Part
Provide the full tooth data sheet, not just the outline drawing. Module, pressure angle, profile shift, quality grade and the required case depth are what a gear shop needs before it can even quote, and an incomplete data sheet is the most common cause of a delayed quotation.
- Send the drawing with material, quantity, quality standard and target delivery date.
- State the inspection class and the zones it applies to, rather than a general note.
- Confirm the packing requirement and the lifting equipment available at the destination.
Related Guides
Other Parts In This Range
Large Steel Structural Castings
Load bearing steel castings up to 20 tonnes
View specifications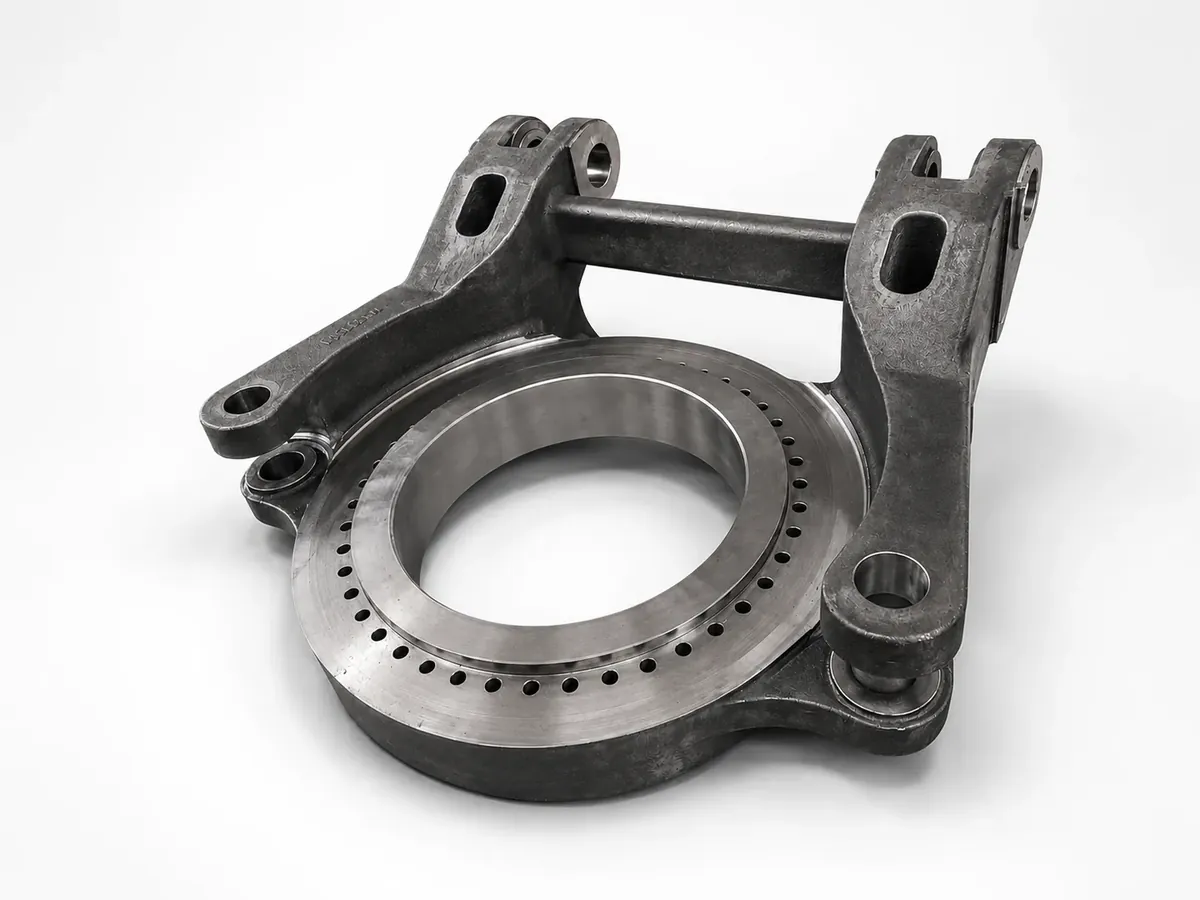
Slewing Support Structural Castings
Rotating support bodies with machined bearing seats
View specifications
Forged Shafts
Stepped shafts with continuous grain flow
View specifications
Flanges and Sleeve Components
Connection flanges and sleeve bodies
View specificationsGears and Transmission Components — Frequently Asked Questions
Which steel grades do you use for gears?
Alloy steels such as 42CrMo4 and case hardening grades such as 16MnCr5, 20MnCr5 and 18CrNiMo7-6 are used in the forging and machining business, selected against the drawing.
Do you supply gears heat treated and ready to fit?
Yes. Heat treatment and machining are coordinated in the same route, so parts can be delivered finished to the drawing.
What do you need to prepare a quotation?
Drawings, material, quantity, quality standard and target delivery date.
Which inspection is included?
The inspection scope is agreed during drawing review. Automated heat treatment lines; zero draft sand casting reaches CT9.
Get A Quotation For Gears and Transmission Components
Send the drawing and the application. We will confirm the process route, the production base and the inspection scope before quoting.