Leveling Machine for Carbon Steel in Color Coating Lines
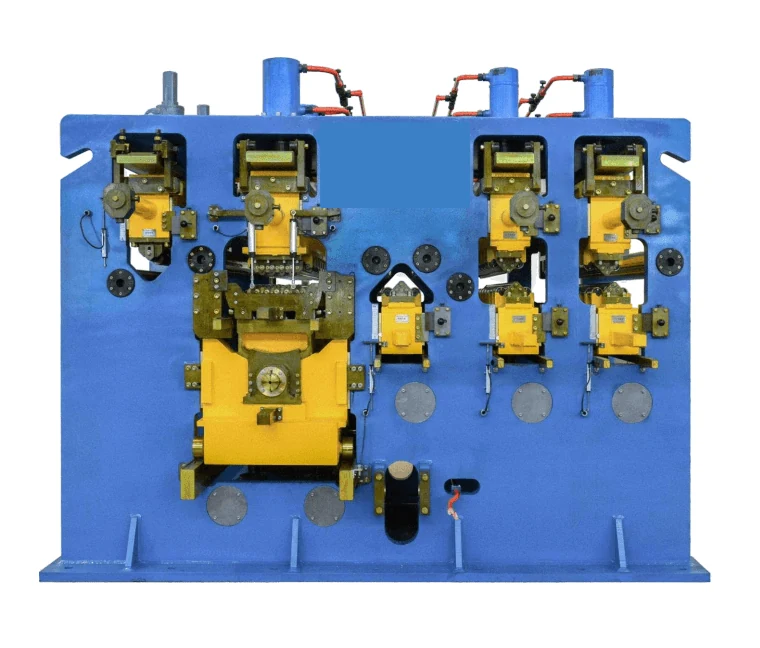
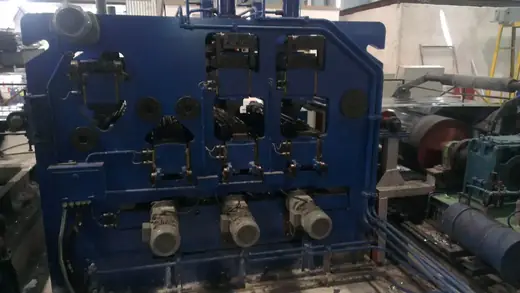
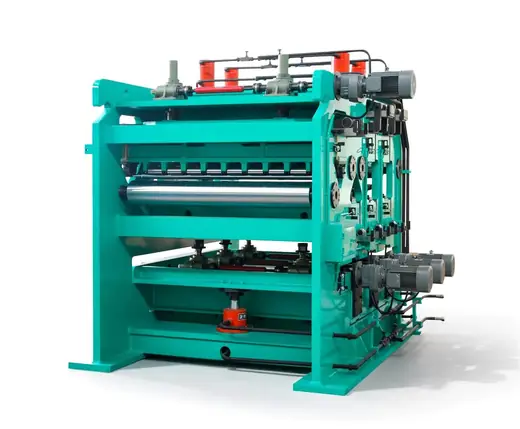
A colour coating line is unforgiving of shape defects because the coating makes every wave visible on the finished panel. This leveling machine applies tension and continuous bending so the strip entering the coater is flat and its internal stress is uniform.
- Two tension rolls at inlet and outlet
- Tension amplified by the roll group
- Two rows of bending components with balancing rollers
- Two stage deformation and correction
Key Benefits
Why leveling matters before coating.
Flat Feed To The Coater
Removing shape defects before coating avoids panels where the coating highlights every wave and buckle.
Uniform Internal Stress
The two stage sequence distributes residual deformation then corrects it, so internal stress tends to uniformity.
Better Mechanical Properties
Improving strip shape also improves the mechanical properties of the material for forming after coating.
Where It Is Used
Line positions and products.
- Colour coating lines for carbon steel
- Prepainted steel sheet production
- Automotive and construction panel material
- Iron and steel manufacturing finishing sections
Who It Is For
- Colour coating line operators
- Prepainted steel producers
- Plants with coating defects traced to strip shape
- Project teams building a new coating line
Problems It Solves
- Shape defects made visible by coating
- Uneven longitudinal extension across the width
- Rolling stress disorder from the mill
- Panels distorting after forming
Technical Features
Machine arrangement.
Tension Stabilisation
Two tension rolls at inlet and outlet stabilise tension and reduce fluctuations before the bending section.
Straightening Unit
The unit carries two rows of bending components with balancing rollers.
Two Stage Correction
Alternating deformation in the first stage evenly distributes residual deformation, which the second stage corrects fully.
Specifications
Machine scope is agreed per project with the coating line builder or owner.
| Application | Colour coating line, carbon steel strip |
|---|---|
| Tension Rolls | 2 sets, inlet and outlet |
| Bending Rows | 2 rows with balancing rollers |
| Correction Stages | 2 |
| Defects Removed | Bilateral wave, unilateral wave, middle wave, two rib wave, warping, buckling |
| Downstream Process | Roll coating and curing sections |
Materials
- Welded and machined machine frame
- Alloy steel work and bending rolls
- Tension drive and hydraulic package
Manufacturing Process
Line Study
Strip range, line speed and coating requirements set the roll configuration.
Frame Manufacturing
Frames are machined so roll centres hold under bending load.
Roll Production
Work, bending and balancing rolls are produced and ground as a set.
Assembly And Test
Roll parallelism, tension control and drive alignment are verified.
Quality Control
- Frame machining inspection
- Roll hardness and geometry records
- Hydraulic and tension system test
- Assembly alignment report
Customization Options
- Strip width and thickness range to your coating line
- Roll configuration for the flatness target
- Interface to the existing line drives
- Scope split for electrical and hydraulic works
Use Guide
- Set elongation from the incoming flatness measurement
- Coordinate leveler settings with the coater to avoid over stretching
- Check balancing roller settings after product changes
- Regrind work rolls before surface condition affects coating adhesion
How It Compares
Leveling options before a coater.
| No leveling before coating | Coating amplifies shape defects visually, so flatness has to be fixed before the coater, not after. |
|---|---|
| Roller leveling without tension | Tension plus bending redistributes internal stress so panels stay flat after forming. |
| Single stage correction | Two stage correction distributes then removes residual deformation, which holds the result through coating and curing. |
Related Products
Tension Leveler for Aluminum Coil
Stress homogenising tension leveler for 0.2-4.0 mm aluminum strip at up to 500 m/min.
View Details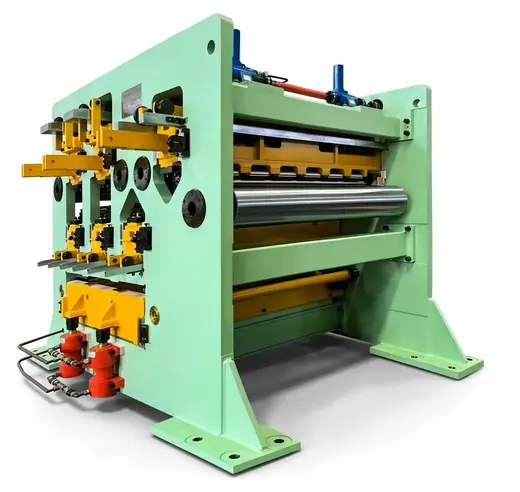
Levelling Machine for Galvanizing Lines
Two stage tension levelling machine removing three dimensional shape defects from carbon steel strip.
View Details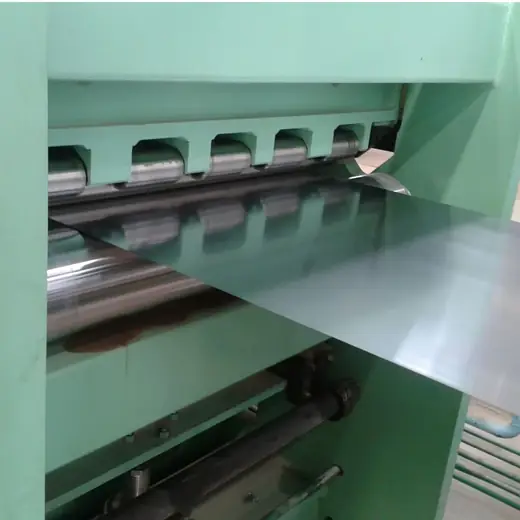
Tension Leveling Machine for Aluminum Plate
Two stage tension and bending machine removing three dimensional shape defects from aluminum plate.
View Details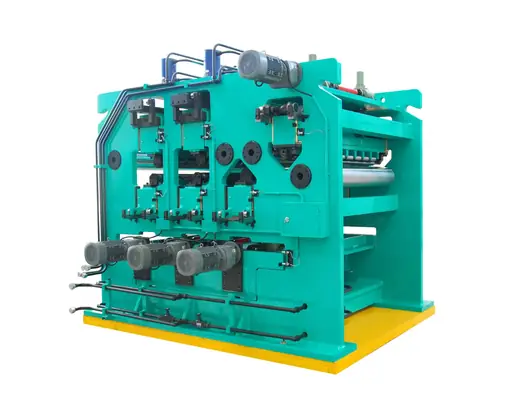
Tension Leveller With Two Bending and Two Levelling Stages
Two bending and two levelling stage leveller for carbon steel in galvanizing lines.
View DetailsRelated Project References
Tension Leveler For A 1550 mm Galvanizing Line
A tension leveler configuration for carbon steel strip on a 1550 mm galvanizing line, with the chrome plated roll set to keep it consistent.
Read More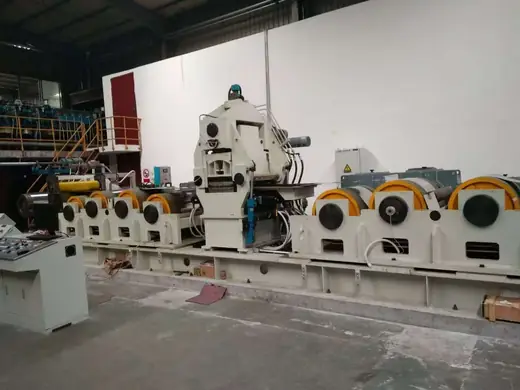
Leveler For An 850 mm Cut To Length Line
A compact leveler for a narrow cut to length line producing blanks for electrical parts and automotive components.
Read MoreRelated Technical Articles
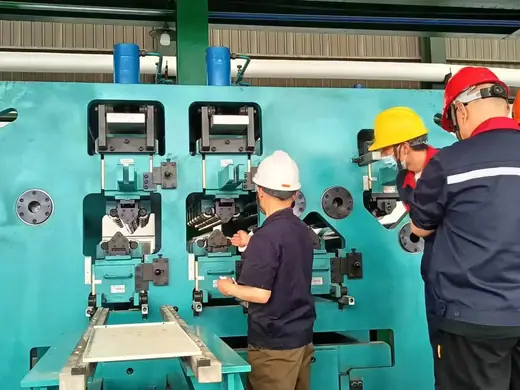
Tension Leveler For Steel Coil Working Principle And Specifications
Double bending and double straightening, the three stage sequence inside the machine, and the specification envelope it works in.
Read More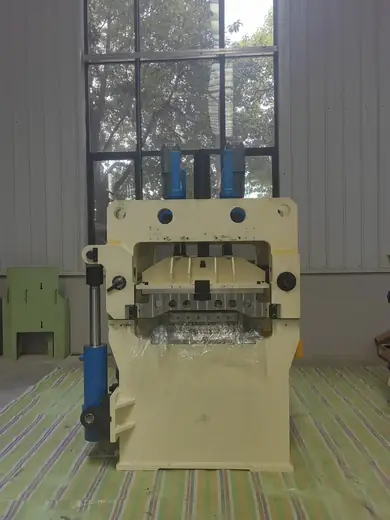
Maintaining A 23 Roll Tension Leveler For Aluminum Plate
Overload, roll wrapping and lubrication are the three operating mistakes that destroy work rolls on aluminum lines.
Read MoreLeveling Machine for Color Coating Lines FAQ
Why level before coating?
Coating makes shape defects visible on the finished panel. Levelling first removes bilateral wave, unilateral wave, middle wave, two rib wave, warping and buckling before the coater.
How does the two stage sequence work?
In the first stage the strip undergoes alternating deformation to distribute residual deformation evenly, and the second stage corrects it fully.
Which materials does it handle?
Carbon steel strip for colour coating lines, including material for automotive and construction panels.
Can it be fitted into an existing line?
Yes. Send the line layout, available length, speed and tension data and we design to fit.
Do you supply the roll spares?
Yes, the complete roll set is produced here so spares match the original drawing.
What do you need to quote?
Strip width and thickness range, steel grade, line speed, incoming and target flatness, and the coating process used.
Prepare Flat Strip For Your Coater
Send your coating line data and our engineers come back with a leveling machine configuration.