Galvanizing and Colour Coating Lines
Coating makes every remaining shape defect visible. This solution covers the levelling that comes before the coater, the coating station itself, and the consumable rolls that decide how long the result stays consistent.
Where The Problems Start
Coating lines fail on flatness and on surface, and both are decided upstream.
- Shape defects amplified visually by the coating
- Coating weight drifting across the strip width
- Roll surface condition marking coated strip
- Flatness drifting between shifts as rolls wear
- Two stage levelling that distributes then corrects residual deformation
- Coating pressure measured through sensors and load cells
- Chrome plated rolls that protect coated surface quality
- A roll replacement plan tied to your tonnage
From Enquiry To After Sales
The stages of a coating line project or upgrade.
Line Study
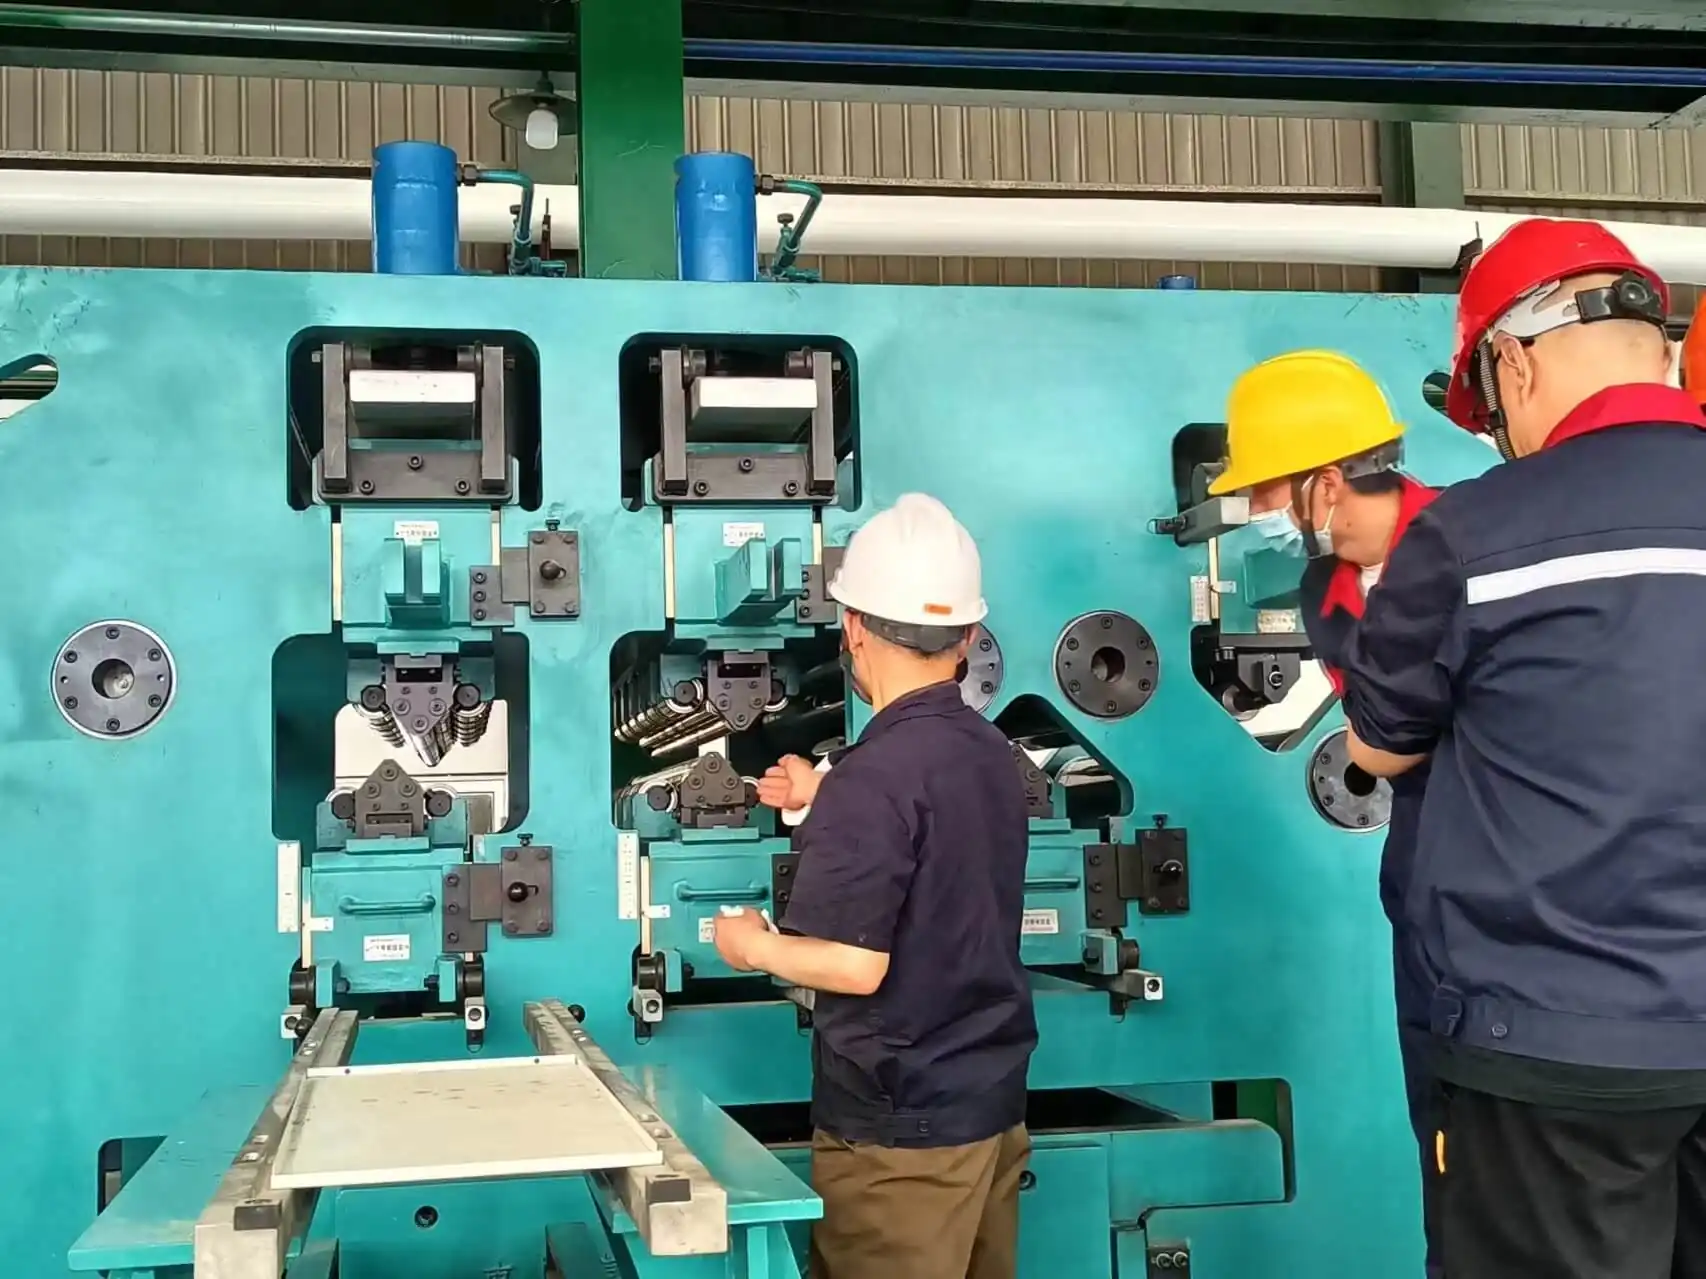
The defect you see at the exit was usually created several sections earlier. We look at incoming flatness, levelling capability and coater condition together before proposing equipment.
Equipment Selection
Levelling and coating are often bought from different suppliers with no shared specification. We configure the leveler and the coater against the same strip programme so the two sections agree.
Manufacturing And Test
Roll parallelism and coating head clearance decide the result. Parallelism, hydraulic response and load cell calibration are verified before shipment.
Commissioning
Operators inherit settings that nobody documented. Personnel training and production commissioning are part of the scope, with settings recorded per product.
Consumable Supply
Coated surface quality falls off slowly as rolls wear. Work rolls, back up rolls and cassettes are supplied against the same drawings on a repeat basis.
Equipment And Parts In This Solution
Equipment and consumables in this solution.
Tension Leveler for 1550 mm Galvanizing Lines
1550 mm galvanizing line tension leveler with two bending rows and balancing rollers.
View Details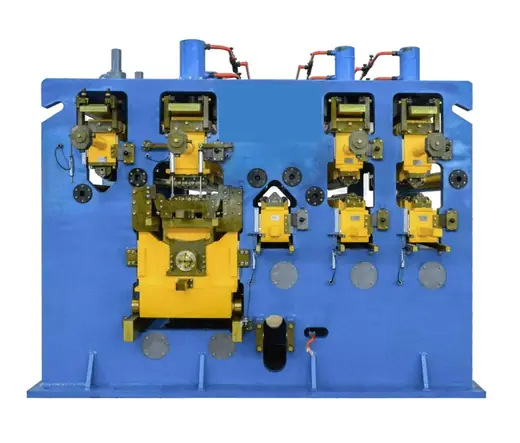
Leveling Machine for Color Coating Lines
Tension and bending leveler preparing carbon steel strip for the coating section.
View Details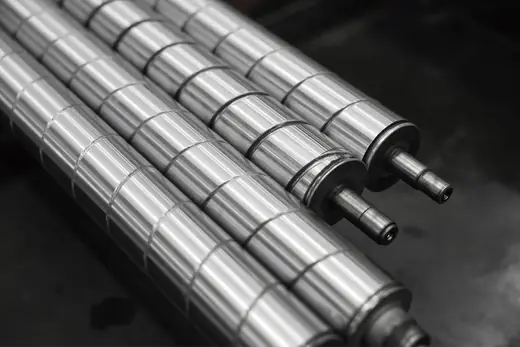
Roll Coating Machine for Galvanizing and Color Coating Lines
Horizontal, vertical and winding type coaters for 450-2200 mm strip at 70-260 m/min.
View Details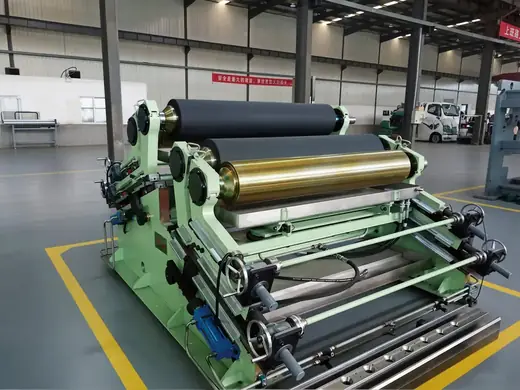
Passivation Roll Coater
Applies trivalent chrome passivation film to protect strip surfaces against corrosion.
View Details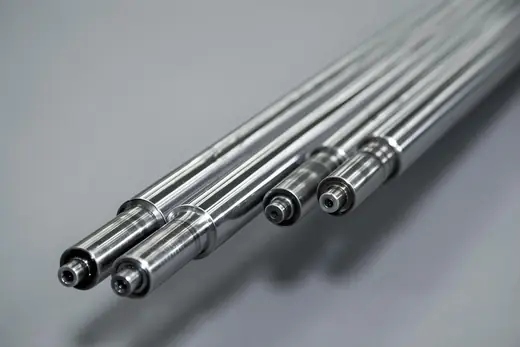
Chrome Plated Working Roll for 1450 mm Tension Leveler
Consumable work roll for 1450 mm galvanizing line tension levelers, chrome plated 0.05 mm.
View Details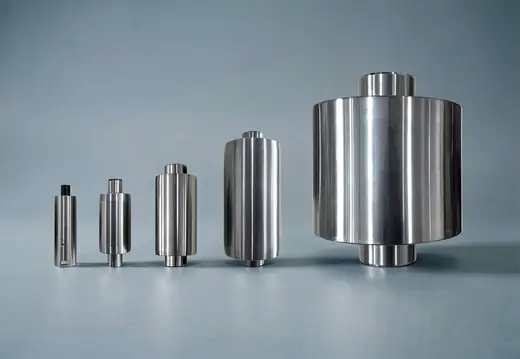
Premium Back Up Rolls for Leveling Machines
Deep heat treated and precision ground back up rolls, roundness held to 0.005 mm class.
View DetailsProject References
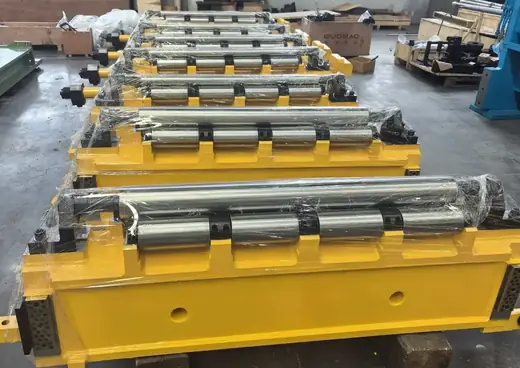
1660 mm Scale Breaker Roll Units For A Wide Cold Rolling Pickling Line
Precision roll units and cassettes for the scale breaking section of a 1660 mm wide cold rolling pickling line handling 0.5-12 mm strip.
Read More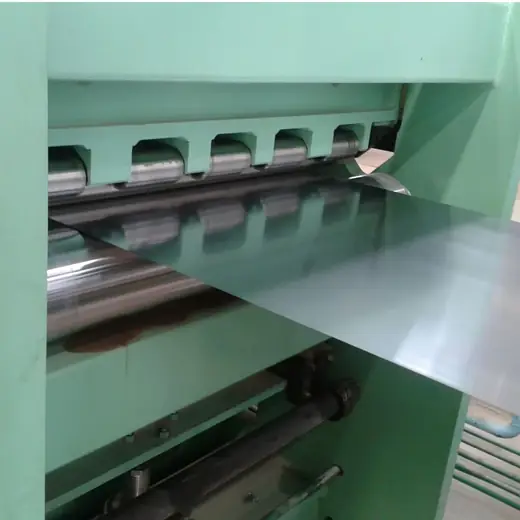
Tension Leveler For A 1550 mm Galvanizing Line
A tension leveler configuration for carbon steel strip on a 1550 mm galvanizing line, with the chrome plated roll set to keep it consistent.
Read MoreGalvanizing and Coating Lines FAQ
Should we level before or after coating?
Before. Coating amplifies shape defects visually, so the strip has to be flat when it reaches the coater.
Which coater type suits a galvanizing line?
The vertical type is generally used in galvanizing lines. All three types, horizontal, vertical and winding, suit colour coating lines.
How do we stop flatness drifting between shifts?
Usually by replacing the support side of the cassette rather than only the work rolls, then recording leveler settings per product.
Can you supply just the roll sets?
Yes. Many customers start with a roll set programme and only later replace the machine.
What surface protection do you apply on coating line rolls?
Hard chrome plating, typically around 0.05 mm, finish ground so the plated surface is concentric with the roll necks.
Fix Flatness Before The Coater
Send your coating line data and our engineers propose the levelling and coating scope.