Roll Coating Machine for Galvanizing and Color Coating Lines
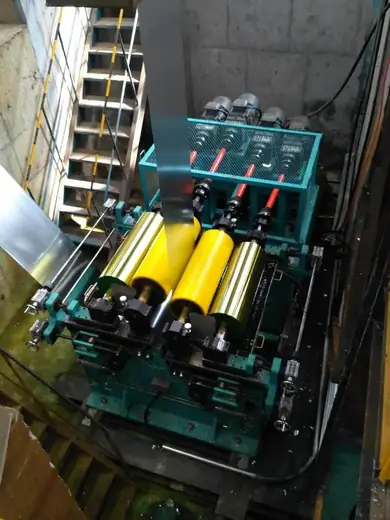
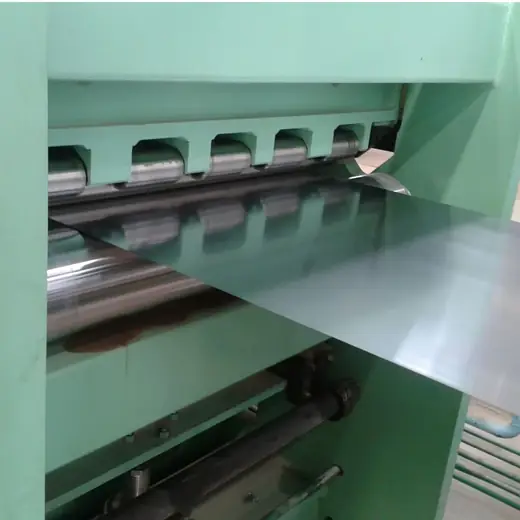
The roll coating machine sits in the finishing section and applies paint or passivation solution evenly across the strip, which is what gives the finished coil its oxidation and corrosion resistance. Applicator and pick up rolls carry the liquid, and coating head position is controlled by hydraulic cylinders with pressure feedback.
- Strip width 450-2200 mm
- Strip thickness 0.15-3 mm
- Operating speed 70-260 m/min
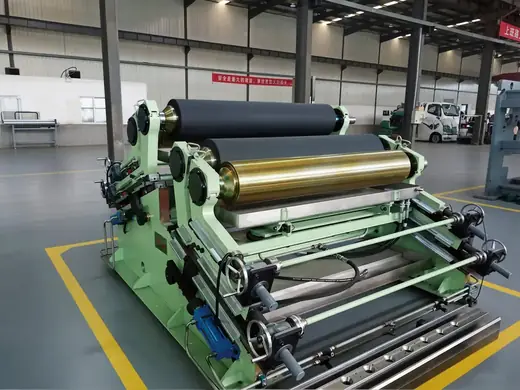
- Horizontal, vertical and winding types available
Key Benefits
What a properly configured coater does for the line.
Even Film Across Full Width
Applicator and pick up rolls transfer paint or passivation evenly, so coating weight does not drift from edge to edge.
Controlled Roll Pressure
Pressure sensors give roll pressure feedback and four load cells are configured for the passivation coating rolls, so the setting is measured rather than guessed.
Fast Access For Colour Change
The top side coating head has a synchronised quick opening mechanism, which is what keeps colour changes short.
Where It Is Used
Where each configuration is used.
- Vertical type in continuous galvanizing lines for passivation
- All three types in colour coating lines
- Primer and finish coat stations on prepainted steel lines
- Passivation stations on aluzinc and galvanized coil
Who It Is For
- Galvanizing lines adding or replacing a passivation coater
- Colour coating line operators
- Project teams building a new prepainted steel line
- Plants widening their strip programme up to 2200 mm
Problems It Solves
- Uneven coating weight across the strip width
- Coating defects from unstable roll pressure
- Slow colour changes holding up the line
- Coater geometry that cannot handle the full width range
Technical Features
Mechanical arrangement.
Front And Rear Applicator Rolls
Coater heads sit on the front and opposite sides of the strip, with a slight non contact clearance from the strip to optimise coating quality.
Hydraulic Head Positioning
The front coating head is driven by hydraulic cylinders, with linear bearings supporting frame movement and handwheels for manual adjustment.
Load Cell Feedback
Four load cells are configured for the passivation coating rolls so applied pressure is monitored during production.
Specifications
Configuration depends on the line. Values below are the standard operating range.
| Applicable Strip Width | 450-2200 mm |
|---|---|
| Applicable Strip Thickness | 0.15-3 mm |
| Operating Speed | 70-260 m/min |
| Configurations | Horizontal, vertical, winding type |
| Coating Head Sets | 2 sets of coating heads |
| Load Cells | 4 sets for passivation coating rolls |
| Head Actuation | Hydraulic cylinders with pressure sensor feedback |
| Frame Support | Linear bearings with manual handwheel adjustment |
Materials
- Machined steel frame with linear bearing guides
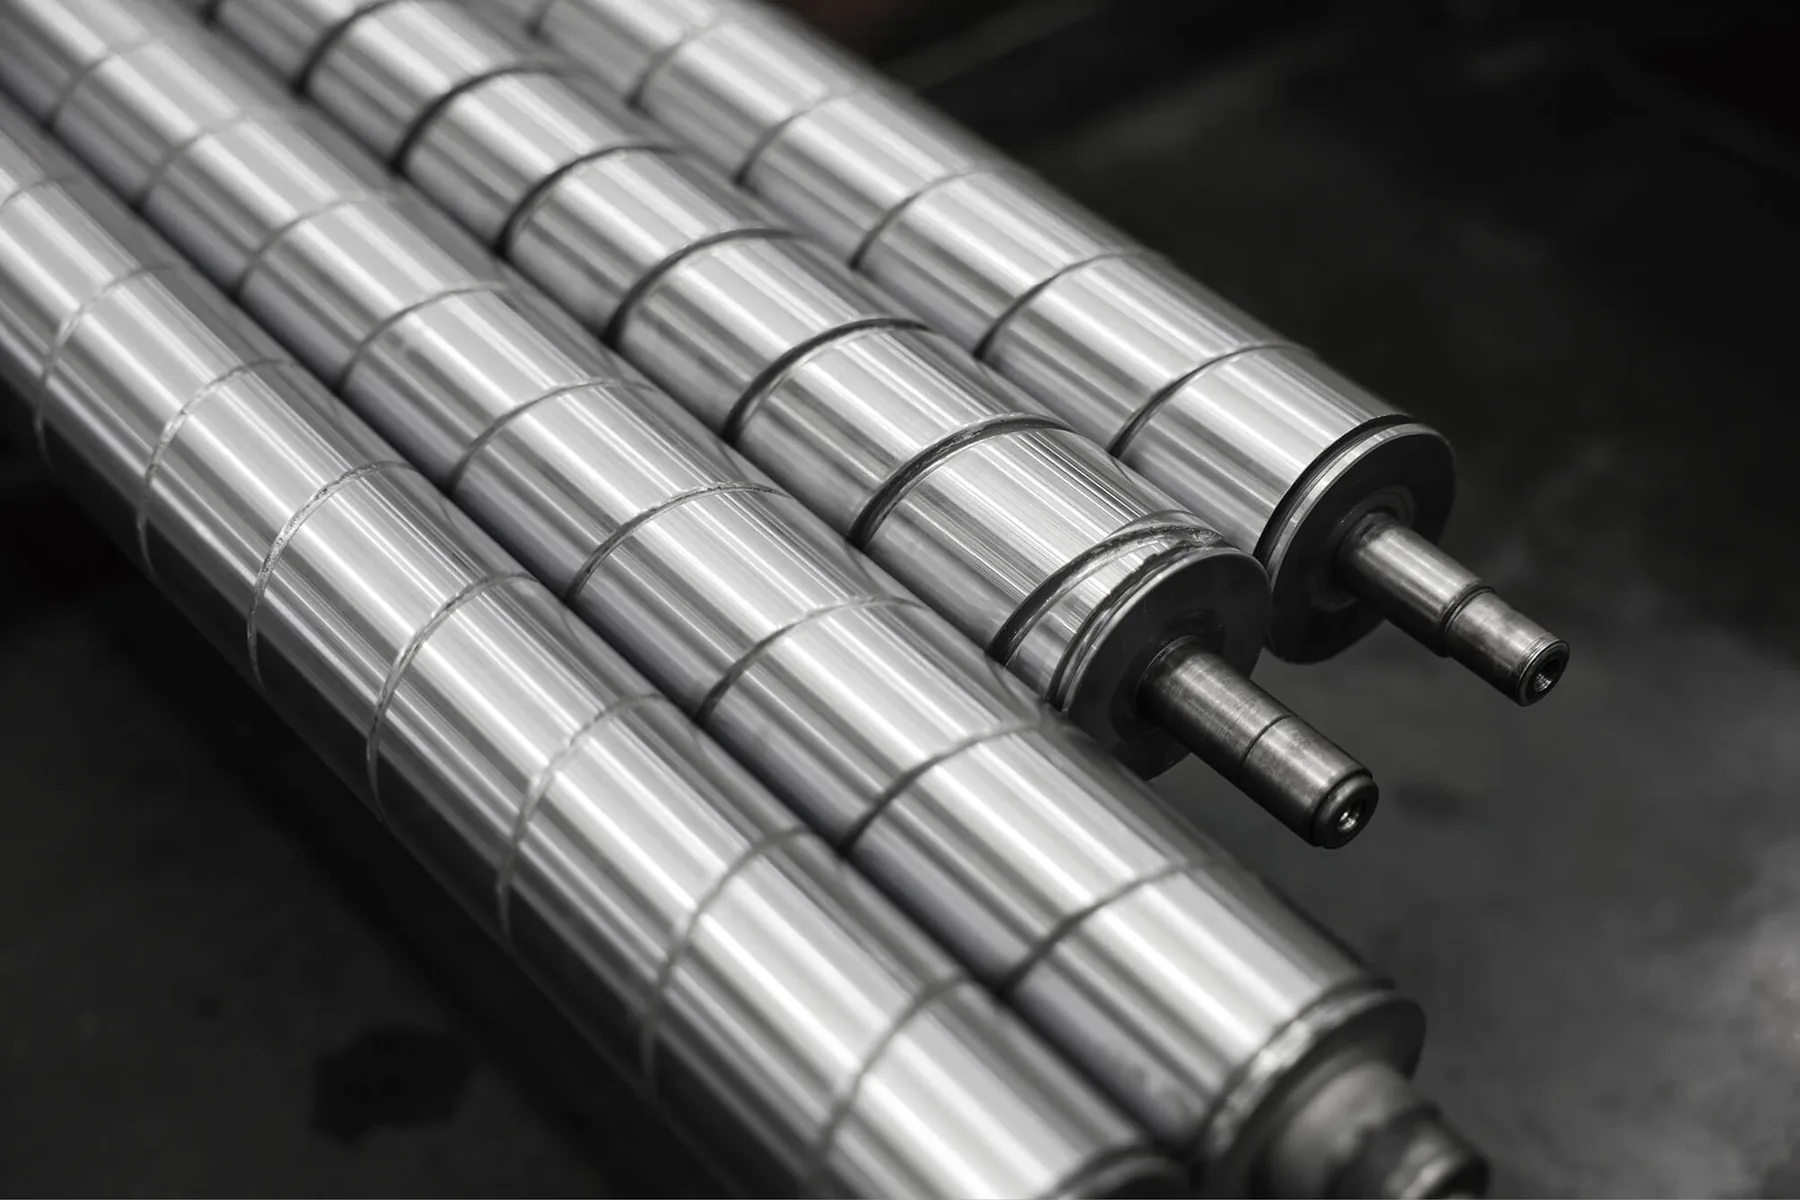
- Applicator and pick up rolls with coating grade surface
- Hydraulic cylinders and load cells
Manufacturing Process
Line Interface Study
Strip width, speed, coating type and the available space in the finishing section set the configuration.
Frame Manufacturing
Frames and head supports are machined so roll parallelism holds during head movement.
Roll And Head Assembly
Coating heads, applicator rolls and pick up rolls are assembled and gap set.
Instrumentation And Test
Pressure sensors and load cells are fitted and the head movement is function tested.
Quality Control
- Frame machining and parallelism inspection
- Roll runout measurement
- Hydraulic circuit pressure test
- Load cell calibration record
Customization Options
- Horizontal, vertical or winding configuration
- Strip width and speed range to your line
- Coating head count and arrangement
- Interface to your existing paint supply and automation
Use Guide
- Keep applicator roll clearance to the strip as specified, contact damages the coating
- Zero the load cells at each product change
- Clean rolls before colour change to avoid carryover
- Record roll pressure settings per product for repeatability
How It Compares
Choosing between the three configurations.
| Horizontal type | Used on colour coating lines where the strip runs horizontally through the finishing section. |
|---|---|
| Vertical type | Generally deployed in galvanizing lines, and also usable on colour coating lines. |
| Winding type | Suits colour coating lines where the strip path wraps the coating rolls. |
Roll Coating Machine for Galvanizing and Color Coating Lines FAQ
Which type should we use in a galvanizing line?
The vertical model is generally deployed in galvanizing lines. All three configurations, horizontal, vertical and winding, are suitable for colour coating lines.
What strip range does it cover?
Strip width 450-2200 mm, thickness 0.15-3 mm and operating speed 70-260 m/min.
How is roll pressure controlled?
The front coating head is driven by hydraulic cylinders and pressure sensors give roll pressure feedback. Four load cells are configured for the passivation coating rolls.
How fast is a colour change?
The top side coating head has a synchronised quick opening mechanism to speed up access. Actual changeover time depends on your cleaning procedure and paint system.
Do you supply the coating rolls afterwards?
Yes, applicator and pick up rolls can be supplied as spares to the same drawing.
What do you need for a quotation?
Strip width and thickness range, line speed, coating type, number of coating stations and whether the unit replaces an existing coater.
Configure A Coater For Your Finishing Section
Send your strip range, line speed and coating type and we come back with the configuration and a quotation.