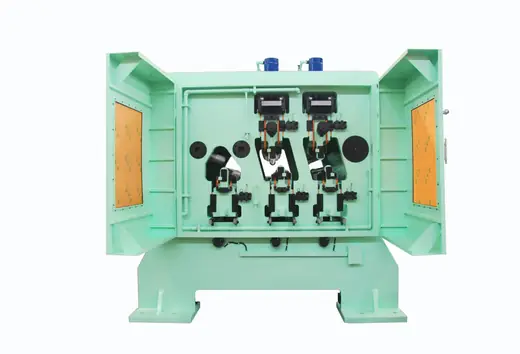
Scale Breaker for 1850 mm Pickling Lines to Protect Strip and Save Acid
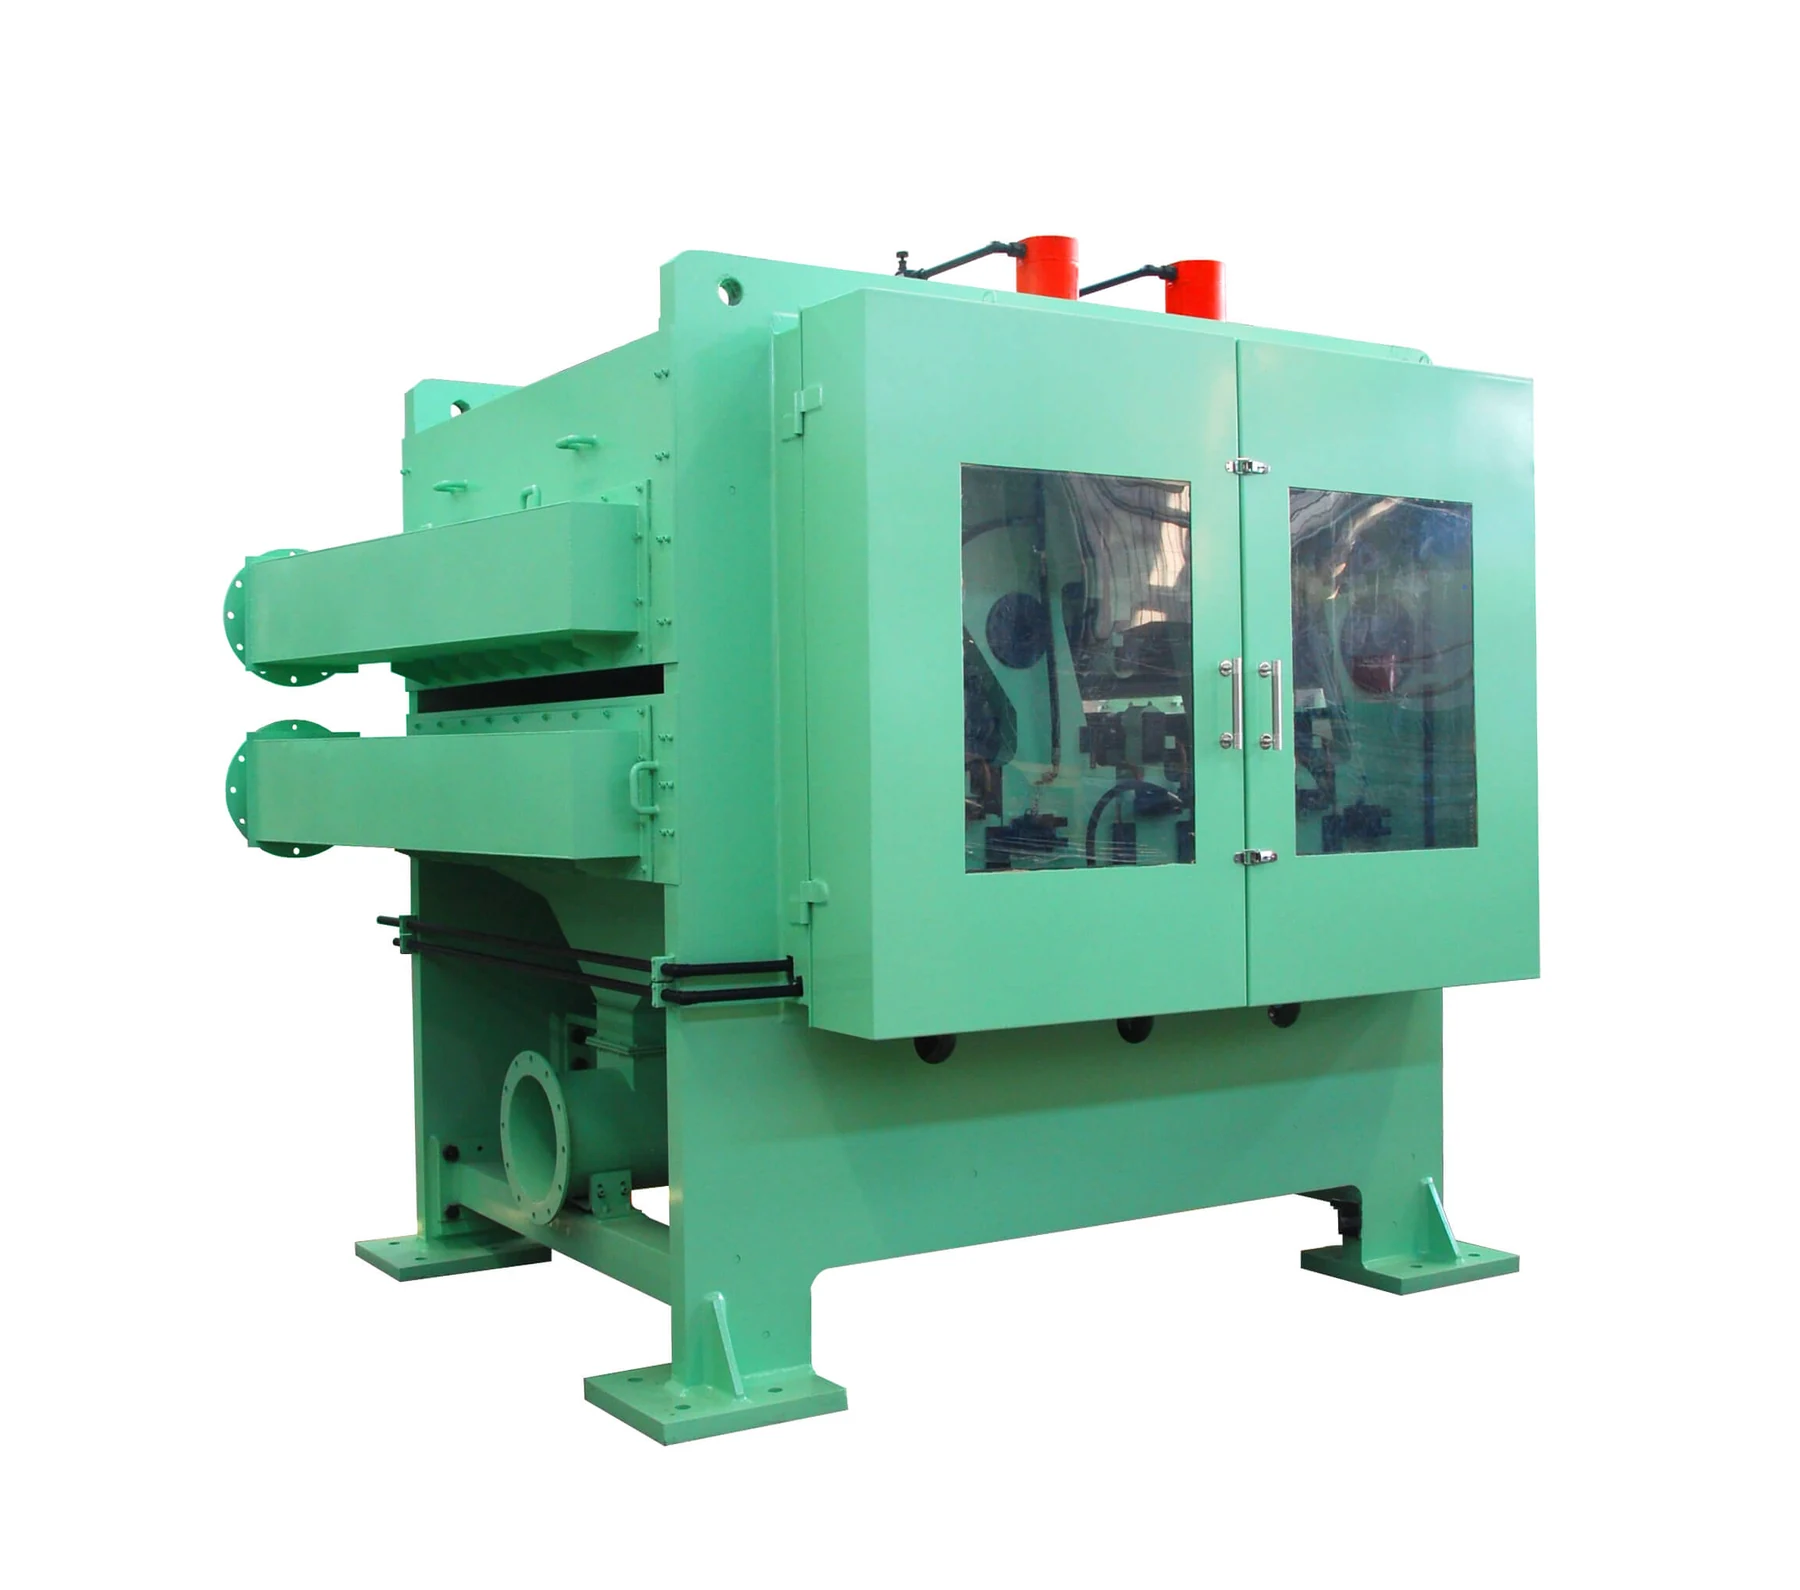
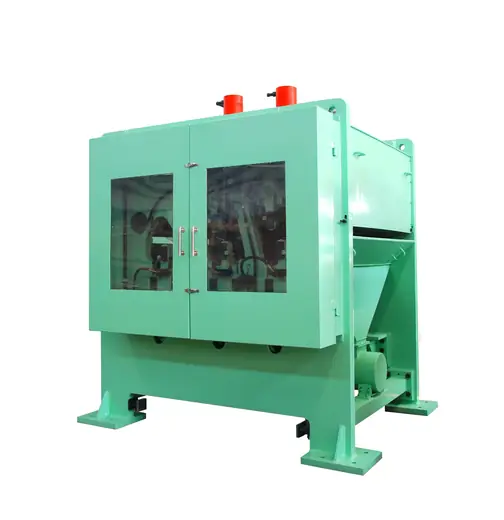
This is the scale breaker configuration for an 1850 mm pickling line. Located in front of the pickling tank, it deforms the hot rolled strip plastically while the oxide surface fractures, saving acid and correcting shape in the same pass.
- For 1850 mm wide pickling lines
- Positioned in front of the pickling tank
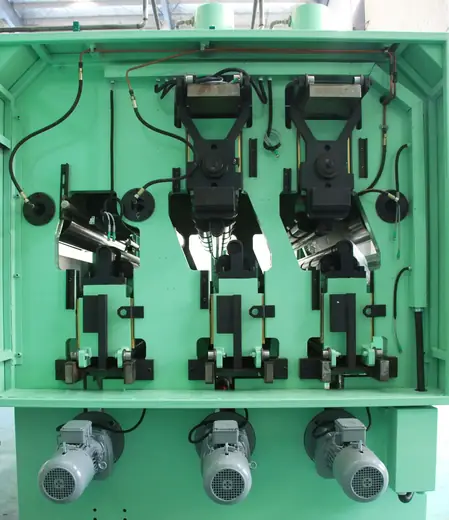
- Bending and correcting roll units at the core
- Saves acid and improves strip correction
Key Benefits
What wide line operators gain.
Acid Saved Across Wide Strip
On a wide line the acid bill is proportionally larger, so fracturing the oxide mechanically produces a bigger absolute saving.
Strip Protected From Rejection
Better correction of hot rolled strip reduces coils rejected for shape after pickling.
Same Technology As Coating Line Levelers
The machine uses tension leveler technology already proven on galvanized, acid rolling and colour coating lines.
Where It Is Used
Line context.
- 1850 mm hot strip pickling lines
- Acid rolling lines
- Wide coil preparation for cold rolling
- Automotive and appliance sheet feedstock preparation
Who It Is For
- Wide pickling line operators
- Mills tracking acid and yield costs
- Plants correcting shape before cold rolling
- Buyers replacing an ageing scale breaker
Problems It Solves
- High acid consumption on wide lines
- Uneven descaling across 1850 mm
- Shape defects carried into cold rolling
- Rejections caused by poor strip shape
Technical Features
Working principle.
Plastic Deformation Of Strip Only
Continuous alternating stretching and bending deforms the strip plastically while the oxide surface, which cannot deform, fractures.
Bending And Correcting Roll Units
The bending and correcting roll units are the core component, and their configuration sets performance.
Wide Line Sizing
Roll length, drive power and frame stiffness are sized for 1850 mm strip.
Specifications
Configuration is agreed against your pickling line data.
| Line Width | 1850 mm |
|---|---|
| Position | In front of the pickling tank |
| Principle | Continuous alternating stretching and bending |
| Core Component | Bending and correcting roll units |
| Material | Hot rolled strip |
| Related Lines | Galvanized wire, acid rolling and colour coating lines |
Materials
- Welded and stress relieved frame
- Alloy steel bending and correcting rolls
- Sealed bearings for acid service
Manufacturing Process
Line Survey
Coil width, thickness, scale condition and line speed are reviewed.
Frame Fabrication
Housings are welded, stress relieved and machined for roll position accuracy.
Roll Unit Production
Bending and correcting roll units are produced and ground.
Assembly And Test
Roll parallelism and drive alignment are verified before shipment.
Quality Control
- Frame machining inspection
- Roll hardness and runout records
- Bearing seal verification
- Assembly parallelism report
Customization Options
- Line width and roll length
- Roll unit configuration for scale condition
- Drive package and automation interface
- Spare roll units and cassettes
Use Guide
- Set elongation from the incoming scale condition
- Check roll gap parallelism after roll changes
- Monitor acid consumption as a performance indicator
- Inspect bearing seals regularly in the acid area
How It Compares
Against other approaches on a wide line.
| Pickling without mechanical descaling | An intact oxide layer costs acid and tank time, especially across wide strip. |
|---|---|
| Separate leveling after pickling | Shape correction in the same pass saves line length and handling. |
| Narrower scale breakers | The 1850 mm configuration handles the full coil width without edge to centre variation. |
Related Products
Scale Breaker for Push Pull Pickling Line 800-1350 mm
Tension leveler type scale breaker for push pull pickling lines handling 800-1350 mm hot rolled strip.
View Details
1850 Scale Breaker for Aluminum Sheet Lines
Stretch bend leveling and scale removal for aluminum strip up to 1850 mm working width.
View Details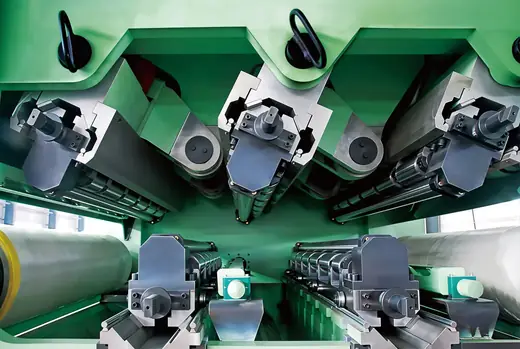
Scale Breaker for 1850 mm Pickling Lines
Pre pickling tank scale breaker for wide hot rolled strip with bending and correcting roll units.
View Details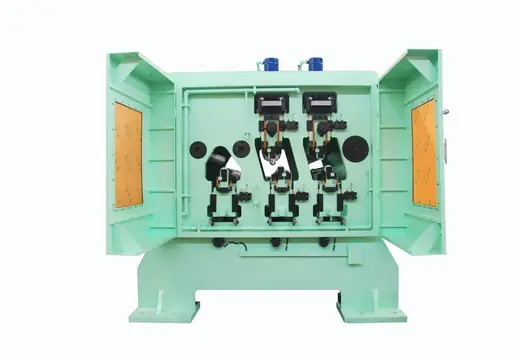
Scale Breaker for Pickling Lines
Pickling line scale breaker fracturing oxide by stretch and bend, saving acid and correcting shape.
View Details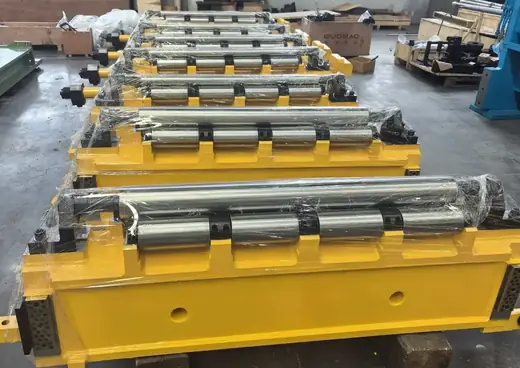
Related Technical Articles
How Scale Breakers Optimise Surface Quality Before Cold Rolling
Dry and wet scale breakers, the elongation window that matters, and why the first processing step decides the last.
Read MoreTension Control In Push Pull Pickling Lines Section By Section
Typical tension ranges for entry, pickling, rinse, dry and exit sections, and what each one is protecting.
Read MoreScale Breaker in 1850 mm Pickling Lines FAQ
What line width is this for?
1850 mm pickling lines. Other widths are configured from your line data.
How does it save acid?
Continuous alternating stretching and bending deforms the strip plastically while the oxide surface fractures. Acid then penetrates instead of dissolving an intact scale layer.
Does the strip get corrected as well?
Yes, the hot rolled strip also receives better shape correction in the same pass.
What is the core component?
The bending and correcting roll units, which determine both scale fracture and shape correction.
Do you supply spares for it?
Yes, roll units, rolls and cassettes are produced in the same shop.
What do you need to quote?
Line width, strip thickness range, scale condition, line speed and layout.
Configure A Wide Line Scale Breaker
Send your 1850 mm line data and we come back with a configuration and budget figure.