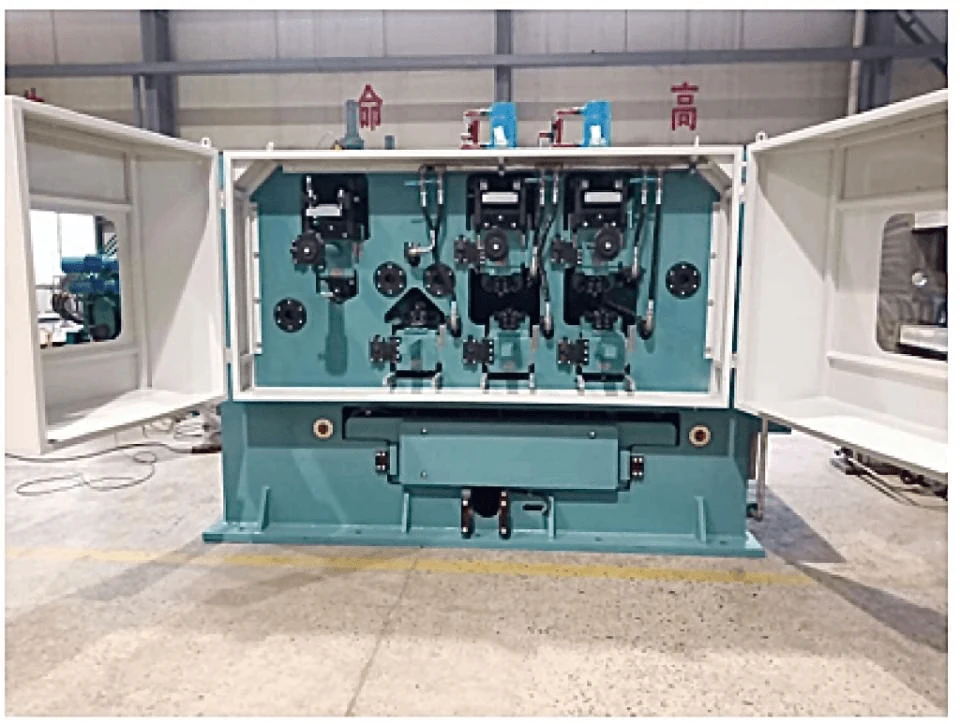
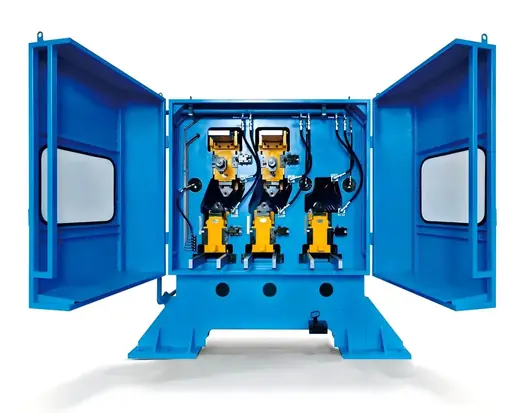
Scale Breaker for Medium Width Push Pull Pickling Lines
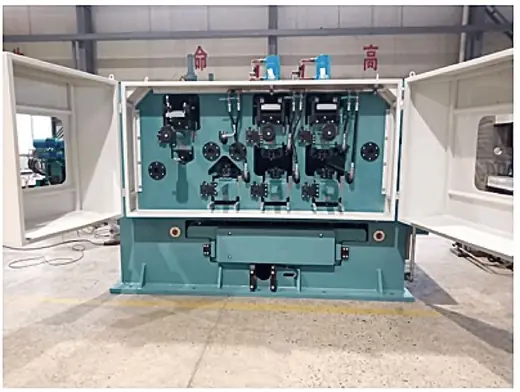
Installed immediately before the acid tanks, this scale breaker cracks the mill scale and corrects strip shape in a single pass. Controlled tension plus alternating bending produce plastic elongation of up to 7 percent, which opens the oxide layer for the acid and removes edge wave, centre wave, buckle and camber at the same time.
- Strip width 800-1350 mm, thickness 1.5-4.0 mm
- Process speed up to 180 m/min
- Annual capacity up to 750,000 tons
- Outgoing flatness below 5 IU
Key Benefits
Why mills put a scale breaker in front of the acid tanks.
Faster Pickling At Lower Acid Cost
Cracking the oxide layer lets acid reach the base metal evenly, so the strip clears the tanks faster and acid consumption falls.
Shape Corrected Before Cold Rolling
Edge waves, centre waves, buckles and camber are removed in the same pass, so the coil reaching the cold mill or the coating line is already flat below 5 IU.
Coil To Coil Flexibility
Because the push pull line processes single coils without welding, grade and dimension changes happen between coils instead of between campaigns.
Where It Is Used
Typical installations.
- Push pull pickling lines at medium width hot strip mills
- Service centres pickling bought in hot rolled coil
- Feed preparation ahead of cold rolling
- Feed preparation for galvanizing and colour coating lines
Who It Is For
- Steel producers running medium width hot rolled coil
- Service centres that pickle before slitting or cutting
- Project teams comparing push pull against continuous pickling investment
- Plants replacing an ageing scale breaker inside an existing line
Problems It Solves
- Uneven pickling caused by an intact scale layer
- Shape defects carried forward into cold rolling
- High acid consumption and long tank residence time
- Capital cost of a continuous pickling line for mixed order books
Technical Features
How the unit is configured.
Dual Action Bending
Alternating bending under tension produces plastic elongation up to 7 percent, which is the level where pickling efficiency is highest on a tension leveler type scale breaker.
Tension Controlled Entry And Exit
Entry and exit bridle rolls hold the strip under stable tension so elongation stays inside the target band on every coil.
Line Speed To 180 m/min
Rolls, bearings and drives are sized for continuous work at process speeds up to 180 m/min.
Specifications
Configuration is matched to the line. The values below are the design envelope for this medium width unit.
| Strip Width | 800-1350 mm |
|---|---|
| Strip Thickness | 1.5-4.0 mm |
| Process Speed | Up to 180 m/min |
| Annual Line Capacity | Up to 750,000 tons |
| Elongation | Up to 7 percent |
| Outgoing Flatness | Below 5 IU |
| Line Type | Push pull pickling line, single coil processing without welding |
Materials
- Welded steel frame stress relieved before machining
- Alloy steel work rolls and back up rolls
- Sealed bearing housings for the acid line environment
Manufacturing Process
Line Study
We review strip width, thickness range, speed and the existing tank layout before fixing the roll configuration.
Frame Fabrication
Housings are welded, stress relieved and machined so roll positions stay true under bending load.
Roll Manufacturing
Work rolls, back up rolls and cassettes are produced and ground to the drawing.
Assembly And Trial
The unit is assembled and checked for roll parallelism and drive alignment before shipment.
Quality Control
- Material certificates for frame plate and roll bar
- Machining check of roll seat positions after stress relief
- Roll hardness and runout records per roll
- Assembly report with roll gap and parallelism values
Customization Options
- Strip width and thickness range to suit your coil programme
- Roll count and diameter to hit the elongation you need
- Drive package and control interface to your line automation
- Entry and exit geometry to fit an existing pickling line
Use Guide
- Keep elongation at or below 7 percent, higher values do not improve pickling
- Check roll gap parallelism after every roll change
- Monitor bearing seals in the acid fume area
- Record flatness readings coil by coil to spot roll wear early
How It Compares
How this unit compares with the other ways to prepare hot rolled strip.
| Continuous pickling line | Lower investment and faster grade change, at throughput that still reaches 750,000 tons per year. |
|---|---|
| Mechanical descaling without leveling | Shape correction happens in the same pass, so no separate leveler is needed before cold rolling. |
| Longer acid residence time | Cracking the scale mechanically cuts pickling time and acid consumption instead of paying for both. |
Related Products
1850 Scale Breaker for Aluminum Sheet Lines
Stretch bend leveling and scale removal for aluminum strip up to 1850 mm working width.
View Details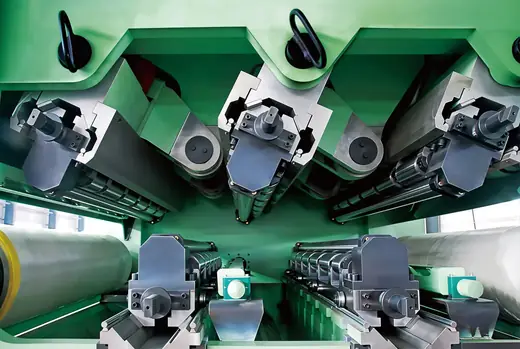
Scale Breaker for 1850 mm Pickling Lines
Pre pickling tank scale breaker for wide hot rolled strip with bending and correcting roll units.
View Details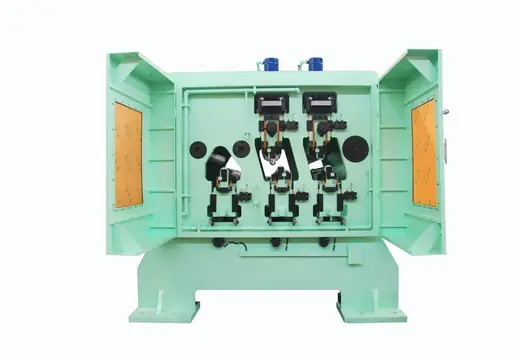
Scale Breaker for Pickling Lines
Pickling line scale breaker fracturing oxide by stretch and bend, saving acid and correcting shape.
View Details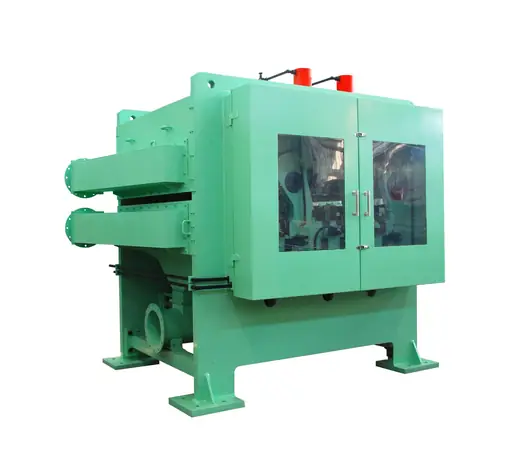
Scale Breaker in 1850 mm Pickling Lines
Wide line scale breaker for 1850 mm pickling lines, fracturing oxide and correcting hot rolled strip.
View Details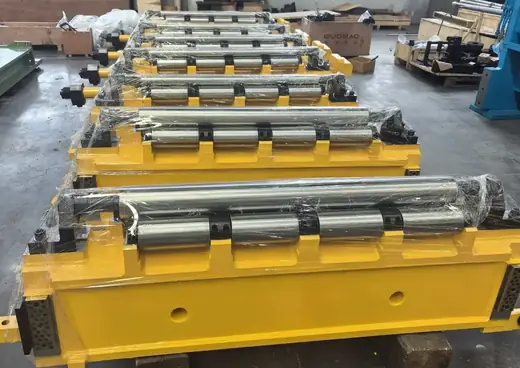
Related Technical Articles
How Scale Breakers Optimise Surface Quality Before Cold Rolling
Dry and wet scale breakers, the elongation window that matters, and why the first processing step decides the last.
Read MoreTension Control In Push Pull Pickling Lines Section By Section
Typical tension ranges for entry, pickling, rinse, dry and exit sections, and what each one is protecting.
Read MoreScale Breaker for Push Pull Pickling Line 800-1350 mm FAQ
What strip range does this scale breaker cover?
It is designed for 800-1350 mm wide and 1.5-4.0 mm thick hot rolled strip, at process speeds up to 180 m/min.
How much elongation should we run?
Up to 7 percent. Pickling efficiency is maximised at that level on a tension leveler type scale breaker, and going higher only consumes strip properties.
What flatness can we expect at the exit?
Below 5 IU, with edge waves, centre waves, buckles, warping and camber removed in the same pass.
Can it be retrofitted into our existing line?
Yes, that is the common case. Send the line layout, available length before the acid tanks and the drive data, and we design the unit to fit.
Do you supply spare rolls afterwards?
Yes. Work rolls, back up rolls and roll cassettes for this unit are made in the same shop, so replacements match the original drawing.
What information do you need to quote?
Strip width and thickness range, line speed, annual tonnage, and whether the unit is for a new line or a replacement inside an existing one.
Discuss Your Pickling Line Upgrade
Send your coil programme and line layout and our engineers come back with a scale breaker configuration and a budget figure.