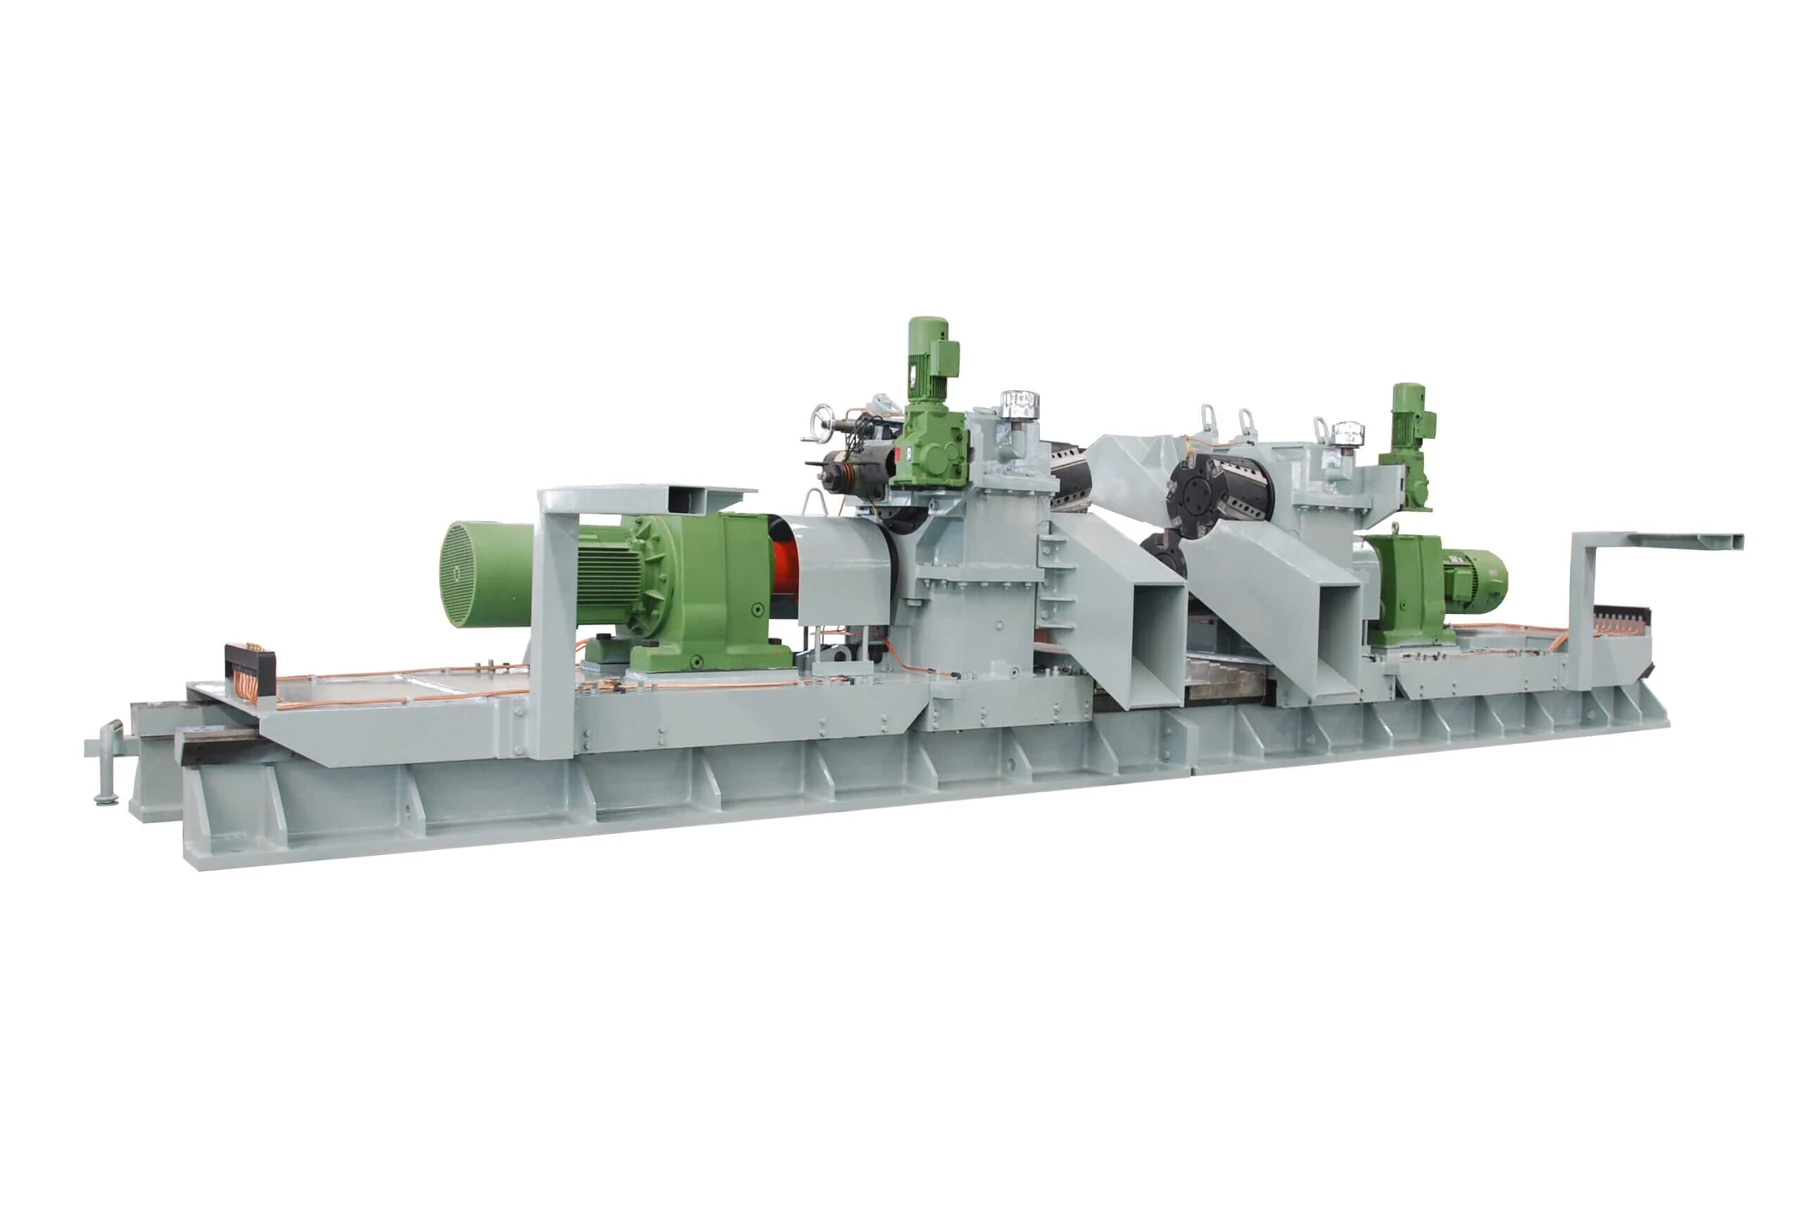
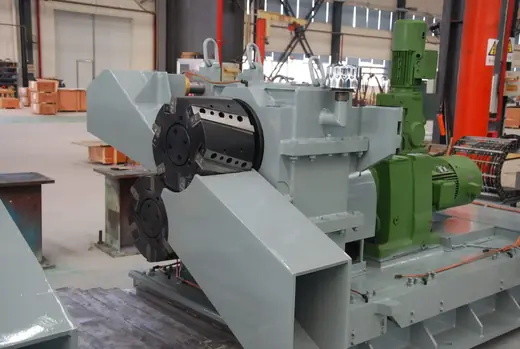
Edge Trimming Unit for Slitting Lines Down to 0.23 mm Strip
Rolled strip often carries small edge defects such as cracks. If they are not trimmed away the strip can break in a later process, so the edge trimmer keeps width consistent and removes the crack sources before they become a line stop.
- Trims strip down to 0.23 mm thickness
- Double head cantilever rotary hybrid power shear
- Double edged blades with end face grinding
- Width adjustment by two oil cylinders with servo control
Key Benefits
What trimming protects.
Strip Breakage Prevented
Removing edge cracks stops the strip breaking in follow up processes, which is the expensive failure this machine avoids.
Consistent Width
Trimming keeps the strip at the same width along its length, which matters for every downstream operation.
Precise Width Setting
Two oil cylinders with servo cylinder control adjust shearing width precisely rather than by manual setting.
Where It Is Used
Where it is used.
- Slitting lines in metallurgical plants
- Continuous processing lines trimming rolled strip
- Thin gauge strip production down to 0.23 mm
- Preparation before further forming or coating
Who It Is For
- Slitting line operators
- Plants with edge crack related strip breaks
- Line builders specifying trimming equipment
- Maintenance teams replacing a worn trimmer
Problems It Solves
- Edge cracks causing strip breaks downstream
- Width variation along the coil
- Slow or imprecise width changes
- Blade wear on thin gauge material
Technical Features
How the cut is made.
Two Blade Shearing Action
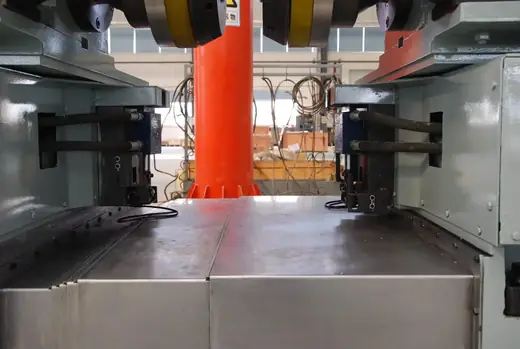
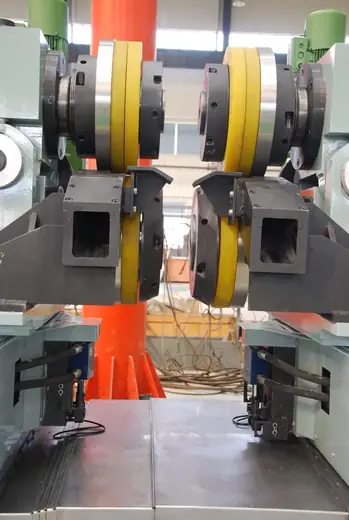
Two displacement and vertical circular blades are set to a defined gap and overlap, so the strip deforms at the contact area until it fractures cleanly.
Double Head Cantilever Structure
A double head cantilever rotary hybrid power shear arrangement carries both trimming heads.
Blade Retention And Grinding
Blades are double edged with end face grinding and hydraulic nut locking.
Specifications
Blade and drive configuration are matched to strip thickness and material.
| Minimum Strip Thickness Reference | 0.23 mm |
|---|---|
| Structure | Double head cantilever rotary hybrid power shear |
| Blades | Double edged with end face grinding |
| Blade Locking | Hydraulic nut locking |
| Width Adjustment | Two oil cylinders with servo cylinder precision control |
| Cutting Principle | Controlled gap and overlap between vertical circular blades |
Materials
- Machine frame with cantilever heads
- Alloy steel blade shafts
- Hardened double edged circular blades
Manufacturing Process
Strip Data Review
Material, thickness, width and trimmed width range define the machine.
Frame And Head Manufacture
Cantilever heads and frame are machined for blade alignment.
Blade Production
Circular blades are hardened and ground on the end faces.
Assembly And Setting
Blade gap and overlap are set and the width adjustment system tested.
Quality Control
- Head alignment inspection
- Blade hardness and grinding verification
- Gap and overlap setting record
- Servo cylinder positioning test
Customization Options
- Trimmed width range for your product mix
- Blade specification by material and gauge
- Drive package to line speed
- Interface to the scrap chopper and chute
Use Guide
- Set blade gap and overlap for the gauge being run
- Regrind blades on the end face before edge quality drops
- Check hydraulic nut locking after each blade change
- Coordinate trimmed width setting with the scrap handling capacity
How It Compares
Against other edge preparation methods.
| Running untrimmed strip | Edge cracks left in place cause strip breaks in follow up processes. |
|---|---|
| Manual width setting | Servo cylinder control adjusts shearing width precisely and repeatably. |
| Single head trimmers | A double head cantilever arrangement trims both edges with matched blade condition. |
Related Products
Edge Trimmer for HiB Silicon Steel Pickling Lines
Pickling line edge trimmer for 1.2-3.0 mm HiB silicon steel with servo width control.
View DetailsCircle Shear for 0.15 mm Strip Slitting Lines
Rotary circle shear trimming edges on very thin strip down to 0.15 mm thickness.
View Details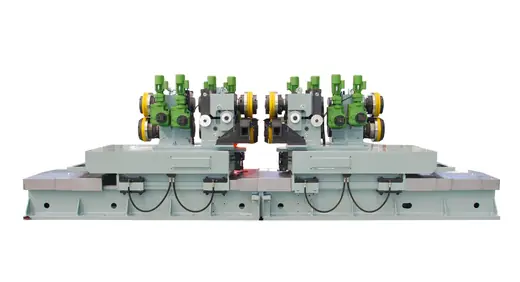
Side Trimmer With 3-50 mm Trimmed Width
Slitting line side trimmer removing 3 to 50 mm from each edge to renew strip width.
View DetailsEdge Trimmer for HiB Silicon Steel Pickling Lines
Pickling line edge trimmer for 1.2-3.0 mm HiB silicon steel with servo width control.
View Details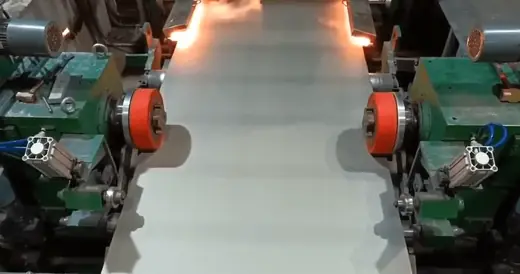
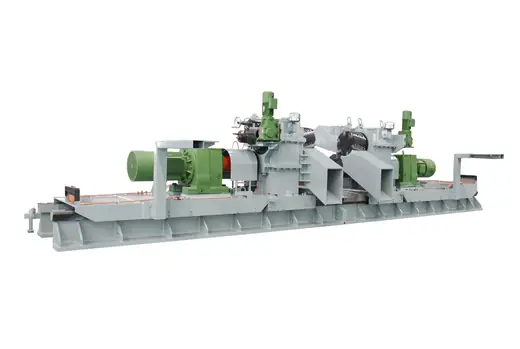
Edge Trimming Unit for Slitting Lines FAQ
How thin a strip can it trim?
This configuration trims down to 0.23 mm thickness. We confirm the range against your material and width.
How does the cut work?
Two displacement and vertical circular blades are set with a defined gap and overlap. As the strip passes, deformation increases with bite depth until the pressurised part fractures.
How is width adjusted?
Two oil cylinders drive the shearing width adjustment, with servo cylinder control for precision.
How are the blades maintained?
Blades are double edged with end face grinding and hydraulic nut locking, so they can be turned and reground.
Do you supply the scrap chopper as well?
Yes, edge trimming and scrap chopping are usually supplied together so trimmed edges are handled continuously.
What do you need to quote?
Strip material, thickness and width range, trimmed width range, line speed and existing layout.
Trim Edges Without Breaking Strip
Send your strip data and trimmed width range and we come back with a trimmer configuration.