A blade that has been sharpened but not restored to its correct geometry will cut, but it will not cut the way it was designed to. The angles matter as much as the edge.
Hook Angle Controls How the Tooth Enters the Material
A more positive hook angle makes the tooth more aggressive, which suits softwood and fast feed rates. A lower or negative hook is what hard material and thin stock need to avoid grabbing. This is why a blade returned from a service with a generic angle cuts differently even though it is perfectly sharp.
Clearance Angle Stops the Tooth Rubbing Behind the Edge
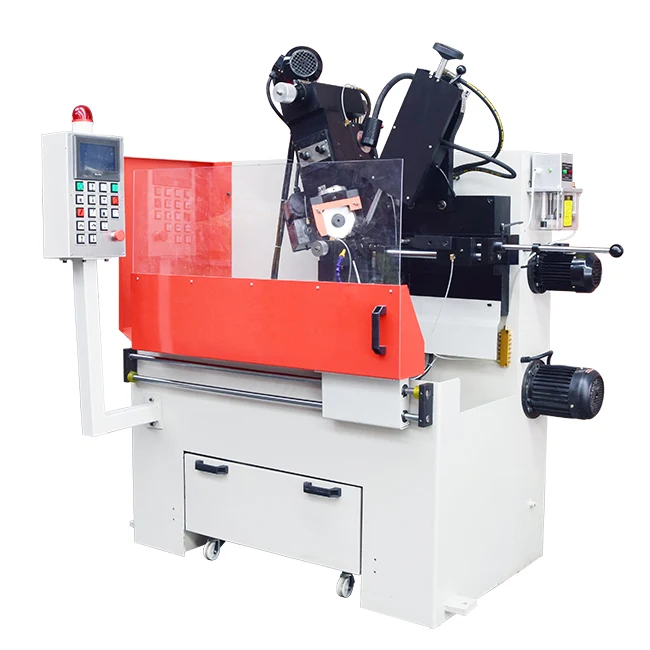
Without clearance the tooth body drags behind the cutting edge, which generates heat and dulls the blade again quickly. Both front and back angles should be set deliberately, which on the WK026 means a range of 5 to 30 degrees on each.
Take the Minimum Stock That Restores a Clean Edge
Every grind shortens blade life. Removing more than the damage requires does not make the blade sharper, it just uses up the tooth. Take a light pass, inspect, and take a second pass only if the edge still shows damage.
- Routine touch up: minimal stock, light pass, fast feed
- Damaged tooth from a foreign object: slower feed and more stock, on the affected area
- Reprofiling after many grinds: check tooth height consistency across the whole blade
Sharpen on a Schedule Not on Failure
Waiting until a blade is visibly dull means every cut before that point was made with a blade past its best, and the damage at the edge is deeper when you finally grind it. A fixed interval based on cutting hours produces better cut quality and longer blade life at the same time.
Wheel Choice Follows Tooth Material
HSS teeth and carbide tipped teeth need different wheels. The machine handles the geometry either way, but grinding carbide tips with the wrong abrasive will not work. Tell us which you run and we specify the wheel with the machine.
Machine Capability Sets the Practical Limits
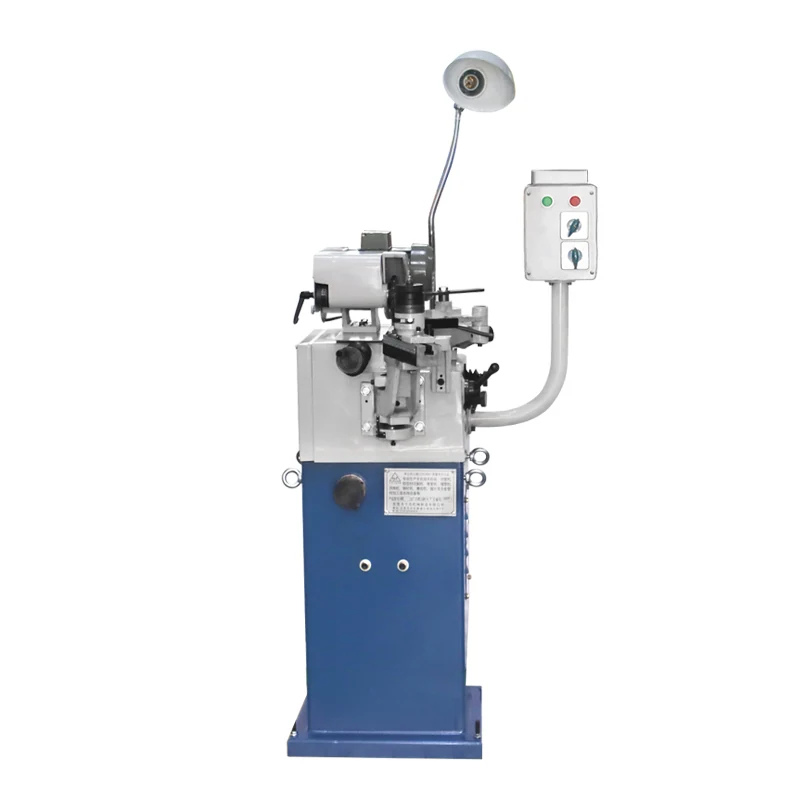
A machine has to cover blade diameter, bore, tooth pitch and thickness. The WK026 covers 80 to 800 mm diameter, 10 to 200 mm bore, 7 to 100 mm pitch and 1 to 7 mm thickness. The WK450 covers 50 to 450 mm diameter, 25 mm pitch and 8 mm thickness. Check your blade rack against both before choosing.