WK22 High Precision Internal and External CNC Punch Grinder
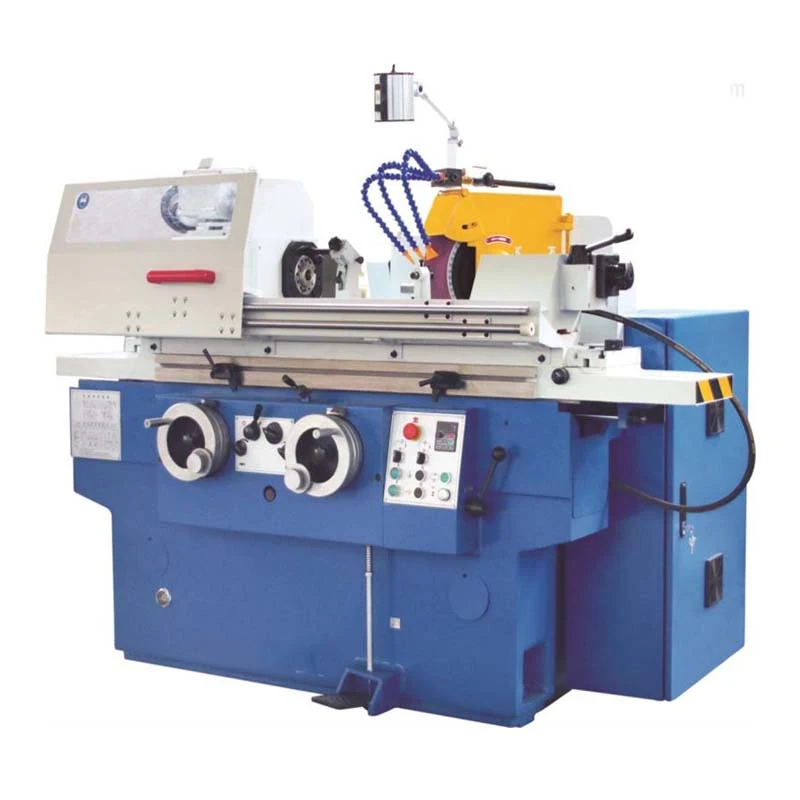
CNC punch and pin grinding from 1 mm up to 150 mm, internal and external.
- Clamping working diameter (ID and OD)1 to 150 mm
- Horizontal travel of worktable150 mm
A stamping plant running progressive dies, where worn punches are shipped to an outside grinding service and replacement punches are bought as finished parts.
Press availability is governed by tooling turnaround. Each punch regrind takes days in transit, so the plant carries spare tooling purely to cover the round trip, and the returned geometry is not always what was asked for.
The WK22 clamps from 1 mm to 150 mm on internal and external diameters, swivels the workhead plus or minus 45 degrees for angled lands, and runs an internal spindle between 10000 and 20000 rpm for die buttons. A 25 mm spindle through hole lets long blanks be supported rather than cantilevered.
Standard configuration ships in 15 to 45 working days after deposit with 12 months warranty. Special control or fixture requirements are quoted with their own dated schedule.
Regrinding becomes a tool room operation measured in hours, and standard blanks can be finished into replacement punches on site. Figures quoted here are machine specifications, not measured results from a named customer installation.
CNC punch and pin grinding from 1 mm up to 150 mm, internal and external.
OD and ID grinding on one machine, for shafts, bushes, needle valves and plungers.
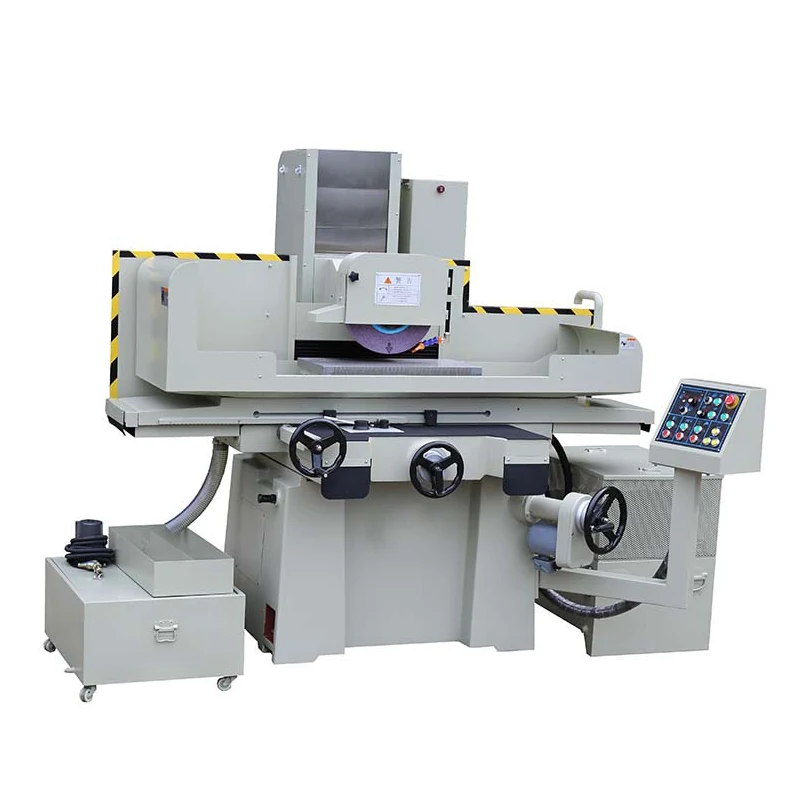
Servo vertical feed and hydraulic table traverse on a 300 x 600 mm table.
If the problem on this page looks like yours, send us the part and the batch size. We will tell you which machine fits and what it will and will not do.