
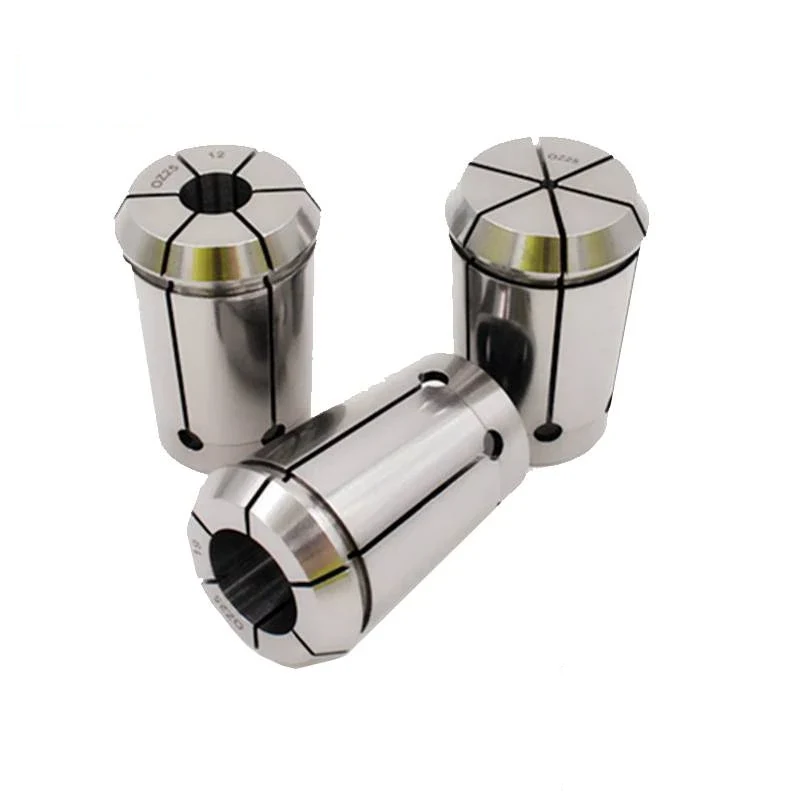
Collet Chuck Series DIN6388A/B EOC
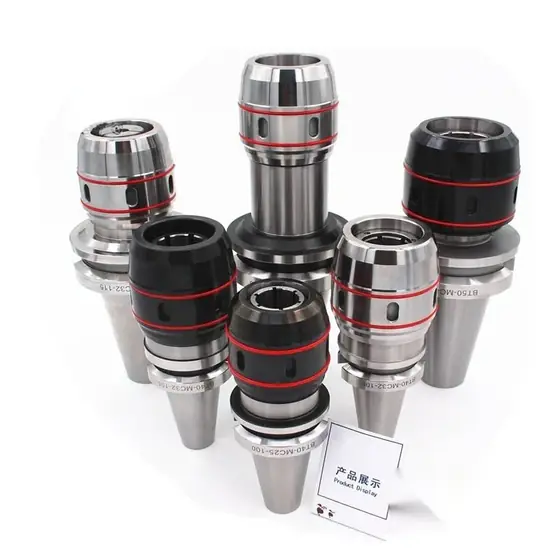
This collet chuck series holds drills, taps, end mills and reamers in a machine spindle with a clamping grip that comes from the elastic steel of the collet itself rather than from a set screw or a sleeve fit. The collets are made to DIN6388A and DIN6388B in the EOC pattern, produced from 65Mn spring steel, hardened to...
What This Machine Does
This collet chuck series holds drills, taps, end mills and reamers in a machine spindle with a clamping grip that comes from the elastic steel of the collet itself rather than from a set screw or a sleeve fit. The collets are made to DIN6388A and DIN6388B in the EOC pattern, produced from 65Mn spring steel, hardened to HRC48-52 and precision ground to a surface roughness within RZ2.5. Run-out is held between 0.008 mm and 0.015 mm, with two precision classes available at 0.005 mm and 0.01 mm for work where tool concentricity drives hole size and tool life. Because the collet closes evenly around the full circumference of the shank, gripping force is spread rather than concentrated at one point, which is what stops tool pull-out during heavy drilling and keeps a cutter running true in milling. The series is used for boring, milling and drilling in production plants, machinery repair shops and building material workshops, and is supplied in a plastic box or to your own packing specification.
Why Buyers Choose This Machine
- Full-circumference elastic clamping spreads grip around the shank and resists tool pull-out
- Run-out held to 0.008 mm to 0.015 mm so hole size and cutter life do not depend on chuck error
- Two precision classes at 0.005 mm and 0.01 mm for work that needs tighter concentricity
- 65Mn spring steel hardened to HRC48-52 keeps the collet slots elastic through repeated clamping cycles
- Precision ground to within RZ2.5 surface roughness on the clamping and seating surfaces
- Made to the DIN6388A and DIN6388B standard so collets interchange with standard holders
- One collet series covers drills taps end mills and reamers instead of a holder per tool type
Where Collet Chuck Series DIN6388A Earns Its Place
Problems It Solves
- A tool held off centre drills oversize and wears on one flute only
- Set-screw holders grip at one point and let heavy-feed drills pull out of the holder
- Soft or poorly heat-treated collets lose their spring and stop clamping after repeated use
- A separate holder for every tool diameter ties up money and setup time
- Non-standard collets cannot be replaced locally when one is damaged
- Poor collet seating surfaces transfer their own error to every tool that goes into the spindle
Who It Is For
- Manufacturing plants standardising tool holding across their machines
- Machinery repair shops that see mixed tool shank sizes every day
- Machine tool distributors and tooling retailers stocking DIN6388 collets
- Workshops upgrading from set-screw holders to collet clamping
- OEM buyers who need collets supplied under their own brand
Application Scenarios
- Holding drills and reamers on drilling and boring machines where hole position depends on run-out
- Clamping end mills for milling where cutter concentricity controls tool life and finish
- Tapping work where the tool must be held concentric and released cleanly
- Tool changing on production machines where a standard collet size range replaces a set of holders
- Machinery repair shops holding a wide range of tool shank diameters on one spindle
- Building material and general workshops running mixed drilling and milling work
Technical Detail
Technical Features
- DIN6388A and DIN6388B EOC collet standard
- 65Mn special elastic spring steel material
- Hardness HRC48-52
- Run-out 0.008 mm to 0.015 mm
- Two precision classes 0.005 mm and 0.01 mm
- Precision ground with surface roughness within RZ2.5
- Suitable for drills taps end mills and reamers
- Used for boring milling and drilling operations
- OEM branding available
Specifications
| Machine type | Collet chuck and collet series (machine tool accessory) |
|---|---|
| Models | DIN6388A / DIN6388B EOC collet chuck series |
| Standard | DIN6388A / DIN6388B |
| Material | 65Mn elastic spring steel |
| Hardness | HRC48-52 |
| Run-out | 0.008 mm - 0.015 mm |
| Precision classes | 0.005 mm and 0.01 mm |
| Surface roughness | Within RZ2.5, precision ground |
| Tools held | Drills, taps, end mills, reamers |
| Operations | Boring, milling, drilling |
| Packing | Plastic box or to customer requirement |
| Branding | OEM available |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Boring
- Milling
- Drilling
- Tapping
- Reaming
Materials Handled
- 65Mn spring steel
Quality Control
- Run-out measured on each collet against the 0.008 mm to 0.015 mm specification
- Hardness checked after heat treatment to confirm HRC48-52
- Ground surface roughness inspected against the RZ2.5 requirement
- Collet bore and taper dimensions checked against DIN6388A/B
- Precision class sorted and marked at 0.005 mm or 0.01 mm before packing
Customisation Options
- Precision class selected at 0.005 mm or 0.01 mm according to your tolerance requirement
- DIN6388A or DIN6388B pattern supplied to match your existing holders
- Collet bore sizes made up as a set covering the shank diameters you run
- OEM branding and marking applied to your specification
- Packing in plastic box or to your own packaging requirement
How It Compares With the Alternatives
| Set-screw end mill holders | A set screw grips at one point and pushes the tool off centre; a collet closes around the whole shank, which is why run-out stays inside 0.015 mm |
|---|---|
| Drill chucks | A drill chuck is convenient for mixed work but its three jaws give more run-out and less holding force than a collet at the same size |
| Standard precision collets at 0.01 mm | The 0.005 mm precision class costs more but halves the concentricity error, which matters where hole size and cutter life are marginal |
| Non-standard collets | DIN6388A/B collets can be replaced from any supplier working to the standard, so a damaged collet does not stop the machine |
Running the Machine
Step 1
Select the collet whose nominal size matches the tool shank diameter you are clamping
Step 2
Wipe the collet the collet seat and the nut taper clean before assembly, chips there cause run-out
Step 3
Snap the collet into the nut first then thread the nut onto the chuck body
Step 4
Insert the tool to the correct clamping length and tighten the nut to the specified torque
Step 5
Check tool run-out with a dial indicator after clamping, especially on precision class work
Step 6
Release by unscrewing the nut, which withdraws the collet, never by hammering the tool
Step 7
Store collets in the supplied box so the clamping surfaces are not knocked or corroded
Related Applications and Guides
Engine Rebuilding Workshops
Engine rebuilding workshops recondition blocks heads crankshafts and valves to a geometry the engine will hold for a full service life. XAIMC supplies
General Machining Job Shops
Job shops take whatever work comes through the door, which means their equipment has to cover a wide range rather than do one thing perfectly. XAIMC s
Gear Hobbing Explained for Buyers of Gear Cutting Machines
Gear hobbing cuts gear teeth by rolling a rotating hob against a rotating blank so that the tooth form is generated rather than copied from a formed c
Radial Drilling Machine vs Bench Drilling Machine
A bench drilling machine brings the work to a fixed spindle, while a radial drilling machine moves the spindle over a heavy stationary workpiece on an
Questions About Collet Chuck Series DIN6388A
What run-out can I expect?
Run-out is 0.008 mm to 0.015 mm as standard. Two precision classes are available at 0.005 mm and 0.01 mm where you need tighter concentricity.
What material are the collets made from?
65Mn elastic spring steel, hardened to HRC48-52 and precision ground to a surface roughness within RZ2.5.
Which standard do they follow?
DIN6388A and DIN6388B in the EOC pattern, so they interchange with holders and nuts made to the same standard.
What tools can they hold?
Drills, taps, end mills and reamers, for boring milling and drilling work.
Can you supply under our own brand?
Yes, OEM branding is available. Send us your marking artwork and we will quote.
What are your payment and trade terms?
FOB CFR and CIF are available. Payment is 30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
What sizes should I order?
Send us the list of tool shank diameters you run and the holder taper on your machines, and we will make up the collet set that covers them.
Request a Quote on the Collet Chuck Series DIN6388A
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.