
EDM
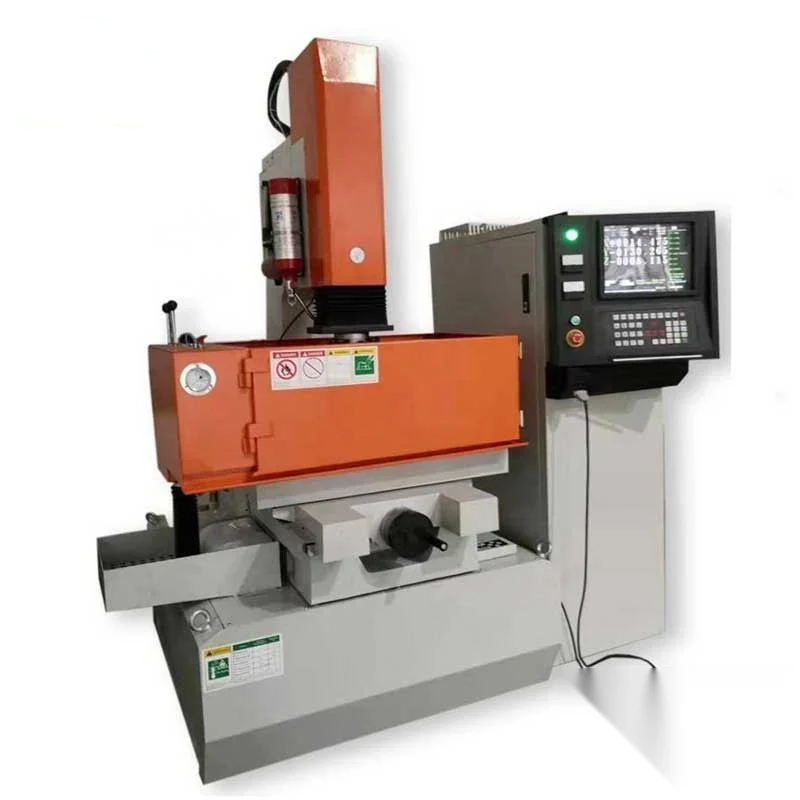
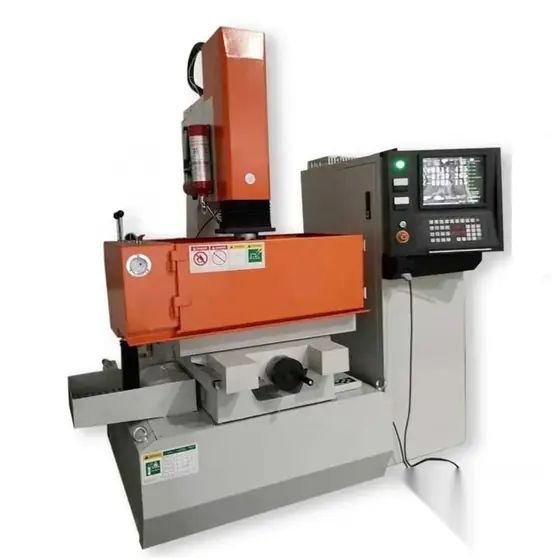
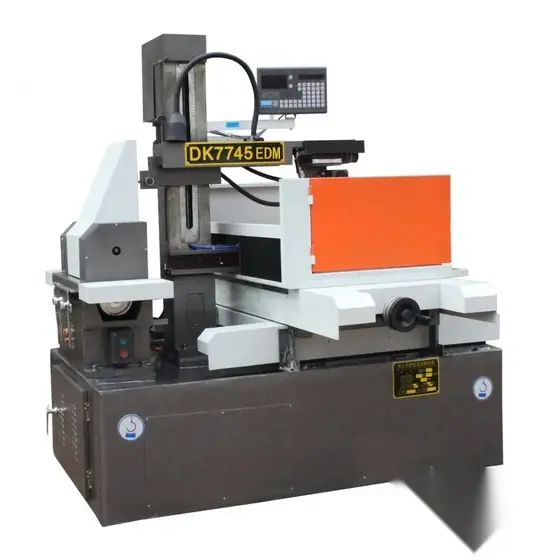
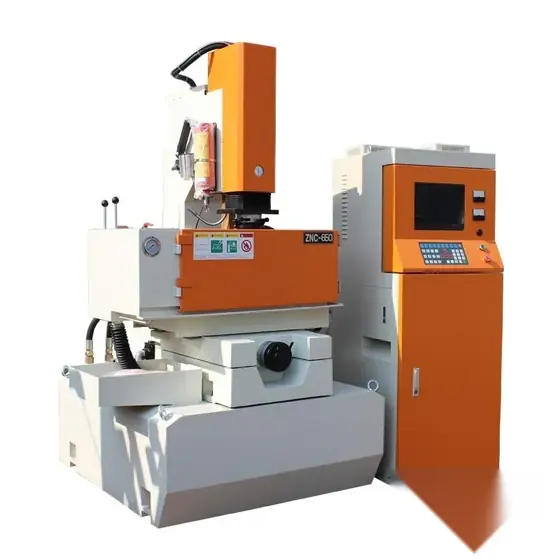
Wire cut and spark erosion CNC electrical discharge machines for hardened material and complex forms.
What This Category Is Really For
Once a die or punch is hardened, conventional cutting is finished. EDM removes material by spark erosion regardless of hardness, which is why die and mould shops cannot work without it — and why an unplanned die repair stops a press line until someone with EDM capacity can take it.
- Wire cut and spark erosion types in one range
- Cuts hardened tool steel without annealing and re-hardening
- CNC control for complex profiles that cannot be produced by milling
- Useful for extracting broken tooling from finished parts
Who Buys EDM Machines and Why
Who It Is For
- Die and mould shops
- Tool rooms supporting press operations
- Precision component manufacturers
- Repair shops extracting broken taps and drills
Where These Machines Are Used
- Cutting punches and die plates from hardened tool steel
- Producing complex internal profiles that a cutter cannot reach
- Sinking cavities in mould tooling
- Removing broken taps and drills from expensive workpieces
EDM Questions
Wire cut or spark erosion?
Wire cut for through profiles cut from plate. Spark erosion for blind cavities and forms sunk into a tool. Die and mould shops usually end up with both.
Does the material have to be conductive?
Yes. EDM works only on electrically conductive materials, which covers steels carbides and most tooling alloys.
Get a Quote on EDM Machines
Tell us the work you need the machine to do and we will confirm the model, the tooling and the lead time.