
Exporting a Cylinder Block and Cylinder Head Pressure Tester
An overseas engine rebuilding customer ordering a single machine to add pressure testing to an existing reconditioning workshop. The customer is not named here at their preference.
Project Challenge
Pressure testing is the step that decides whether the hours about to be spent on a block or head are worth spending. Without it, a crack is found after boring, honing and surfacing are already done — or worse, after assembly, when it comes back as a warranty engine. The workshop had the machining capability but no way to verify a casting before working on it.
Customer Pain Points
- Cracks discovered after machining time had already been invested in the casting
- Failures appearing after assembly rather than before it
- No objective record that a casting was sound before it entered the rebuild
- A single machine shipment still has to survive sea freight intact
Our Solution
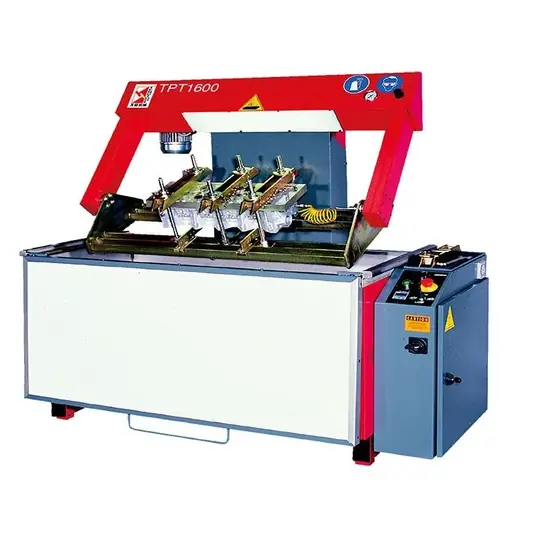
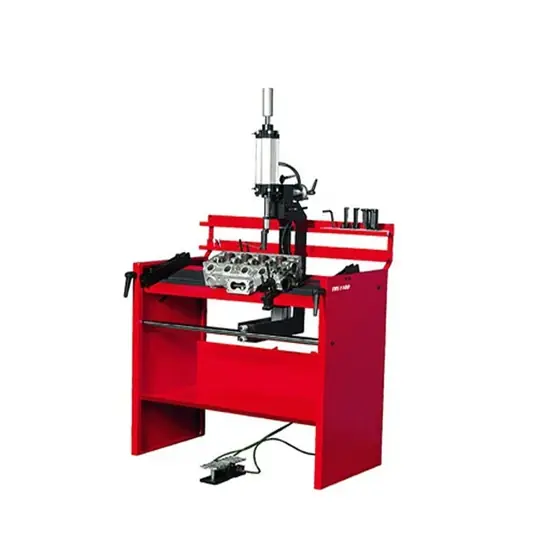
A cylinder block and cylinder head pressure tester was specified against the range of castings the workshop handles, built, tested and shipped as a single crated unit. The machine lets the shop verify a block or head before any machining time goes into it, which moves the reject decision to the cheapest possible point in the process.
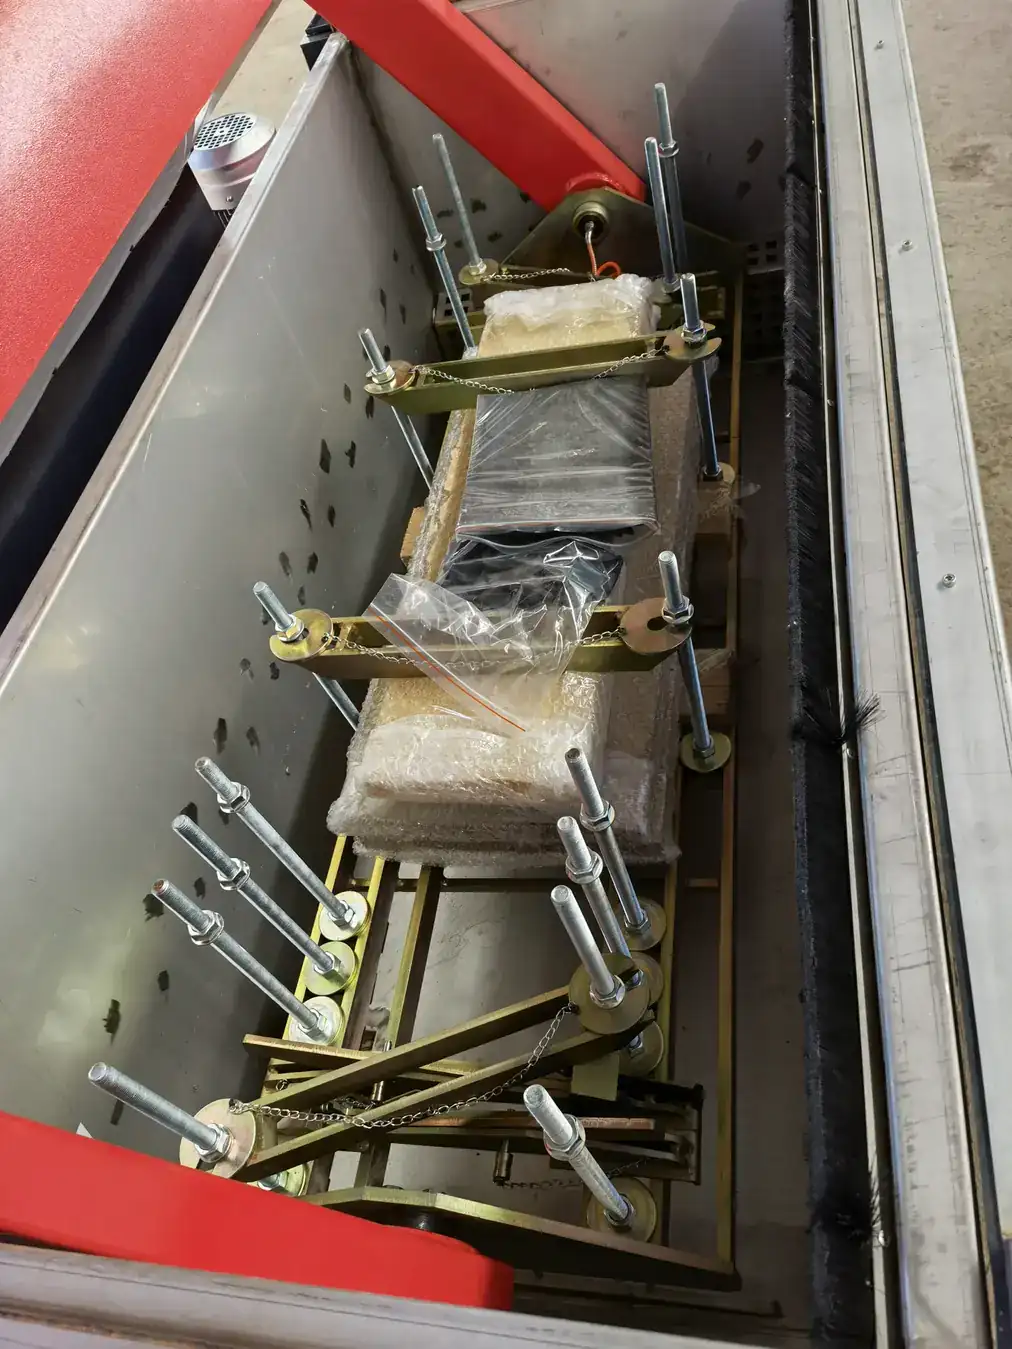
What We Photographed
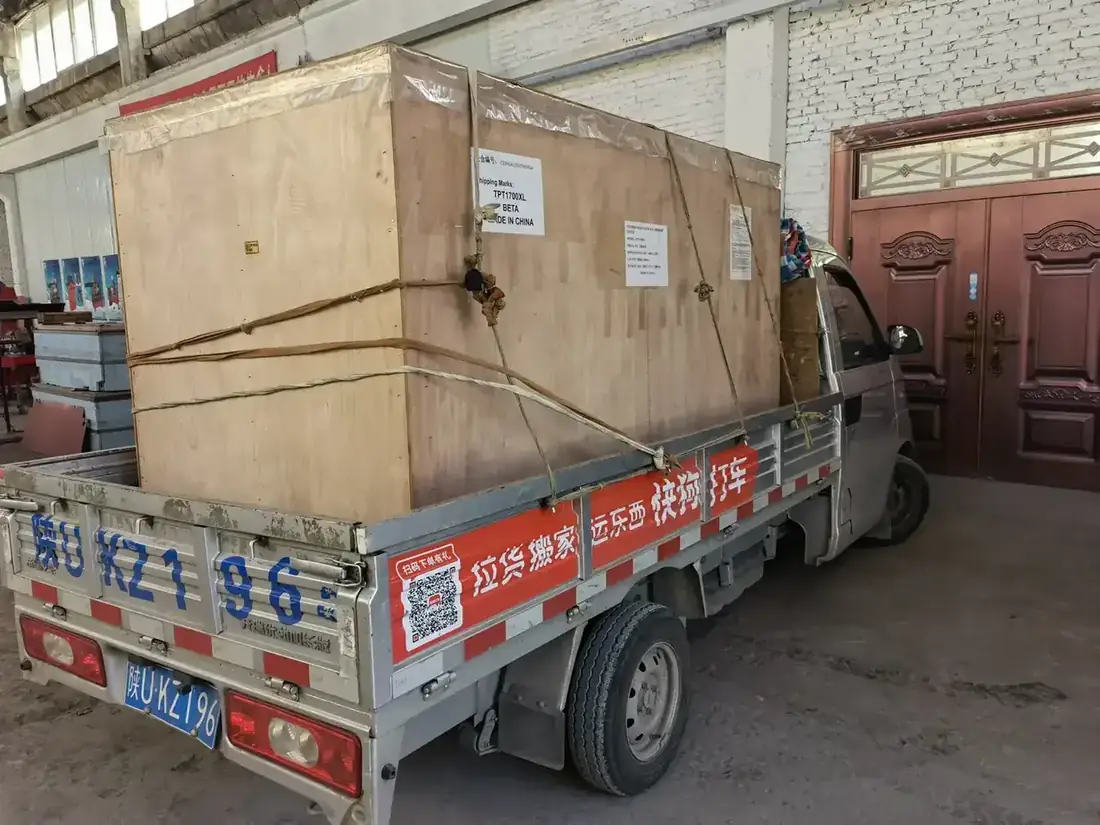
How It Was Built and Shipped
Manufacturing Process
- Machine specified against the customer's block and head size range
- Fabrication and machining completed in-house
- Assembly in the constant-temperature assembly workshop
- Painted on the automatic sheet-metal spraying line
- Function tested by the inspection department before packing
Supply Chain Coordination
Built, inspected, packed and despatched from the XAIMC works in Xi'an. The machine was crated for sea freight and loaded for onward transport to the port as a single consignment.
Quality Control
Function testing before packing, and a physical check that the crate was intact and correctly secured at loading. Photographs of the assembled machine and of the loaded crate were taken at despatch.
Final Result
The machine was completed, tested, crated and despatched to the customer in June 2022.
Customer Benefit
Pressure testing moved in-house and to the front of the rebuild sequence, so a cracked casting is now identified before machining hours are spent on it rather than after.
Engine Rebuilding Workshops
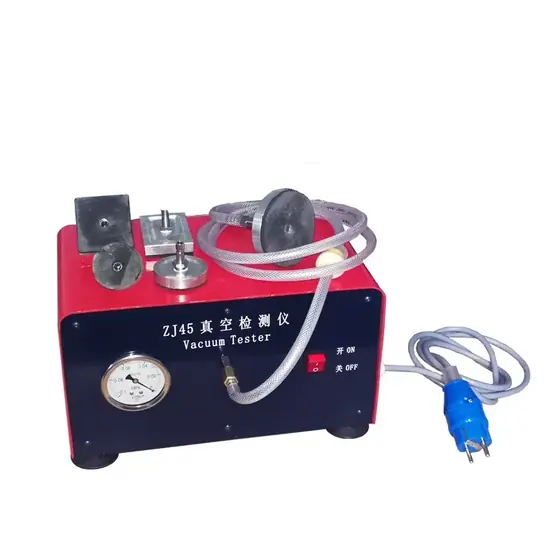
Engine rebuilding workshops recondition blocks heads crankshafts and valves to a geometry the engine will hold for a full service life. XAIMC supplies the boring honing grinding surfacing and testing machines those workshops run.
Talk To Us About a Similar Requirement
Send us the machine you need or the problem you are trying to solve. We will tell you what it takes.