
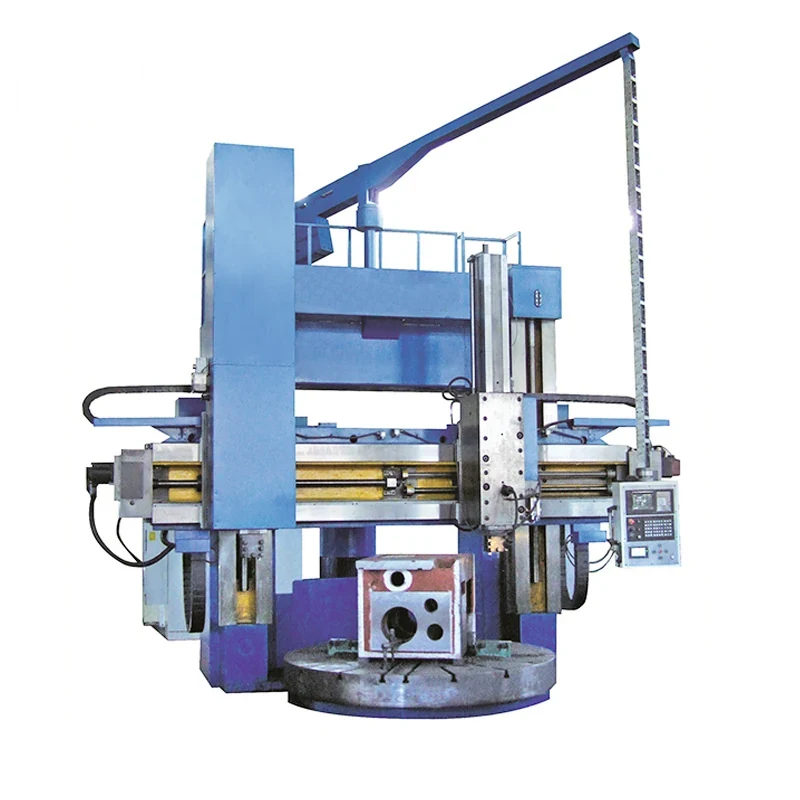
CK5225 Double Column Vertical CNC Lathe Machine
The CK5225 is the CNC version of the C52 double column vertical lathe, offered with the CK5231 and CK5240 as diameter increases. It covers internal and external turning, internal and external tapering, facing, slotting, threading and contour surface turning, the last of which is only practical under CNC control. The sp...
What This Machine Does
The CK5225 is the CNC version of the C52 double column vertical lathe, offered with the CK5231 and CK5240 as diameter increases. It covers internal and external turning, internal and external tapering, facing, slotting, threading and contour surface turning, the last of which is only practical under CNC control. The spindle drive uses servo motors through a two-step speed changing unit, so the table runs with stepless speed regulation rather than fixed gears. Wear is addressed where it actually happens: the vertical beam rail and ram guideways are super audio quenched to HRC 50 or above and the sliding surfaces carry a laminating treatment on both the swash plate surface and the iron mask, which is what holds accuracy and is stated to extend the overhaul period beyond ten years. The machine handles rough and fine turning of cylinders, round dimensional surfaces, ends and grooves across all sectors of machining.
Why Buyers Choose This Machine
- CNC control adds contour surface turning that a manual vertical lathe cannot produce
- Servo spindle drive through a two-step unit gives stepless table speed regulation
- Beam rail and ram guideways quenched to HRC 50 or above resist the wear that ends accuracy
- Laminating treatment on sliding surfaces including swash plate and iron mask preserves precision
- Overhaul period extended beyond ten years by the guideway treatment
- Rough and fine turning on the same machine so a part is finished in one setting
- Three frames CK5225 CK5231 and CK5240 covering rising diameters
Where CK5225 Double Column Vertical CNC Lathe Machine Earns Its Place
Problems It Solves
- Contoured and profiled surfaces cannot be turned repeatably by hand on a manual vertical lathe
- Fixed gear table speeds cannot hold surface speed as the tool moves across a large face
- Untreated guideways wear and the machine loses accuracy long before its structure is worn out
- Rough and fine turning split between machines introduces concentricity error
- Operator-dependent results in vertical turning vary between shifts
- Frequent overhauls of a large vertical machine take it out of production for weeks
Who It Is For
- Manufacturers of profiled rings discs and housings needing repeatable contours
- Wind energy pressure vessel and heavy machinery producers
- Shops moving from manual vertical turning to programmed production
- Plants that measure machine value by overhaul interval and accuracy retention
- Importers supplying CNC vertical turning capacity
Application Scenarios
- Contour surface turning of profiled discs and rings under CNC control
- Internal and external tapering of conical seats and housings
- Facing slotting and threading on large circular parts
- Rough and fine turning of the same casting in one setting
- Production batches where table speed has to change with diameter through the cut
- Machining across mixed sectors where part profiles change frequently
Technical Detail
Technical Features
- Double column vertical CNC lathe structure
- Servo motor spindle drive through a two-step speed changing unit
- Stepless table speed regulation
- Vertical beam rail and ram guideways super audio quenched to HRC 50 or above
- Laminating process on sliding surfaces including swash plate surface and iron mask
- Overhaul period stated at more than ten years
- Internal and external turning tapering facing slotting and threading
- Contour surface turning under CNC control
- Frames CK5225 CK5231 and CK5240
Specifications
| Machine type | Double column vertical CNC lathe |
|---|---|
| Models | CK5225 CK5231 CK5240 |
| Control | CNC with contour surface turning |
| Spindle drive | Servo motors through a two-step speed changing unit |
| Table speed | Stepless regulation |
| Guideway treatment | Super audio quenched to HRC 50 or above |
| Sliding surfaces | Laminating process on swash plate surface and iron mask |
| Overhaul period | More than 10 years |
| Operations | Internal and external turning tapering facing slotting threading contour turning |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Turning
- Facing
- Taper turning
- Slotting
- Thread cutting
- Contour turning
Quality Control
- Guideway hardness verified at HRC 50 or above after super audio quenching
- Laminating on sliding surfaces inspected before the beam and ram are assembled
- Servo drive and two-step unit tested across the stepless speed range
- CNC axes checked through a contour turning test cycle
- Full machine run and inspected before it is prepared for shipment
Certifications
- CE
Customisation Options
- Frame selected from CK5225 CK5231 or CK5240 by part diameter
- CNC configuration and operating language set for your shop
- Tool rest and tooling package specified for your materials and profiles
- Supply voltage frequency and phase built for your site
- Foundation and installation drawings prepared for the frame ordered
How It Compares With the Alternatives
| Manual Vertical Turret Lathe C5225 | Same double column family and frame size, but the CNC build adds contour surface turning servo drive and stepless table speed, and repeats a profile part after part |
|---|---|
| Vertical lathe with geared table drive | Servo drive through a two-step unit holds surface speed as the tool crosses a large diameter, where gears force a compromise |
| Untreated guideway machines | Quenching to HRC 50 or above plus the laminating process on sliding surfaces is what keeps the machine accurate and pushes the overhaul interval past ten years |
| Splitting roughing and finishing across two machines | Rough and fine turning in one setting on the CK5225 removes the re-clamping error between the two operations |
Running the Machine
Step 1
Clamp the workpiece on the table and check run-out before the first program run
Step 2
Load or write the program for the profile including rough and fine passes
Step 3
Let the servo drive set the table speed for each diameter rather than fixing one speed
Step 4
Prove the contour on the first part and inspect before running the batch
Step 5
Keep roughing and finishing in the same setting to preserve concentricity
Step 6
Keep the guideway sliding surfaces clean so the laminated surfaces are not scored by chips
Step 7
Follow the lubrication and CNC maintenance schedule to protect the overhaul interval
Related Applications and Guides
General Machining Job Shops
Job shops take whatever work comes through the door, which means their equipment has to cover a wide range rather than do one thing perfectly. XAIMC s
Heavy Equipment and Plant Maintenance
Mines quarries plantations and processing plants cannot wait for imported spares. XAIMC supplies the boring gear cutting turning and grinding machines
Machine Tool Installation and Commissioning Checklist
Installing an imported machine tool correctly means preparing the site, unpacking and positioning the machine, levelling it, connecting services and p
Preventive Maintenance for Manual Lathes and Milling Machines
Manual lathes and milling machines keep their accuracy through lubrication, cleanliness, correct adjustment of gibs and backlash, and regular geometri
Questions About CK5225 Double Column Vertical CNC Lathe Mach
What does the CNC version add over the manual C5225?
Contour surface turning, servo spindle drive with stepless table speed, and repeatable programmed cycles. A manual machine cannot hold a profiled contour part after part.
Which frame should I order?
CK5225, CK5231 and CK5240 differ in diameter capacity. Send us your maximum part diameter, height and weight and we will confirm the frame.
How hard are the guideways?
The vertical beam rail and ram guideways are super audio quenched to HRC 50 or above, with a laminating treatment on the sliding surfaces.
How long between overhauls?
The guideway treatment is stated to extend the overhaul period beyond ten years in normal service. Actual intervals depend on your duty and maintenance.
Which CNC system is used and in what language?
The control and operating language are set with the order. Tell us what your operators and maintenance team already support.
What foundation and shipping arrangements are needed?
We supply the installation and foundation drawing for the frame ordered, and the machine is shipped for sea freight from Xi'an on FOB CFR or CIF terms.
What are your payment terms?
30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
Request a Quote on the CK5225 Double Column Vertical CNC Lathe Mach
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.