
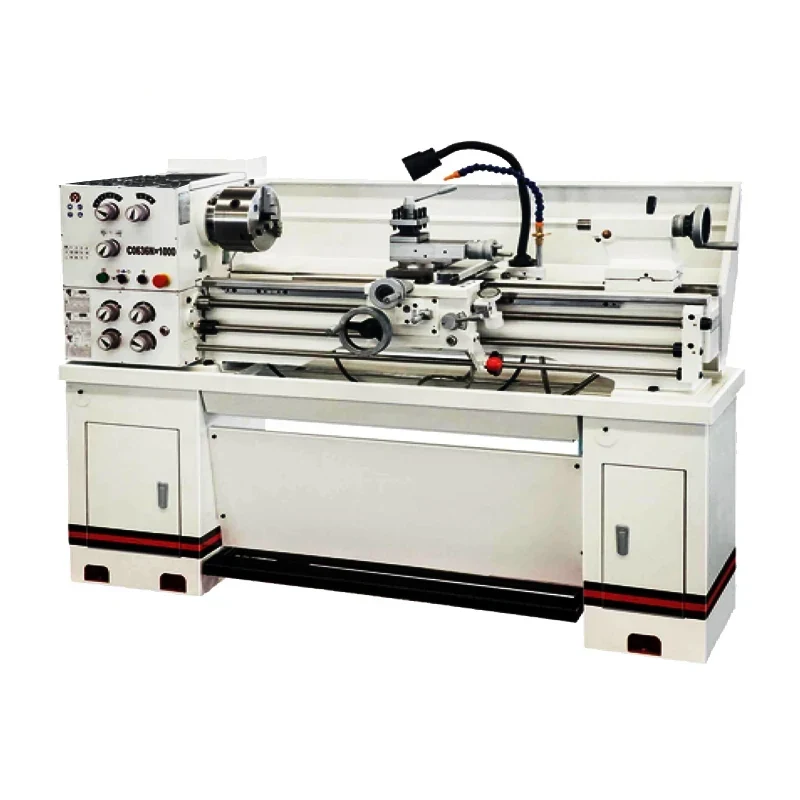
C0636N Bench Metal Lathe Machine
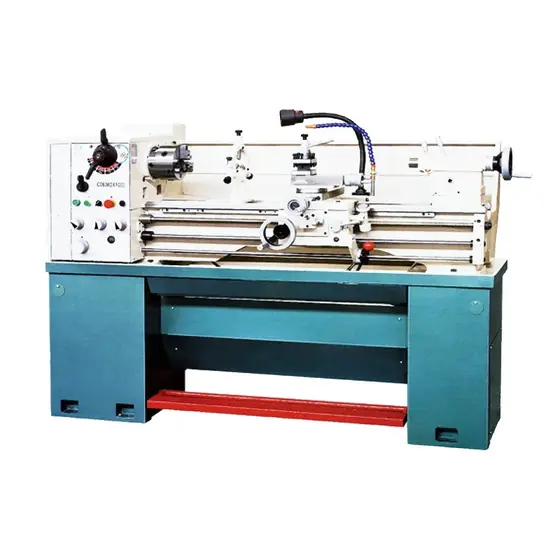
The C0636N is a bench metal lathe for machining and repair shops working on shafts, spindles, sleeves and small to medium disc parts. It swings 360mm over the bed, 223mm over the support and 502mm over the gap, with a 179mm centre height and 1000mm between centres on a bed 187mm wide and 290mm high. The feature that se...
What This Machine Does
The C0636N is a bench metal lathe for machining and repair shops working on shafts, spindles, sleeves and small to medium disc parts. It swings 360mm over the bed, 223mm over the support and 502mm over the gap, with a 179mm centre height and 1000mm between centres on a bed 187mm wide and 290mm high. The feature that sets it apart in this size class is the 52mm through-hole spindle bore, which lets larger bar stock pass through the headstock instead of being held out in front of the chuck. The spindle uses a D1-5 cam lock system and an MT No.6 taper and runs from 70 to 2000 r.p.m., driven by a 1.5kw motor wired for 220V or 380V. Cross slide travel is 160mm, compound slide travel 95mm, the lead screw is 22mm and the feed rod 19mm, with a tool post for 16mm by 16mm tooling. It cuts imperial, diametric and module threads, and the compact construction keeps it quiet and easy to service.
Why Buyers Choose This Machine
- 52mm through-hole spindle bore takes larger bar than most bench machines of this swing
- 502mm gap swing lets discs and flanges be faced without moving the job to a bigger lathe
- D1-5 cam lock spindle nose makes chuck changes fast and repeatable
- 70-2000 r.p.m. from a 1.5kw motor covers roughing at full swing and finishing at small diameters
- Imperial diametric and module threading covers repair work beyond plain metric pitches
- Supplied for 220V or 380V so the same machine suits single and three phase shops
- Compact construction with low noise and straightforward access for repair
Where C0636N Bench Metal Lathe Machine Earns Its Place
Problems It Solves
- Small spindle bores force long bar to project dangerously from the chuck
- Disc and flange work larger than the bed swing has to be subcontracted without a gap
- Module and diametric threads normally require special change gear sets
- Shops with only single phase supply cannot run a 380V-only machine
- Threaded spindle noses waste time on every chuck change
- Noisy loose bench lathes lose accuracy and are unpleasant to work beside all day
Who It Is For
- Machining and tool room shops handling mixed shaft and disc work
- Repair workshops needing a bench lathe with a large through bore
- Small production shops running short bar-fed batches
- Training workshops teaching turning and multi-system threading
- Distributors supplying light and medium engineering shops
Application Scenarios
- Bar work up to 52mm fed through the spindle for repeat turned parts
- Turning shafts and spindles up to 1000mm between centres
- Facing and boring discs and flanges up to 502mm in the gap
- Cutting imperial diametric and module threads for gear and repair work
- Sleeve and bush machining in a tool room or repair shop
- Middle and small disc work where a floor lathe would be oversized
Technical Detail
Technical Features
- 52mm through-hole spindle bore
- D1-5 cam lock spindle system with MT No.6 taper
- Spindle speed range 70-2000 r.p.m.
- 1.5kw motor for 220V or 380V supply
- Gap bed giving 502mm swing over the gap
- Cross slide travel 160mm and compound slide travel 95mm
- Lead screw 22mm diameter and feed rod 19mm
- Tool post for 16mm x 16mm tooling
- Imperial diametric and module thread cutting
Specifications
| Machine type | Bench metal lathe |
|---|---|
| Models | C0636N |
| Swing over bed | 360mm |
| Swing over support | 223mm |
| Swing over gap | 502mm |
| Centre height | 179mm |
| Distance between centres | 1000mm |
| Bed width | 187mm |
| Bed height | 290mm |
| Spindle bore | 52mm |
| Spindle nose | D1-5 cam lock |
| Spindle taper | MT No.6 |
| Spindle speed | 70-2000 r.p.m. |
| Motor output | 1.5kw |
| Voltage | 220V or 380V |
| Cross slide travel | 160mm |
| Compound slide travel | 95mm |
| Lead screw diameter | 22mm |
| Feed rod diameter | 19mm |
| Cutting tool max section | 16mm x 16mm |
| Threading | Imperial diametric and module threads |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Turning
- Facing
- Boring
- Thread cutting
- Taper turning
- Parting
Quality Control
- Spindle bore concentricity and run-out checked with the D1-5 nose assembled
- Speed range verified from 70 to 2000 r.p.m. under the 1.5kw drive
- Gap piece fit and bed alignment checked with the gap in and out
- Thread chart positions exercised and a sample thread cut and measured
- Motor and electrics tested at the 220V or 380V supply specified on the order
Customisation Options
- Wired for 220V or 380V and for your frequency and phase
- Chuck steady rest follow rest and tool post package selected with the order
- Standard and optional accessory sets quoted against the work you run
- Manual and machine plates prepared in your language
- Export packing for sea or air shipment
How It Compares With the Alternatives
| Bench lathes with a small spindle bore | The 52mm through hole takes bar that smaller-bore machines of the same swing cannot pass through the headstock |
|---|---|
| Horizontal Bench Type Lathe Machine C0632A | The C0632A is the smaller frame; the C0636N gives 360mm swing 502mm in the gap and a 52mm bore on a 187mm bed |
| Floor-standing engine lathe of similar swing | The C0636N keeps compact construction and bench mounting, which matters when floor area rather than capacity is the limit |
| Turning discs on a vertical or manual fixture | The gap and the 179mm centre height let a 502mm disc be turned and bored in one concentric setup |
Running the Machine
Step 1
Mount the lathe on a rigid bench and level it before the first cut
Step 2
Check that bar passed through the 52mm bore is supported and guarded behind the headstock
Step 3
Fit the chuck on the D1-5 cam lock nose and lock every cam to its mark
Step 4
Set the spindle speed within 70-2000 r.p.m. for the diameter and material
Step 5
Select the thread system and pitch from the chart before engaging the lead screw
Step 6
Remove the gap piece only for large diameter work and refit it for shaft turning
Step 7
Clean and lubricate the ways lead screw and feed rod at the end of each shift
Related Applications and Guides
General Machining Job Shops
Job shops take whatever work comes through the door, which means their equipment has to cover a wide range rather than do one thing perfectly. XAIMC s
Heavy Equipment and Plant Maintenance
Mines quarries plantations and processing plants cannot wait for imported spares. XAIMC supplies the boring gear cutting turning and grinding machines
Machine Tool Installation and Commissioning Checklist
Installing an imported machine tool correctly means preparing the site, unpacking and positioning the machine, levelling it, connecting services and p
Preventive Maintenance for Manual Lathes and Milling Machines
Manual lathes and milling machines keep their accuracy through lubrication, cleanliness, correct adjustment of gibs and backlash, and regular geometri
Questions About C0636N Bench Metal Lathe Machine
How large a bar can pass through the spindle?
Up to 52mm through the spindle bore. Larger stock has to be chucked and supported at the tailstock.
What is the largest diameter it will swing?
360mm over the bed, 223mm over the support and 502mm over the gap. Centre height is 179mm and centre distance 1000mm.
Can it run on single phase?
The 1.5kw motor is supplied for 220V or 380V. Tell us your voltage phase and frequency with the order and we will wire it accordingly.
Which threads can it cut?
Imperial, diametric and module threads. Send us the specific pitches you need and we will confirm they are on the chart of your machine.
What chucks fit the spindle?
Any correctly backed D1-5 cam lock chuck or face plate. We can supply the chuck set with the machine if you tell us the sizes.
What is the lead time and how is it packed?
Lead time depends on the accessory package; send us the configuration and we will confirm. Machines are packed for sea or air freight and shipped FOB CFR or CIF.
What are your payment terms?
30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
Request a Quote on the C0636N Bench Metal Lathe Machine
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.