
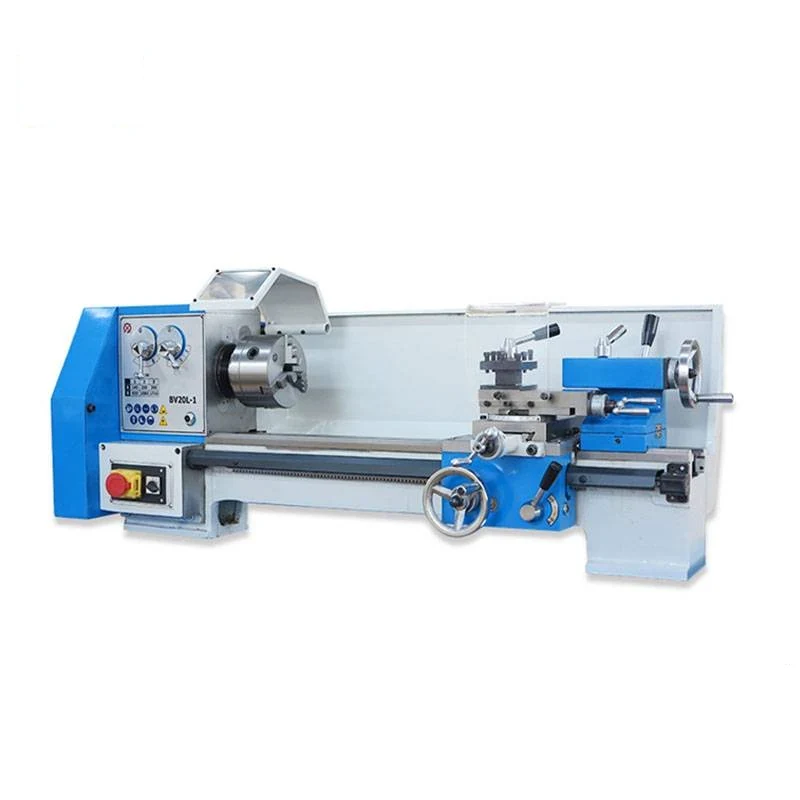
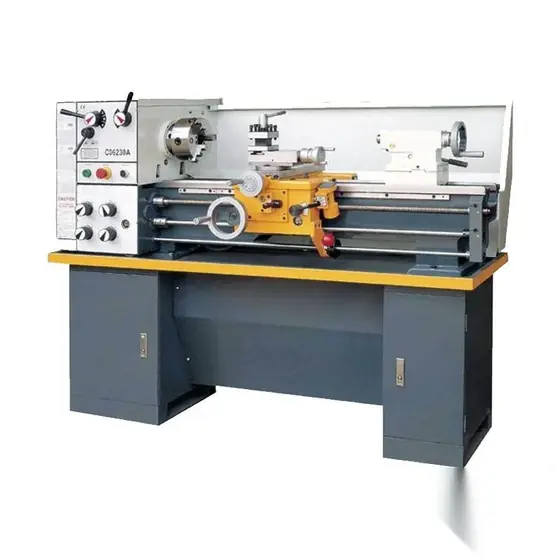
BV20-1/BV20L-1 Manual Small Bench Lathe Machine
The BV20-1 is a manual bench lathe for the small turning jobs a workshop needs done the same day: a bush, a shaft repair, a spacer, a thread to fit a part that is no longer available. Swing over the bed is 220mm and swing over the cross slide 120mm, with 350mm between centres on the BV20-1 and 520mm on the long-bed BV2...
What This Machine Does
The BV20-1 is a manual bench lathe for the small turning jobs a workshop needs done the same day: a bush, a shaft repair, a spacer, a thread to fit a part that is no longer available. Swing over the bed is 220mm and swing over the cross slide 120mm, with 350mm between centres on the BV20-1 and 520mm on the long-bed BV20L-1. The spindle bore is 20mm with an MT3 taper, running in precision roller bearings, and the bed ways are hardened by supersonic frequency treatment then ground, which is what keeps the carriage accurate rather than wearing a hollow at the chuck end. Headstock gears are made of steel that is ground and hardened. Six spindle speed steps cover 140 to 1710 r.p.m., and the lathe cuts 11 kinds of metric thread from 0.4 to 3mm and 11 kinds of imperial thread from 8 to 28 per inch. Main motor is 750W.
Why Buyers Choose This Machine
- Supersonic frequency hardened and ground bed ways keep carriage accuracy as the machine is used
- Precision roller bearings on the spindle for steady running at the 140 to 1710 r.p.m. speed range
- Ground and hardened steel headstock gears in place of soft gears that wear quickly
- 11 metric threads from 0.4 to 3mm and 11 imperial threads from 8 to 28 per inch cut on the machine
- BV20L-1 gives 520mm between centres where the standard 350mm is not enough
- 220mm swing over bed and 20mm spindle bore cover the usual small repair work
- 125 kg net weight and a 1254x575x600mm packing size so it installs on a bench not a foundation
Where BV20-1 Earns Its Place
Problems It Solves
- Waiting days for a simple turned part stops a repair that could be finished the same day
- Soft unhardened bed ways wear at the chuck end and the lathe loses accuracy
- Soft headstock gears fail early under repeated speed changes
- Obsolete threads cannot be bought and must be cut
- A full-size lathe needs floor space and a foundation a small workshop does not have
Who It Is For
- Maintenance workshops making their own small replacement parts
- Repair shops that need occasional turning without a full machine shop
- Technical schools and training centres
- Distributors supplying small workshop machine tools in export markets
Application Scenarios
- Turning a replacement bush or spacer when the original part is unavailable
- Cutting a metric or imperial thread on a repair component
- Facing and reducing a small shaft during a machine repair
- Training work in a technical school or workshop apprentice bay
- Small batch turned parts in a maintenance workshop
- Longer shaft work up to 520mm between centres on the BV20L-1
Technical Detail
Technical Features
- Supersonic frequency hardened bed way, ground after hardening
- Spindle running in precision roller bearings
- Ground and hardened steel gears inside the headstock
- Six steps of spindle speed from 140 to 1710 r.p.m.
- Metric thread cutting 11 kinds from 0.4 to 3mm
- Imperial thread cutting 11 kinds from 8 to 28 per inch
- MT3 spindle taper and MT2 tailstock taper
- 45mm tailstock quill travel 115mm cross travel and 63mm compound travel
Specifications
| Machine type | Manual small bench lathe |
|---|---|
| Models | BV20-1 / BV20L-1 |
| Swing over bed | 220mm |
| Distance between centres | 350 / 520mm |
| Swing over cross slide | 120mm |
| Spindle bore | 20mm |
| Spindle taper | MT3 |
| Steps of spindle speed | 6 |
| Range of spindle speed | 140-1710 r.p.m. |
| Metric threads | 11 kinds / 0.4-3mm |
| Imperial threads | 11 kinds / 8-28 per inch |
| Tailstock quill travel | 45mm |
| Cross travel | 115mm |
| Compound travel | 63mm |
| Tailstock spindle taper | MT2 |
| Main motor | 750W |
| Packing size | 1254x575x600mm |
| Net / gross weight | 125 / 140 kgs |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Turning
- Facing
- Thread cutting
- Drilling from the tailstock
Quality Control
- Bed way hardness and ground finish checked after the supersonic frequency treatment
- Spindle run-out measured at the MT3 nose on the assembled headstock
- Spindle speeds verified at each of the six steps across 140 to 1710 r.p.m.
- Thread pitches test cut and checked against the metric and imperial charts
- Machine run in and a test part turned before packing
Customisation Options
- BV20-1 at 350mm or BV20L-1 at 520mm between centres according to your longest workpiece
- Chuck steady and tooling package quoted with the machine
- Supply voltage and frequency set for your market for the 750W motor
- Metric or imperial thread chart supplied according to your workshop practice
- Manual prepared in your working language
How It Compares With the Alternatives
| BVB25 3in1 multipurpose milling drilling machine | The BVB25 adds milling and drilling on the same base; the BV20-1 stays a dedicated lathe with a smaller 220mm swing for bench installation |
|---|---|
| Universal desktop lathe machine BL1224 | The BL1224 gives a larger 305mm swing 12 speeds and a gap bed; the BV20-1 is the lighter 125 kg machine for small parts |
| Buying small turned parts outside | Turning a bush or a thread in-house on the BV20-1 removes the wait and keeps the repair moving |
Running the Machine
Step 1
Bolt the lathe down on a solid bench and check it is level
Step 2
Mount the work in the chuck within the 220mm swing and 350 or 520mm between centres
Step 3
Select one of the six spindle speeds for the material and diameter
Step 4
Set the tool on centre height and take a light first cut
Step 5
Use the 115mm cross travel and 63mm compound travel for the cut you need
Step 6
For threading select the metric or imperial pitch from the chart and engage the feed
Step 7
Support long work with the tailstock through its 45mm quill travel
Related Applications and Guides
General Machining Job Shops
Job shops take whatever work comes through the door, which means their equipment has to cover a wide range rather than do one thing perfectly. XAIMC s
Heavy Equipment and Plant Maintenance
Mines quarries plantations and processing plants cannot wait for imported spares. XAIMC supplies the boring gear cutting turning and grinding machines
Machine Tool Installation and Commissioning Checklist
Installing an imported machine tool correctly means preparing the site, unpacking and positioning the machine, levelling it, connecting services and p
Preventive Maintenance for Manual Lathes and Milling Machines
Manual lathes and milling machines keep their accuracy through lubrication, cleanliness, correct adjustment of gibs and backlash, and regular geometri
Questions About BV20-1
What is the difference between BV20-1 and BV20L-1?
Bed length. The BV20-1 has 350mm between centres and the BV20L-1 has 520mm. Send us your longest workpiece and we will confirm which you need.
What threads can it cut?
11 kinds of metric thread from 0.4 to 3mm and 11 kinds of imperial thread from 8 to 28 per inch.
What is the spindle bore and taper?
20mm bore with an MT3 taper. The tailstock spindle takes MT2.
How heavy is the machine and how is it packed?
125 kg net and 140 kg gross, packed at 1254x575x600mm, so it ships easily and installs on a bench.
What power supply does it need?
The main motor is 750W. We set the voltage and frequency for your market, so confirm your supply on the order.
Are the bed ways hardened?
Yes. The bed way is supersonic frequency hardened and then ground, and the headstock gears are steel, ground and hardened.
What are your payment and trade terms?
FOB CFR and CIF. Payment is 30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
Request a Quote on the BV20-1
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.