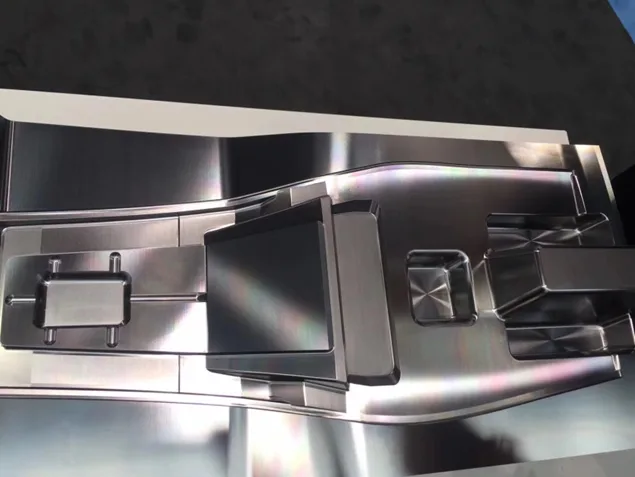
Polished Cavity Insert for Automotive Trim
Machined and polished insert carrying a long automotive trim form with sharp shut-offs.
Polished Cavity Insert for Automotive Trim
Polished Cavity Insert for Automotive Trim is one of the parts molded on tooling built at our Dongguan shop. Machined and polished insert carrying a long automotive trim form with sharp shut-offs.
Before any steel is roughed we run the filling, packing, warpage and cooling study, so the cooling layout on this tool comes out of the analysis rather than out of habit.
Final mold inspection and packing inspection are the last two steps before shipment, because a tool that passes trial can still arrive damaged.
Key Benefits
- Full 3D design issued in your own CAD format
- A written DFM before fabrication, so changes happen while they are still cheap
- Final mold and packing inspection before the tool is shipped
- ISO 9001:2015 quality management covering design, manufacture and service
Problems It Solves
- Weld lines landing on a visible face because gating was chosen for fill alone
- Cavity finishes agreed after the steel was cut instead of before
- Warpage found at assembly rather than in the cooling study
Who It Is For
- Tool shops outsourcing overflow cavity and core work
- Mold owners needing spare or replacement inserts
- OEMs holding their own tools and buying consumable components
- Buyers needing electrode and insert work with an inspection record
Application Scenarios
- Cavity and core plates for production molds
- Slide blocks, lifters and shut-off inserts
- Core pins, blades and ground details
- Replacement inserts for tools already in production
How the Tool Behind Polished Cavity Insert for Automotive Trim Is Built
- Design
Full 3D mold design completed to one hundred percent and checked in a design review meeting.
- DFM and MoldFlow
A written DFM for your comment, and filling, packing, warpage and cooling analysis on mass production tools.
- Machining
CNC and EDM work with steel inspected dimensionally after machining and electrodes inspected before burning.
- Trial and inspection
Mold trial with trial report and sample dimension report, then final mold and packing inspection.
Technical Data
The source material for this site records the part, its category and the photograph. Dimensions, resin grade, cavity count and tolerances are project data and are confirmed in the quotation.
| Product name | Polished Cavity Insert for Automotive Trim |
|---|---|
| Reference on our catalogue | Mold Component 1 |
| Category | Mold Components |
| Process | Plastic injection molding |
| Tooling built by | Dongguan JEC Mold Co., Limited, Dongguan, China |
| Designed tool life | More than 1 million shots |
| Mold standard | Customer standard, or DME / Meusburger / HASCO / Progressive / MISUMI |
| Design data formats | STEP, IGES, Parasolid, CATIA, SolidWorks |
| Quality system | ISO 9001:2015 — Design, Manufacture and Service of Injection Molded Moulds; Manufacture and Service of Plastic Injection Molded Parts |
| Part dimensions | TBC — confirmed in the quotation |
| Resin or alloy grade | TBC — confirmed in the quotation |
| Cavity count | TBC — confirmed in the quotation |
| Dimensional tolerance | TBC — confirmed in the quotation |
| Surface finish | TBC — confirmed in the quotation |
| Annual volume | TBC — confirmed in the quotation |
What Is Checked
- Customer mold specification and requirement review and discussion during the kick-off meeting
- 3D and 2D mold design review meeting before the design is sent to you, and a final check before fabrication
- Incoming material inspection
- Steel hardness inspection and steel certification
- Electrode dimension and surface finish inspection
- Steel dimension inspection after machining
- Mold trial reports with a sample dimension report (FAI)
- Final mold inspection and packing inspection
Certification
ISO 9001:2015 — scope: Design, Manufacture and Service of Injection Molded Moulds; Manufacture and Service of Plastic Injection Molded Parts.
Customization
Mold standard, cavity count, gating strategy, surface finish and mold base supplier are all specified per project. Tell us what your own standard requires and it is folded into the DFM rather than handled as a change later.
Compared With a Prototype Tool
A production mold for Polished Cavity Insert for Automotive Trim is built to run for more than 1 million shots and is documented with a trial report and a sample dimension report. A rapid prototype mold answers a different question — is the design right — at a lower price and a faster lead time, and is not built for that life. If the design is still moving, the prototype stage is usually the cheaper route into the production tool.
Rapid Prototype MoldsUse Guide
- Send 3D part data in STEP, IGES, Parasolid, CATIA, SolidWorks
- State the resin or alloy, the annual volume and the mold standard
- Comment on the DFM before fabrication — that is the cheapest point to change anything
- Review the trial report and sample dimension report against your own drawing before release
- Keep the mold standard on file so spares stay available locally
Others in Mold Components
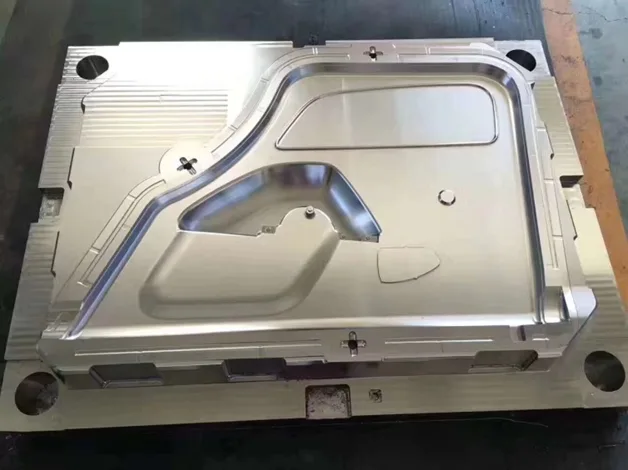
Cavity Plate for Appliance Panel
Large cavity plate with a deep panel form, guide bores and a full cooling pattern.
View details →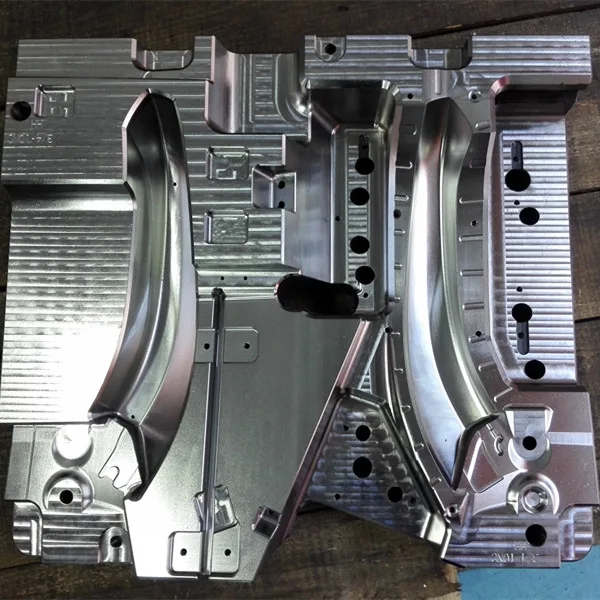
Mold Plate with Lamp Housing Cavity
Plate carrying a curved lamp housing cavity with slide pockets and ejector bores.
View details →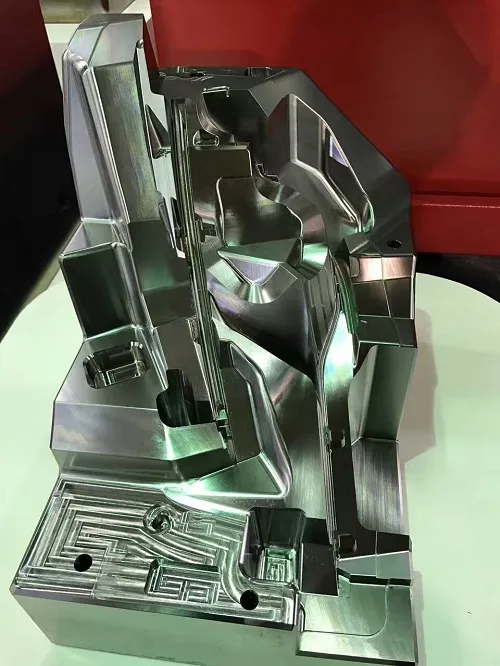
Precision Core Insert Block
Tall machined core block with stepped faces, deep slots and interlocking shut-offs.
View details →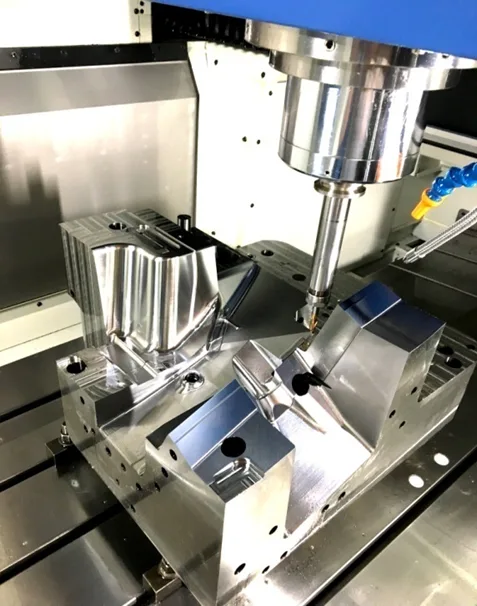
CNC Machined Mold Inserts
Set of inserts on the machine table, cut in one clamping for form accuracy.
View details →Polished Cavity Insert for Automotive Trim — Buyer Questions
Do you make the part as well as the mold for Polished Cavity Insert for Automotive Trim?
We can. Mold-making is ninety percent of our business and injection production is the other ten percent, and both sit inside the same ISO 9001:2015 scope.
Do you run MoldFlow before building the mold for Polished Cavity Insert for Automotive Trim?
For mass production molds, yes. We run the practical study in four stages — filling, then packing, then warpage, then cooling — and the cooling layout is designed from the result.
How are molds packed for export?
Final mold inspection is followed by a packing inspection before the tool leaves. Ninety percent of our molds go to overseas markets, so export packing is the normal case here rather than the exception.
Who do we talk to during the project?
Our engineering team has been trained on customer mold standards and corresponds in English. Response to customers is no later than 24 hours.
Quote Polished Cavity Insert for Automotive Trim
Send the 3D data, the resin and the annual volume. A professional quotation with technical comment comes back within two working days.