- Home
- Machines
- Automatic Concrete Block Machine
- QT8-15 Automatic Hollow Block Making Machine
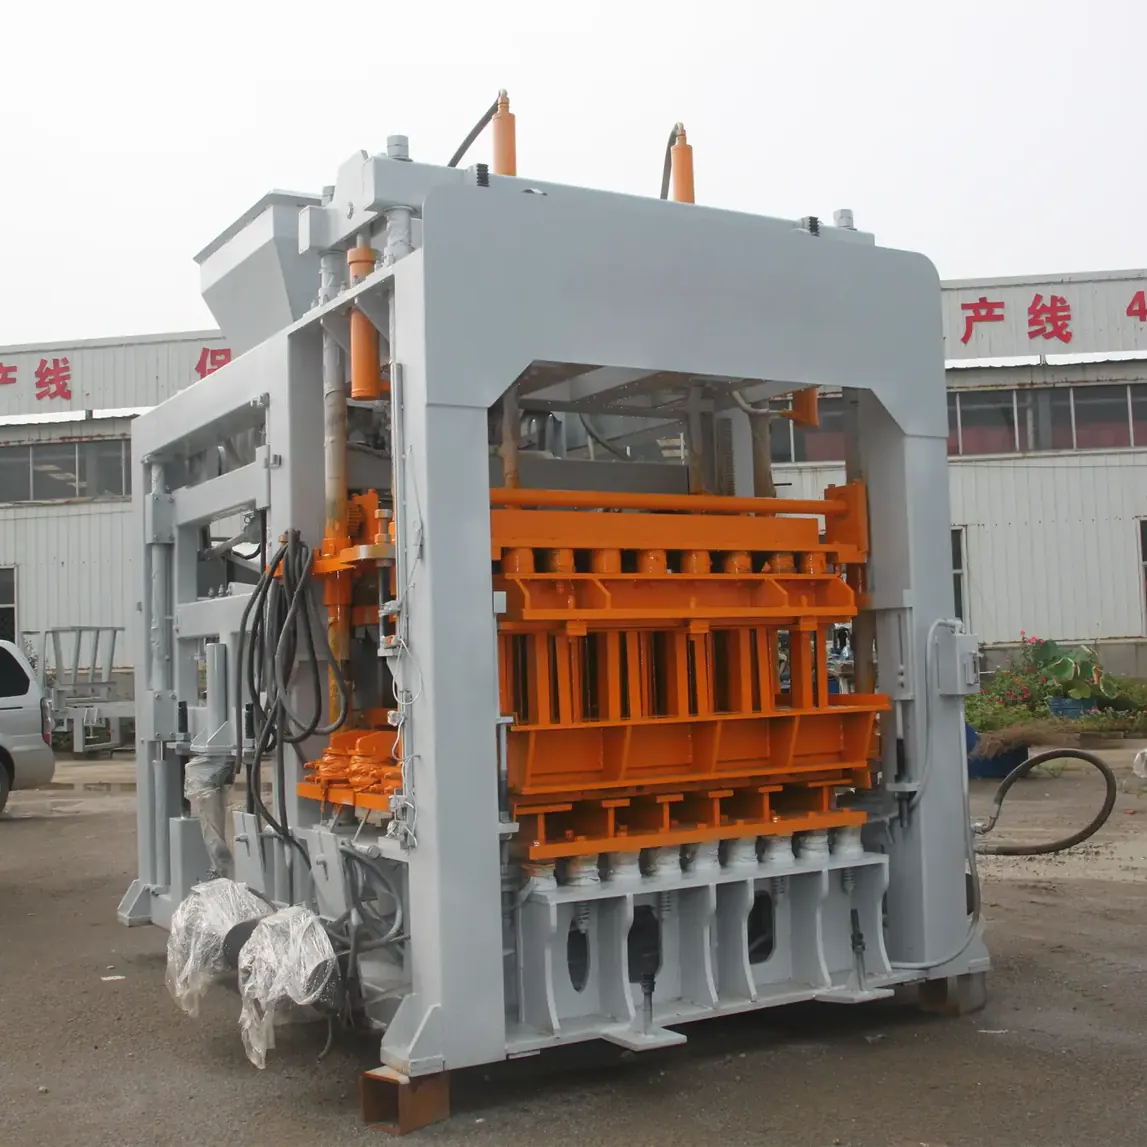
QT8-15 Automatic Hollow Block Making Machine
90 kN hydraulic automatic machine moulding eight hollow blocks per cycle, 15360 blocks per 8 hour shift.
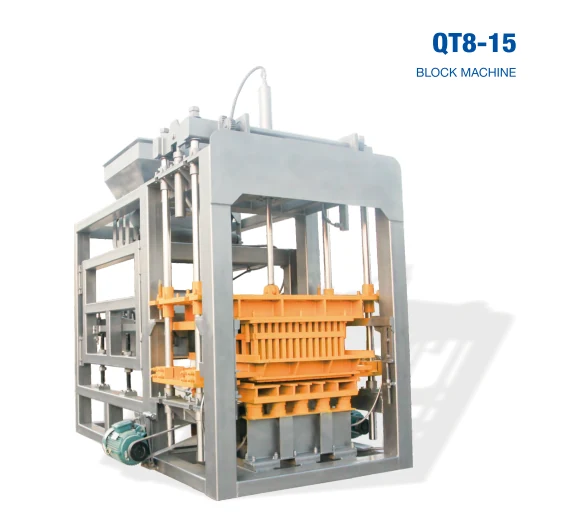
Machine Overview
The QT8-15 is the first machine in the range at 90 kN vibration force. Eight hollow blocks are moulded per cycle on a 960 x 870 mm pallet, giving 1920 pieces per hour and 15360 per 8 hour shift. Hydraulic pressure moulding keeps the press stable at that rate, and the electrical package is specified around Omron or Schneider switches with Siemens or ABB motors so the line runs with a low failure rate on continuous shifts.
Key Benefits
- 1920 hollow blocks per hour, 15360 per 8 hour shift
- 7200 standard bricks per hour at 230 x 110 x 70 mm
- 90 kN vibration force at 2500 to 4000 times per minute
- Omron or Schneider switches with Siemens or ABB motors
- 960 x 870 mm pallet carrying eight blocks per cycle
At A Glance
- Model
- QT8-15
- Type
- Full Automatic Block Machine
- Family
- Automatic Concrete Block Machine
- Built in
- Linyi, Shandong, China
- Warranty
- 12 months from shipment on frame, vibration system, drive motors and PLC
Customisation
- Moulds designed from your block drawing and local wall standard
- Motor voltage and control cabinet built to your grid supply
- Free plant layout, machine foundation and batching plant drawings
- Free moulding test with your own aggregate before the order is confirmed
Who It Is For
- Plants whose order book already exceeds 12000 blocks a shift
- Producers supplying both walling and paving in volume
- Buyers who want branded electrical components for uptime rather than list price
Problems It Solves
- Peak season orders that cannot be met from existing capacity
- Downtime caused by unbranded electrical components on a continuous line
- Handling cost that rises with every extra block if the line is not automatic
Application Scenarios
- A large block plant supplying multiple contractors daily
- Continuous two-shift production of standard bricks as a clay brick replacement
- Interlocking paver production at 5040 pieces per hour
- Plants that need spare capacity for seasonal demand peaks
Technical Features
- 40.5 kW on a 9400 x 2660 x 2880 mm machine
- 90 kN vibration force at 2500 to 4000 times per minute
- 15 to 20 second moulding cycle
- 960 x 870 mm pallet size
- Hydraulic pressure moulding with wire cut and carburised moulds
Technical Parameters
Reproduced from the manufacturer specification. Where a figure is not published the table says so rather than carrying an estimate.
| Machine overall size | 9400 x 2660 x 2880 mm |
| Power | 40.5 KW |
| Vibration force | 90 KN |
| Moulding cycle | 15-20 s |
| Vibration frequency | 2500-4000 times/min |
| Pallet size | 960 x 870 mm |
| Control switches | Omron or Schneider |
| Main motor | Siemens or ABB |
Quality Control In The Workshop
- One-piece cast vibration box with large imported bearings
- Laser cut steel plate and robot welded stress points
- Shot blasted frame under automotive grade paint
- 12 month warranty on main frame, vibration system, drive motors and PLC
Use Guide
- Size the batching plant to keep a 15 to 20 second cycle fed without waiting
- Plan pallet stock around eight blocks per cycle and the curing time of your mix
- Keep spare vibration box bearings and hydraulic valves on site for a continuous line
- Log cycle times daily: a creeping cycle is the first sign of a hydraulic problem
Published Output By Block Size
Capacity is indicative. Actual output varies with operator efficiency, mould and material quality, which is how the manufacturer specification states it.
| Block size (mm) | Pcs per mould | Pcs per hour | Pcs per 8 hours |
|---|---|---|---|
| 400 x 200 x 200 | 8 | 1920 | 15360 |
| 230 x 110 x 70 | 30 | 7200 | 57600 |
| 200 x 100 x 60 | 28 | 5040 | 40320 |
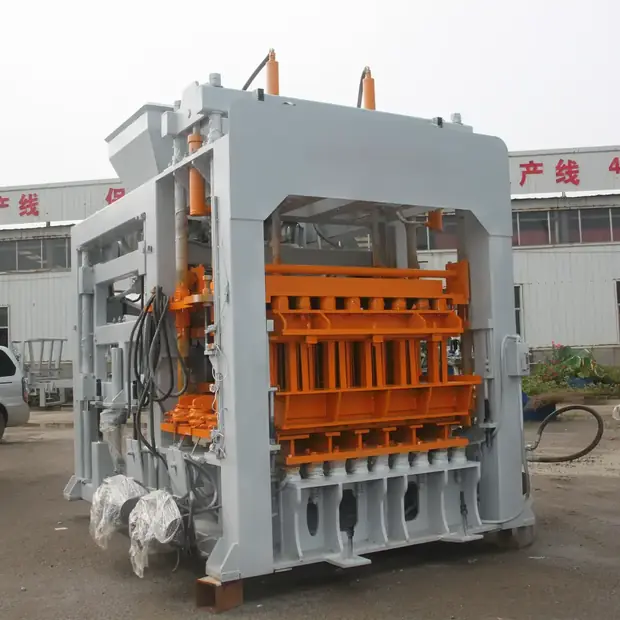
What The Machine Looks Like
How It Compares With The Alternatives
A technical comparison against the other ways of solving the same problem, using the figures each machine publishes for itself.
| QT6-15 automatic machine | Six blocks per cycle at 50-70 kN. The QT8-15 adds two blocks per cycle and lifts vibration force to 90 kN on a longer 9.4 m machine. |
| QT10-15 production line | Ten blocks per cycle with Yuken hydraulics and a 1100 x 900 mm pallet, up to 5200 vibrations per minute. |
| Running a second QT6-15 | One QT8-15 reaches 15360 blocks a shift on a single crew, where a second QT6-15 would duplicate mixing, handling and supervision. |
QT8-15 Automatic Hollow Block Making Machine Questions
What is the shift output of the QT8-15?
What vibration force does it apply?
Which components are branded?
How long is the machine?
Are spare parts held in stock?
Machines Usually Considered Alongside This One
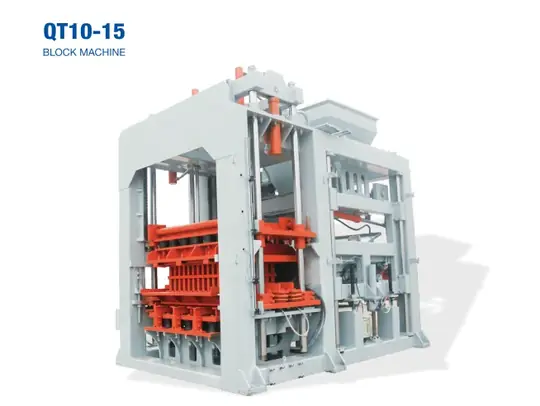
QT10-15 Full Automatic Concrete Block Production Line
Large production line with Siemens, Omron and Yuken components, 90 kN vibration and a published output table across seven block types.
3600-4800 pcs/hour at 400 x 100 x 200 hollow block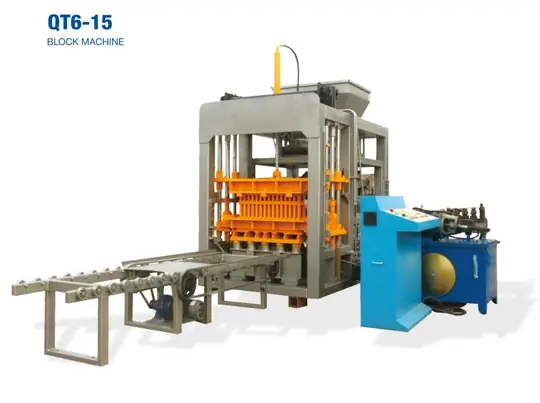
QT6-15 Medium Large Scale Cement Brick Machine
Hydraulic automatic press moulding six hollow blocks per cycle at 40.5 kW, for plants moving into medium large scale output.
1440 pcs/hour at 400 x 200 x 200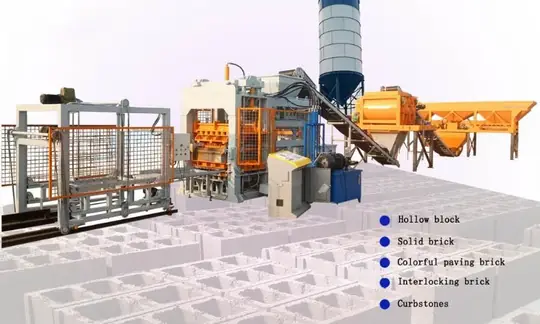
QT12-15 Full Automatic Concrete Block Production Line
Largest line in the range: twelve blocks per cycle, 102 kN vibration and 96000 standard bricks per 8 hour shift.
2880 pcs/hour at 400 x 200 x 200Request A Quotation For The QT8-15
Send your block sizes, target output per shift, local voltage and workshop dimensions. A configuration list, layout drawing and quotation come back.