
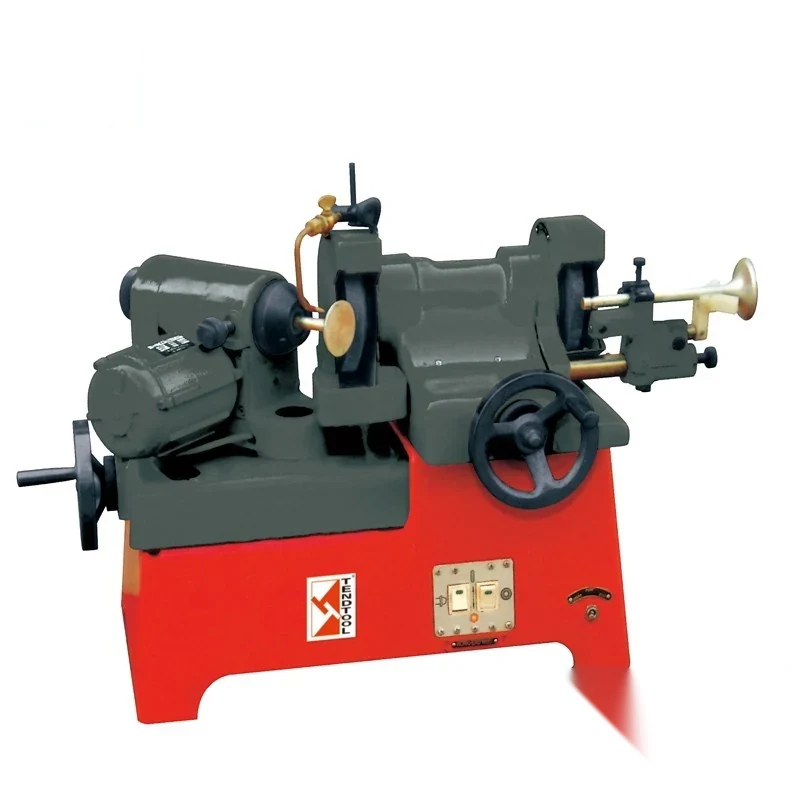
Valve Grinder VR90
The VR90 is the valve refacing machine for an ordinary automobile repair factory or agricultural machinery repair centre, rather than for a specialist head shop. It grinds valve faces up to a maximum diameter of 90 mm on valve stems from 6 to 16 mm, at grinding angles from 15 to 60 degrees, with a maximum grinding dept...
What This Machine Does
The VR90 is the valve refacing machine for an ordinary automobile repair factory or agricultural machinery repair centre, rather than for a specialist head shop. It grinds valve faces up to a maximum diameter of 90 mm on valve stems from 6 to 16 mm, at grinding angles from 15 to 60 degrees, with a maximum grinding depth of 0.025 mm per setting. The work head has 115 mm of cross travel and 95 mm of longitudinal travel, which is enough to sweep a full valve face without repositioning the valve. Wheel speed is 4500 r/min from a 370 W grinding head motor. The whole machine is 680 x 600 x 600 mm and weighs 120 kg, so it fits on a bench area in a working repair shop rather than needing a machine bay. Construction is deliberately simple and the machine is easy to operate, which is what makes it practical as standard equipment for automobile repair service.
Why Buyers Choose This Machine
- Compact at 680 x 600 x 600 mm and 120 kg so it fits into a working repair shop without a dedicated machine bay
- Grinding angles from 15 to 60 degrees cover the seat angles found in car and agricultural engines
- Valve stem range 6 to 16 mm and maximum grinding diameter 90 mm covers most repair-shop valve work
- Maximum grinding depth of 0.025 mm keeps stock removal fine so valve margin is preserved
- 4500 r/min wheel speed from a 370 W grinding head motor gives a clean cut on valve faces
- 115 mm cross travel and 95 mm longitudinal travel sweep the full face in one setup
- Simple construction and easy operation so an ordinary repair technician can run it
Where Valve Grinder VR90 Earns Its Place
Problems It Solves
- A worn valve face will not seat and the engine loses compression after overhaul
- Specialist valve refacers are too large and too costly for a general repair shop
- Sending valves out for refacing holds up an engine that is already in pieces
- Coarse grinding takes too much off the valve and destroys the margin
- Shops without a valve machine end up replacing valves that could be refaced
Who It Is For
- Automobile repair factories doing their own engine overhauls
- Agricultural machinery repair centres
- General repair workshops adding valve refacing as an in-house service
- Distributors supplying small and medium repair shops in export markets
Application Scenarios
- Refacing valves during routine engine overhaul in a car repair factory
- Valve work on tractor and agricultural machinery engines
- Grinding valves with larger seat angles up to 60 degrees
- Occasional valve refacing in a general repair shop that cannot justify a specialist machine
- Light valve reconditioning alongside other engine service work
Technical Detail
Technical Features
- Maximum grinding diameter 90 mm
- Valve axle diameter 6 to 16 mm
- Grinding angle 15 to 60 degrees
- Cross travel of work head 115 mm
- Longitudinal travel of work head 95 mm
- Maximum grinding depth 0.025 mm
- Wheel speed 4500 r/min
- Grinding head motor 370 W
- Compact light construction for easy installation
Specifications
| Machine type | Valve grinding machine |
|---|---|
| Models | VR90 |
| Max grinding diameter | 90 mm |
| Valve axle diameter | 6 to 16 mm |
| Grinding angle | 15 to 60 degrees |
| Cross travel of work head | 115 mm |
| Longitudinal travel of work head | 95 mm |
| Max grinding depth | 0.025 mm |
| Wheel speed | 4500 r/min |
| Grinding head motor | 370 W |
| Overall dimensions | 680 x 600 x 600 mm |
| Weight | 120 kg |
| Shipping port | Shanghai |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Valve face grinding
- Valve refacing
Quality Control
- Ground valve face run-out measured against the stem on a test valve
- Grinding angle setting verified across the 15 to 60 degree range
- Wheel speed checked against the 4500 r/min figure
- Work head travel checked over the full 115 mm cross and 95 mm longitudinal movement
- Machine run in and a sample valve refaced before packing
Customisation Options
- Grinding wheel grade selected for the valve materials you work on
- Workholding specified for your valve stem range within 6 to 16 mm
- Supply voltage and frequency set for your market
- Spare wheels included in the shipment where you run higher volumes
- Manual prepared in your working language
How It Compares With the Alternatives
| Valve grinding machine TVG90 | The TVG90 gives a wider valve length and angle range with a built-in wheel dresser; the VR90 is the compact lower-cost machine for a general repair shop |
|---|---|
| Valve grinder TVR100 | The TVR100 adds a 6-ball chuck and a rocker arm attachment; the VR90 stays simple at 120 kg and 680 x 600 x 600 mm for shops with limited space |
| Replacing worn valves | Refacing at up to 0.025 mm grinding depth recovers valves that are otherwise serviceable rather than buying a full set |
Running the Machine
Step 1
Check the valve stem within the 6 to 16 mm range for wear or bend
Step 2
Load the valve in the work head and set the grinding angle between 15 and 60 degrees
Step 3
Bring the wheel up to the face using the cross and longitudinal travels
Step 4
Take a light pass keeping within the 0.025 mm maximum grinding depth
Step 5
Sweep the full face with the 115 mm cross travel until it cleans up
Step 6
Check the valve margin before returning it to the head
Step 7
Dress or change the wheel when the cut stops working cleanly
Other Machines in Engine Rebuilding Machine
Hydraulic Valve Guide Press Machine TGP1200
View Machine →
Cylinder Head Pressure Tester TPT1600/TPT1600L/TPT1700
View Machine →
Universal Workstation TWS1100/TWB500
View Machine →
Vacuum Tester ZJ45
View Machine →Related Applications and Guides
Engine Rebuilding Workshops
Engine rebuilding workshops recondition blocks heads crankshafts and valves to a geometry the engine will hold for a full service life. XAIMC supplies
Automotive Service and Fleet Workshops
Service centres and fleet depots keep vehicles moving. XAIMC supplies the lifting tyre wheel and fluid handling equipment those workshops use, includi
Cylinder Boring vs Honing - What Each Operation Does
Boring removes metal to bring a worn cylinder back to a round straight bore at a new oversize, while honing produces the final diameter, geometry and
How to Choose a Valve Seat Cutting Machine
A valve seat cutting machine machines the seat angles and the valve guide bore in a cylinder head so that the valve seals concentrically against the s
Questions About Valve Grinder VR90
What valves will the VR90 handle?
Valve axle diameters of 6 to 16 mm and a maximum grinding diameter of 90 mm. Send us your valve sizes and we will confirm they are covered.
What grinding angles can I set?
15 to 60 degrees, which covers the seat angles in car and agricultural machinery engines.
How much space does the machine need?
Overall dimensions are 680 x 600 x 600 mm and the machine weighs 120 kg, so it sits comfortably in a working repair shop.
What power supply does it need?
The grinding head motor is 370 W. We set the supply voltage and frequency for your market, so confirm your supply with the order.
How much can it take off in a pass?
Maximum grinding depth is 0.025 mm, which keeps the cut fine enough to protect the valve margin.
How is the machine packed and shipped?
Crated for sea freight and shipped from Shanghai. Send us your destination port for an FOB CFR or CIF price.
What are your payment terms?
30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
Request a Quote on the Valve Grinder VR90
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.