
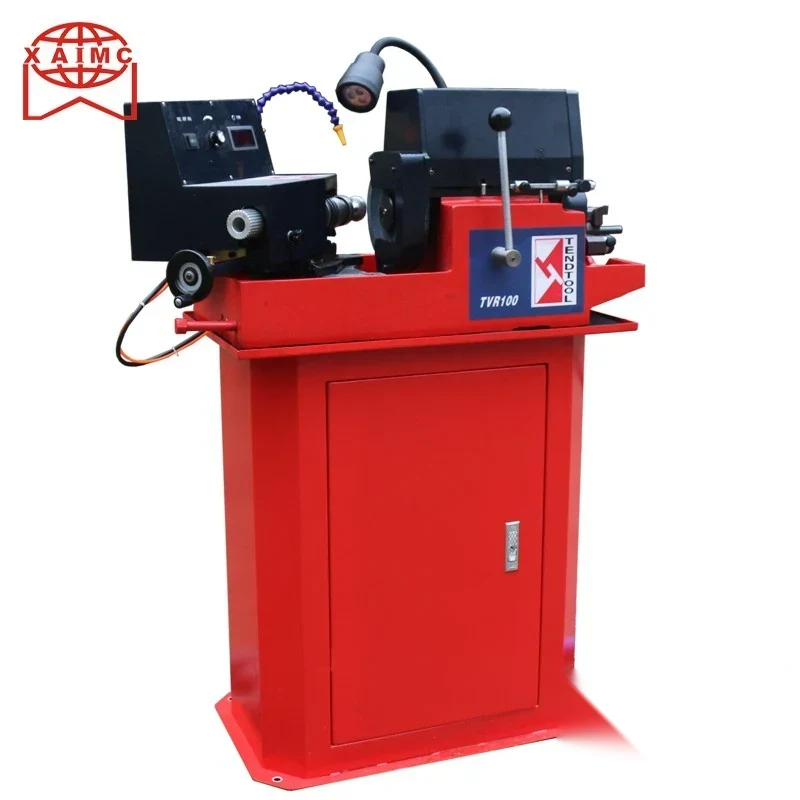
Valve Grinder TVR100
The TVR100 refaces engine valves and, with the attachment included as standard, grinds rocker arms as well. Its chuck is a precision 6-ball design that centres the valve stem as it closes, so valves are loaded and centred quickly and there are no collets to change between sizes. Standard chuck capacity runs from 4mm to...
What This Machine Does
The TVR100 refaces engine valves and, with the attachment included as standard, grinds rocker arms as well. Its chuck is a precision 6-ball design that centres the valve stem as it closes, so valves are loaded and centred quickly and there are no collets to change between sizes. Standard chuck capacity runs from 4mm to 14.3mm, which covers the stem sizes found across most car and light commercial engines. Chuck speed is variable, which matters because valves today are made in a range of materials and each wants a different surface speed if the face is to grind cleanly rather than burn or load the wheel. For a rebuild shop the machine removes two separate jobs from the bench at once: valve faces get a true seating surface, and rocker arm pads get ground on the same machine instead of being replaced or left worn.
Why Buyers Choose This Machine
- Precision 6-ball chuck centres the valve stem as it closes with no collets to change between sizes
- Standard chuck capacity 4mm to 14.3mm covers the usual car and light commercial valve stems
- Variable chuck speed lets the operator match speed to the valve material being ground
- Rocker arm grinding attachment is included so rocker pads are reconditioned on the same machine
- Fast loading means a full set of valves can be refaced without stopping to swap workholding
- Keeps valve and rocker work in the shop rather than replacing parts or sending them out
Where Valve Grinder TVR100 Earns Its Place
Problems It Solves
- A worn valve face will not seal against a freshly cut seat and the head leaks after rebuild
- Changing collets for every valve stem size wastes time on a multi-valve head
- A fixed grinding speed burns or loads the wheel on valves in harder materials
- Worn rocker pads are often replaced when they could be ground back
- Poorly centred valves grind an eccentric face that never seats properly
Who It Is For
- Cylinder head reconditioning shops
- Engine rebuilders doing full head overhauls in-house
- Automotive and light commercial repair workshops
- Distributors equipping head shops in export markets
Application Scenarios
- Refacing a full set of inlet and exhaust valves during a cylinder head overhaul
- Grinding rocker arm pads that have worn a hollow against the valve tip
- Valve work on mixed engine types where stem sizes change between jobs
- Grinding valves in harder modern materials where surface speed has to be reduced
- Batch valve refacing in a head reconditioning line
Technical Detail
Technical Features
- Precision 6-ball chuck for fast accurate valve centring
- No collets required for standard stem sizes
- Standard chuck capacity 4mm to 14.3mm
- Variable speed chuck drive
- Rocker arm grinding attachment included as standard
- High-performance chuck available alongside the standard chuck
- Bench-mounted horizontal valve refacing layout
Specifications
| Machine type | Valve refacing and rocker arm grinding machine |
|---|---|
| Models | TVR100 |
| Chuck type | Precision 6-ball chuck |
| Standard chuck capacity | 4mm to 14.3mm |
| Minimum chuck capacity | Standard .1575 in (4mm) |
| Chuck speed | Variable |
| Included attachment | Rocker arm grinding attachment |
| Chuck options | Standard chuck and high-performance chuck |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Valve face grinding
- Rocker arm grinding
- Stem end grinding
Quality Control
- Chuck centring checked on test valves across the 4mm to 14.3mm range
- Ground valve face run-out measured against the stem axis
- Variable speed drive tested through its full range under load
- Rocker arm attachment fitted and function checked before shipment
- Machine run in and a sample valve refaced before packing
Customisation Options
- Standard or high-performance chuck specified according to the accuracy your work needs
- Grinding wheel grade selected for the valve materials you handle
- Supply voltage and frequency set for your market
- Additional rocker arm tooling quoted where rocker work is a large part of your volume
- Manual prepared in your working language
How It Compares With the Alternatives
| Valve grinding machine TVG90 | The TVG90 is a horizontal refacer built around a wider valve head and angle range; the TVR100 leads on chuck handling with its 6-ball chuck and includes rocker arm grinding |
|---|---|
| Valve grinder VR90 | The VR90 is the compact machine for general repair shops; the TVR100 adds the collet-free 6-ball chuck and variable speed for mixed valve materials |
| Lapping valves by hand | Lapping blends a face into a seat but cannot restore a worn or pitted valve face angle; the TVR100 grinds a new face |
Running the Machine
Step 1
Clean the valve stem and check it for bend or wear before loading
Step 2
Load the stem in the 6-ball chuck within the 4mm to 14.3mm capacity
Step 3
Set the chuck speed to suit the valve material
Step 4
Dress the wheel and set the grinding angle for the valve face
Step 5
Take light passes until the face cleans up fully across its width
Step 6
Fit the rocker arm attachment when grinding rocker pads
Step 7
Check the margin thickness before returning a refaced valve to the head
Other Machines in Engine Rebuilding Machine
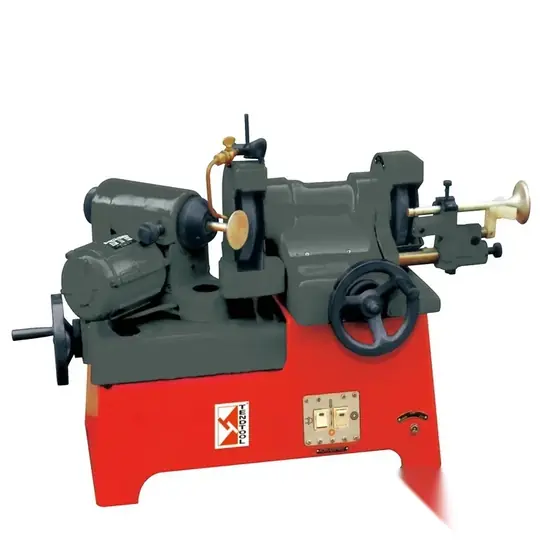
Valve Grinder VR90
View Machine →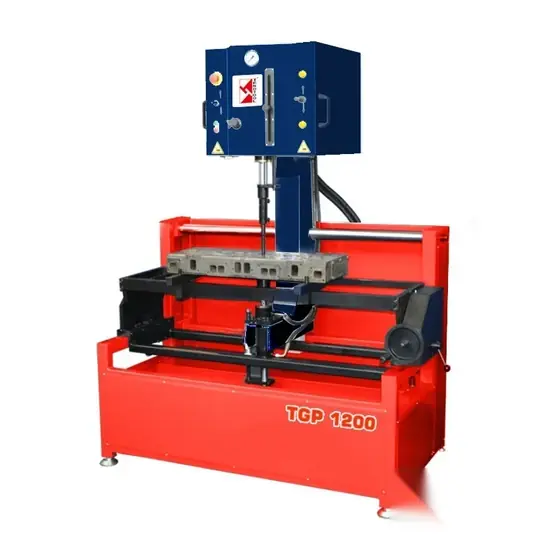
Hydraulic Valve Guide Press Machine TGP1200
View Machine →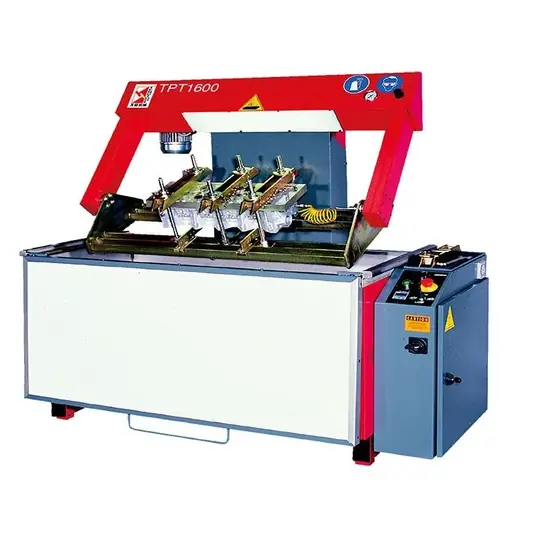
Cylinder Head Pressure Tester TPT1600/TPT1600L/TPT1700
View Machine →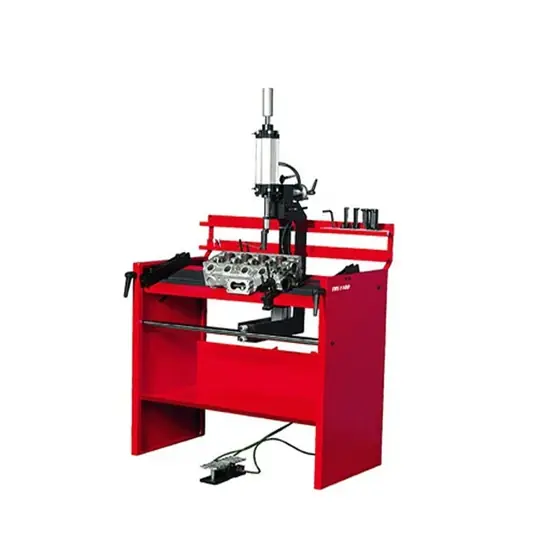
Universal Workstation TWS1100/TWB500
View Machine →Related Applications and Guides
Engine Rebuilding Workshops
Engine rebuilding workshops recondition blocks heads crankshafts and valves to a geometry the engine will hold for a full service life. XAIMC supplies
Automotive Service and Fleet Workshops
Service centres and fleet depots keep vehicles moving. XAIMC supplies the lifting tyre wheel and fluid handling equipment those workshops use, includi
Cylinder Boring vs Honing - What Each Operation Does
Boring removes metal to bring a worn cylinder back to a round straight bore at a new oversize, while honing produces the final diameter, geometry and
How to Choose a Valve Seat Cutting Machine
A valve seat cutting machine machines the seat angles and the valve guide bore in a cylinder head so that the valve seals concentrically against the s
Questions About Valve Grinder TVR100
What valve stem sizes does the standard chuck take?
4mm to 14.3mm. Tell us the stem sizes you work on and we will confirm the standard chuck covers them.
Do I need to change collets between valve sizes?
No. The precision 6-ball chuck centres the valve directly, so there are no collets to change.
Can it grind rocker arms?
Yes. A rocker arm grinding attachment is included as standard equipment.
Why does the machine need variable speed?
Valves today are made in a variety of materials, and the chuck speed has to be matched to the material for the face to grind cleanly instead of burning or loading the wheel.
What is the high-performance chuck for?
It is the higher-accuracy chuck option offered alongside the standard chuck. Tell us the accuracy your work requires and we will quote the right one.
What are your trade and payment terms?
FOB CFR and CIF. Payment is 30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
What spares should I order with the machine?
Grinding wheels are the main consumable. Send us your monthly valve volume and we will suggest a starting wheel package.
Request a Quote on the Valve Grinder TVR100
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.