
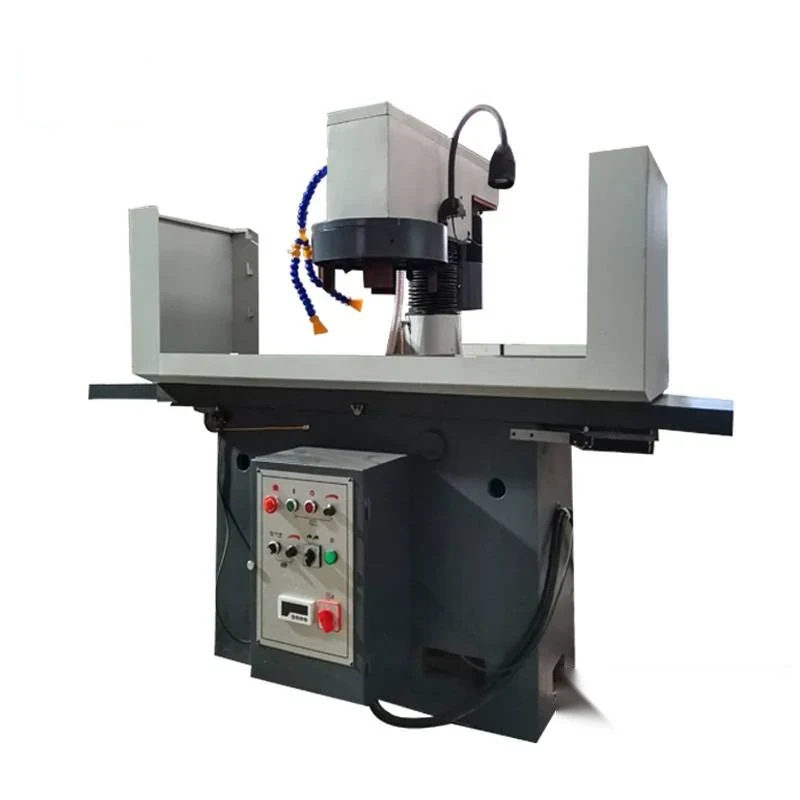
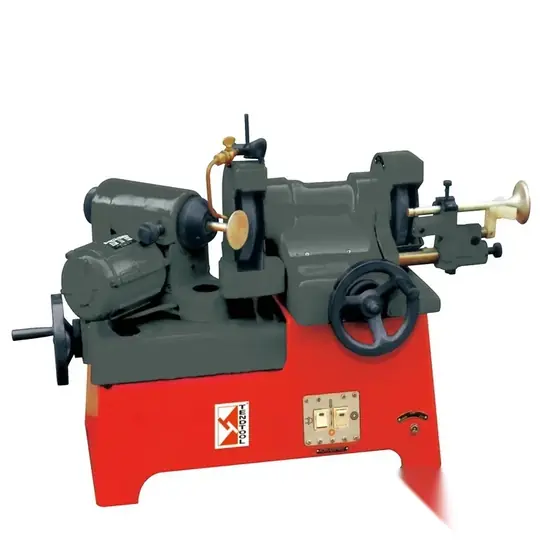
TSM850 Cylinder Head Disc Grinding and Milling Machine
The TSM850 resurfaces the joint face of an engine block or cylinder head, either by grinding or by milling on the same vertical machine. A head that has been cooked or a block that has been in service a long time no longer presents a flat sealing face, and no gasket will hold on it until the face is brought back true. ...
What This Machine Does
The TSM850 resurfaces the joint face of an engine block or cylinder head, either by grinding or by milling on the same vertical machine. A head that has been cooked or a block that has been in service a long time no longer presents a flat sealing face, and no gasket will hold on it until the face is brought back true. The table on the TSM850 is driven by a gear motor and ball screw with stepless frequency speed control, so feed can be dialled to suit a light grinding pass or a heavier milling cut without changing gears. With the right fixture the machine also takes multi-angle work on heads, and with general-purpose fixturing it will face other flat parts. Castings are made by resin sand casting, which keeps distortion low and gives the machine a stable base to hold accuracy in a working shop. Table travel is 1115 mm on the TSM850.
Why Buyers Choose This Machine
- Grinding and milling on one vertical machine so light cleanup and heavy stock removal are both covered
- Gear motor and ball screw table drive with stepless frequency control makes feed adjustment simple and stable
- Multi-angle grinding of cylinder heads is possible with the matching special fixtures
- Resin sand cast structure keeps distortion low so accuracy holds in service
- 1115 mm table travel handles long cylinder heads as well as blocks
- Extra fixtures turn the machine into a general flat surfacing machine for other parts
- Brings warped block and head faces back to a sealing surface instead of replacing the part
Where TSM850 Cylinder Head Disc Grinding and Milling M Earns Its Place
Problems It Solves
- A warped head or block face will not seal and the gasket fails again soon after assembly
- Shops with only a milling option cannot get the fine finish a modern gasket needs
- Fixed-speed table feeds force a compromise between cut rate and finish
- Multi-angle head faces are difficult to set up on a machine without dedicated fixtures
- Sending head surfacing out adds days to every engine job
Who It Is For
- Engine rebuilding workshops doing routine head and block resurfacing
- Truck bus and agricultural machinery service shops
- Machine shops offering head and block surfacing to local garages
- Distributors equipping engine rebuild workshops in export markets
Application Scenarios
- Resurfacing a cylinder head face after a blown head gasket
- Facing an engine block deck before a rebuild
- Multi-angle grinding on cylinder heads using special fixtures
- Batch resurfacing work taken in as a subcontract service
- Flat surfacing of other machined parts with suitable fixturing
Technical Detail
Technical Features
- Vertical grinding and milling machine layout
- Table movement driven by gear motor and ball screw
- Stepless frequency speed control on the table feed
- Special fixtures for multi-angle grinding of cylinder heads
- Resin sand cast structural parts with low distortion
- Table travel 1115 mm
- Grinding and milling heads interchangeable for the same work
Specifications
| Machine type | Vertical cylinder head and block disc grinding and milling machine |
|---|---|
| Models | TSM850 |
| Table travel | 1115 mm |
| Table drive | Gear motor and ball screw |
| Feed control | Stepless frequency speed control |
| Casting | Resin sand casting |
| Operations | Grinding and milling of block and cylinder head joint faces |
| Tooling | Special fixtures for multi-angle cylinder head grinding |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Surface grinding
- Milling
- Face resurfacing
Quality Control
- Table travel checked over the full 1115 mm for straightness and smooth feed
- Flatness of a test workpiece measured after a finishing pass
- Spindle run-out verified before the grinding disc is fitted
- Stepless feed control tested across its range under load
- Machine run in and a sample face ground before packing
Customisation Options
- Special fixtures quoted for the head and block types you actually run
- Grinding disc or milling cutter package specified for your workload
- Supply voltage and frequency set for your market
- Multi-angle fixturing added where you do angled head faces
- Manual and control labelling prepared in your working language
How It Compares With the Alternatives
| Cylinder block grinding-milling machine 3M9735B | The 3M9735B is built around larger block work; the TSM850 with its 1115 mm table travel is aimed at head and block faces in a general rebuild shop |
|---|---|
| Milling only on a general workshop mill | A mill can take the stock off but the TSM850 grinds as well, which is what gives the face the finish a modern gasket needs |
| Hand lapping a head face | Hand lapping follows the existing warp; the TSM850 cuts a new flat reference face across the whole surface |
Running the Machine
Step 1
Clean and inspect the face and note where the warp sits
Step 2
Clamp the head or block on the table with the correct fixture
Step 3
Choose grinding for a finish pass or milling where more stock has to come off
Step 4
Set the table feed on the stepless frequency control to suit the cut
Step 5
Take a light first pass and check that the cut is picking up across the whole face
Step 6
Work down until the face cleans up completely then measure flatness
Step 7
Clean the part so no abrasive or swarf is carried into assembly
Other Machines in Engine Rebuilding Machine
Related Applications and Guides
Engine Rebuilding Workshops
Engine rebuilding workshops recondition blocks heads crankshafts and valves to a geometry the engine will hold for a full service life. XAIMC supplies
Automotive Service and Fleet Workshops
Service centres and fleet depots keep vehicles moving. XAIMC supplies the lifting tyre wheel and fluid handling equipment those workshops use, includi
Cylinder Boring vs Honing - What Each Operation Does
Boring removes metal to bring a worn cylinder back to a round straight bore at a new oversize, while honing produces the final diameter, geometry and
How to Choose a Valve Seat Cutting Machine
A valve seat cutting machine machines the seat angles and the valve guide bore in a cylinder head so that the valve seals concentrically against the s
Questions About TSM850 Cylinder Head Disc Grinding and Milli
Can the TSM850 both grind and mill?
Yes. It is a vertical grinding and milling machine used to grind or mill the connecting plane of the engine block and cylinder head.
What is the table travel?
1115 mm, which covers cylinder heads and block decks within that length. Send us the longest part you resurface and we will confirm it fits.
Can it do multi-angle cylinder head faces?
Yes, with the corresponding special fixtures. Tell us the head types and angles you work on so we can quote the right fixture set.
Can it be used on parts other than engines?
Yes. With corresponding fixtures it can be used for plane processing of other parts.
Why does the resin sand casting matter?
The castings are made by resin sand casting, which gives small deformation and a stable structure, so the machine holds its accuracy over time in a working shop.
What are your payment and trade terms?
FOB CFR and CIF. Payment is 30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
What consumables will I need?
Grinding discs and milling inserts are the running consumables. Tell us your monthly volume and the material mix and we will propose a starting package.
Request a Quote on the TSM850 Cylinder Head Disc Grinding and Milli
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.