
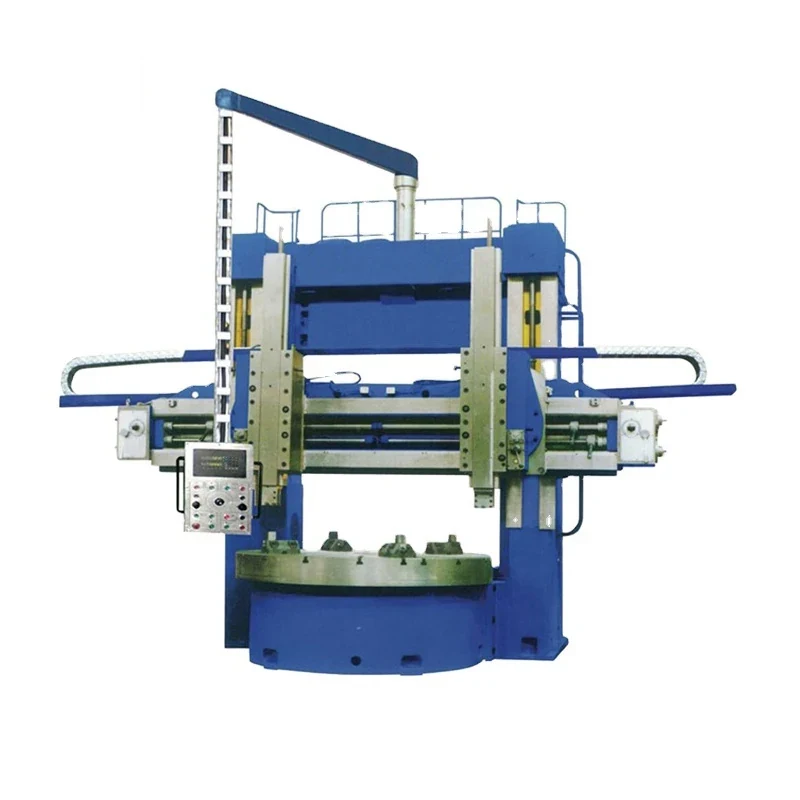
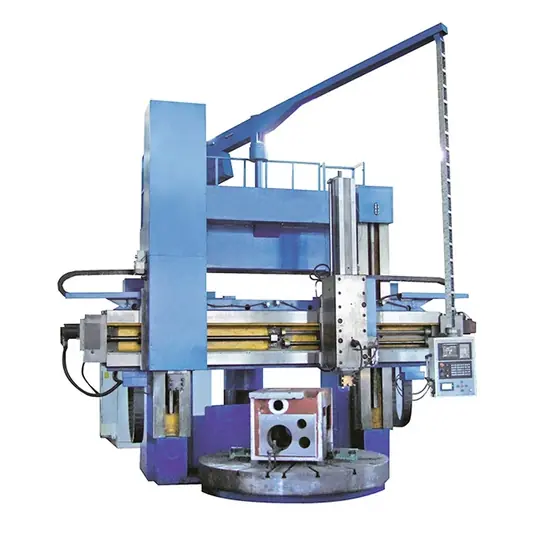
Manual Vertical Turret Lathe C5225
The C5225 is the smallest frame in a range of double column vertical lathes that continues through the C5240, C5250, C5263 and C5280. It cuts a workpiece up to 2500mm in diameter on a 2250mm table, takes a part up to 1600mm or 2000mm high and up to 10 or 15 tonnes in weight, with table speeds from 2 to 63 r/min and a m...
What This Machine Does
The C5225 is the smallest frame in a range of double column vertical lathes that continues through the C5240, C5250, C5263 and C5280. It cuts a workpiece up to 2500mm in diameter on a 2250mm table, takes a part up to 1600mm or 2000mm high and up to 10 or 15 tonnes in weight, with table speeds from 2 to 63 r/min and a maximum table torque of 63 kn.m. The larger frames scale from there to 8000mm cutting diameter and 150 tonnes. It works with high speed steel and hard alloy cutting tools on cylinders, cone surfaces, end faces and grooves in ferrous metals, non-ferrous metals and some non-metallic parts. In roughing, the machine is intended to remove not less than 4mm in a single pass on castings, steel castings and materials such as No.45 steel, which is the figure to plan your roughing allowance around.
Why Buyers Choose This Machine
- 2500mm maximum cutting diameter on a 2250mm table takes parts no horizontal lathe of normal size can hold
- Workpiece weight capacity of 10 or 15 tonnes with a maximum table torque of 63 kn.m
- Workpiece height of 1600mm or 2000mm covers tall housings and cases as well as flat discs
- Roughing removal of not less than 4mm per pass on castings and steel so heavy stock comes off fast
- Table speed range of 2 to 63 r/min covers large slow diameters and smaller faster work
- Double column structure resists the cutting forces that deflect a single column at this size
- Frames up to C5280 at 8000mm diameter so one supplier covers the whole size range
Where Manual Vertical Turret Lathe C5225 Earns Its Place
Problems It Solves
- Parts of 2500mm diameter and many tonnes cannot be chucked safely on a horizontal lathe
- Single column machines deflect under the cutting forces that large diameter roughing produces
- Planning roughing allowance without a known minimum depth of cut wastes passes and time
- Tall housings will not fit under the tooling of machines built only for flat discs
- Sending large castings out for first machining blocks the whole production schedule
- Ordering one frame size for a growing product range means refusing larger parts later
Who It Is For
- Foundries and heavy casting machine shops
- Pressure vessel ring and flange manufacturers
- Wind energy mining and cement equipment builders
- Heavy plant maintenance departments repairing large rotating parts
- Subcontractors taking in large diameter vertical turning
Application Scenarios
- Turning cylinders and cone surfaces on large castings and steel castings
- Facing and grooving heavy flanges rings and housings
- Roughing cast parts with a 4mm or greater depth of cut per pass
- Machining No.45 steel and similar materials with hard alloy tooling
- Tall workpiece machining up to 1600mm or 2000mm high
- Heavy component work up to 10 or 15 tonnes on the C5225 frame
Technical Detail
Technical Features
- Double column vertical lathe structure
- Maximum workpiece cutting diameter 2500mm
- Workbench diameter 2250mm
- Maximum workpiece height 1600mm or 2000mm
- Maximum workpiece weight 10t or 15t
- Workbench speed range 2-63 r/min
- Maximum worktable torque 63 kn.m
- High speed steel and hard alloy cutting tools
- Roughing removal of not less than 4mm per pass on castings steel castings and No.45 steel
Specifications
| Machine type | Manual double column vertical turret lathe |
|---|---|
| Models | C5225 C5240 C5250 C5263 C5280 |
| Max cutting diameter of workpiece | 2500mm (C5225) |
| Workbench diameter | 2250mm (C5225) |
| Max height of workpiece | 1600mm or 2000mm (C5225) |
| Max weight of workpiece | 10t or 15t (C5225) |
| Workbench speed range | 2-63 r/min (C5225) |
| Max torque of worktable | 63 kn.m (C5225) |
| Series range | Up to 8000mm cutting diameter and 150t on C5280 |
| Tooling | High speed steel and hard alloy cutting tools |
| Minimum roughing pass | Not less than 4mm on castings steel castings and No.45 steel |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Turning
- Facing
- Taper turning
- Grooving
- Parting
Materials Handled
- Cast iron
- Steel castings
- No.45 steel
- Non-ferrous metals
- Some non-metallic materials
Quality Control
- Table running accuracy checked at speeds across the 2-63 r/min range
- Worktable torque verified against the 63 kn.m rating under load
- Column and cross rail alignment measured with the tool rest at full travel
- Test roughing cut taken at 4mm depth in cast material
- Machine run and inspected before it is dismantled for shipment
Customisation Options
- Frame chosen from C5225 to C5280 by cutting diameter and part weight
- Workpiece height option of 1600mm or 2000mm specified on the C5225
- Tool rest and tooling package set for your materials
- Supply voltage frequency and phase built for your site
- Foundation and installation drawings prepared for the frame ordered
How It Compares With the Alternatives
| Single Column Vertical Turning Lathe Machine C5112 | The single column range suits medium parts and less floor area; the C5225 double column frame takes 2500mm diameter and workpieces of 10 to 15 tonnes |
|---|---|
| Larger C5240 to C5280 frames | The larger frames go up to 8000mm cutting diameter and 150 tonnes; the C5225 is the right frame when your parts stay within 2500mm and 15 tonnes |
| Horizontal lathe for large diameter work | A heavy ring or casting sits on the vertical table under its own weight instead of being held out in a horizontal chuck |
| Boring mill for face and bore work | On the vertical lathe the part rotates and the tool stays fixed, which gives a turned finish on large circular surfaces a boring mill cannot match |
Running the Machine
Step 1
Check the part diameter height and weight against the frame before loading
Step 2
Clamp the workpiece on the table and check run-out before starting the cut
Step 3
Select a table speed within 2-63 r/min suited to the diameter being cut
Step 4
Plan roughing at not less than 4mm per pass on castings and No.45 steel
Step 5
Use high speed steel or hard alloy tooling according to the material
Step 6
Take face groove and taper cuts in one setting so features stay concentric
Step 7
Keep the table and clamping faces clear of chips and follow the lubrication schedule
Related Applications and Guides
General Machining Job Shops
Job shops take whatever work comes through the door, which means their equipment has to cover a wide range rather than do one thing perfectly. XAIMC s
Heavy Equipment and Plant Maintenance
Mines quarries plantations and processing plants cannot wait for imported spares. XAIMC supplies the boring gear cutting turning and grinding machines
Machine Tool Installation and Commissioning Checklist
Installing an imported machine tool correctly means preparing the site, unpacking and positioning the machine, levelling it, connecting services and p
Preventive Maintenance for Manual Lathes and Milling Machines
Manual lathes and milling machines keep their accuracy through lubrication, cleanliness, correct adjustment of gibs and backlash, and regular geometri
Questions About Manual Vertical Turret Lathe C5225
What is the largest part the C5225 will take?
2500mm maximum cutting diameter on a 2250mm table, up to 1600mm or 2000mm high and 10 or 15 tonnes in weight. Larger frames in the range go up to 8000mm and 150 tonnes.
What depth of cut should I plan for roughing?
Not less than 4mm per pass on castings, steel castings and materials such as No.45 steel. Plan your machining allowance around that.
What table speeds are available?
2 to 63 r/min on the C5225, with a maximum worktable torque of 63 kn.m.
Which frame should I order?
C5225, C5240, C5250, C5263 and C5280 differ in cutting diameter, height, weight and torque. Send us your largest part and we will confirm the frame.
What tooling does it use?
High speed steel and hard alloy cutting tools. Tell us your materials and cut depths and we will advise the tooling package.
What foundation does it need and how is it shipped?
It needs a foundation matched to the frame and part weight; we supply the installation drawing. The machine is shipped for sea freight from Xi'an on FOB CFR or CIF terms.
What are your payment terms?
30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
Request a Quote on the Manual Vertical Turret Lathe C5225
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.