
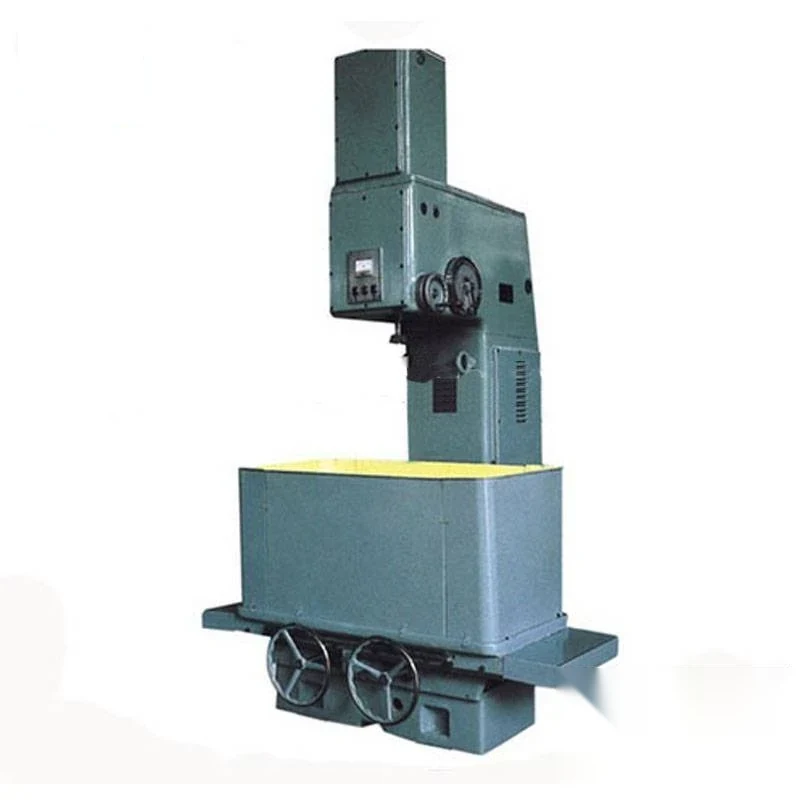
M4215 Hydraulic Vertical Cylinder Honing Machine
The M4215 hones cylinder block bores, cylinder liner bores, hydraulic cylinder bores and other precision bores to a controlled size and finish after boring has left the wall oversize and rough. The honing head reciprocates under hydraulic drive, which gives an even stroke speed through the bore rather than the uneven r...
What This Machine Does
The M4215 hones cylinder block bores, cylinder liner bores, hydraulic cylinder bores and other precision bores to a controlled size and finish after boring has left the wall oversize and rough. The honing head reciprocates under hydraulic drive, which gives an even stroke speed through the bore rather than the uneven rhythm an operator produces by hand, and expansion and contraction of the stones is set directly on the feed handwheel so the operator controls stock removal without leaving the machine. Roundness of 0.0025mm and a surface finish of Ra 0.4 can be obtained on this machine. Where a bore has gone tapered, the taper can be corrected by working a short stroke at the tight end instead of scrapping the block or liner. The structure is deliberately simple, so a shop can put a rebuild technician rather than a specialist on the machine. M4215/1 covers the smaller bore range where the work is liners and hydraulic cylinders rather than engine blocks.
Why Buyers Choose This Machine
- Hydraulically driven reciprocating head keeps stroke speed even through the bore so the crosshatch is consistent top to bottom
- Roundness of 0.0025mm and surface finish of Ra 0.4 are achievable which is what a ring needs to seat and seal
- Bore taper can be corrected with a short stroke instead of writing off a worn block or liner
- Stone expansion is set directly on the feed handwheel so stock removal stays in the operator's hand
- Simple structure means a rebuild technician can run it without specialist honing training
- One machine covers engine block bores cylinder liners and hydraulic cylinder bores
- M4215 and M4215/1 between them cover a wide honing diameter range on the same machine layout
Where M4215 Hydraulic Vertical Cylinder Honing Machine Earns Its Place
Problems It Solves
- A bored cylinder wall is too rough and out of round for rings to seat which causes oil consumption after a rebuild
- Hand honing gives a different crosshatch and a different size on every bore
- Tapered bores are normally treated as scrap when they could be corrected
- Sending honing out to a subcontractor adds days to every engine job
- Shops without a honing machine are limited to whatever oversize pistons they can buy
Who It Is For
- Engine rebuilding workshops that already bore blocks and need a controlled finishing step
- Hydraulic cylinder repair shops reconditioning tubes in-house
- Truck tractor and marine engine service shops handling liners
- Distributors equipping engine rebuild lines in export markets
Application Scenarios
- Finishing cylinder block bores after boring in an engine rebuild shop
- Honing replacement cylinder liners to final size and finish before fitting
- Reconditioning hydraulic cylinder tubes for plant and construction equipment
- Correcting bore taper in worn blocks that would otherwise be scrapped
- Sizing precision bores on general machined components with suitable fixturing
Technical Detail
Technical Features
- Vertical honing layout with hydraulically driven reciprocating head
- Honing head expansion and contraction controlled directly by feed handwheel
- Four-step spindle speed selection
- Short stroke working mode for taper correction
- Roundness capability of 0.0025mm
- Surface finish capability of Ra 0.4
- Simple mechanical structure for straightforward operation and maintenance
Specifications
| Machine type | Hydraulic vertical cylinder honing machine |
|---|---|
| Models | M4215 / M4215/1 |
| Roundness | 0.0025mm |
| Surface finish | Ra 0.4 |
| Head drive | Hydraulic reciprocation |
| Stone feed | Direct feed handwheel control |
| Spindle speeds | Four steps |
| Applications | Cylinder block bores cylinder liner bores hydraulic cylinder bores precision bores |
| Packing | Plywood case |
| Shipping port | Shanghai or Tianjin |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Honing
- Bore finishing
- Taper correction
Quality Control
- Bore roundness checked on a test piece against the 0.0025mm figure before shipment
- Surface finish verified against Ra 0.4 on a honed sample bore
- Hydraulic reciprocation stroke checked for even speed over the full travel
- Spindle speed steps run through and checked under load
- Machine run in and function tested before packing in the plywood case
Customisation Options
- M4215 or M4215/1 chosen according to the smallest bore diameter you hone
- Honing heads and stone sets specified for your bore range and material
- Supply voltage and frequency set for your market
- Fixturing quoted for liners or hydraulic tubes if you are not honing engine blocks
- Operating manual prepared in the language your shop needs
How It Compares With the Alternatives
| Hand-held honing tool in a drill | A hand hone can deglaze a bore but cannot hold roundness or correct taper; the M4215 works to 0.0025mm roundness under a driven stroke |
|---|---|
| Cylinder boring machine | A boring machine takes the bore to size but leaves a cut surface; the M4215 is the finishing step that gives the wall the roundness and Ra 0.4 finish the rings need |
| Subcontracting honing out | In-house honing removes the transport leg from every engine job and keeps the block in your shop until it ships |
Running the Machine
Step 1
Mount and align the block liner or cylinder tube square to the honing spindle
Step 2
Select the honing head and stone grade for the bore diameter and material
Step 3
Set spindle speed on the four-step selector to suit the bore size
Step 4
Expand the stones with the feed handwheel until they contact the wall evenly
Step 5
Run the full stroke for general honing and check size and roundness on the first bore
Step 6
Switch to a short stroke at the tight end where a bore is tapered
Step 7
Flush the bore and inspect the crosshatch before moving to the next cylinder
Other Machines in Engine Rebuilding Machine
Line Boring Machine LB100
View Machine →
Line Boring Machine T8120*20/T8120SF/LB2300
View Machine →
Con-Rod Bushing Boring Machine T8216/T8210D
View Machine →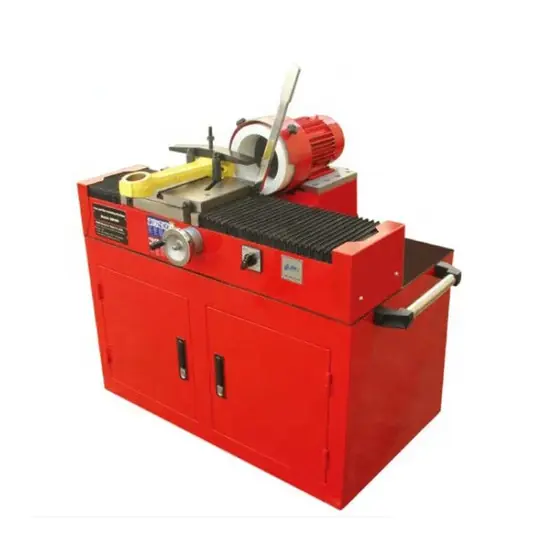
Cap and Rod Grinding Machine DM50/DM100
View Machine →Related Applications and Guides
Engine Rebuilding Workshops
Engine rebuilding workshops recondition blocks heads crankshafts and valves to a geometry the engine will hold for a full service life. XAIMC supplies
Automotive Service and Fleet Workshops
Service centres and fleet depots keep vehicles moving. XAIMC supplies the lifting tyre wheel and fluid handling equipment those workshops use, includi
Cylinder Boring vs Honing - What Each Operation Does
Boring removes metal to bring a worn cylinder back to a round straight bore at a new oversize, while honing produces the final diameter, geometry and
How to Choose a Valve Seat Cutting Machine
A valve seat cutting machine machines the seat angles and the valve guide bore in a cylinder head so that the valve seals concentrically against the s
Questions About M4215 Hydraulic Vertical Cylinder Honing Mac
What is the difference between M4215 and M4215/1?
The honing diameter range. M4215/1 starts at a smaller bore diameter than the standard M4215. Send us the smallest and largest bores you hone and we will confirm which model covers them.
What accuracy can I expect?
Roundness of 0.0025mm and a surface finish of Ra 0.4 can be obtained on this machine when the stones and speed are correctly selected for the material.
Can it correct a tapered bore?
Yes. Bore taper is corrected by working a short stroke concentrated at the tight end of the bore rather than stroking the full length.
Can it hone hydraulic cylinders as well as engine blocks?
Yes. The machine is used for cylinder block bores cylinder liner bores hydraulic cylinder bores and other precision bores. Tell us the tube length and diameter you work on so we can confirm the setup.
How is the machine packed and shipped?
The machine is packed in a plywood case and ships from Shanghai or Tianjin. We quote FOB CFR or CIF against the port you nominate.
What are your payment terms?
30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
What spare parts should I order with the machine?
Honing stones are the consumable item. Tell us your typical bore diameters and monthly volume and we will propose a first stone package with the machine.
Request a Quote on the M4215 Hydraulic Vertical Cylinder Honing Mac
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.