
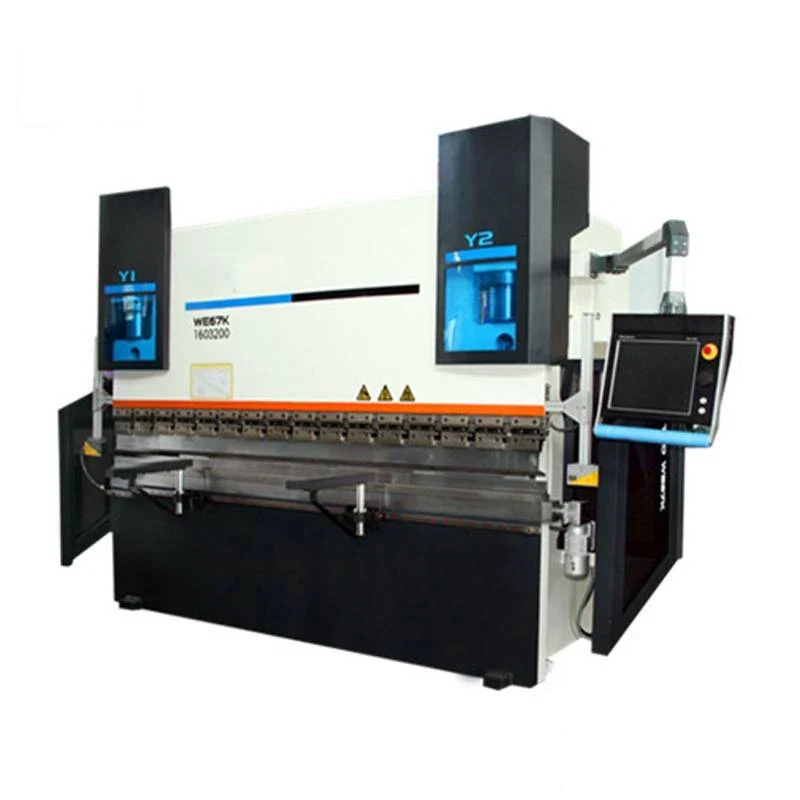
WC67K CNC Hydraulic Press Brake Machine
The WC67K is a CNC hydraulic press brake built on a welded monoblock steel frame in ST44 A1 material, designed to resist the deflection moment that opens up bend angles at the centre of a long part. Control is by E210 or DELEM DA41, giving the operator programmed control of the standard two axes Y and X with a manual R...
What This Machine Does
The WC67K is a CNC hydraulic press brake built on a welded monoblock steel frame in ST44 A1 material, designed to resist the deflection moment that opens up bend angles at the centre of a long part. Control is by E210 or DELEM DA41, giving the operator programmed control of the standard two axes Y and X with a manual R axis, so bend sequences are entered once and recalled rather than set by hand for every part. The hydraulic system is integrated and uses Bosch-Rexroth valves and components from Germany, which keeps the circuit compact and the valve response precise. Positioning accuracy is quoted at 0.01mm. The machine is used on aluminium and other sheet materials in the WC67K range, for example the 80T3200 build with 3200mm bending length. It is supplied with CE marking.
Why Buyers Choose This Machine
- CNC control of the Y and X axes recalls stored bend programs instead of resetting by hand
- E210 or DELEM DA41 control gives failsafe handling of the machine's vital functions
- Monoblock ST44 A1 welded frame resists the deflection moment that opens angles mid-bend
- Bosch-Rexroth valves give precise ram control and predictable service parts
- Positioning accuracy of 0.01mm holds flange widths across a production batch
- Manual R axis lets the operator set backgauge height for formed and returned parts
- Integrated hydraulic control system reduces external pipework and maintenance points
Where WC67K CNC Hydraulic Press Brake Machine Earns Its Place
Problems It Solves
- Resetting the backgauge by hand for every bend in a multi-bend part wastes most of the cycle
- Frames that deflect under load give a different angle at the centre of a long bend
- Flange widths drift across a batch when positions are set by measurement each time
- Backgauge fingers foul on formed parts when there is no height adjustment
- Scattered hydraulic pipework is slow to trace when a leak appears
Who It Is For
- Sheet metal shops running multi-bend parts in repeat batches
- Enclosure cabinet and panel manufacturers
- Fabricators upgrading from an NC brake to programmed bending
- Machinery distributors supplying CNC press brakes into export markets
Application Scenarios
- Multi-bend sheet metal parts where each bend needs a different backgauge position
- Aluminium panel and enclosure bending
- Repeat production batches where flange width must stay within a tight tolerance
- Subcontract shops quoting complex parts that are slow to set on an NC brake
- Long bends on wide sheet such as the 3200mm bending length build
Technical Detail
Technical Features
- Welded monoblock steel frame in ST44 A1 material
- European streamlined machine design rigid to deflection moment
- E210 or DELEM DA41 CNC control
- CNC control of standard 2 axes Y and X with manual R axis
- Integrated hydraulic control system
- Bosch-Rexroth hydraulic valves and components from Germany
- Positioning accuracy 0.01mm
- CE marked
Specifications
| Machine type | CNC hydraulic press brake |
|---|---|
| Models | WC67K series example build WC67K 80T3200 |
| Frame | Welded monoblock steel frame ST44 A1 |
| CNC control | E210 or DELEM DA41 |
| Axes | CNC control of Y and X axes with manual R axis |
| Hydraulic system | Integrated system with Bosch-Rexroth valves Germany |
| Accuracy | 0.01mm positioning accuracy |
| Bending length example | 3200mm on the 80T3200 build |
| Bending materials | Aluminium and other sheet materials |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Sheet metal bending
- Press braking
- CNC forming
Materials Handled
- Aluminium
Quality Control
- Frame welded and checked for rigidity before machining
- Ram parallelism and synchronisation checked across the bending length
- CNC axis positioning verified against the 0.01mm accuracy figure
- Hydraulic circuit pressure tested and checked for leaks
- Control system run through a full bending program before despatch
- CE conformity documentation prepared with the machine
Certifications
- CE
Customisation Options
- Tonnage and bending length specified for your parts such as the 80T3200 build
- E210 or DELEM DA41 control specified on the order
- Punch and die tooling quoted against your material thickness and radii
- Supply voltage phases and frequency built for your market
- Control language and manual prepared for your operators
How It Compares With the Alternatives
| WC67Y hydraulic press brake | The WC67Y is NC controlled with an E21 display; the WC67K adds CNC control of the Y and X axes, so multi-bend parts are programmed once and recalled |
|---|---|
| Manual backgauge setting | Hand setting a backgauge for each bend is the slowest part of a multi-bend job; CNC X axis positioning removes that step between bends |
| FD series electric folding machine | The folder is quicker to set for simple flanges; the WC67K is the machine for thicker material, tighter tolerance and programmed bend sequences |
Running the Machine
Step 1
Fit punch and die for the material thickness and bend radius
Step 2
Enter the part program on the E210 or DELEM DA41 control including bend sequence
Step 3
Set the manual R axis height so the backgauge fingers clear formed features
Step 4
Run a first part and measure the flange widths and angles
Step 5
Correct the program values then run the batch
Step 6
Keep the hydraulic oil clean and check filter condition on a routine schedule
Step 7
Back up the machine programs so a control replacement does not lose your part data
Other Machines in Press Brakes
Related Applications and Guides
Sheet Metal Fabrication
Sheet metal shops cut, bend, roll and form. XAIMC supplies shears press brakes plate rolls tube benders and fibre laser cutting across the manual to C
Press Brake and Guillotine Shear Basics for Sheet Metal Shops
A guillotine shear cuts sheet to size and a press brake folds that sheet into the finished part, and the two machines together form the core of almost
Questions About WC67K CNC Hydraulic Press Brake Machine
Which control will my machine have?
The WC67K is offered with E210 or DELEM DA41. Tell us which your operators already use, because it affects programming and the spares you hold.
How many axes are controlled?
Standard is CNC control of two axes, Y and X, with a manual R axis for backgauge height.
What positioning accuracy can I expect?
Positioning accuracy is quoted at 0.01mm. Achieved part tolerance also depends on tooling condition and material consistency.
Does the machine carry CE marking?
Yes, the machine is supplied CE marked. Confirm any additional local requirements for your market with the order so we can prepare the documentation.
What bending length can I order?
The range covers several tonnage and length combinations, for example the 80T3200 build with 3200mm bending length. Send us your longest part and material thickness and we will recommend the model.
What are your trade and payment terms?
FOB CFR and CIF. Payment is 30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
How do I order spares for the hydraulic system?
The system uses Bosch-Rexroth components. Send us your machine model and the item required and we will quote against your machine record.
Request a Quote on the WC67K CNC Hydraulic Press Brake Machine
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.