
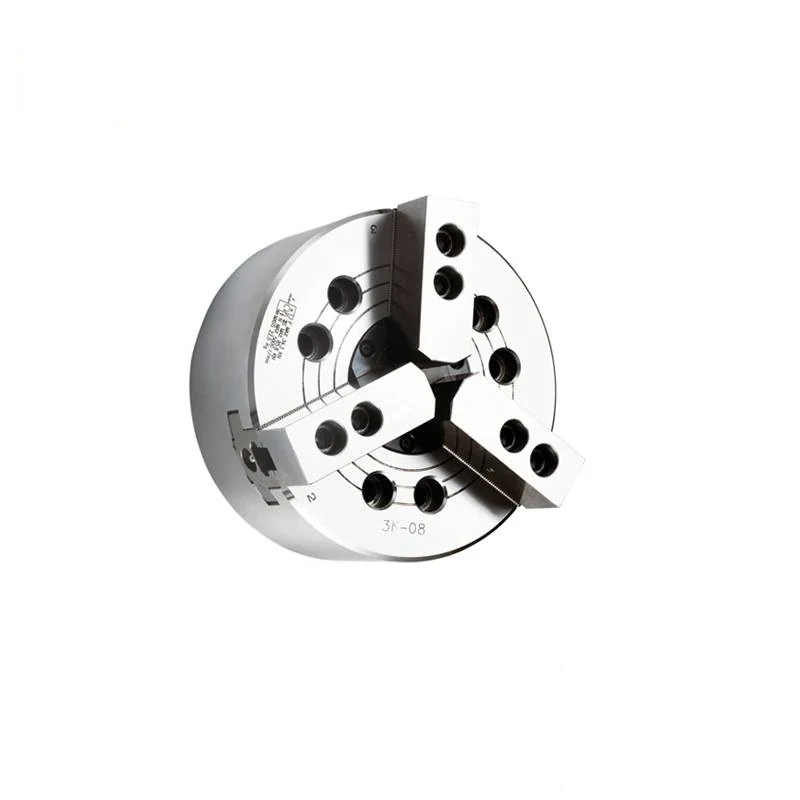
3K Three-Jaw Hollow Power Chuck
The 3K is a three-jaw hollow power chuck for lathes and turning centres that clamp hydraulically through a draw tube instead of by chuck key. The hollow body lets bar stock pass through, so turned parts are produced one after another from a single length of material. Three jaws self-centre, which is the reason this chu...
What This Machine Does
The 3K is a three-jaw hollow power chuck for lathes and turning centres that clamp hydraulically through a draw tube instead of by chuck key. The hollow body lets bar stock pass through, so turned parts are produced one after another from a single length of material. Three jaws self-centre, which is the reason this chuck is the default for round work: the operator loads the bar and the chuck finds the centre rather than the operator dialling it in. Clamping force is high and repeat positioning accuracy is close, so tool offsets hold across a production run and the part does not creep under a roughing cut. The chuck is stable at speed and built to run continuously in automatic production. The range starts at the compact 3K-04 with a 110mm body and runs through 3K-05, 3K-06, 3K-08, 3K-10, 3K-12, 3K-15 and 3K-18 at 450mm, with mountings from A4 to A11.
Why Buyers Choose This Machine
- Hollow body allows bar feeding so parts are turned from a continuous length of stock
- Three self-centring jaws locate round work without individual jaw adjustment
- High clamping force holds the part through roughing and interrupted cuts
- High repeat positioning accuracy keeps tool offsets valid across a production run
- Stable at high speed so workholding does not cap your spindle speed
- Eight sizes from 3K-04 at 110mm to 3K-18 at 450mm cover small to large turned parts
- Mountings from A4 to A11 fit a wide range of lathe spindle noses
Where 3K Three-Jaw Hollow Power Chuck Earns Its Place
Problems It Solves
- Manual chuck keys cannot be used inside an automatic machining cycle
- Clamping force that changes with the operator lets parts pull out under load
- Solid-back chucks block bar feeding so stock must be cut into short billets
- Loss of repeat position between parts means resetting tool offsets on the machine
- Chuck instability at speed forces the programmer to cut the surface speed
Who It Is For
- CNC turning shops running repeat round components
- Production machine shops moving from manual to power clamping
- Machine tool rebuilders fitting workholding to lathes
- Distributors supplying chucks and lathe accessories
Application Scenarios
- Bar fed production turning on CNC lathes
- Repeat turning of shafts bushes and round fittings
- Automatic and unattended production cycles
- Second operation turning where part position must repeat
- Upgrading a manual lathe to power clamping for higher output
Technical Detail
Technical Features
- Three-jaw self-centring hollow power chuck
- High speed stability
- High accuracy of repeat positioning
- Large clamping force suitable for automatic production
- Strong and durable construction
- Through bore machined to H6 tolerance
- Mounting sizes A4 A5 A6 A8 and A11 across the range
Specifications
| Machine type | Three-jaw hollow hydraulic power chuck |
|---|---|
| Models | 3K-04 3K-05 3K-06 3K-08 3K-10 3K-12 3K-15 3K-18 |
| Body diameter A | 110mm 3K-04 135mm 3K-05 169mm 3K-06 210mm 3K-08 254mm 3K-10 304mm 3K-12 381mm 3K-15 450mm 3K-18 |
| Mounting | A4 A5 A6 A8 and A11 according to model |
| Body height B | 59mm 3K-04 60mm 3K-05 81mm 3K-06 91mm 3K-08 100mm 3K-10 110mm 3K-12 133mm 3K-15 |
| Through bore C | 85mm 3K-04 71mm 3K-05 91mm 3K-06 103mm to 109mm 3K-08 113mm to 120mm 3K-10 122mm 3K-12 149mm to 160mm 3K-15 in H6 |
| Jaw count | Three self-centring jaws |
| Application | Automatic production turning and bar work |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Turning
- Bar feeding
- Boring
- Facing
Quality Control
- Through bore machined and checked to H6 tolerance
- Jaw repeat positioning accuracy verified on assembly
- Clamping force checked on the assembled chuck
- Mounting face and register run-out checked
- Chuck run at speed to confirm stability before packing
Customisation Options
- Chuck size selected from 3K-04 to 3K-18 by part and bar diameter
- Mounting specified for your spindle nose from A4 to A11
- Soft or hard jaws quoted for your workpieces
- Draw tube adapter specified for the cylinder on your machine
How It Compares With the Alternatives
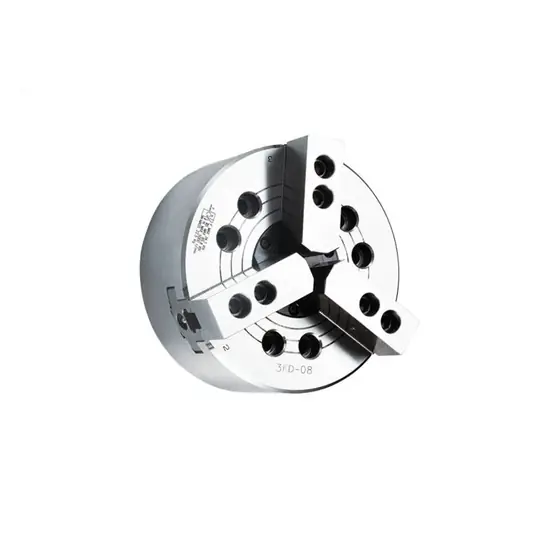
| 3KD three-jaw large through-hole power chuck | The 3KD has the larger through-hole for feeding bigger bar and tube; the 3K covers the same three-jaw duty where the bore requirement is more modest |
|---|---|
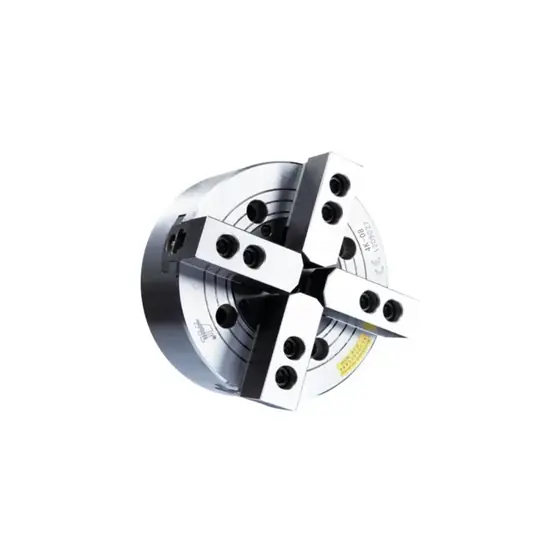
| 4K four-jaw hollow power chuck | The 4K holds irregular and square work on four jaws; the 3K self-centres on round stock and is quicker to load for shaft and bush production |
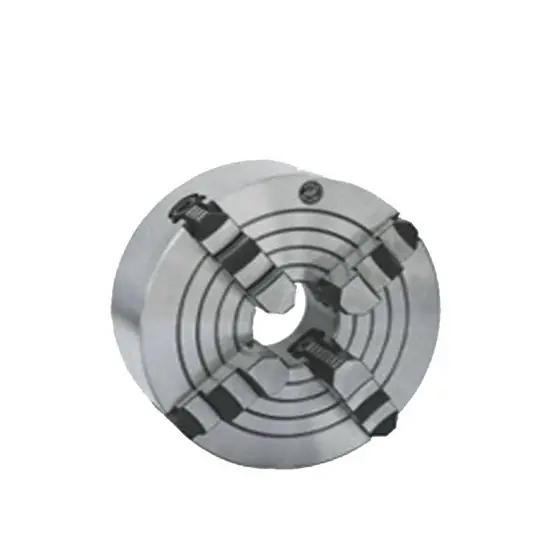
| K72 four-jaw independent chuck | An independent chuck is set jaw by jaw for off-centre work; the 3K clamps hydraulically and repeats position, which is what production turning needs |
Running the Machine
Step 1
Confirm the bar diameter passes through the chuck bore and the spindle
Step 2
Mount the chuck to the matching spindle nose and check run-out on the register
Step 3
Connect the draw tube to the machine cylinder and set clamping pressure
Step 4
Bore soft jaws in place where concentricity matters
Step 5
Clamp a test part and check repeat position over several clamping cycles
Step 6
Grease the jaw slots and wedge mechanism to the maintenance schedule
Step 7
Recheck the clamping pressure whenever you change jaws or part diameter
Related Applications and Guides
Engine Rebuilding Workshops
Engine rebuilding workshops recondition blocks heads crankshafts and valves to a geometry the engine will hold for a full service life. XAIMC supplies
General Machining Job Shops
Job shops take whatever work comes through the door, which means their equipment has to cover a wide range rather than do one thing perfectly. XAIMC s
Gear Hobbing Explained for Buyers of Gear Cutting Machines
Gear hobbing cuts gear teeth by rolling a rotating hob against a rotating blank so that the tooth form is generated rather than copied from a formed c
Radial Drilling Machine vs Bench Drilling Machine
A bench drilling machine brings the work to a fixed spindle, while a radial drilling machine moves the spindle over a heavy stationary workpiece on an
Questions About 3K Three-Jaw Hollow Power Chuck
Which 3K size should I order?
Choose by part diameter, bar diameter and spindle nose. Body diameters run from 110mm on the 3K-04 to 450mm on the 3K-18. Send us your lathe model and typical part and we will confirm.
Will it fit my lathe spindle?
Mountings across the range cover A4, A5, A6, A8 and A11. Tell us your spindle nose designation and we will match the chuck.
What is the difference between the 3K and the 3KD?
Both are three-jaw power chucks. The 3KD is the large through-hole version, intended where you feed larger diameter bar or tube through the spindle.
What clamping force does the chuck develop?
It depends on chuck size and on the draw bar pull available from your machine cylinder. Send us the size and your cylinder data and we will confirm the working figures.
Are jaws included?
Jaws are specified against your work. Tell us the diameters you hold and whether you want soft or hard jaws and we will quote them with the chuck.
How are the chucks packed for export?
Individually packed and shipped from our storehouse in Xi'an. Tell us your port and quantity and we will quote FOB CFR or CIF.
What are your payment terms?
30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
Request a Quote on the 3K Three-Jaw Hollow Power Chuck
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.