Ford CD4 ETC Pad
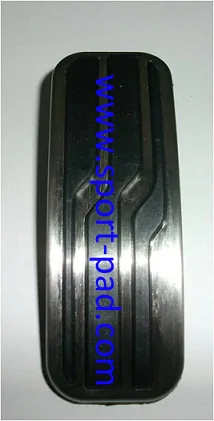
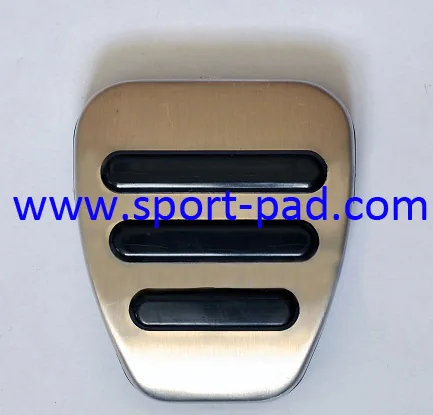
ETC means electronic throttle control: a drive-by-wire accelerator with a hanging pedal, which is why this face is the tallest and slimmest of the CD4 group.
Specification
| Part family | Overmoulded finisher plate |
|---|---|
| Construction | Metal face with moulded rubber inserts |
| Face detail | Tall, slim black-and-stainless face for an electronic throttle pedal. |
| Face finish options | Brushed aluminium, sand blasted stainless steel or polished stainless steel |
| Face marking | Laser etching available on steel components |
| Insert compounds | EPDM, SBR, TPE or TPE-SEBS, to drawing |
| Tooling | Designed and built in house |
| Prototype parts | 4 weeks from prototype tool |
| PPAP | Typically 8 weeks, to ISO/TS 16949 or VDA |
| Dimensions | Built to customer drawing or to a supplied sample |
| Moulded from | Beijing rubber plant (rubber) / Shanghai plant (plastics) |
The face on this part
Tall, slim black-and-stainless face for an electronic throttle pedal. It sits in the Ford Sport Pads group, and the photograph above is of the part itself rather than a rendering — what you see is the tread, the outline and the finish as they leave the tool.
What we need to quote it
A drawing in SolidWorks, Pro-E or UG — a STEP export is fine — or the physical sample, which we will measure and model for your approval. Annual volume and the required PPAP standard complete the picture.
Where it is made and tested
The stainless work and assembly run through our Shanghai and Beijing sites; the rubber insert is moulded in Beijing, where the test equipment sits next to the production line. Hardness, ozone, ageing and oil resistance are all checked there.
How a finisher plate is built
The plate is cut from sheet — laser cut if the material is thin, CNC machined if it is thicker — then finished and married to a moulded rubber insert. On an overmoulded part the plate goes into the rubber tool and the compound is moulded onto and through it, so the two leave as one piece. On a press fit part the insert is moulded separately and pressed home.
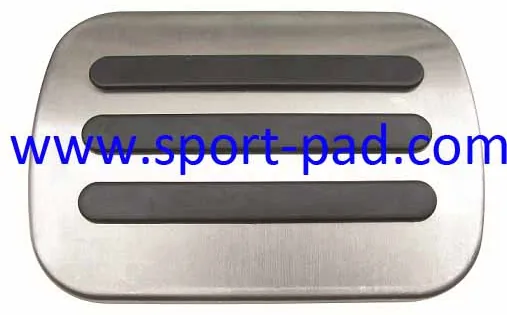
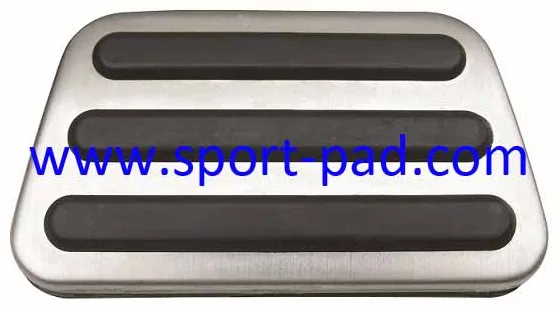
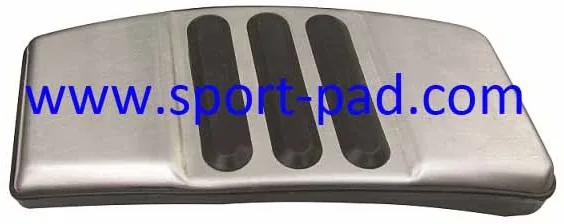
Other parts in Ford Sport Pads
Background reading
Sport Pad or Rubber Pad? The Difference That Decides Your Tooling Cost
A sport pad has a metal face; a rubber pad does not. That single difference drives tooling count, unit price and how the part is validated.
Overmoulding vs Press Fit: Two Ways to Get Rubber Onto a Finisher Plate
Both produce a metal-faced pedal pad. They differ in tooling, in retention and in how easily the part can be pulled apart.
Brushed, Sand Blasted or Polished: Picking a Pedal Face Finish
The three finishes buyers actually ask for, what each one hides, and why a finish change is not a tooling change.
Questions buyers ask
Can the metal face be changed without retooling the rubber?
Yes. The stainless or aluminium blank and the rubber insert are separate tools, so a change of finish — brushed, sand blasted or polished — does not touch the rubber tool. A change to the insert pattern does.
How long before I see a real Ford CD4 ETC Pad sample?
All tooling is designed and made in house, and we deliver parts from a prototype tool in 4 weeks. Full PPAP to ISO/TS 16949 or VDA typically takes a further 8 weeks.
What do you need from us to quote it?
Send the sample if you have no drawing. We will measure it, model it and come back with a drawing for your approval before anything is cut.
How is the material verified?
Our production facilities in Beijing, Shanghai and Wuhan are ISO/TS certified, and the rubber test equipment sits next to the Beijing production line so a bad batch is stopped, not diagnosed later.
Quote the Ford CD4 ETC Pad
Send the annual volume and, if you have one, the drawing. Prototype parts follow 4 weeks after a prototype tool.