Overmoulded Finisher Plates
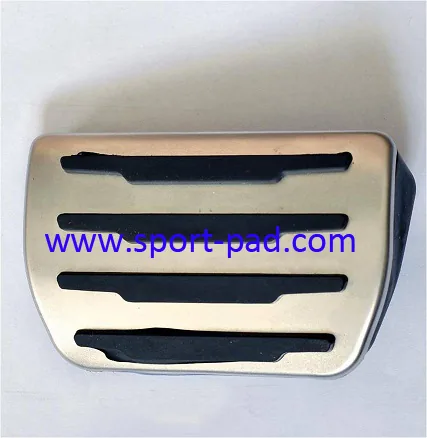
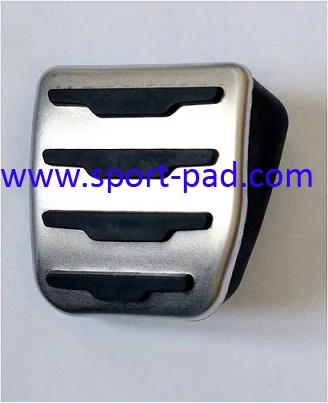
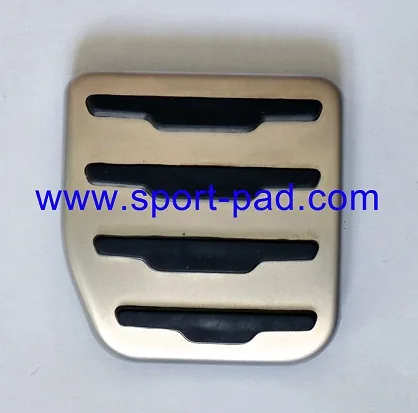
Rubber moulded directly onto a steel or aluminium face, so the insert cannot be levered out.
What it is
The metal face is placed in the rubber tool and the compound is moulded onto and through it in one operation. The result is a single part: there is no adhesive line to fail and no insert that can be picked out of the plate with a fingernail.
When to specify it
Where the pad is visible, where the insert is small enough to be pried at, or where the part has to pass a pull-off test. Most of the sport pads in this catalogue are built this way.
What it costs you
A second tool and a loading step. The metal blank and the rubber insert are separate tools, which is also the advantage: a change of face finish does not touch the rubber tool.
Other capabilities
Press Fit Finishers
A separately moulded rubber insert pressed into the finisher plate — the lower-tooling route to the same look.
Rubber Compound Selection
EPDM, SBR, TPE, TPE-SEBS, PVC and PP — and the test data that tells you which one the part actually needs.
Metal Face Finishing
Brushed aluminium, sand blasted or polished stainless steel, plus laser etching, laser cutting and CNC machining.
Prototype to PPAP
Parts from a prototype tool in 4 weeks; full PPAP to ISO/TS 16949 or VDA typically in 8 weeks.
In-House Tooling
Every tool behind these parts was designed and built in our own shop.
Questions buyers ask
Is this quoted separately or inside the part price?
Inside the part price, unless it is a one-off engineering activity such as tooling. Tooling is always quoted as its own line.
How early do I need to decide this?
Before the production tool is cut. The prototype stage — parts 4 weeks from a prototype tool — exists precisely so these decisions can still be changed.
Who do I talk to about it?
Our designers, not only a salesperson. The team works in SolidWorks, Pro-E and UG and sits in the same buildings as the tool shop in Shanghai and Beijing.
Need overmoulded finisher plates?
Send the drawing or the sample and we will tell you what it takes to make it here — tooling, compound and timing.