
AKJ301 Sintered Flux for Submerged Arc Welding of Carbon and Low Alloy Steels.
A silicon-manganese type sintered flux with basicity of about 1.0, designed for stable arc, clean slag removal, and excellent mechanical properties in circular seam and multi-pass welding applications.
Product Overview
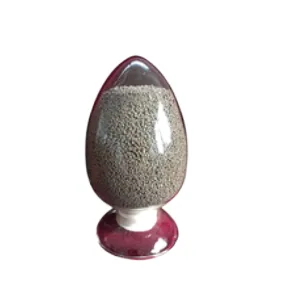
AKJ301 is a sintered flux with a basicity of about 1.0, formulated for submerged arc welding of ordinary carbon steel and certain low alloy steels. It consists of black-gray round particles with a size range of 10~60 mesh (approximately 2.0~0.28 mm).
The flux is compatible with both DC and AC power supplies, and when using DC, the welding wire must be connected to the positive pole. It provides a stable arc, a well-shaped weld bead, and slag that detaches easily without flowing during welding.
It is especially suited for welding circular seams, where short slag and no flow are critical for consistent weld quality. The deposited metal exhibits good low temperature impact toughness and is suitable for multi-pass, double-sided single-pass, and multi-wire submerged arc welding.
Application: With corresponding welding wires (such as H08A, H08E, HO8MnA, etc.), it is mainly used for welding ordinary carbon steel and some low alloy steels (such as Q235, X65, etc.) structures and submerged arc welding of boiler pressure vessels, ships, bridges, oil pipelines, etc. The deposited metal has good low temperature impact toughness. It can be used for multi-pass welding, double-sided single-pass welding, and multi-wire submerged arc welding.
Key Benefits
Stable Arc and Clean Weld Bead.
The flux delivers a stable arc across a range of welding currents, resulting in a consistent, well-formed weld bead with minimal spatter and no slag flow during welding.
Easy Slag Removal
The slag produced is thin and lifts off easily after welding, reducing post-weld cleaning time and minimizing the risk of slag entrapment in subsequent passes.
Excellent Mechanical Properties
The deposited metal achieves good mechanical properties, including high impact toughness at low temperatures, suitable for demanding structural applications.
Suitable for Complex Welding Configurations.
Designed for circular seams, multi-pass welding, double-sided single-pass, and multi-wire welding, making it versatile for complex fabrication tasks.
Where It Is Used
- Submerged arc welding of ordinary carbon steel structures.
- Welding of low alloy steels such as Q235 and X65.
- Boiler and pressure vessel fabrication.
- Shipbuilding and bridge construction.
- Oil pipeline and structural steel welding.
Who It Is For
- Welding consumable distributors supplying flux for industrial fabrication.
- Fabricators working with carbon and low alloy steels in structural and pressure applications.
- Contractors involved in pipeline, ship, and bridge construction requiring reliable flux for circular and multi-pass welds.
Problems It Solves
- Inconsistent slag behavior and flow during circular seam welding due to poor flux formulation.
- Difficult slag removal and increased post-weld cleaning time from fluxes with stubborn slag.
- Lack of low temperature impact toughness in deposited metal for cold climate or safety-critical applications.
Specifications
Published by the factory for AKJ301. Values not shown are not published on the datasheet and are marked as such rather than estimated.
| Element | Content |
|---|---|
| SiO₂+TiO₂ | 25.0-35.0 |
| CaO+MgO | 15.0-25.0 |
| S | 0.06 |
| P | 0.08 |
| CaF₂ | 5.0-15.0 |
| Al₂O₃+MnO | 30.0-40.0 |
Mechanical property data for this grade is not published on the factory datasheet. Ask our technical team for the test record before you qualify it.
Size: 10-60
Technical Features
- Silicon-manganese type sintered flux with basicity of about 1.0.
- Particle size: 10~60 mesh (approximately 2.0~0.28 mm)
- Compatible with DC and AC power supplies; welding wire connected to positive pole when using DC.
- Suitable for multi-pass, double-sided single-pass, and multi-wire submerged arc welding.
- Chemical composition includes SiO₂+TiO₂ (25.0-35.0%), CaO+MgO (15.0-25.0%), CaF₂ (5.0-15.0%), Al₂O₃+MnO (30.0-40.0%), S (0.06%), P (0.08%)
- Deposited metal has good low temperature impact toughness.
Use Guide
- Select appropriate welding wire such as H08A, H08E, or HO8MnA based on base metal and joint requirements.
- Ensure the flux is kept dry and stored in sealed packaging to prevent moisture absorption.
- Use DC power supply with the welding wire connected to the positive pole for optimal arc stability.
- Maintain proper flux layer thickness and travel speed to achieve consistent weld bead shape and slag coverage.
- Clean slag completely between passes to avoid contamination and ensure sound weld metal.
How It Compares
AKJ301 is a silicon-manganese type sintered flux with basicity of about 1.0, differing from basic fluxes which have higher basicity and are used for high-strength or low-hydrogen applications. It offers better slag control and easier removal than some high-silica fluxes, which can produce more viscous slag. Compared to fused fluxes, sintered fluxes like AKJ301 typically provide better slag fluidity and are more forgiving in variable welding conditions.
Related Grades
Other welding flux in the same family.
AKJ301 Questions
What is the particle size range of AKJ301?
Which welding wires are recommended with AKJ301?
What are the key chemical components in AKJ301?
Can AKJ301 be used with AC power supply?
What packing is AKJ301 supplied in?
Can we test AKJ301 before placing a production order?
Request a Quotation for AKJ301
Send the diameter, the quantity and the destination port. Our technical team replies with packing, pricing and the data you need to qualify the grade.