
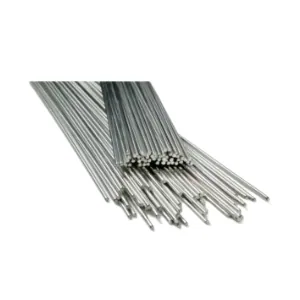
AK-ER4047 Aluminum-Silicon Welding Wire for Cast and Al-Mg-Si Alloys.
An aluminum-silicon eutectic alloy wire suitable for TIG and MIG welding of cast aluminum, 2000 series, and Al-Mg-Si series alloys, with performance comparable to ER4043.
Product Overview
AK-ER4047 is an aluminum-silicon eutectic alloy welding wire used for TIG and MIG welding. It is designed for joining cast aluminum, 2000 series, and Al-Mg-Si series aluminum alloys.
The wire has a chemical composition that results in good weldability and mechanical properties similar to ER4043, making it a suitable alternative for applications requiring high ductility and crack resistance in the weld zone.
Application: Suitable for welding cast aluminum, 2000 series and Al-Mg-Si series aluminum alloys.
Key Benefits
Eutectic Composition for Good Fluidity.
The 11.0-13.0 percent silicon content forms a eutectic structure that improves fluidity in the molten pool, reducing the risk of solidification cracking in the weld.
Low Iron and Copper Content.
With iron limited to ≤0.80 percent and copper to ≤0.30 percent, the wire minimizes the risk of hot cracking and maintains good corrosion resistance in the weld deposit.
Suitable for Soldering Applications.
The wire can be used as a solder in low-temperature joining processes where aluminum-silicon alloys are required.
Compatibility with Common Aluminum Alloys.
It is recommended for welding cast aluminum, 2000 series, and Al-Mg-Si series alloys, where good mechanical properties and crack resistance are needed.
Where It Is Used
- Welding of cast aluminum components.
- Joining 2000 series aluminum alloys.
- Repair and fabrication of Al-Mg-Si series aluminum structures.
- Low-temperature soldering applications requiring aluminum-silicon filler metal.
Who It Is For
- Welding consumable distributors supplying aluminum welding wires.
- Fabricators working with cast aluminum and high-strength aluminum alloys.
- Maintenance teams repairing aluminum structures and components in industrial settings.
Problems It Solves
- Matching filler metal chemistry to cast aluminum and 2000 series alloys where hot cracking is a concern.
- Finding a wire with mechanical properties and weldability similar to ER4043 but with a different silicon content for specific joint requirements.
- Sourcing a single wire that can serve both welding and soldering applications in aluminum fabrication.
Specifications
Published by the factory for AK-ER4047 (TIG / MIG). Values not shown are not published on the datasheet and are marked as such rather than estimated.
| Standard | Designation |
|---|---|
| Classification 1 | EN ISO 18273 S Al 4047 |
| Classification 2 | AWS A5.10 ER4047 |
| Classification 3 | GB/T 10858 SAl 4047 |
| Element | Content |
|---|---|
| Si | 11.0-13.0 |
| Fe | ≤0.80 |
| Cu | ≤0.30 |
| Mn | 0.15 |
| Mg | 0.10 |
| Zn | ≤0.20 |
| Al | Bal |
| Be | ≤0.0003 |
| Property | Value |
|---|---|
| Tensile strength (MPa) | 175 |
| Yield Stress (MPa) | 125 |
| Elongation (%) | 14 |
Technical Features
- Aluminum-silicon eutectic alloy with 11.0-13.0 percent silicon.
- Iron content ≤0.80 percent, copper ≤0.30 percent, manganese 0.15 percent, magnesium 0.10 percent, zinc ≤0.20 percent, beryllium ≤0.0003 percent.
- Balanced aluminum base with trace elements to control solidification and mechanical behavior.
- Supplied to EN ISO 18273 S Al 4047, AWS A5.10 ER4047, and GB/T 10858 SAl 4047 standards.
- Deposited metal tensile strength of at least 175 MPa, yield stress of at least 125 MPa, elongation of at least 14 percent.
Use Guide
- Select wire diameter based on joint thickness and welding process; ensure compatibility with the welding machine and shielding gas (typically argon or argon-helium mix).
- Clean the base metal surface thoroughly to remove oil, oxide, and moisture before welding to avoid contamination and porosity.
- Use proper shielding gas flow rates and torch angles to maintain a stable arc and consistent weld bead.
- Avoid excessive heat input to prevent grain coarsening and reduce the risk of cracking in the weld zone.
How It Compares
AK-ER4047 and ER4043 both provide aluminum-silicon filler metal for welding aluminum alloys, but ER4047 has a higher silicon content (11.0-13.0 percent vs. ER4043 offers higher strength and better ductility in some applications, while AK-ER4047 is better suited for cast aluminum and alloys prone to hot cracking. For applications requiring lower silicon content, ER4043 may be preferred.
Related Grades
Other welding and brazing rods in the same family.
AK-ER4047 (TIG / MIG) Questions
What standards does AK-ER4047 meet?
What is the silicon content range in AK-ER4047?
What are the mechanical properties of the deposited metal?
Can this wire be used for soldering?
What packing is AK-ER4047 (TIG / MIG) supplied in?
Can we test AK-ER4047 (TIG / MIG) before placing a production order?
Request a Quotation for AK-ER4047 (TIG / MIG)
Send the diameter, the quantity and the destination port. Our technical team replies with packing, pricing and the data you need to qualify the grade.