
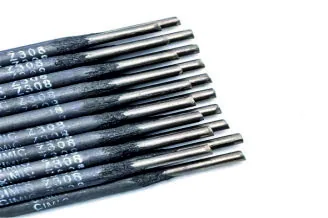
AK-J100SD Low Hydrogen Sodium Coated Electrode for High Strength Steel Welding.
A high strength, low hydrogen sodium coated electrode for all-position welding of B950CF and similar high-strength steel applications requiring excellent crack resistance and low-temperature toughness.
Product Overview
AK-J100SD is a low hydrogen sodium coated electrode designed for all-position manual metal arc welding of high strength steels. It is suitable for welding B950CF and other steel grades with comparable strength levels, particularly in hydraulic pressure pipelines and related structural applications.
The electrode delivers excellent weld metal properties with tensile strength of at least 1005 MPa and yield stress of at least 869 MPa. It maintains impact energy of at least 85 J at minus 40 degrees C and diffused hydrogen content of no more than 4.0 mL per 100 g of molten metal, measured by mercury or thermal conductivity method.
Welding is performed using direct current reverse polarity (DC) with recommended current ranges provided for each diameter. The coating ensures stable arc performance and good slag detachability, supporting clean, crack-resistant welds.
Application: AK-J100SD is a high strength steel electrode with low hydrogen sodium coating. DC reverse connection can be used for all-position welding. Excellent welding process performance, low hydrogen diffusion in weld, with excellent low-temperature toughness and crack resistance. Mainly used for B950CF and the corresponding strength level of hydraulic pressure pipeline welding and installation.
Key Benefits
High Strength and Toughness.
Deposited metal achieves tensile strength of at least 1005 MPa and yield stress of at least 869 MPa, with impact energy of at least 85 J at minus 40 degrees C, meeting the demands of high-strength steel applications.
Low Hydrogen Diffusion
Diffused hydrogen content in the molten metal is limited to 4.0 mL per 100 g, reducing the risk of hydrogen-induced cracking in high-strength and thick-section welds.
Excellent Crack Resistance
The low hydrogen sodium coating and controlled chemical composition provide high resistance to cold cracking, especially in thick or constrained joints.
All-Position Welding Capability
DC reverse polarity allows welding in flat, horizontal, vertical, and overhead positions, enabling consistent performance across different joint orientations.
Where It Is Used
- Welding of B950CF and equivalent high-strength steel pressure pipelines.
- Hydraulic and high-pressure system fabrication and installation.
- Structural components requiring high strength and low-temperature toughness.
- Critical joints in heavy industrial equipment where crack resistance is essential.
Who It Is For
- Welding consumable distributors supplying high-strength steel electrodes.
- Fabricators and EPC contractors working with B950CF and similar high-strength steels.
- Pipeline and pressure vessel welders requiring low hydrogen, crack-resistant electrodes.
Problems It Solves
- Achieving required mechanical properties and low-temperature toughness in high-strength steel welds without compromising crack resistance.
- Reducing the risk of hydrogen-induced cracking in thick-section or high-constraint joints through low hydrogen diffusion and proper post-weld treatment.
- Providing a single electrode solution for all-position welding of high-strength steel, avoiding the need for multiple consumables.
Specifications
Published by the factory for AK-J100SD. Values not shown are not published on the datasheet and are marked as such rather than estimated.
| Standard | Designation |
|---|---|
| Classification | EN ISO —— AWS —— GB/T —— |
| Element | Content |
|---|---|
| C | 0.04 |
| Si | 0.16 |
| Mn | ≥1.90 |
| S | 0.004 |
| P | 0.008 |
| Ni | 3.07 |
| Mo | 0.52 |
| Cr | 0.96 |
| V | 0.01 Mechanical |
| Tensile strength (MPa) | ≥1005 |
| Yield Stress (MPa) | ≥869 |
| Elongation (%) | ≥18.5 |
| Impact values (J) | 85J/-40℃ Diffused hydrogen |
| content of molten metal | ≤4.0mL/100g(mercury method or thermal conductivity method) Molten metal |
| Grade I Recommended parameters | (Polarity: |
| DC) 2.5mm | F(H)-70-100A/ |
| V(OH)-60-90A 3.2mm | F(H)-90-130A/ |
| V(OH)-80-120A 4.0mm | F(H)-140-170A/ |
| V(OH)-130-150A 5.0mm | F(H)-170-210A |
Mechanical property data for this grade is not published on the factory datasheet. Ask our technical team for the test record before you qualify it.
Note: 1. The welding rod must be baked at 380 ° C for 1-2 hours before use, and put into 100- 150 ° C incubator, 2. welding should be thoroughly removed the surface of the weld rust, oil, moisture and other impurities. 3. After welding, 180 ° C ~ 250 ° C hydrogen elimination treatment was carried out (holding time was decided by plate thickness) . 4. Use short arc and narrow pass during welding
Technical Features
- Low hydrogen sodium coating for improved crack resistance and weld metal cleanliness.
- Deposited metal tensile strength at least 1005 MPa, yield stress at least 869 MPa, elongation at least 18.5 percent.
- Impact energy at least 85 J at minus 40 degrees C, diffused hydrogen content no more than 4.0 mL/100g.
- Available in 2.5 mm, 3.2 mm, 4.0 mm, and 5.0 mm diameters with specified current ranges for each.
- Chemical composition includes carbon 0.04%, silicon 0.16%, manganese ≥1.90%, sulfur 0.004%, phosphorus 0.008%, nickel 3.07%, molybdenum 0.52%, chromium 0.96%, vanadium 0.01%
Use Guide
- Bake electrodes at 380 °C for 1–2 hours before use, then store in an incubator at 100–150 °C until welding.
- Clean weld surfaces thoroughly to remove rust, oil, moisture, and other contaminants before welding.
- Use short arc and narrow pass techniques during welding to control heat input and minimize distortion.
- Perform hydrogen elimination treatment at 180–250 °C after welding, with holding time based on plate thickness.
How It Compares
AK-J100SD is a low hydrogen sodium coated electrode suitable for high-strength steel welding. It differs from rutile-coated electrodes like E6013 in that it provides higher strength and lower hydrogen content, making it appropriate for critical structural and pressure applications. Unlike cellulosic electrodes, it offers better control and lower spatter but requires stricter pre- and post-weld procedures. It is not intended for general-purpose mild steel welding where lower strength and higher hydrogen levels are acceptable.
Related Grades
Other welding electrodes in the same family.

AK-J100SD Questions
What are the recommended welding parameters for each diameter?
What is the diffused hydrogen content in the weld metal?
What is the minimum impact toughness of the deposited metal?
What pre-weld and post-weld treatments are required?
What packing is AK-J100SD supplied in?
Can we test AK-J100SD before placing a production order?
Request a Quotation for AK-J100SD
Send the diameter, the quantity and the destination port. Our technical team replies with packing, pricing and the data you need to qualify the grade.