
AK-J80SD Ultra-Low Hydrogen Low Alloy Electrode for High-Strength Applications.
A high-strength, low-alloy electrode with excellent crack resistance and low-temperature toughness, designed for demanding applications in hydroelectric, marine, and oil pipeline construction.
Product Overview
AK-J80SD is an ultra-low hydrogen low alloy electrode formulated for high-strength welding applications. It delivers excellent mechanical performance, including high toughness and resistance to cracking in the deposited metal.
The electrode is suitable for welding base metals with a strength level of 800 MPa, including spiral cases in hydroelectric power equipment, pressure pipelines, marine structures, and oil pipelines requiring matching strength and durability.
Application: AK-J80SD is an ultra-low hydrogen low alloy electrode with high strength and toughness. It has excellent welding performance, low temperature impact toughness and crack resistance of deposited metal. It is suitable for the welding of spiral case and 800MPA base metal of pressure pipeline in water power equipment, and the welding of marine engineering ship and oil pipeline with the same strength.
Key Benefits
High Strength and Toughness.
The deposited metal achieves high tensile strength and maintains impact toughness at low temperatures, meeting the demands of critical structural applications under stress and cold conditions.
Excellent Crack Resistance
The ultra-low hydrogen formulation reduces the risk of hydrogen-induced cracking, particularly important in high-strength steels and thick-section welds.
Low-Temperature Impact Performance
The electrode produces weld metal with proven resistance to brittle fracture at low temperatures, ensuring reliability in cold environments.
Stable Welding Performance
The electrode provides consistent arc stability and good bead appearance, supporting reliable welding across various positions and joint types.
Where It Is Used
- Welding of spiral cases in hydroelectric power equipment.
- Joining 800 MPa strength pressure pipelines in water power systems.
- Marine engineering ship structures requiring high-strength welds.
- Oil and gas pipelines with matching high-strength base metals.
Who It Is For
- Pressure vessel and boiler makers working with high-strength low-alloy steels.
- Hydroelectric and marine engineering contractors requiring crack-resistant welds.
- Pipeline and oil & gas fabricators needing consistent, certified consumables for critical joints.
Problems It Solves
- Achieving weld metal properties that meet code requirements for high-strength, low-alloy steels without relying on multiple electrode types.
- Preventing hydrogen-induced cracking in thick-section or high-stress welds through ultra-low hydrogen electrode design.
- Ensuring consistent performance across long weld runs by using a single, well-characterized electrode for demanding applications.
Specifications
Published by the factory for AK-J80SD. Values not shown are not published on the datasheet and are marked as such rather than estimated.
| Standard | Designation |
|---|---|
| Classification 1 | EN ISO —— AWS A5.5 E1101S-G H4 |
| Classification 2 | GB/T 32533 E7815-G |
| Element | Content |
|---|---|
| C | 0.10 |
| Si | 0.60 |
| Mn | ≥1.30 |
| S | 0.015 |
| P | 0.020 |
| Ni | ≥2.00 |
| Mo | 0.60 |
| Cr | 0.60 |
Mechanical property data for this grade is not published on the factory datasheet. Ask our technical team for the test record before you qualify it.
Note: 1. The electrode is baked at 380 ° C for 1 ~ 2 hours before use, and then put into 100 ~ 150 ° C incubator. 2. must be removed before the welding surface of water, oil, rust and other impurities. 3. Arc-starting and return transportation technology or arc-starting plate should be used to strengthen arc. 4. according to the plate thickness and steel grade, using different temperature for appropriate preheating. 5. Apply short arc and narrow weld bead during welding
Technical Features
- Supplied to EN ISO —— AWS A5.5 E1101S-G H4 and GB/T 32533 E7815-G classifications.
- Chemical composition includes C: 0.10%, Si: 0.60%, Mn: ≥1.30%, S: 0.015%, P: 0.020%, Ni: ≥2.00%, Mo: 0.60%, Cr: 0.60%
- Designed for base metals with a minimum yield strength of 800 MPa.
- Requires pre-baking at 380 °C for 1–2 hours before use, then stored at 100–150 °C until welding.
Use Guide
- Bake electrodes at 380 °C for 1–2 hours prior to use, then store in a 100–150 °Cholding oven until welding.
- Clean the welding surface thoroughly to remove water, oil, rust, and other contaminants before striking the arc.
- Use arc-starting plates or arc-backing techniques to ensure stable arc initiation and avoid defects at the start of the weld.
- Apply appropriate preheating based on plate thickness and base metal grade to reduce hardening and cracking risk.
- Maintain a short arc length and narrow weld bead during welding to control heat input and minimize distortion.
How It Compares
AK-J80SD is a high-strength, ultra-low hydrogen electrode designed for 800 MPa base metals. It differs from standard low-alloy electrodes by offering enhanced crack resistance and low-temperature toughness. It is not intended for general-purpose mild steel welding. For lower strength applications, electrodes with lower hydrogen content and different alloying elements may be more suitable.
Related Grades
Other welding electrodes in the same family.

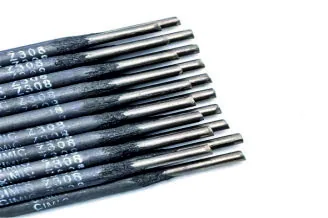
AK-J80SD Questions
What standards does AK-J80SD meet?
What is the chemical composition of the deposited metal?
What pre-welding treatment is required?
What welding techniques are recommended?
What packing is AK-J80SD supplied in?
Can we test AK-J80SD before placing a production order?
Request a Quotation for AK-J80SD
Send the diameter, the quantity and the destination port. Our technical team replies with packing, pricing and the data you need to qualify the grade.