
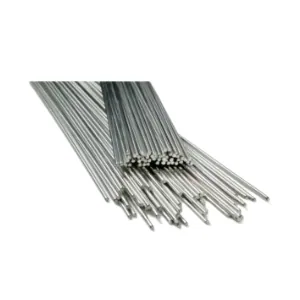
AK-ER5183 Aluminum-Magnesium Welding Wire for TIG and MIG Welding.
A high-strength aluminum-magnesium alloy wire with excellent crack and corrosion resistance, ideal for welding aluminum-magnesium and aluminum-zinc-magnesium alloys in demanding applications.
Product Overview
AK-ER5183 is an aluminum-magnesium welding wire containing magnesium and manganese, formulated for use in gas tungsten arc welding (GTAW) and gas metal arc welding (GMAW). It delivers excellent crack resistance, corrosion resistance, and high strength in the deposited weld metal.
The wire exhibits stable arc performance, minimal spatter, and produces a smooth, aesthetically pleasing weld bead, making it suitable for critical joints in offshore platforms, cryogenic vessels, railway locomotives, and automotive components.
Application: It is suitable for argon arc welding of aluminum-magnesium alloys and aluminum zinc magnesium alloys, and is one of the most commonly used aluminum alloy welding wires. It is often used in aluminum alloy welding related to offshore pla tforms, cryogenic vessels, railway locomotives and automobile industries.
Key Benefits
High Strength and Crack Resistance.
With magnesium content between 4.30% and 5.20%, AK-ER5183 provides high tensile strength and resistance to solidification cracking in welded joints, especially in thick-section or high-stress applications.
Excellent Corrosion Resistance
The balanced composition, including controlled levels of chromium and manganese, enhances resistance to atmospheric and aqueous corrosion, suitable for marine and cryogenic environments.
Stable Arc and Low Spatter.
The wire ensures consistent arc stability and minimal spatter during TIG and MIG welding, reducing post-weld cleaning and improving process efficiency.
Smooth and Aesthetic Weld Bead.
The deposited weld metal forms a clean, uniform bead profile with good fusion, reducing the need for grinding or finishing.
Where It Is Used
- Welding of aluminum-magnesium alloys in offshore platforms and marine structures.
- Joining cryogenic vessels and low-temperature service components.
- Railway locomotive and rolling stock fabrication.
- Automotive body and structural parts made from aluminum alloys.
Who It Is For
- Welding consumable distributors supplying aluminum welding wires for industrial and transport sectors.
- Fabricators working with aluminum-magnesium and aluminum-zinc-magnesium alloys.
- Maintenance teams in offshore, rail, and automotive industries requiring reliable, code-compliant filler metal.
Problems It Solves
- Achieving crack-free welds in high-magnesium aluminum alloys prone to solidification cracking during welding.
- Meeting corrosion resistance requirements in marine and cryogenic environments without compromising strength.
- Reducing spatter and post-weld cleanup in automated or high-productivity TIG and MIG welding operations.
Specifications
Published by the factory for AK-ER5183 (TIG / MIG). Values not shown are not published on the datasheet and are marked as such rather than estimated.
| Standard | Designation |
|---|---|
| Classification 1 | EN ISO 18273 S Al 5183 |
| Classification 2 | AWS A5.10 ER5183 |
| Classification 3 | GB/T 10858 SAl 5183 |
| Element | Content |
|---|---|
| Si | 0.40 |
| Fe | ≤0.40 |
| Cu | ≤0.10 |
| Mn | 0.50-1.0 |
| Mg | 4.30-5.20 |
| Zn | ≤0.25 |
| Al | Bal |
| Be | ≤0.0005 |
| Cr | 0.05-0.25 |
| Ti | 0.15 |
| Property | Value |
|---|---|
| Tensile strength (MPa) | 302 |
| Yield Stress (MPa) | 208 |
| Elongation (%) | 16 |
Technical Features
- Complies with EN ISO 18273 S Al 5183, AWS A5.10 ER5183, and GB/T 10858 SAl 5183 standards.
- Chemical composition includes Mg 4.30–5.20%, Mn 0.50–1.0%, Cr 0.05–0.25%, Ti 0.15%, Si ≤0.40%, Fe ≤0.40%, Cu ≤0.10%, Zn ≤0.25%, Be ≤0.0005%
- Deposited metal tensile strength of at least 302 MPa, yield stress of at least 208 MPa, elongation of at least 16%
- Suitable for GTAW and GMAW processes with argon shielding gas.
Use Guide
- Select wire diameter based on joint thickness and welding position; ensure compatibility with the welding machine and gas flow settings.
- Clean the base metal surface thoroughly from oil, grease, oxide, and moisture before welding to prevent porosity and contamination.
- Use pure argon shielding gas with a flow rate appropriate for the welding current and joint configuration.
- Maintain consistent travel speed and torch angle to achieve uniform bead appearance and full penetration.
How It Compares
AK-ER5183 is designed for high-strength, crack-resistant welds in aluminum-magnesium alloys. It differs from ER5356, which has lower magnesium and is used for general-purpose aluminum welding. ER5183 offers higher strength and better resistance to hot cracking but may require more precise heat control than lower-magnesium grades. For applications requiring maximum corrosion resistance in chloride environments, ER5554 may be considered, though it has lower strength than ER5183.
Related Grades
Other welding and brazing rods in the same family.
AK-ER5183 (TIG / MIG) Questions
What standards does AK-ER5183 meet?
What are the mechanical properties of the deposited metal?
What is the magnesium content range in AK-ER5183?
Can I get technical data and packaging details before ordering?
What packing is AK-ER5183 (TIG / MIG) supplied in?
Can we test AK-ER5183 (TIG / MIG) before placing a production order?
Request a Quotation for AK-ER5183 (TIG / MIG)
Send the diameter, the quantity and the destination port. Our technical team replies with packing, pricing and the data you need to qualify the grade.