
AKJ101 Sintered Flux for Submerged Arc Welding of Low Carbon and Low Alloy Steel.
A fluorine-alkali sintered flux with alkalinity of about 1.8, designed for stable arc and clean welds when used with matching welding wires on low carbon and low alloy steel structures.
Product Overview
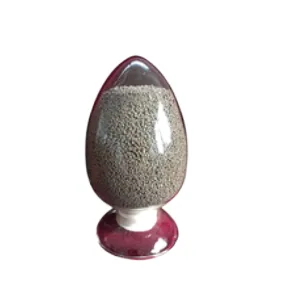
AKJ101 is a fluorine-alkali sintered flux with an alkalinity of approximately 1.8. It consists of gray round particles with a size range of 10 to 60 mesh (about 2.0 to 0.28 mm).
The flux is suitable for both DC and DC power supply, with the welding wire connected to the positive pole when using DC. It delivers a stable arc, a well-shaped weld bead, and slag that melts easily during welding.
When used with compatible welding wires such as H08MnA, H10Mn2, JH-WQ1, JH-WGX2, and others, AKJ101 is primarily applied in submerged arc welding of low carbon steel and certain low alloy steel structures including 16Mn, X65, X70, 14MnNiq, WQ490D, WQ490E, and Q345C.
The deposited metal exhibits good low temperature impact toughness, making it suitable for applications requiring reliable performance under cold conditions.
Application: with the corresponding welding wire (such as H08MnA, H10Mn2, JH- WQ1, JH-WGX2, etc.), mainly used for welding low carbon steel and some low alloy steel (such as 16Mn, x65, X70, 14MnNiq, WQ490D, WQ490E, Q345C etc.) structures and submerged arc welding of boiler pressure vessels, ships, bridges, oil pipelines, etc. Deposited metal has; good low temperature impact toughness.
Key Benefits
Stable Arc with DC Power.
The flux maintains a stable arc when used with DC power supply, especially when the welding wire is connected to the positive pole, ensuring consistent weld quality.
Clean Weld Bead and Easy Slag Removal.
The slag produced melts easily and does not adhere strongly to the weld surface, reducing the need for post-weld cleaning and minimizing the risk of slag inclusions.
Good Low Temperature Impact Toughness.
The deposited metal achieves good impact toughness at low temperatures, supporting safe performance in service environments where cold resistance is required.
Compatibility with Multiple Base Metals.
Designed for use with low carbon steel and low alloy steels such as 16Mn, X65, X70, 14MnNiq, WQ490D, WQ490E, and Q345C, supporting diverse industrial applications.
Where It Is Used
- Submerged arc welding of low carbon steel structures.
- Welding of low alloy steel components including 16Mn, X65, X70, 14MnNiq, WQ490D, WQ490E, and Q345C.
- Boiler and pressure vessel fabrication.
- Shipbuilding and bridge construction.
- Oil pipeline and structural steel welding.
Who It Is For
- Welding consumable distributors supplying flux for industrial fabrication.
- Fabricators working with low carbon and low alloy steel in structural and pressure applications.
- Contractors involved in shipbuilding, pipeline, and bridge projects requiring consistent submerged arc welding performance.
Problems It Solves
- Achieving stable arc and consistent weld quality when using DC power with the welding wire connected to the positive pole.
- Reducing post-weld cleaning time due to slag that melts easily and does not stick to the weld surface.
- Meeting low temperature impact toughness requirements in critical joints without changing flux type.
Specifications
Published by the factory for AKJ101. Values not shown are not published on the datasheet and are marked as such rather than estimated.
| Element | Content |
|---|---|
| SiO₂+TiO₂ | 15.0-25.0 |
| CaO+MgO | 25.0-35.0 |
| S | 0.06 |
| P | 0.08 |
| CaF₂ | 15.0-25.0 |
| Al₂O₃+MnO | 20.0-30.0 |
Mechanical property data for this grade is not published on the factory datasheet. Ask our technical team for the test record before you qualify it.
Size: 10-60
Technical Features
- Fluorine-alkali sintered flux with alkalinity of about 1.8.
- Particle size: 10 to 60 mesh (approximately 2.0 to 0.28 mm)
- Suitable for DC and DC power supply; welding wire connected to positive pole when using DC.
- Chemical composition: SiO₂+TiO₂ 15.0–25.0%, CaO+MgO 25.0–35.0%, CaF₂ 15.0–25.0%, Al₂O₃+MnO 20.0–30.0%, S ≤ 0.06%, P ≤ 0.08%
- Deposited metal has good low temperature impact toughness.
Use Guide
- Select the appropriate welding wire such as H08MnA, H10Mn2, JH-WQ1, or JH-WGX2 based on the base metal and application.
- Use DC power supply with the welding wire connected to the positive pole for optimal arc stability and weld quality.
- Ensure the flux is stored in a dry environment and protected from moisture before use.
- Clean the joint surfaces of oil, rust, paint, and moisture prior to welding to prevent defects in the deposited metal.
How It Compares
AKJ101 is a fluorine-alkali sintered flux with alkalinity of about 1.8, differing from basic fluxes which have higher alkalinity and are used for high-strength or low-hydrogen applications. It is not intended for use with high-alloy or stainless steels. Compared to other sintered fluxes, AKJ101 offers a balance of arc stability, slag fluidity, and mechanical properties suitable for low carbon and low alloy steel welding.
Related Grades
Other welding flux in the same family.
AKJ101 Questions
What is the particle size range of AKJ101 flux?
Which welding wires are compatible with AKJ101?
What is the alkalinity of AKJ101 flux?
Can AKJ101 be used with AC power supply?
What packing is AKJ101 supplied in?
Can we test AKJ101 before placing a production order?
Request a Quotation for AKJ101
Send the diameter, the quantity and the destination port. Our technical team replies with packing, pricing and the data you need to qualify the grade.